Late multi cable transit 1 delivery stalls an E-house panel line fast. I have watched integrators blank openings with plywood while our TSC modules sat two weeks out. Timing fixes this.
Align multi cable transit delivery with E-house panel assembly by tying it to engineering gates, not calendar dates: order frames at interface design freeze so they land before wall cutouts, release sealing modules after the cable schedule freezes, and deliver modules before compression unit installation and factory acceptance testing.
That sounds simple. In practice it breaks down at four points. Samples arrive late. Lead times get planned as one number. Cutout dimensions get assumed instead of checked. Documents trail the shipment. I will take each one in order below, using what we see from our own production line and from the BESS, data center, and switchgear builders we supply.
How can I time my MCT validation samples so they don't delay my E-house panel assembly kickoff?
A sourcing manager in Germany once emailed us for validation samples four working days before his panel line kickoff. We shipped the same day. It still arrived late.
Request free validation samples at interface design freeze, at least one full module lead time plus a two-week qualification window before panel assembly kickoff. Test fit, compression, and cable diameter range against the current cable schedule, then release the production order before the panel line starts.
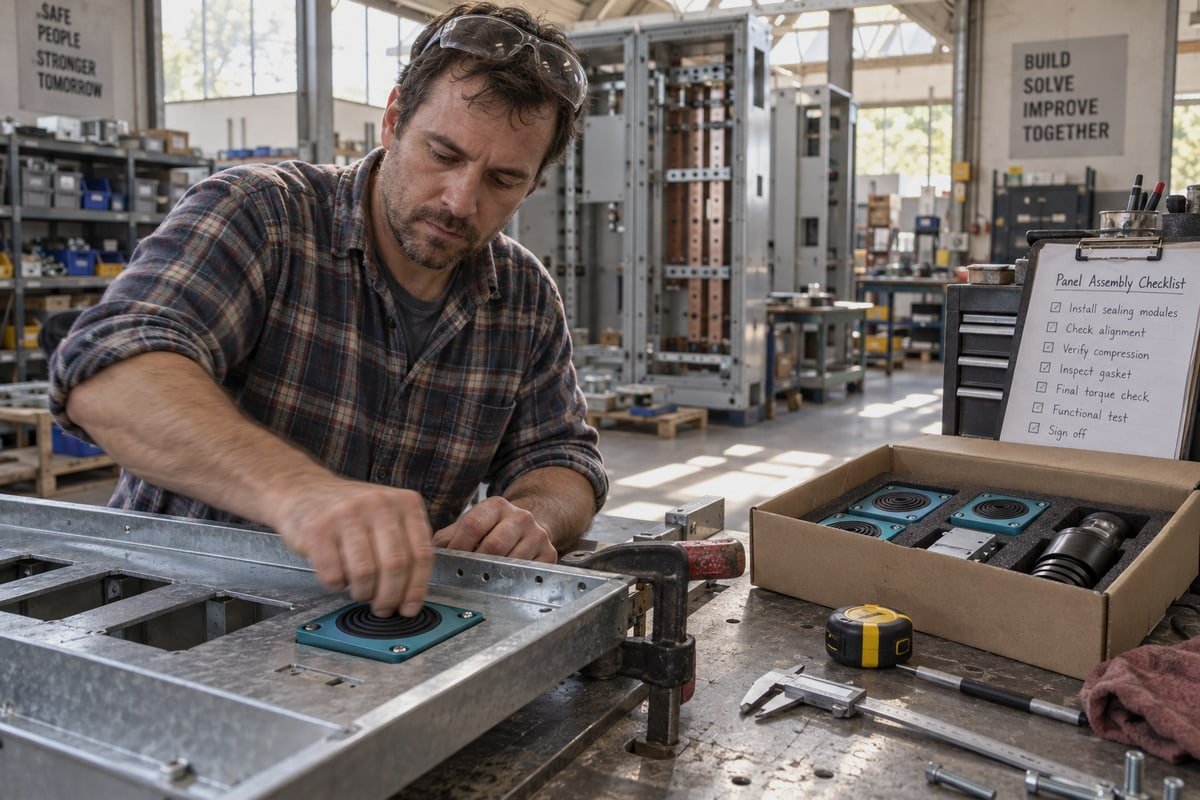
Validation samples are the cheapest schedule insurance in an E-house project. But they only work if they arrive before the decision they support. Our free sample kit is small: two or three TSC square modules in the sizes your cable schedule calls for, a TSR round assembly if you have pipe or single-cable penetrations, and a spare compression unit. The kit is not the hard part. The timing is.
Anchor samples to the interface design freeze
Most sample delays we see have one cause. The buyer requests samples when the panel line is already booked, not when the interface design is frozen. Then qualification, procurement approval, and production all land in the same two weeks. Something gives, and it is usually the line.
The fix is to put the sample request 2 on the same interface register as your cutouts and gland plates. When the cable management schedule reaches its issued-for-design revision, request samples the same week. The table below shows how we ask customers to sequence it.
| Engineering gate | Sample activity | Output you should hold |
|---|---|---|
| Cable schedule issued for design | Request free validation samples with cutout drawings | Sample kit dispatched |
| Interface design freeze | Fit test in existing 120-frame, compress with your own compression unit | Signed fit report |
| Procurement gate | Approve DEWIN model against the cross-reference table | Purchase order released |
| Panel assembly kickoff | Production modules already on the line | No blanked openings |
What a sample must prove in one week
Keep the test list short. Check the module drops into the cutout without force. Peel the step-core down to the smallest and the largest cable diameter on your schedule and confirm both seal. Compress with your existing unit and check the stay plate seats flat. Ask for the fire and IP68 documents in parallel so certification review does not wait for the fit test.
"Can we skip samples if the cross-reference table matches?"
I hear this often from switchgear panel integration teams under time pressure. My answer is no, but the table shortens the work. A cross-reference table narrows the model choice to one candidate. It does not replace the fit test. Weld distortion, paint thickness, and machining tolerance on an existing frame all affect fit. The sample confirms the real cutout, not the drawing. The table shortens qualification. The sample closes it.
What lead time should I plan for drop-in MCT modules to match my container build schedule?
Order early and eat rework, or order late and idle the line. That is the trade-off our planning team weighs with every BESS container builder we supply.
Plan two lead times, not one: order MCT frames at design freeze so they arrive before structural steel penetration cutting, and release sealing modules after cable schedule freeze so they arrive one to two weeks before compression unit installation. Hold a buffer of step-core modules for late diameter changes.
The early-versus-late debate never resolves because both sides argue about the wrong thing. They treat the multi cable transit as one line item. It is not. It is at least two.
Why one lead time is the wrong model
Early-procurement advocates have a point. E-house vendors such as ABB and Siemens sell these units on shorter lead times, and Siemens treats transport planning, load capacity, and mode selection as a defined delivery step. Nobody wants a cable sealing system to be the item that holds up a transport-ready unit.
Late-customization advocates also have a point. Roxtec's own selection guidance for buildings and E-houses says the transit choice depends on the cable and pipe schedule plus sealing and certification requirements. Order modules off a first-draft schedule and you buy the wrong sizes.
Both are right, about different parts. So split the order.
The two-trigger sequence we recommend
- At interface design freeze, order frames, stay plates, and compression units. Frames are steel. They do not care about cable diameter.
- Frames arrive before wall panel fabrication and are welded in during the structural steel penetration stage.
- At cable schedule freeze, generate the module BOM from the schedule and release the module order.
- Modules arrive kitted by zone and labelled per panel, one to two weeks before compression unit installation.
- Install, compress, and inspect every penetration before factory acceptance testing 3.
- Ship a small site kit for late field cables, so the E-house leaves the factory sealed.
| Component | Order trigger | Must arrive before | Cost of getting it wrong |
|---|---|---|---|
| Frames | Interface design freeze | Wall panel fabrication | Hot work on a finished wall |
| Compression units and stay plates | Same as frames | Module installation | Idle fitters, open apertures |
| Sealing modules (TSC, TSR) | Cable schedule freeze | Compression unit installation | Wrong diameters, rework, storage damage |
| Site kit | Cable schedule freeze | E-house dispatch | Field improvisation with cable gland alternatives |
Buffer stock, kitting, and the second-source advantage
Our step-core halogen-free EPDM modules 4 adapt to a range of diameters within one module size. That is what makes a buffer tray work. Hold the two or three most common sizes on the line and most late cable additions never touch the procurement lead times at all. Zone-based kitting matters just as much. Bulk cartons get opened once and lose parts. Kits labelled per panel get opened at the panel.
One more objection I hear: factory install or site install? Factory install wins on sealing integrity and on testing during FAT. Site install only wins where field devices are frozen late. The site kit above gives you both.
How do I confirm dimensional compatibility with my existing 120-frame cutouts before my panel line starts?
Our incoming QC bench in Shaanxi holds a reference 120-frame. Every TSC module batch gets dropped into it and compressed before it leaves the factory.
Confirm compatibility by checking the frame opening, module row height, module widths, compression unit stroke, and stay plate slots against a supplier cross-reference table and STEP files, then physically drop a validation sample into a spare cutout and compress it before the panel line starts.
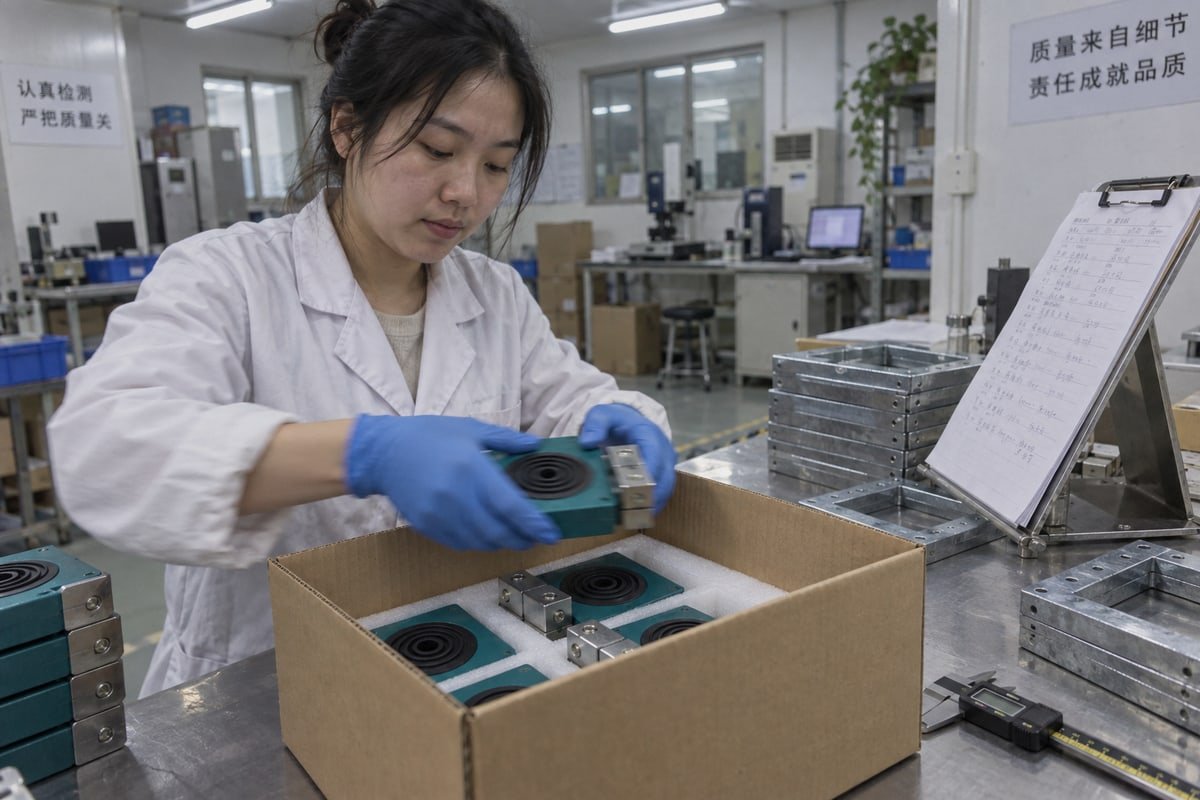
Dimensional compatibility is where second sourcing lives or dies. A module can meet every fire and IP rating and still be useless if it sits two millimetres proud of the stay plate. So we treat this as a checklist, not a conversation.
The five checks that catch almost every mismatch
The 120-frame family is defined by its module row height. Everything else follows from it. When a purchasing engineer sends us an existing frame drawing, our engineers run the same five checks we run on our own QC bench.
| Check | What you compare | Where the data comes from |
|---|---|---|
| Frame opening width and height | Clear aperture versus total module stack | Your cutout drawing, our STEP file |
| Module row height | Existing row pitch versus DEWIN module height | Cross-reference table |
| Module widths | Each module size in the stack versus the existing BOM | Cable schedule plus cross-reference table |
| Compression unit stroke and thread | Existing bolt pattern and travel versus DEWIN unit | Compression unit drawing |
| Stay plate slot | Slot depth and thickness versus plate | Frame section drawing |
Run these on the CAD model first. The ranking guidance on this topic is right that MCT geometry belongs in the 3D BIM or CAD model from the initial E-house design phase. Clashes with structural members and busbar routes are cheap to fix on screen and expensive to fix in steel. We supply CAD and STEP files for exactly this reason.
Standard modules or a project-specific mold?
Standardized transit designs cut engineering and procurement time. Most prefabricated electrical room 5 projects should stay standard. But a trend worth noting is the growth of pre-terminated cables with large connectors, which icotek and others now design around. A connector that must pass through the frame can exceed any standard module size. That is where our in-house mold making earns its place. We cut a custom module without moving you off the standard frame.
Plan spare capacity now, not later
Install frames with 20 to 30 percent spare module capacity. Blank modules fill the space today. Tomorrow a new fiber run or instrument cable drops in without hot work on a finished wall. If your panel layout or cable density changes mid-assembly, send us the revised schedule the same day. A shared model, even a simple one, lets us re-issue the module BOM before the kit ships.
What certification documents do I need in hand before my procurement team approves the delivery schedule?
Early on, we learned that a procurement approval without test reports attached is only a promise. Now our document pack ships before the sample kit does.
Before approving the delivery schedule, hold the supplier's ISO 9001 and IATF 16949 certificates, BV factory approval, A-0/A-60 fire test reports, IP68 ingress report, watertight and gas-tight pressure test data at 0.01–0.4 MPa, halogen-free material declaration, and the model cross-reference table.
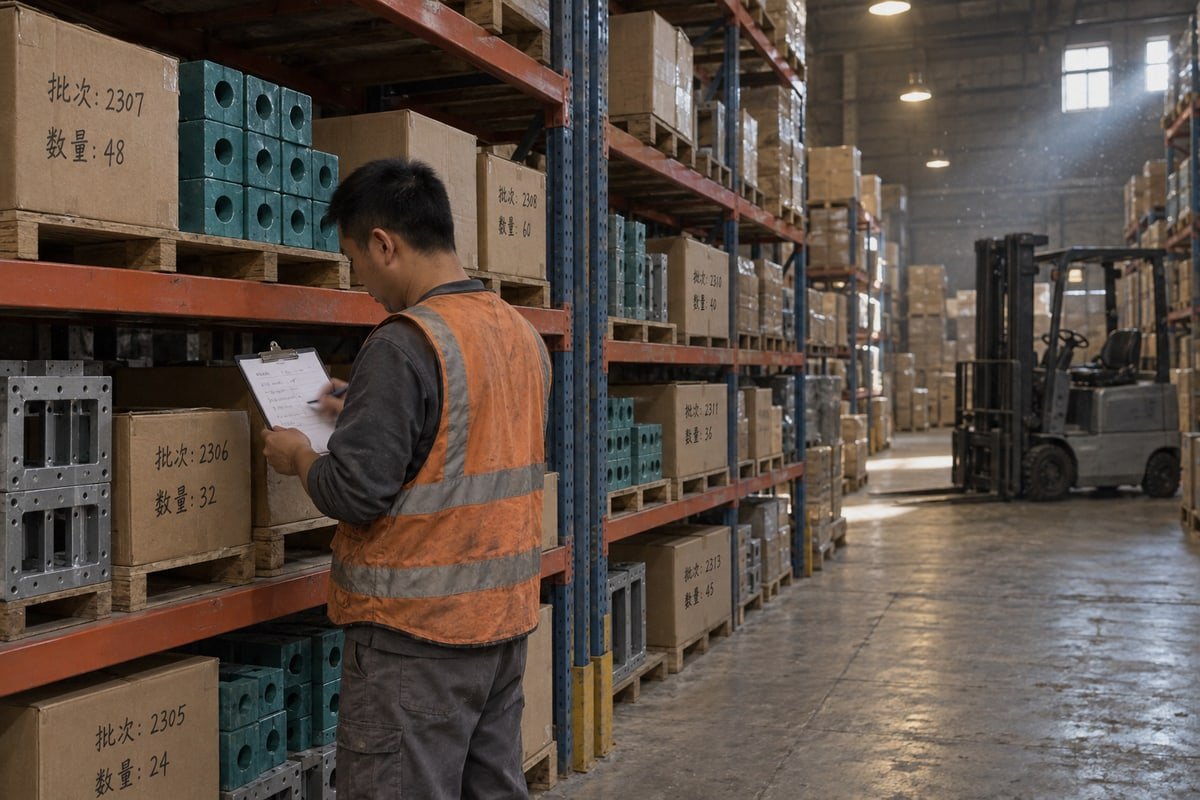
Skeptical buyers read spec sheets before they reply to emails. I respect that, and I design our document pack for that reader. The pack has one purpose. It lets a procurement team approve a delivery schedule without a second round of questions.
The document checklist
| Document | What it proves | When you need it |
|---|---|---|
| ISO 9001 and IATF 16949 certificates | Quality system covers design, production, and traceability | Before supplier qualification |
| BV factory approval | Third-party surveyed production, not a trading company | Before supplier qualification |
| A-0 / A-60 fire test reports | Fire-rated cable transits meet the E-house bulkhead rating | Before procurement approval |
| IP68 ingress protection report | Sealed penetration under immersion | Before procurement approval |
| Watertight and gas-tight test, 0.01–0.4 MPa | Pressure performance for modular substation construction | Before procurement approval |
| Halogen-free EPDM material declaration | No halogen release in a fire, relevant for enclosed rooms | Before procurement approval |
| Model cross-reference table and STEP files | Drop-in compatibility with the existing 120-frame | Before validation samples |
| Batch certificate of conformity and packing list | Delivered lot matches the tested design, export paperwork complete | With each delivery |
Why the documents belong on the schedule, not after it
Certification is a schedule item because factory acceptance testing depends on it. If your FAT procedure includes a pressure or water test on penetrations, the inspector wants the type-test report on the table before the test starts. The same logic applies later. A site integration test on a prefabricated electrical room often re-checks penetrations after transport. The report you hold at FAT is the report you show on site.
"Can the certificates follow the shipment?"
I hear this when buyers are trying to compress procurement lead times. The honest answer is that sending documents late saves nothing. Our documents are ready on request because the tests are already done. Ask for them at qualification. A supplier who cannot produce them at that point is not a second source. They are a risk you have not priced yet.
Fazit
Late or early MCT delivery both cost you panel line hours. Tie frames to design freeze, modules to cable schedule freeze, and documents to procurement approval. That is the method.
Fußnoten
1. ISO is the primary international body for industrial and manufacturing standards. ↩︎
2. Bureau Veritas is a leading authority for testing and certification of industrial components. ↩︎
3. ISA provides the professional standards and procedures for industrial factory acceptance testing. ↩︎
4. The IEC provides standards for halogen-free materials used in electrical cable management. ↩︎
5. IEEE is the leading technical authority for electrical engineering and modular substation design. ↩︎


 English
 Español de México
 Deutsch
 Français
 العربية
 Русский