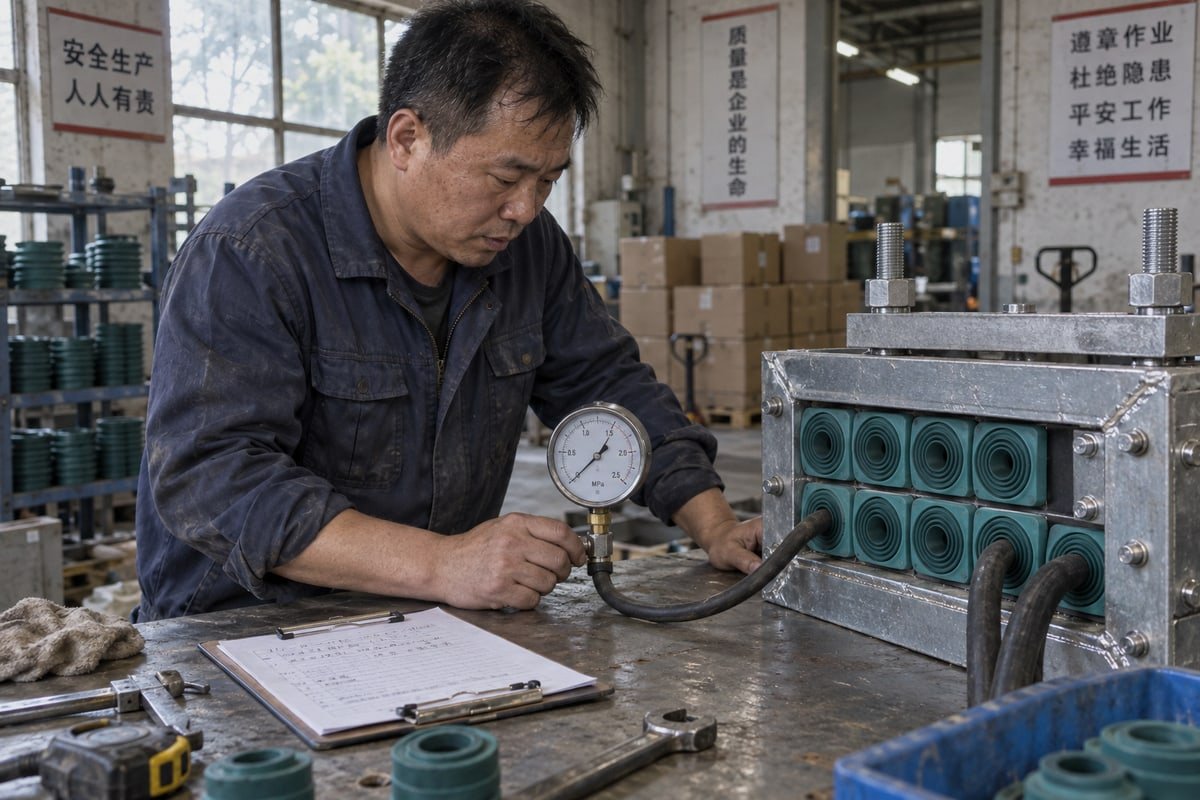
Vague specs reach our factory weekly: “IP68, fire rated.” Those three words hide every failure mode. Acceptance criteria for multi cable transit systems must be measurable instead.
Acceptance criteria for multi cable transit systems should specify the exact fire integrity rating and test standard, IP protection class, watertight and gastight pressure range, hazardous-area certification if needed, cable fill ratio and spare capacity, frame dimensions and tolerances, plus third-party test reports and material traceability certificates.
That list is the short version. Each item needs a number, a test method, and a document behind it. Below I break down how we help sourcing engineers write those criteria, what paperwork to demand, how to prove a drop-in fit into a 120-frame cutout, and which reports show the seal will still hold years from now.
How do I define measurable acceptance criteria that align with IP68 and fire rating standards?
Our QC bench runs a pressure hold on sample modules before they ship. Watching that gauge taught me what "IP68" actually needs to say in a purchase specification.
Measurable criteria state the IP protection class with its test depth and duration, the fire class (A-0 or A-60) with the named test standard and exposure time, the watertight and gastight pressure range such as 0.01–0.4 MPa, and pass/fail limits for each.
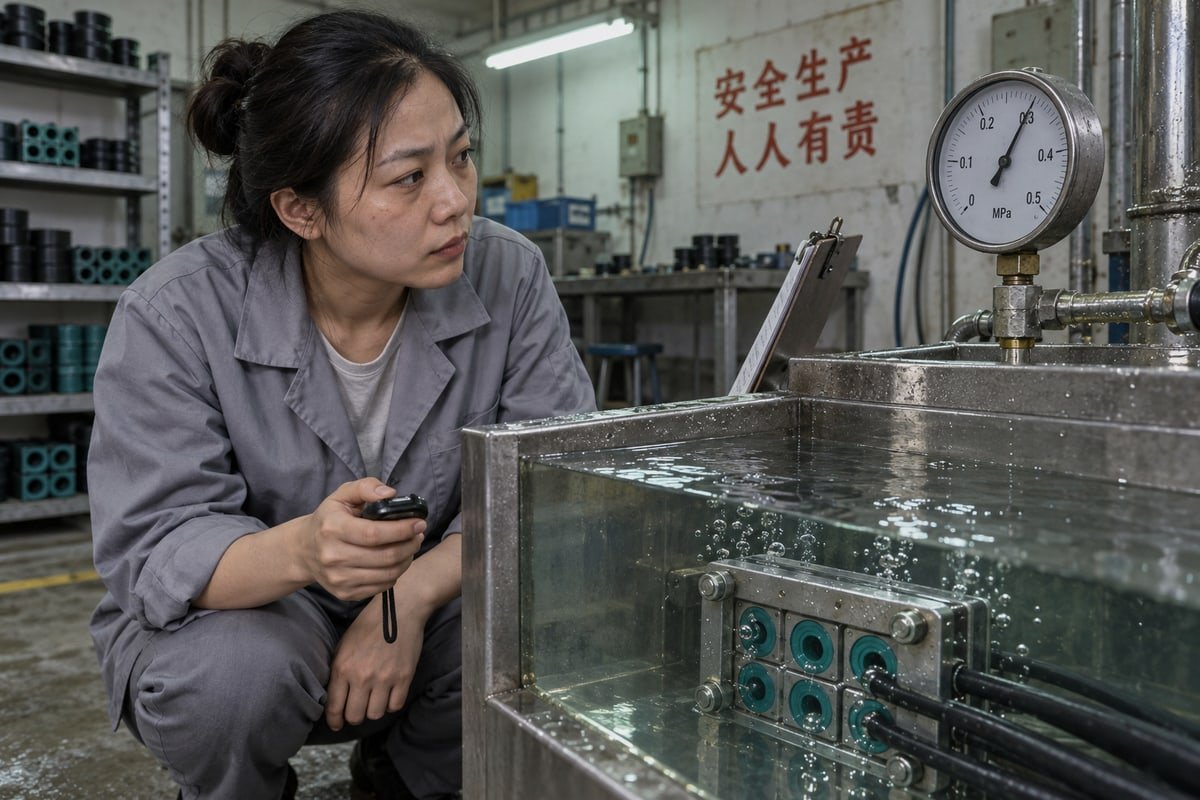
A rating is a label. A criterion is a label plus a test plus a limit. The gap between the two is where disputes start. When a buyer writes "IP68" alone, the supplier picks the depth and the time. When the buyer writes "IP68 per IEC 60529, immersion depth and duration as stated on the test report, no water ingress past the inner sealing lip," both sides know what passes.
Turning IP68 into numbers
IP protection class covers dust and water only. It says nothing about gas or about pressure from the other side of the bulkhead. So we tell buyers to write water and gas tightness as a separate line. Our TSR and TSC modules are tested for watertight and gastight sealing from 0.01 to 0.4 MPa, and we put that range in the submittal. Some supplier literature for offshore systems quotes watertight testing up to 4.5 bar or higher. Do not assume that figure. State the minimum pressure and hold time your project needs, and ask for the report that shows it.
Fire integrity versus insulation
Fire integrity ratings are also easy to state loosely. Marine and offshore rules under SOLAS and IMO fire-test procedures 1 use A-class divisions (A-0 to A-60) and H-class divisions (H-0 to H-120), and some offshore projects add jet-fire exposure. Building and industrial projects use different regimes. Your criterion should name the class, the standard, the exposure time, and whether the transit must hold integrity only or integrity plus insulation. Our modules carry A-0 and A-60 ratings, and we send the test document rather than a brochure claim.
| Attribute | Weak wording | Measurable wording |
|---|---|---|
| Ingress protection | "IP68 rated" | "IP68 per IEC 60529; depth and duration per attached report; zero ingress" |
| Fire | "Fire rated" | "A-60 per IMO FTP Code; 60 min; integrity and insulation" |
| Pressure | "Watertight" | "Watertight and gastight 0.01–0.4 MPa; hold time stated; no leakage" |
| Hazardous area | "Ex suitable" | "Certified per IEC 60079-0 / ATEX for stated zone; direct mounting allowed" |
Some buyers argue that basic ingress protection and a low unit price are enough for a control panel. I push back on that. A failed transit in a BESS container or switchgear room stops production, triggers a failed inspection, and costs far more than the module. The lowest-cost view only works if you never open the enclosure again.
What documentation should I require from suppliers before approving a sample batch?
A sourcing manager in Germany once asked us for our "certificate" before a sample order. I sent a folder, not one file, and asked which he actually needed.
Before approving a sample batch, require the type approval or factory approval certificate, ISO 9001 quality system certificate, fire and pressure test reports naming the standards, material traceability certificates for the EPDM and steel, dimensional drawings with tolerances, installation instructions, and a cross-reference table to your existing models.
That German buyer taught me that "certificate" means five different things to five different engineers. So now we sort our submittal into layers. Each layer answers one question. If a supplier cannot fill a layer, you have found your risk before the sample arrives.
The five layers of a submittal
- Who approved the factory or product? For marine and offshore work, procurement teams look for DNV GL type approval 2, ABS, or Lloyd's Register certificates. Our factory holds BV approval, and we run ISO 9001 and IATF 16949 3 quality systems. Ask for the certificate number and the scope, and check that the scope covers the module type you are buying.
- What was tested? Fire and pressure test reports must name the standard, the specimen configuration, and the result. A report for a different frame size or a different cable fill does not transfer automatically.
- What is it made of? Material traceability certificates for the EPDM compound and the steel frame link each batch to a compound lot and a heat number. Add halogen-free certification 4 if your project has low-smoke toxicity rules. ESG-driven buyers in Europe increasingly ask for Life Cycle Assessment data as well.
- Does it fit? Dimensional drawings with tolerances, CAD or STEP files, and for building projects, BIM objects. We supply STEP files with every sample request because a drawing without a native model slows down the buyer's integration review.
- Can it be installed and checked? Installation instructions, an inspection checklist, and torque or compression values for the compression unit.
| Document | What it proves | Red flag |
|---|---|---|
| Type or factory approval | Third-party oversight | Scope excludes your module size |
| Test reports | Rated performance | Only a summary sheet, no lab name |
| Material traceability certificates | Batch origin | Generic datasheet, no lot number |
| Cross-reference table | Drop-in equivalence | Model match with no dimension data |
| Installation and inspection sheet | Field verification | No compression or gap criteria |
Some project teams accept equivalent evidence rather than an exact one-to-one test match when the transit has broad certification and field history. I understand that view, and it does reduce procurement friction. But equivalence should be written down. Ask the supplier to state, in the submittal, which report covers your configuration and why. If the argument fits on one page with references, accept it. If it needs a phone call, it is not evidence yet.
How can I verify dimensional compatibility with my existing 120-frame cutouts before acceptance?
Tightening a frame tolerance sounds free. It is not. Every tenth of a millimetre we hold on our 120-frame profiles costs mold time, so we weigh it against fit risk.
Verify compatibility by requesting the supplier's cross-reference table and STEP or CAD files, checking frame outer dimensions, module heights, and stayplate positions against your cutout drawing, then fitting a free validation sample into a real frame and confirming compression wedge travel and cable fill ratio.
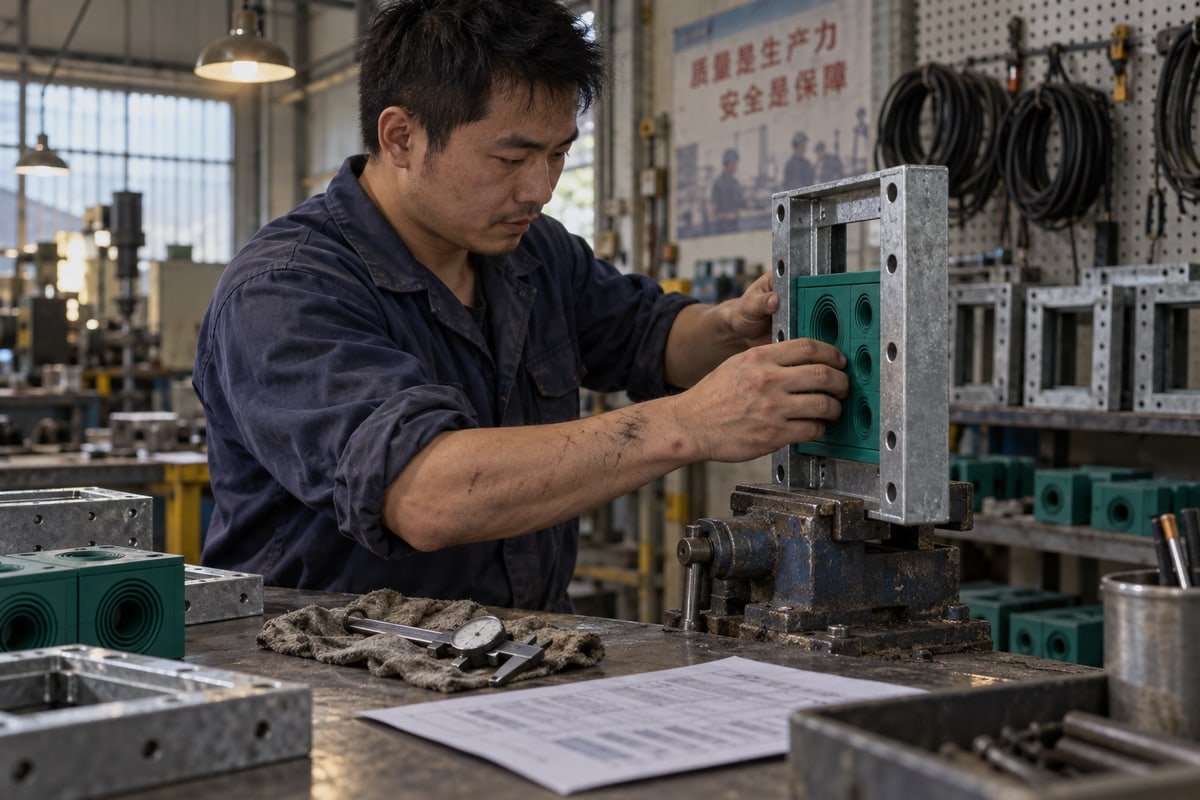
The 120-frame standard is common across the industry, and that is exactly what makes drop-in second sourcing possible. But "compatible with 120-frame" is a claim about the frame opening. It says nothing yet about module stack height, stayplate thickness, or how much travel the compression wedge has left when the last module goes in. Those three details decide whether a replacement seals or leaks.
A four-step verification process
- Paper check. Compare the supplier's cross-reference table (existing model → new model) against your bill of materials. We publish these tables so a buyer can map their installed modules to our TSC or TSR sizes without guesswork.
- Model check. Load the STEP file into your enclosure assembly. Check frame outer dimensions, weld flange width, bolt pattern, and the height of each module row.
- Physical check. Fit a free validation sample into a spare frame. Our step-core EPDM modules 5 adapt to a range of cable diameters within one module size, so verify that your smallest and largest cables both sit within the marked steps. Confirm stayplate positioning between rows and check that no visible gap remains between sealing modules after compression.
- Load check. Confirm the cable fill ratio and the frame loading limit from the supplier's data. Then apply your spare capacity requirements. Many EPC specs set a minimum percentage of empty frame area for future cables. Write that percentage into the acceptance sheet.
| Check point | How to measure | Accept if |
|---|---|---|
| Frame outer dimensions | Calipers vs. cutout drawing | Within stated tolerance both axes |
| Module stack height | Sum of rows plus stayplates | Leaves stated compression wedge travel |
| Stayplate positioning | Visual and gauge check per row | Plates seated, rows level |
| Cable fill ratio | Count cables and blank modules | Below supplier maximum, spare capacity met |
| Compression wedge installation | Compress to specified value | No visible gaps, wedge not bottomed out |
Conservative engineers tell me that a second source should never go in without a full retest for the exact application. I respect the intent. But a full retest for every panel variant is what locks integrators into a single supplier at premium prices. The workable middle path is this: use the same frame, verify dimensions on a sample, and demand the supplier's own fire and pressure reports for the matching module size. That is how our customers qualify us at 40–60% lower component cost without loosening their criteria.
What test reports and certifications should I request to confirm long-term sealing performance?
The lesson that changed our test plan: a module that passes a fresh pressure test can still fail after ageing. So we now ask what happens after re-entry and heat.
Request hydrostatic pressure testing reports at your stated bar and duration, fire integrity test reports with post-fire watertightness results, re-enterability test evidence, EPDM ageing data covering UV, ozone, and chemical exposure, halogen-free material certificates, and third-party type approval such as BV, DNV GL, or ABS.
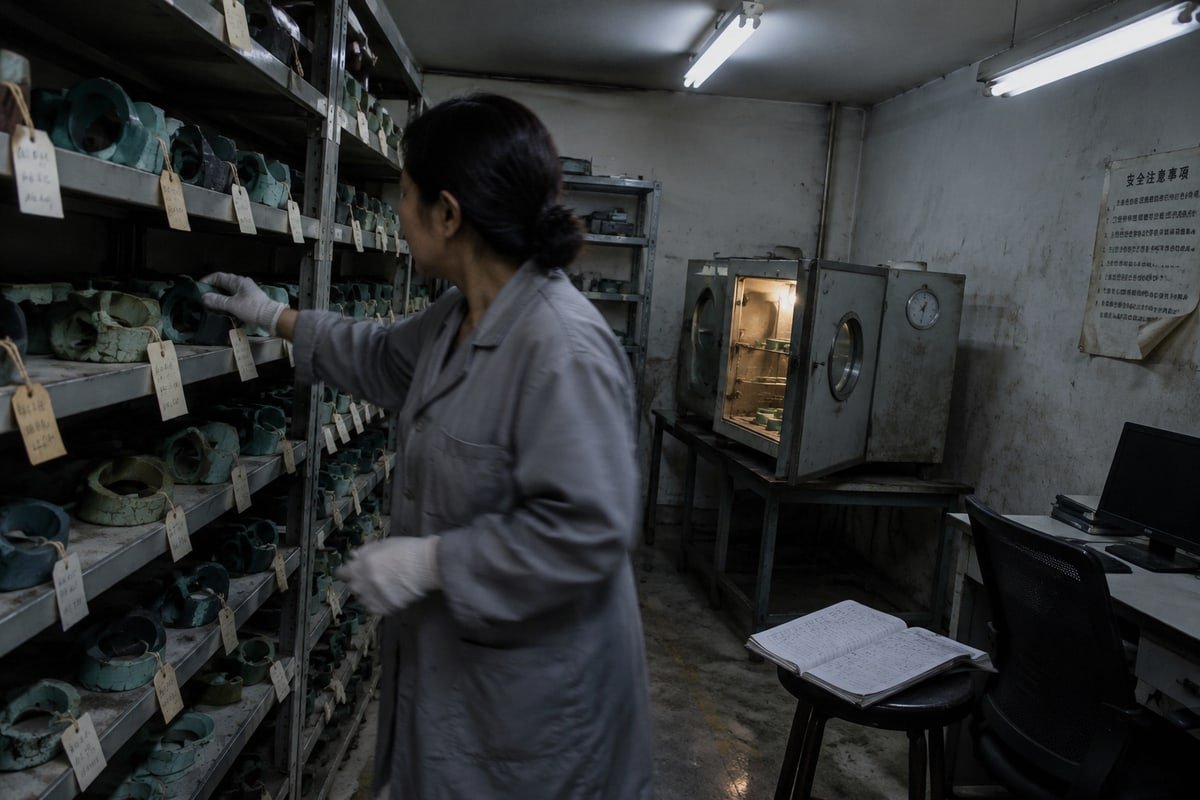
Long-term performance is where marketing and evidence drift apart the most. A brochure photo of a clean, dry frame tells you nothing about year eight. The reports below do. I group them by the question each one answers, because that is how our own engineers review them before a private-label run.
Does it hold pressure now and after stress?
Hydrostatic pressure testing at the project's stated pressure is the baseline. Our modules are documented from 0.01 to 0.4 MPa for water and gas. But the more useful reports show the seal after something bad has happened. Offshore and marine users ask for post-fire watertight integrity, meaning the transit is fire-tested and then pressure-tested. The current trend is combined performance, fire plus water plus gas, rather than three separate single-attribute sheets. Write that combination into your request if the application justifies it.
Does it survive the environment?
EPDM is chosen for cable transits because it resists ozone, UV, and heat ageing better than many other elastomers. Still, ask for the compound data. For BESS containers and outdoor switchgear, we get asked about temperature cycling and vibration. For offshore work, buyers add hydrocarbon exposure and corrosion resistance for the galvanized or stainless frame. Site-specific chemicals should be named in the request, not implied.
Does it survive people?
Cables get added. Modules get pulled. Re-enterability protocols prove that modules can be removed and reinstalled several times without losing the original fire or pressure result. This matters most for modular data centers, where pre-terminated cables change more often than the frame does. Ask how many re-entry cycles the supplier has tested.
Does it satisfy the authority?
For hazardous areas, request certification for the intended zone under ATEX or IEC 60079-0, or an accepted practice such as API RP 500/505 for North American schemes. State whether the transit mounts directly on equipment or inside an enclosure, because approval scope differs. For marine, DNV GL type approval, ABS, or Lloyd's Register is the usual gate. Our BV factory approval, ISO 9001, and IATF 16949 systems cover the industrial and energy projects we most often supply in Europe and the Middle East.
Some buyers still judge on purchase price and a basic IP rating. The better position is total installed cost: labor, rework risk, inspection burden, and the cost of the next cable change. A transit that costs less but cannot be re-entered is not the cheaper option over the asset's life.
Fazit
Vague specs invite vague products. Vague products fail inspections. Write measurable acceptance criteria, demand documents and samples, and accept only suppliers who prove performance for your exact conditions.
Fußnoten
1. Official site for the International Maritime Organization, which sets fire-test procedures for marine vessels. ↩︎
2. Leading classification society providing type approval for marine and offshore cable transit systems. ↩︎
3. Official site for the ISO 9001 quality management standard referenced for supplier evaluations. ↩︎
4. Official site for the IEC, which develops international standards for halogen-free material testing. ↩︎
5. Technical resource explaining the properties and industrial applications of EPDM rubber used in sealing modules. ↩︎


 English
 Español de México
 Deutsch
 Français
 العربية
 Русский