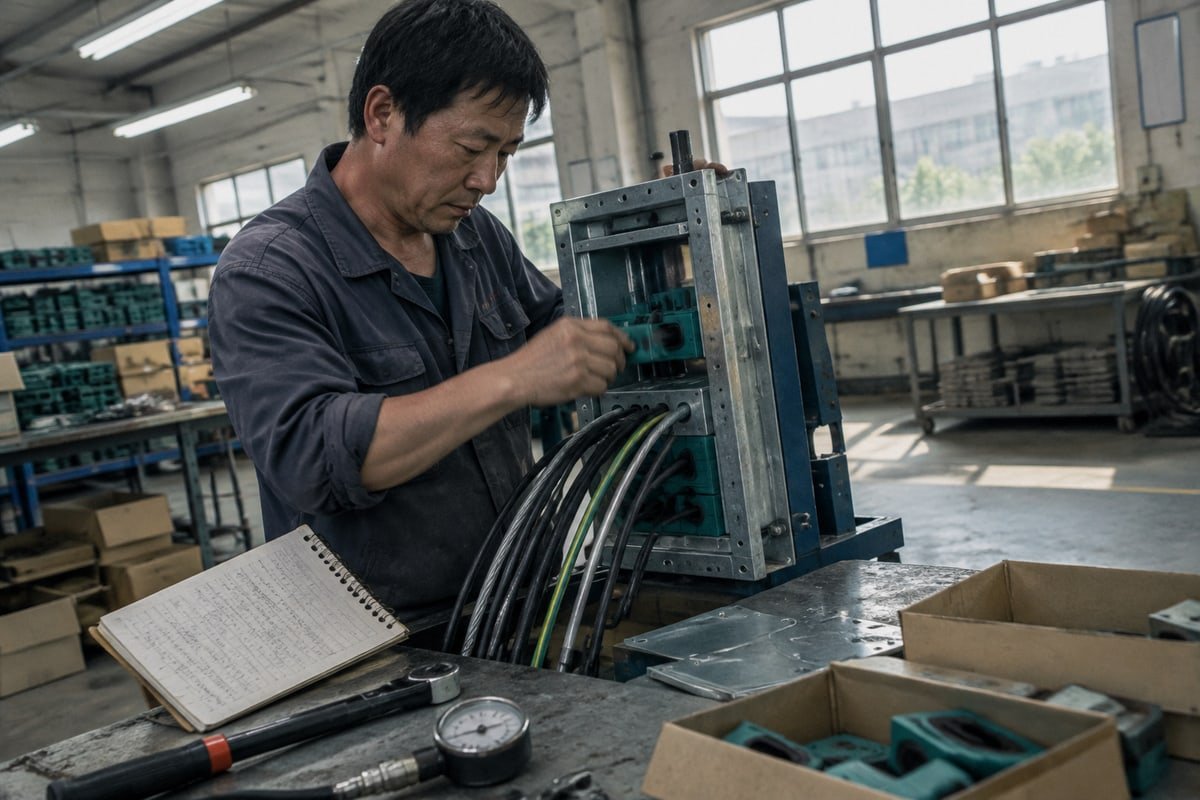
Fire inspection rectification requirements for multi cable transit sealing systems arrive with hard deadlines. Miss one and the site stalls. On our production line, we build the fix.
To address fire inspection rectification requirements for multi cable transit sealing systems, identify each defect, restore the transit to its tested configuration with certified A-0/A-60 modules, verify compression, IP68 and gas-tight performance, then document everything in a transit register for the follow-up inspection.
A multi cable transit is part of your passive fire protection. It is not a hole with rubber in it. The inspector treats it as a tested system. So the fix must be a tested system too. Below I walk through the four questions our customers ask most often when a notice lands.
What fire rating certification and test reports do I need to satisfy the inspector's rectification notice?
A sourcing manager in Europe once emailed us a rectification notice with one line highlighted: no valid fire test evidence provided. We sent our A-60 test file within the hour.
You need a fire resistance test report to a recognised standard such as EN 1366-3 with EN 13501-2 classification, or UL 1479 / ASTM E814, plus the product approval certificate, installation instructions, and a declaration that the installed configuration matches the tested assembly.
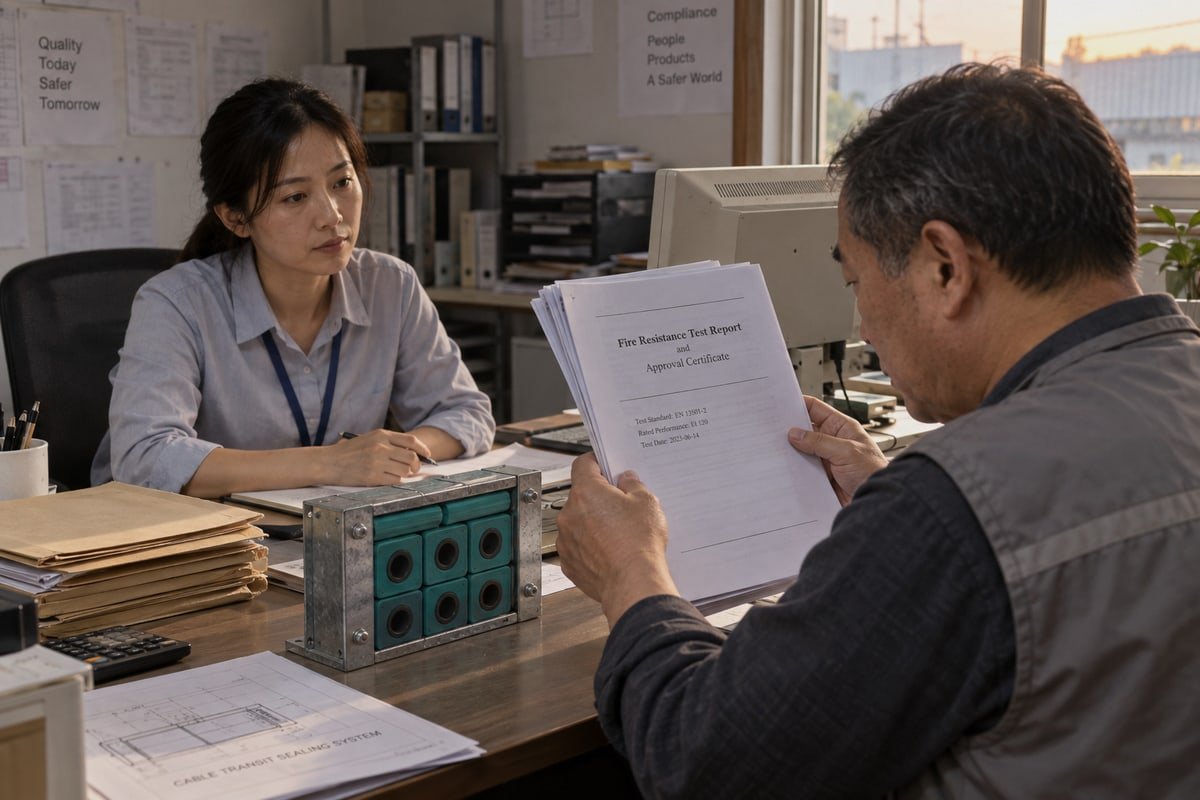
Inspectors do not want a brochure. They want proof that the product on the wall is the product that was burned in a furnace. That is the whole game. In our experience exporting to Europe and the Middle East, the documents below settle most rectification notices without a second visit.
The document set an inspector expects
| Document | What it proves | Who issues it |
|---|---|---|
| Fire resistance test report | Fire integrity and insulation for a timed period, often 60 minutes and up to four hours | Accredited test laboratory |
| Classification or approval certificate | The tested system is approved for the stated rating, such as A-0 or A-60 for marine bulkheads | Classification society or certification body |
| Installation instructions | Module sizes, cable fill ratio 1, compression method, spare capacity rules | Manufacturer |
| Declaration of conformity | The delivered modules match the tested batch and material | Manufacturer |
| Site installation record | Who installed it, when, and to which drawing | Contractor or owner |
Match the standard to the market
The inspector's regime decides which report counts. In Europe, EN 1366-3 is the test method for penetration seals 2, and EN 13501-2 gives the classification such as EI 60 or EI 120. In North America, the Authority Having Jurisdiction usually asks for UL listed firestop assemblies tested to UL 1479 3 or ASTM E814, tied to NFPA fire safety standards and the local building code. On ships and offshore units, a BV or similar class approval to A-0 or A-60 is the reference. Our factory holds BV approval, and our modules carry A-0/A-60 fire ratings. We keep the test documents ready to send on request, because a notice rarely gives you weeks to hunt for them.
The same as tested principle
Here is where many rectification jobs fail. A report is only valid for the configuration that was tested. If the site used a different filler, a different cable fill ratio, or a hand-cut block, the report no longer covers that transit. Firestop system compliance means the drawing, the modules, and the compression all match the approval. So before you send documents, compare the installed transit with the tested layout. If they differ, fix the transit first. Then the paperwork will hold.
Can I replace non-compliant MCT modules with a drop-in solution without redesigning my existing frame?
Every week our engineers weigh the same trade-off: keep a weld-in frame that passed inspection, or cut it out to fit a new brand's modules. Cutting is rarely necessary.
Yes. If your frame follows a common 120-frame standard, dimensionally compatible modules such as our TSC square and TSR round series drop into the existing cutout. You replace only the non-compliant modules, stay plates, and compression unit, keeping the frame, and verify against a cross-reference table.
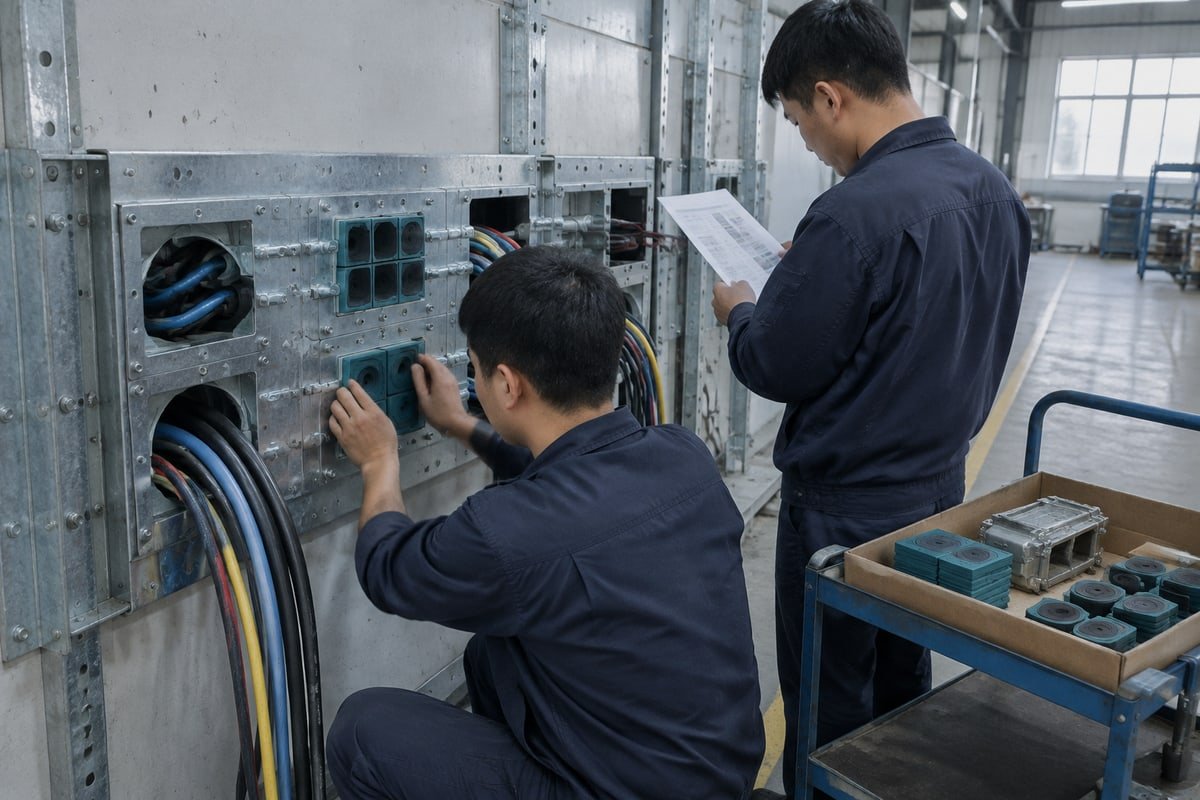
The frame is usually the healthiest part of a transit. It is steel, it is welded or bolted, and it rarely fails inspection on its own. What fails is the soft content. So the sensible path in remedial firestopping is to keep the frame and rebuild the fill. Here is how we guide customers through that.
Step-by-step drop-in rectification
- Photograph the existing transit and record the frame type, inner opening size, and number of rows.
- Remove the compression unit, stay plates, and every module. Do not reuse packing that shows heat damage, cracks, or permanent set.
- Clean the frame internal surfaces. Check for corrosion, weld cracks, and distortion. If the frame is sound, it stays.
- Map each cable outer diameter to a module size. Our step-core halogen-free EPDM modules cover a range of diameters within one size, which cuts the parts list.
- Fill unused space with solid blind blocks. Never leave voids or use unrated foam.
- Lubricate modules with approved lubricant, load rows with stay plates, and compress to the manufacturer's torque or visual indicator.
- Fit the identification plate and update the record.
What to keep and what to replace
| Component | Keep or replace | Reason |
|---|---|---|
| Steel frame | Keep if free of corrosion and distortion | It is the load-bearing part of the tested system |
| Sealing modules | Replace if field-modified, heat-exposed, or wrong size | Hand-drilled or shaved blocks void the approval |
| Blind blocks | Replace with rated solid blocks | Spare capacity must be sealed to rating |
| Stay plates | Replace if bent or corroded | They keep row alignment under compression |
| Compression unit | Replace if threads or wedge are worn | It sets the final seal force |
The objection: replace everything or repair locally?
Some manufacturer guidance says that after fire exposure or extreme heat, all packing must be replaced, even if one side looks fine. I agree with that rule for heat-exposed transits. Hidden damage in EPDM is real. But for a transit that failed on a wrong cable fill ratio or a missing blind block, condition-based repair is defensible. You restore the tested configuration with approved parts and correct compression. The inspector cares whether the result matches the approval, not how many parts you bought.
Cable density matters here too. If cables were bundled so tightly that modules could not touch each jacket around the full circumference, spreading them across more rows is part of the fix. Cable penetration seals only work when every module grips its cable.
We back this with a cross-reference table that maps the existing model to the DEWIN equivalent, and we send free validation samples so your team can test the fit in the actual frame before you commit. That is how a qualified second source should behave.
How do I verify that IP68 and gas-tight sealing performance will actually pass the follow-up inspection?
During a pressure test in our Shaanxi plant last year, a module set that looked perfect leaked well below its rated range. The cause was one under-torqued compression bolt.
Verify sealing by confirming compression to the manufacturer's torque or visual indicator, checking full circumferential module contact on every cable, then testing with a pressure decay or bubble test at the rated pressure, and screening with ultrasonic leak detection before you request the follow-up inspection.
Fire rating and tightness are a package. A transit can hold fire and still pass smoke or water. So the follow-up inspection may include a pressure check, especially on vessels, BESS containers, and switchgear rooms. Visual inspection alone is not verification. Let me break down what actually gets tested.
Compression is the root of every seal
The elastomer only seals when it is squeezed enough to deform around the cable and against the frame. Too little force and there is an air path. Too much and the cable jacket cold-flows over time. So compression wedge maintenance is not optional. Confirm the torque value or the visual indicator on the compression unit. On older installations, run a cold flow audit: look for jackets that have thinned under long-term pressure. Those transits need re-compression or new modules.
High-amperage cable runs add another factor. Thermal cycling expands and contracts the bundle. Some operators now use predictive thermal modeling to set a tighter re-torque schedule for those transits. That is good practice for data center and energy storage projects.
Verification methods compared
| Method | What it detects | When to use it |
|---|---|---|
| Visual and dimensional check | Wrong module sizes, gaps, missing blind blocks | Always, first pass |
| Torque or indicator check | Under- or over-compression | Always, before any pressure test |
| Bubble or soap test at low pressure | Local air paths | Quick site screening |
| Pressure decay test | Overall gas tightness at rated pressure | Where the regime requires proof |
| Ultrasonic acoustic sensor | Air-path leaks invisible to the eye | Large transit banks, fast screening |
| Water immersion or spray | Ingress protection to IP68 | Marine, outdoor, and container walls |
Know your target numbers
Industry material often cites 1.5 bar watertightness and 1 bar gastightness for penetration systems. Our TSC and TSR modules are tested watertight and gas-tight across 0.01 to 0.4 MPa and carry IP68 ingress protection. Ask your supplier for the test document that states the pressure, the duration, and the configuration. Then test the rectified transit at or near that condition. If your site cannot pressure-test, an ultrasonic scan plus a documented torque check is the next best evidence. Some newer modules also embed RFID or NFC tags so an inspector can read the material batch and fire rating from a phone without opening the seal.
How quickly can I source certified replacement modules to meet my rectification deadline?
The hardest lesson from our first decade of exporting: a rectification deadline does not wait for a mold. So we keep standard module sizes ready and cut samples fast.
Certified replacement modules can be sourced within days for standard sizes when the supplier holds stock of 120-frame compatible parts, offers free validation samples, and ships test documents with the order. Send the inspector's notice, your frame drawing, and cable diameters, then confirm the cross-reference before releasing the PO.
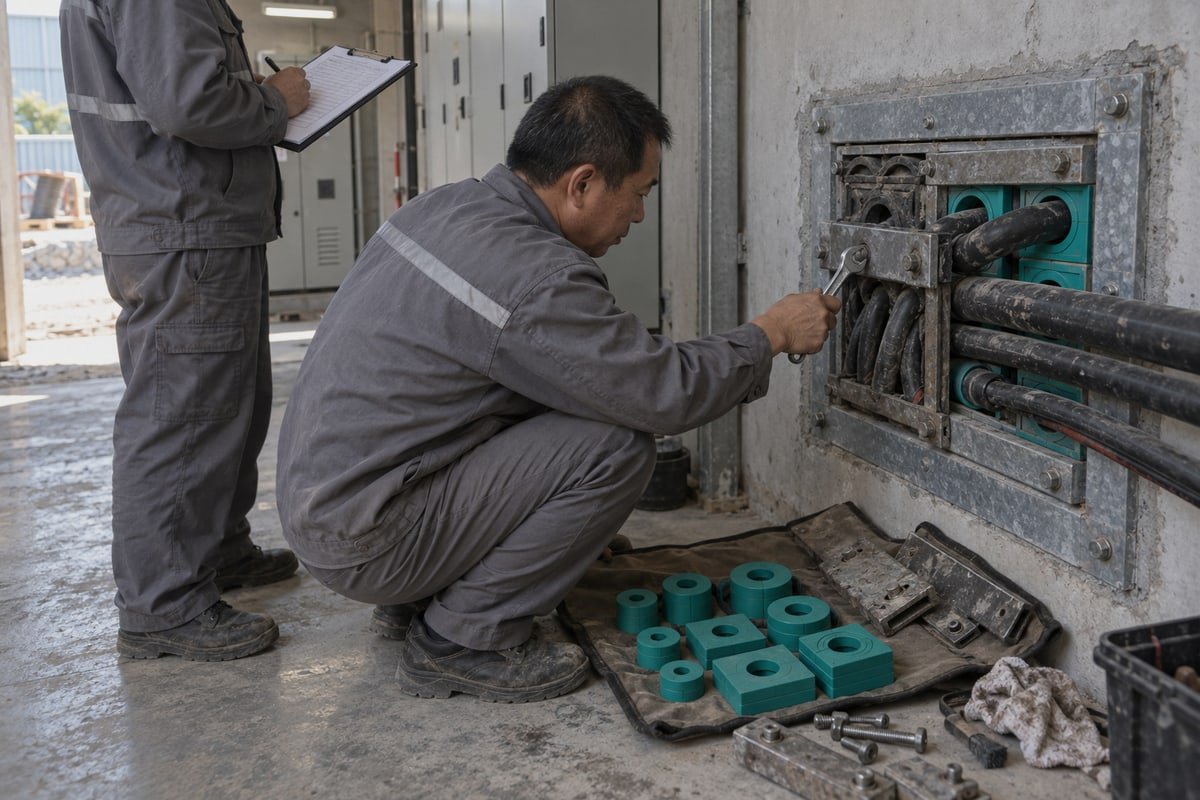
Speed comes from preparation on both sides. Your side needs clean data. Our side needs stock, molds, and paperwork ready to go. Since 2013 we have run production in Shaanxi, Shandong, and Hunan, which lets us move spare sealing modules out quickly and keep lead times stable. Here is the sequence that works.
A rectification sourcing timeline
- Day 0: Send the notice, frame photos, inner opening dimensions, and a cable schedule with outer diameters. A CAD or STEP file of the frame helps, and we return our module STEP files so your drawing office can check the fit.
- Day 1: We reply with the cross-reference from your existing model to the DEWIN model, the fill layout, and the test documents for A-0/A-60, IP68, and gas tightness.
- Day 2 to 3: Free validation samples ship so your team can dry-fit them in the live frame.
- On approval: Standard TSC and TSR modules, blind blocks, stay plates, and compression units ship with export documentation handled. Custom sizes go to our in-house mold shop, which is faster than outsourcing tooling.
- On site: Install, verify, and update the register.
The objection: cost-first versus compliance-first
Owners want the least disruptive and cheapest fix. Inspectors want a transit that matches the tested assembly. Those two goals are not in conflict if you choose a second source that is both certified and compatible. Our drop-in modules typically cost 40 to 60 percent less than the original brand, and they come with ISO 9001 4 and IATF 16949 quality systems behind them. The saving is real, but it is not the point. The point is that you meet the deadline with parts that hold the rating.
Close the loop with records
Fast sourcing means nothing if the follow-up inspector cannot trace the fix. On ships and offshore units, IACS and SOLAS 5 expect a Cable Transit Seal Systems Register. Each transit gets a location, product approval, drawing, inspection history, and every later repair. Onshore, a fire barrier management system does the same job and supports building code compliance. Add the new modules, batch numbers, torque values, and test results to that record on the day you finish. Then the rectification stands up in audits, insurance reviews, and re-inspection.
Conclusion
Rectification notices stall projects. Improvised patches fail re-inspection. Restore the tested configuration with certified drop-in modules, verify tightness, and record it. We supply the parts and proof.
Footnotes
1. Reference for cable fill ratio concepts in penetration systems. ↩︎
2. Reference for penetration seals and firestopping terminology. ↩︎
3. Official site for UL 1479 fire test standards. ↩︎
4. Official site for international quality management standards. ↩︎
5. Official site for international maritime safety conventions. ↩︎


 English
 Español de México
 Deutsch
 Français
 العربية
 Русский