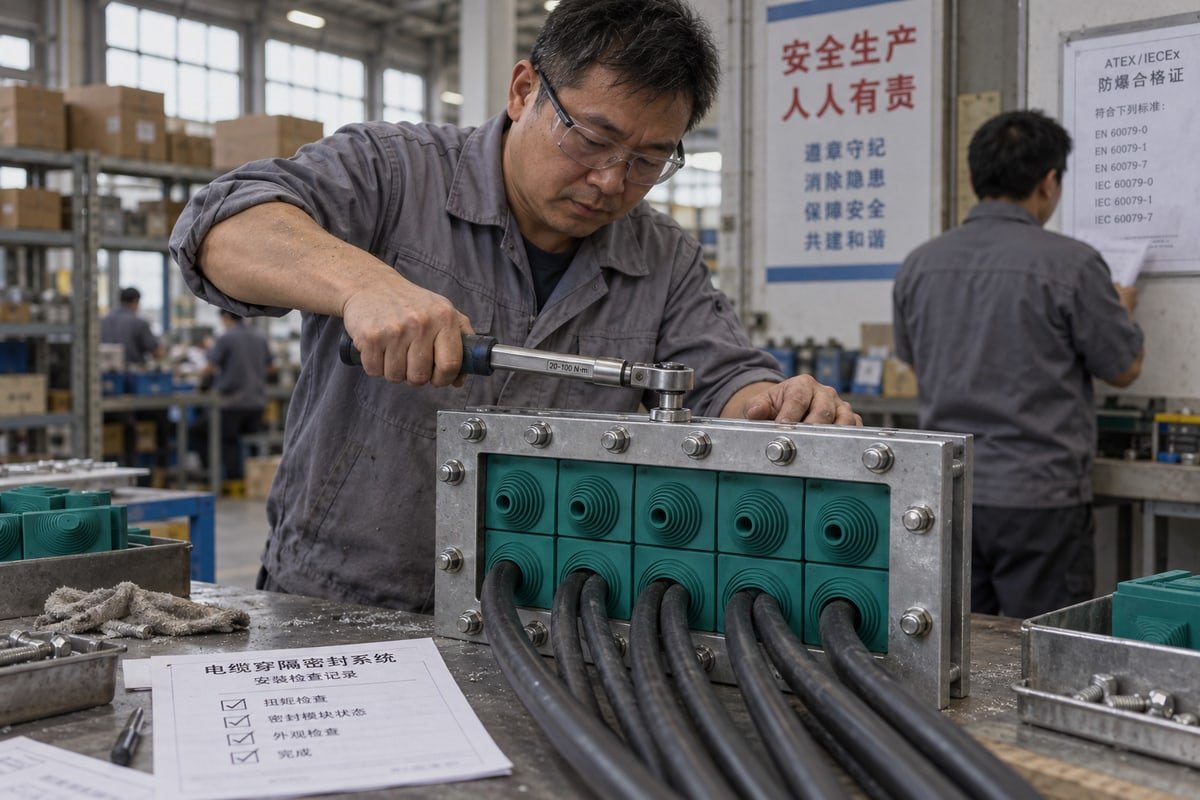
A buyer once sent our factory a spec that called zone-specific explosion-proof multi cable transits “just rugged glands.” That assumption fails Ex audits. So our engineers mapped every requirement below.
Zone-specific explosion-proof multi cable transits must be certified for the exact hazardous area (Zone 1/2 gas or 21/22 dust) under ATEX or IECEx, use halogen-free flame-retardant EPDM modules, hold gas-tight and IP66–IP68 sealing, retain cables mechanically, and be installed as part of a certified barrier system.
That is the short version. The longer version matters because each of those five points is a separate design decision. I will walk through them in the order a sourcing engineer actually meets them: zone rating first, then sealing specs, then documents, then whether the modules fit your existing frames.
How do I determine which explosion-proof zone rating my MCT system actually needs?
One lesson our export team learned early: the zone rating comes from the plant's hazardous area classification drawing, not from the cable count or the frame size.
Determine the zone rating from the site's hazardous area classification document: Zone 0/1/2 for gas and Zone 20/21/22 for dust. Most certified MCT products cover Zone 1 and 2 plus Zone 21 and 22; Zone 0 and 20 need separate equipment selection and engineering review.
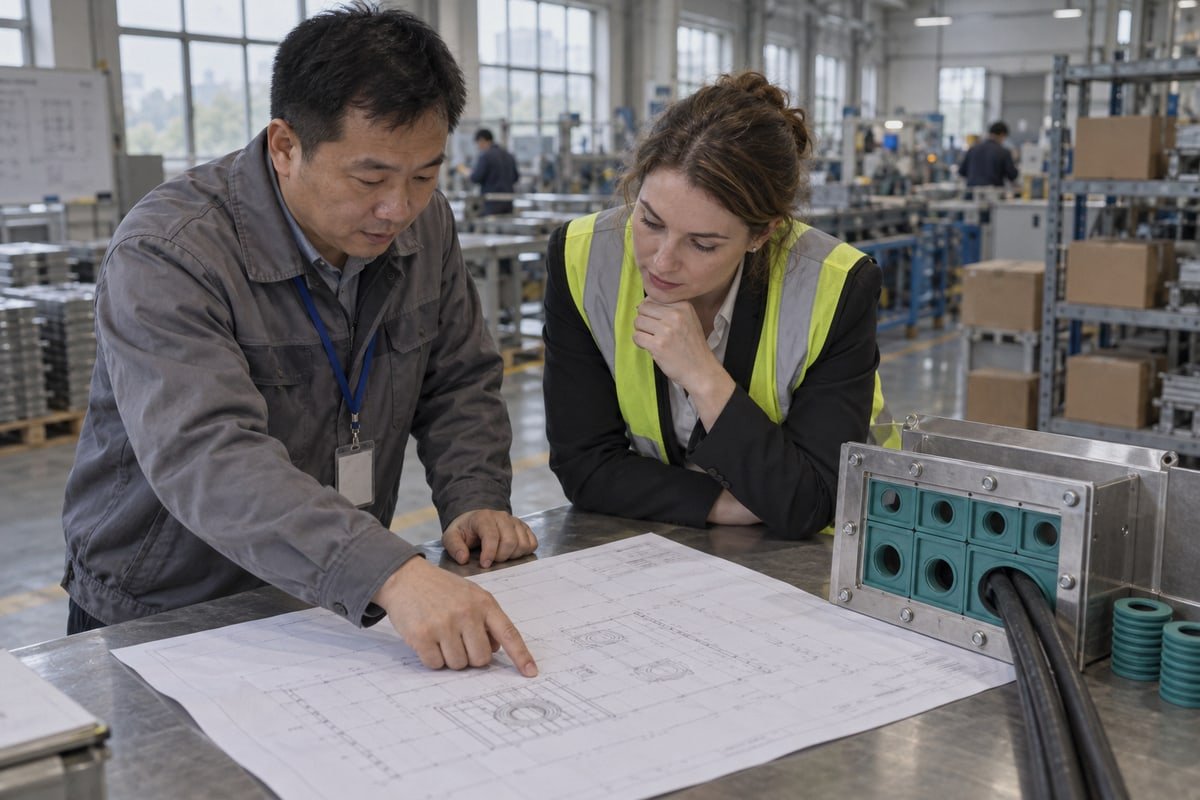
The zone tells you how often an explosive atmosphere 1 is expected at the penetration point. That frequency drives everything else. A transit that sits between a Zone 1 compressor bay and a safe control room does a different job than one inside a Zone 22 dust silo wall. Here is the map I use when a buyer sends me a drawing.
Zone classification at a glance
| Zone | Atmosphere | How often it is present | Typical certified MCT coverage |
|---|---|---|---|
| Zone 0 | Gas / vapor | Continuously or for long periods | Rarely; needs special selection |
| Zone 1 | Gas / vapor | Likely in normal operation | Commonly certified |
| Zone 2 | Gas / vapor | Unlikely, short duration only | Commonly certified |
| Zone 20 | Combustible dust | Continuously or for long periods | Rarely; needs special selection |
| Zone 21 | Combustible dust | Likely in normal operation | Commonly certified |
| Zone 22 | Combustible dust | Unlikely, short duration only | Commonly certified |
Most product families on the market, ours included, are built around Zone 1 and 2 compliance plus the dust equivalents. If your drawing shows Zone 0 or Zone 20 at the wall, stop and involve the Ex engineer. Do not assume a Zone 1 part scales up.
Read the barrier, not just the room
The second thing I check is what the transit separates. If it sits in a wall between a hazardous area and a safe area, the transit is the boundary. It must stop fugitive emissions from migrating across. If it mounts directly into a motor control center, junction box, or Ex enclosure, the entry device becomes part of that enclosure's hazardous-location design. In that case the certificate must cover the transit as an enclosure entry, not only as a wall penetration. This is where flameproof cable seals and standard industrial seals part ways.
Glands or a transit?
A common objection I hear from plant engineers: individual glands are simpler to inspect and replace. That is fair for three or four cables. For twenty or more cables through one bulkhead, each gland is a separate penetration and a separate leak path. A single transit frame turns those into one inspected, one documented barrier. It also gives a clean route for earthing armored or screened cables, which helps electromagnetic interference shielding 2 in control rooms. So the answer depends on cable density, not preference.
What sealing, IP, and pressure-tightness specs must zone-rated MCT modules meet?
On our pressure test bench, each batch of EPDM rubber modules is held at rated pressure before shipment. That routine shapes how I read sealing specs.
Zone-rated MCT modules must deliver gas-tight and watertight sealing, typically verified from 0.01 up to 0.4 MPa, achieve IP66/67 or IP68 ingress protection, use halogen-free flame-retardant elastomer, resist cable pull-out under vibration, and keep fire integrity (A-0/A-60) where the penetration crosses fire-rated bulkheads.
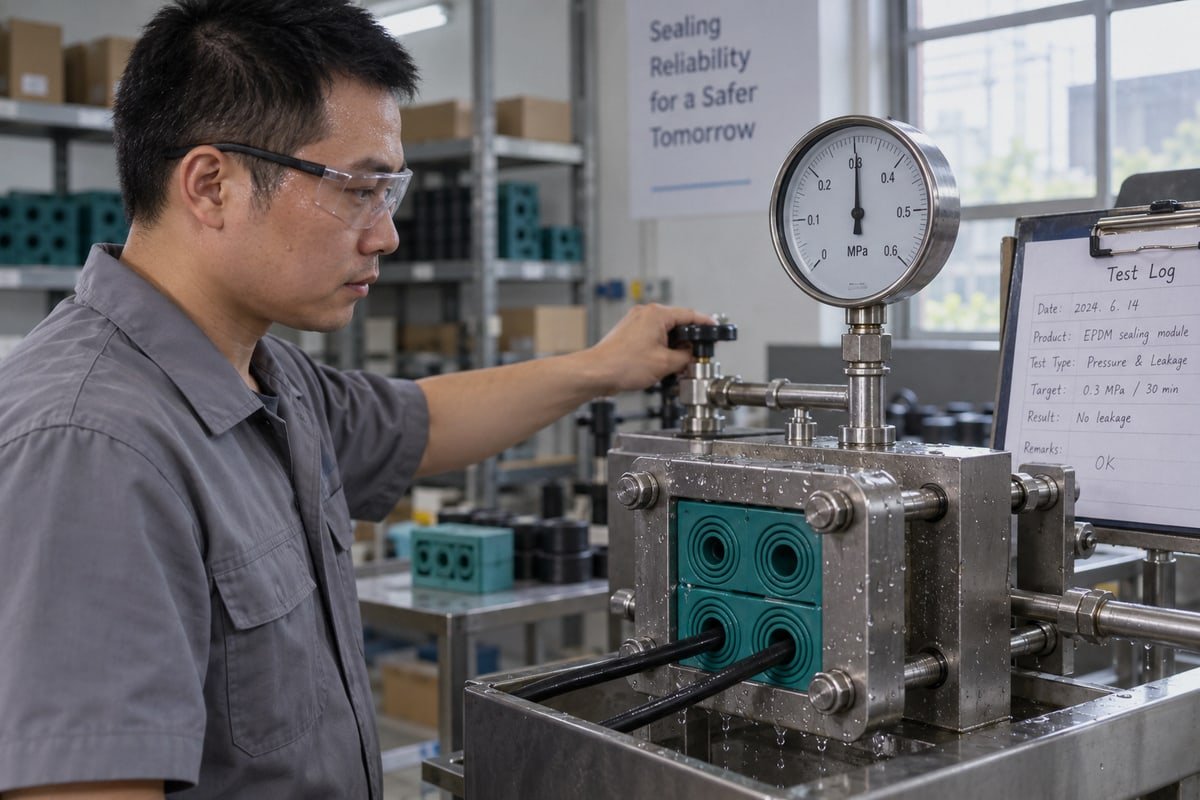
Explosion protection and sealing are two different jobs done by the same part. The certificate handles the first. The specs below handle the second. I have seen buyers request one and forget the other. Both belong in the purchase order.
The core sealing specs in one table
| Requirement | Target value or property | Why it matters in an Ex zone |
|---|---|---|
| Gas-tightness | Verified at 0.01–0.4 MPa | Prevents flammable gas or dust migrating across the barrier |
| Water-tightness | IP66/67 for washdown, IP68 for submersion | Environmental ingress can degrade the seal and the Ex barrier |
| Elastomer | Halogen-free, flame-retardant EPDM | Keeps sealing pressure and structure during a fire event |
| Fire rating | A-0 / A-60 where required | Needed when the penetration crosses fire-rated bulkheads |
| Frame material | Galvanized steel or 316L stainless | Corrosion resistance for offshore and chemical sites |
| Cable retention | High pull-out resistance | Cables must stay seated under vibration and pressure shock |
How the compression wedge system does the work
Gas-tight cable penetrations depend on compression, not adhesive. The modular sealing blocks stack inside the frame. Stay plates keep the rows aligned. A compression wedge system at the top pushes the stack together, and the EPDM squeezes around each cable. Two things follow from this. First, mechanical cable retention comes from the same compression, so an under-torqued wedge means both a leak and a loose cable. Second, the module must match the cable diameter. Our step-core modules adapt to a range of diameters within one module size, which removes the manual gap calculation that causes most field errors. I still ask installers to record the final compression, because vibration and thermal cycling test that setting over years, not days.
Blast loads and the "one system" question
Some offshore and petrochemical projects add a blast requirement, often stated as resistance above 10 psi for more than 60 milliseconds. This is a structural spec on the frame and the bulkhead, not only on the rubber. A recurring buyer objection is whether one transit can credibly handle fire, gas sealing, and blast at once. My answer is that it can, but only if each function has its own test report for the same assembly. If the blast report references a different frame than the fire report, you do not have one system. You have three claims.
Which certifications and test reports should I request to verify Ex-zone compliance?
A sourcing manager in the Netherlands once replied to our quote with one line: send the certificates first. I respect that. Documents are the product in Ex work.
Request the ATEX or IECEx certificate for the complete transit assembly, its Ex marking and zone scope, the ingress protection test report (IP66/67/68), gas-tightness and pressure test data, fire test reports for rated bulkheads, material declarations for halogen-free elastomer, and the installation instructions referenced by the certificate.
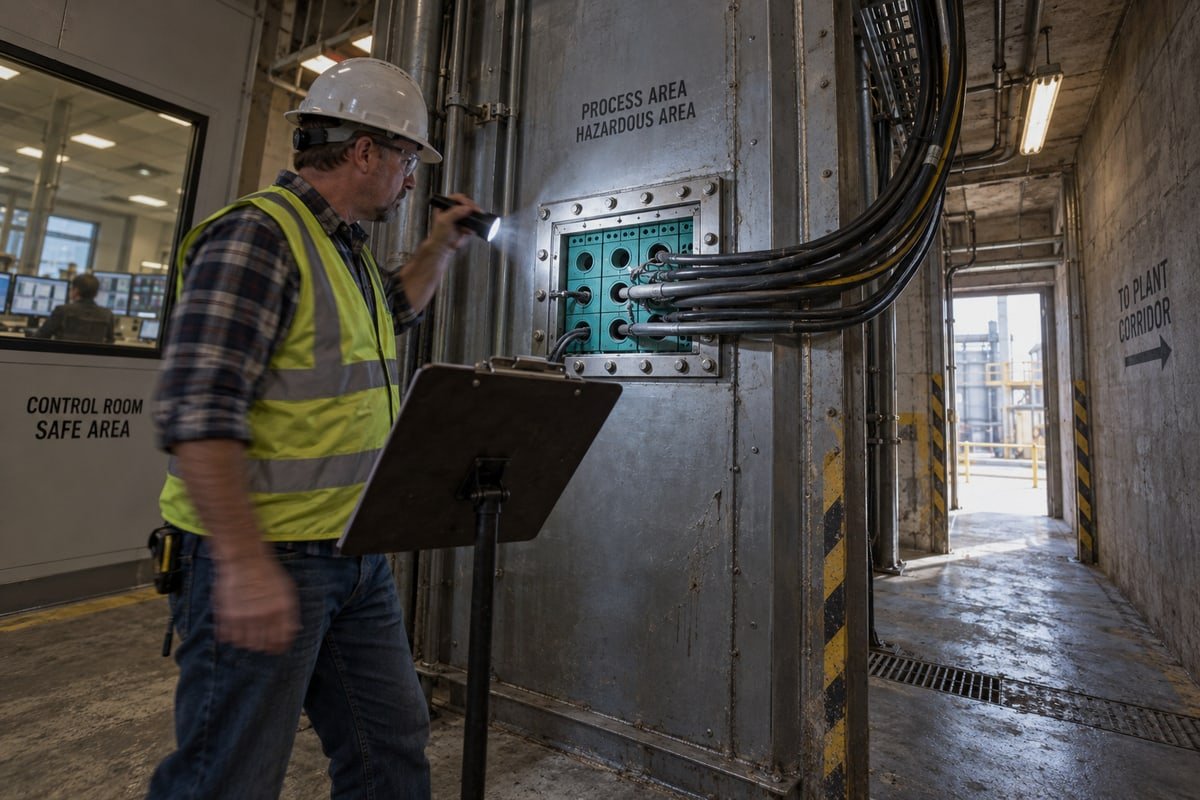
There is a real difference between "certified for hazardous location use" and "robust enough for industrial use." Marketing pages blur it. A document pack does not. Below is the checklist I send to buyers who are qualifying us as a second source, with the specific point to verify on each item.
The document checklist
| Document | What it proves | What to check before accepting it |
|---|---|---|
| ATEX and IECEx certification | Suitability for the stated zone | Certificate covers the full assembly: frame, modules, compression unit |
| Ex marking on the nameplate | Traceability to the certificate | Marking on the shipped part matches the certificate number |
| IP test report | IP66/67 ingress protection or IP68 | Test was run on the same module and frame combination |
| Gas-tight / pressure test | Vapor migration control | Pressure range stated, e.g. 0.01–0.4 MPa, with pass criteria |
| Fire test report | A-0 / A-60 bulkhead integrity | Wall or deck construction in the test matches yours |
| Material declaration | Halogen-free, flame-retardant EPDM | Batch traceability to the elastomer compound |
| Installation instructions | Certified installation method | Torque values, spare space rules, and cable mix limits |
| Quality system certificates | Process control | ISO 9001 4 and, for automotive-grade buyers, IATF 16949 |
What our own pack contains, and what it does not
I want to be precise here. Our factory holds ISO 9001 and IATF 16949 5 systems and is BV-approved. Our sealing modules carry A-0/A-60 fire ratings, IP68 ingress protection, and watertight and gas-tight test results in the 0.01–0.4 MPa range. All of those test documents are available on request. For an Ex-zone project, the extra step is to confirm that the Ex certificate scope matches the exact frame, module, and compression unit combination you will install. We go through that scope line by line with the buyer's Ex engineer before we release a validation sample. A certificate for a component is not a certificate for an assembly.
Digital verification is coming
The newest trend I see in tenders is a request for RFID or NFC tags on the frame. An inspector taps a phone and reads the certificate, torque record, and maintenance log on the spot. It does not replace the paper pack. It does make audits faster in a Zone 2 area where opening a binder is inconvenient. I expect this to become a standard line item within a few years.
Can zone-rated MCT modules still drop into my existing 120-frame cutouts without redesign?
The trade-off I weigh most often is simple: keep the customer's existing 120-frame cutout, or redesign for a new frame. Redesign costs weeks. Compatibility costs verification.
Yes, in most cases. Modules built to common 120-frame dimensions drop into existing cutouts as a second source, provided the frame, compression unit, and stay plates match and the certificate covers that assembly. Confirm fit with a cross-reference table and a validation sample before qualification.
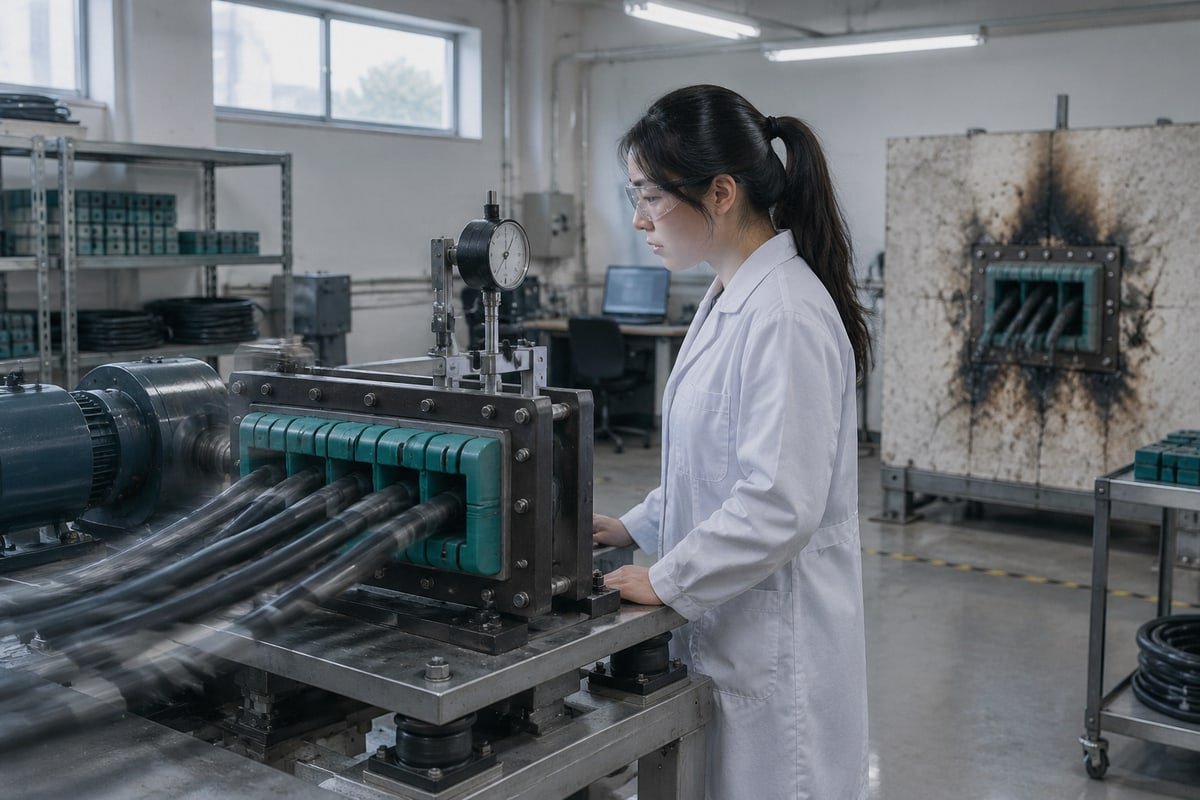
Dimensional compatibility is the reason second sourcing works at all in this product category. Our TSC square modules and TSR round assemblies are made to common 120-frame standards, so they seat in the same cutouts and stack in the same rows. But "it fits" and "it is qualified" are two different milestones. Here is the process I recommend, step by step.
A four-step qualification process
- Cross-reference the model numbers. Send us your existing module list. We return a table mapping each existing model to the DEWIN equivalent, with module height, cable diameter range, and frame size.
- Check the four match points. Frame internal dimensions, stay plate thickness, compression unit travel, and module height. If any one differs, the seal pressure changes and the certificate may not apply.
- Test a free validation sample. Fit it in a spare frame, torque the compression wedge system to spec, and run your own pressure or IP check. We supply CAD and STEP files so your drawing office can confirm the cutout before the sample arrives.
- Review the certificate scope. Confirm the Ex, fire, and IP reports cover the mixed assembly you will actually build.
What must match for a true drop-in
| Element | Must match | Why |
|---|---|---|
| Frame cutout | 120-frame standard dimensions | Otherwise a new hole in a fire-rated bulkhead |
| Module height | Same row height as existing blocks | Keeps the stack count and compression unchanged |
| Cable diameter range | Step-core range covers your cables | Peelable layers remove manual gap guessing |
| Spare capacity | Plan around 25 percent free space | Future cables without breaking the seal |
| Compression hardware | Same wedge travel and bolt spec | Seal pressure is the certified variable |
The cost objection, answered honestly
Buyers often say an MCT costs more up front than a handful of glands. That is true for small cable counts. For dense penetrations, our modules typically come in 40–60 percent below the incumbent brand while keeping the same fire, IP68, and gas-tight test data. The lifecycle value comes from fewer wall penetrations, faster installation, and spare modules that ship quickly because we mold them in-house. Some offshore projects are now also asking for non-conductive composite frames to cut weight and avoid galvanic corrosion in Zone 1 topside modules, and for BIM models to simulate blast response before installation. Both are custom work, but in-house mold making means we can quote them without a third-party tooling delay.
Conclusion
Zone-specific explosion-proof multi cable transits succeed only when zone rating, certification, sealing specs, and installation all match. Get the documents first, then the sample, then the order.
Footnotes
1. Official IEC page explaining standards for equipment used in explosive atmospheres. ↩︎
2. Official IEC page detailing electromagnetic compatibility and interference shielding standards. ↩︎
3. Official IEC resource explaining ingress protection (IP) ratings for electrical equipment. ↩︎
4. Official ISO page for the ISO 9001 quality management system standard. ↩︎
5. Official site for the IATF 16949 automotive quality management standard. ↩︎



 English
 Español de México
 Deutsch
 Français
 العربية
 Русский