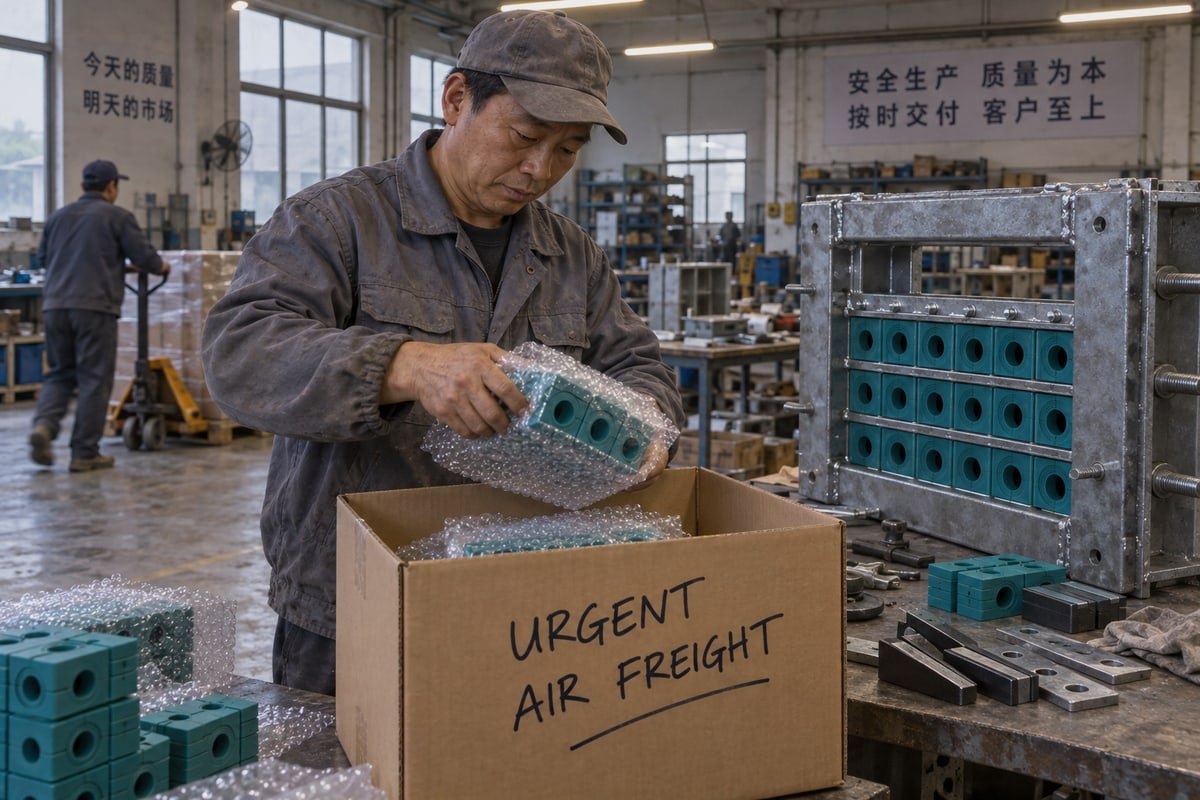
Our production line once air-freighted a single box of spare cable sealing modules to a BESS integrator whose replenishment cycles and safety stock for multi cable transits had quietly failed.
Set replenishment cycles and safety stock for multi cable transits together: choose a review cadence that fits supplier dispatch windows, then size safety stock as service factor times demand variability over lead time plus review period. Segment modules by criticality and qualify a drop-in second source.
That box cost more in freight than the modules inside it IATF 16949 1. The container line stood idle for two shifts before it arrived. All of it was avoidable. Below I walk through the four questions [purchasing engineers](https://dewinmct.com/?p=731) ask us most often, with formulas, tables, and one worked example you can copy into a spreadsheet.
How do I calculate the right safety stock level for MCT sealing modules and spare parts?
A purchasing engineer at a switchgear plant showed me his stock report during a validation-sample visit: shelves full of standard modules, zero compression wedges.
Calculate safety stock for MCT sealing modules as Z × σ × √LT: Z is the service factor for your service level target, σ is the standard deviation of period demand, and LT is lead time in periods. For periodic ordering, add the review interval to LT.
That stock report is the most common pattern I see in MRO inventory management for cable transits. The cheap, fast-moving item is overstocked. The item that actually stops the job is missing. The fix is not "more stock." The fix is a service level target 2 per item class, and a buffer sized from demand variability rather than from average usage.
Start with service level targets, not a stock number
ABC analysis works well here because MCT components have very different failure costs. A missing compression wedge blocks the whole frame from being sealed. A missing rare module size can usually be covered by a multi-diameter module from the next size up.
| Class | Typical MCT items | Service level target | Z factor |
|---|---|---|---|
| A – stops the job | Compression units, compression wedges, stay plates | 99% | 2.33 |
| B – common consumables | High-run TSC and TSR module sizes, blank modules, lubricant | 95–98% | 1.65–2.05 |
| C – slow movers | Rare module sizes, frame accessories | 90% | 1.28 |
A worked example you can copy
Say one TSC module size averages 40 pieces per week, with a standard deviation 3 of 15. Inventory lead time is 6 weeks. With a 98% target, Z is 2.05.
Continuous review: 2.05 × 15 × √6 = 2.05 × 15 × 2.45 ≈ 76 modules.
Periodic review with a monthly cycle adds about 4 weeks of exposure: 2.05 × 15 × √10 = 2.05 × 15 × 3.16 ≈ 98 modules.
The same item needs roughly 22 more modules on the shelf just because it is reviewed monthly instead of continuously. That is the cost of a long review cycle, and it is the number buyers most often forget.
Shrink σ before you buy buffer
Three levers reduce the variability term before you spend a cent on stock. First, cut SKU count. Our step-core EPDM modules cover a range of cable diameters within one module size, so demand that used to spread across several fixed-bore sizes pools into one. Pooled demand is smoother, and σ falls. Second, count physical reserve capacity. Blank modules already compressed inside installed frames are non-warehouse safety stock; a new cable can be routed without a procurement cycle. Third, adjust for environmental degradation factors. Modules in high-vibration or chemically aggressive zones get replaced more often, so their demand estimate should be raised before the formula is applied.
One more point. After commissioning, pivot from project-phase bulk stocking of frames and tools to lifecycle maintenance stocking of high-turnover sealing modules, wedges, and lubricant. The ABC classes change when the project ends.
What lead time data should I use when setting replenishment cycles for cable transit components?
One container from our Shandong plant cleared the factory in days and then waited on customs for longer than it took to mold the modules.
Use measured total inventory lead time, from purchase order release to goods receipt, not the supplier's quoted production time. Track the mean and standard deviation per supplier and route, include customs and inbound inspection, and refresh the data after every supplier or route change.
That customs delay taught me that a factory lead time quote is only one slice of the number a planner needs. When we send a lead time to a European buyer, we now break it into segments so their planner can put the right figure into the replenishment formula. If you only use the production quote, your buffer will be too small every time freight or customs slips.
Break inventory lead time into its parts
| Segment | What it covers | Who controls it | Variability driver |
|---|---|---|---|
| Order processing | PO release, confirmation, internal approval | Buyer | Procurement cycle time, approval queues |
| Production | Molding, compression unit assembly, QC | Supplier | Order size, custom mold work |
| Export documentation | Packing list, certificate of origin, booking | Supplier | Document errors, vessel cut-off |
| Freight | Sea or air transit | Forwarder | Route, season, port congestion |
| Customs and inland | Clearance, duties, delivery to site | Broker | Country, paperwork quality |
| Receipt and inspection | Unloading, dimensional check, put-away | Buyer | Receiving capacity |
Only the sum of all six rows is the lead time your formula needs. For remote or offshore assets, the freight and customs rows swing the most, so those sites justify a higher buffer than a plant near a main port.
Measure the spread, not just the mean
Record actual dates for every purchase order. Calculate the mean and standard deviation for each supplier and each route. A supplier with a 6-week mean and 1-week spread is a very different risk from one with a 6-week mean and 3-week spread. Both average the same. Only the second one causes stockouts.
Refresh the data set after any change: new forwarder, new supplier, new port, new incoterm. Old lead time data is the most common silent error in reorder point calculation.
Match the review cadence to the protection period
Here is where buyers push back. One camp says: run short weekly cycles, hold less buffer. The other says: order monthly in bigger lots, get cheaper freight and less admin. Both are right for different items. In one documented DDMRP case, a weekly replenishment cycle let replenishment signals fire within 1 to 5 days of a demand event. That responsiveness is worth it for A-class wedges and stay plates. For C-class rare module sizes, a monthly or quarterly review is fine, because the extra buffer is cheap.
So the answer is segmentation. Set the cycle per class. Then align the cycle with your Moves, Adds, and Changes schedule, so planned network expansions or container builds are fed through material requirements planning as dated demand, not absorbed by the buffer.
How does dual sourcing with a drop-in second supplier reduce my required safety stock?
Every time we quote a drop-in TSC module against an incumbent brand, I weigh a trade-off the buyer rarely sees: qualification effort now versus buffer stock carried forever.
A drop-in second supplier cuts safety stock by shortening effective lead time and reducing lead-time variability, because either source can fill the same 120-frame cutout. With two sources, a stockout needs both to fail, so you size buffer on the shorter lead time, not the worst case.
The trade-off is real, but it is lopsided. Qualification is a one-time cost. Safety stock is carrying cost every month, on every SKU, at every site. Once a second source is dimensionally qualified, the inputs to the safety stock formula change in your favor. This is the core of buffer stock optimization for cable transits.
What a second source actually changes in the formula
| Input | Single source | Dual drop-in source | Effect on buffer |
|---|---|---|---|
| Effective lead time | Incumbent quote plus freight | Shorter of the two, order by order | Lowers the √LT term |
| Lead-time standard deviation | One supplier's spread | Second source covers the incumbent's slips | Lowers σLT |
| Supply failure risk | One factory, one route | Two factories, two routes | Independent failures multiply, not add |
| MOQ and pack size | Locked to one supplier | Choose the smaller minimum | Reduces overstock on C items |
Because our TSC and TSR modules are dimensionally compatible with common 120-frame standards, the second source needs no frame change and no rework of the as-built documentation. The module simply drops into the existing cutout.
Qualification steps that keep the buffer honest
- Start with the cross-reference table. Map each existing model number to the DEWIN equivalent so the item master has two approved lines per part.
- Request free validation samples and fit-test them in a real frame at your plant, with the real compression unit torque.
- Ask for the test documents, not the brochure: A-0/A-60 fire rating, IP68 ingress protection 4, and watertight and gas-tight sealing across 0.01–0.4 MPa, plus the ISO 9001 5 and IATF 16949 certificates and BV factory approval.
- Load the CAD/STEP files into your engineering library so the drawing set does not depend on one brand.
- Run a small pilot order and log the measured lead time from PO to receipt. That measured number is what goes into the formula, not our quote.
Pool across facilities and answer the admin objection
Buyers tell me a second supplier doubles their admin. In practice it adds one line to the item master and one approved-vendor record. What it removes is the expedite fee, the air freight, and the idle line. A second benefit is cross-asset inventory pooling: if you standardize module ranges across several plants or container lines, one shared buffer can serve all of them, and the aggregated demand is less variable than each site alone. The 40–60% lower unit cost of a factory-direct second source usually funds the qualification project several times over in the first year.
What reorder point formula works best for spare sealing modules with variable project demand?
The lesson I learned from years of shipping spare sealing modules to EPC contractors: a reorder point built on average demand fails exactly when a project phase starts.
For spare sealing modules with variable project demand, use ROP = (average daily demand × lead time in days) + Z × √(LT × σd² + d² × σLT²). It covers demand and lead-time variability. Layer known project pulls on top as planned orders, not extra buffer.
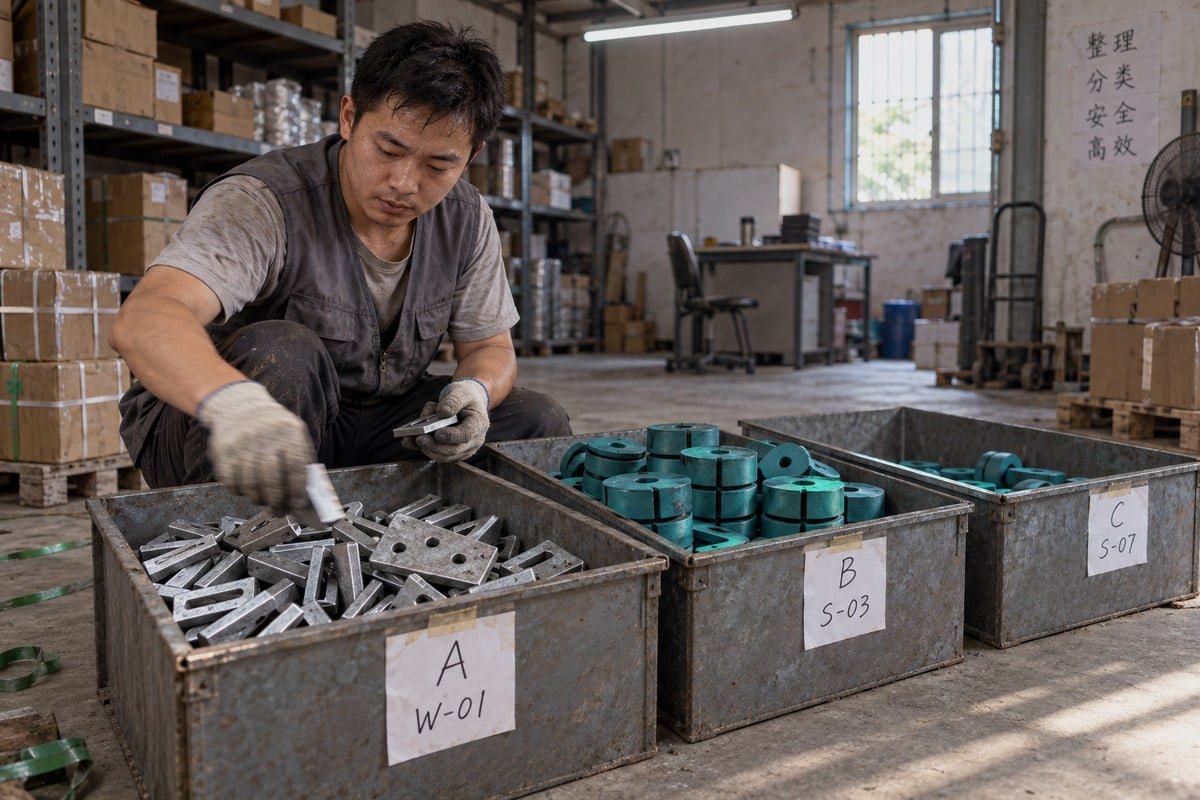
The problem with project demand is that it is not random. It is lumpy and it is scheduled. If you feed a 600-module container order into the statistical formula as if it were noise, σ explodes and you carry a huge buffer for the eleven months when nothing happens. Then the project starts and the buffer still is not enough.
Separate base demand from project pulls
Split the demand stream in two. Base demand is maintenance, repairs, and small adds. It is genuinely variable, and it belongs in the reorder point calculation. Project demand is known from the bill of materials and the build schedule. It belongs in material requirements planning as dated planned orders. The ROP protects the base stream. MRP feeds the project stream. When both run together, the buffer stays small and the project still gets its modules.
A worked example with lead-time variability
All figures below are illustrative. Base demand for one module size is 8 pieces per day, σd = 4. Measured inventory lead time is 42 days, σLT = 7 days. Service level target is 98%, so Z = 2.05.
| Step | Calculation | Result |
|---|---|---|
| Demand during lead time | 8 × 42 | 336 |
| Demand-variance term | 42 × 4² = 42 × 16 | 672 |
| Lead-time-variance term | 8² × 7² = 64 × 49 | 3,136 |
| Combined standard deviation | √(672 + 3,136) = √3,808 | ≈ 61.7 |
| Safety stock | 2.05 × 61.7 | ≈ 127 |
| Reorder point | 336 + 127 | 463 |
Compare that with the simple version, Z × σd × √LT = 2.05 × 4 × 6.48 ≈ 53. Ignoring lead-time variability would cut the buffer by more than half, and it would cut it on the exact input that a long international route makes uncertain. This is why a stockout risk assessment for cable transits should always look at σLT, not only σd.
Trigger the ROP from field data, then tune it
For continuous review, the ROP fires whenever stock position drops below 463. A digital transit management system that holds the as-built status of every frame can trigger this from actual consumption in the field, so the signal does not wait for a warehouse count. For periodic review, convert the ROP into an order-up-to level by adding demand over the review interval.
Some buyers ask whether optimization software beats these rules. It can, but only with clean lead time data and disciplined parameter maintenance. Start rule-based. Review stockouts and expedite orders every quarter. Recalculate σd and σLT from the last twelve months. Then decide if the extra tooling is worth it.
Conclusion
Unplanned stockouts of cable sealing modules stop lines and burn freight budgets. Set the cycle first, size the buffer from real data, and qualify a drop-in second source.
Footnotes
1. Automotive quality management standard used to ensure high-reliability manufacturing processes for sealing components. ↩︎
2. Defines the performance goal for inventory management to balance stock availability against carrying costs. ↩︎
3. Statistical measure used to quantify demand and lead-time variability in safety stock calculations. ↩︎
4. International standard for defining levels of sealing effectiveness against moisture and foreign bodies. ↩︎
5. Official international standard for quality management systems required for qualifying industrial cable transit suppliers. ↩︎


 English
 Español de México
 Deutsch
 Français
 العربية
 Русский