Multi cable transit trial orders often pass on paper and fail on site IATF 16949 1. Since 2013, our factory has watched that gap wreck rollouts; a stricter acceptance standard prevents it.
Multi cable transit trial orders should meet four standards before scaling: verified fire certification (A-0/A-60 or ASTM E814/UL 1479, EN 1366-3), documented IP68 and pressure test results, confirmed dimensional fit with existing 120-frame cutouts, and a trial batch large enough to prove repeatable installation and re-entry performance.
Each of those four standards is a separate gate. I will take them one at a time. First the certificates, then the dimensions, then the test documents, and finally the batch size.
Which certifications should I verify before approving a trial order for multi cable transit systems?
A sourcing engineer in Germany once asked us for our BV factory approval certificate 2 before he even opened the price sheet. That order of priorities was correct.
Before approving a trial order for multi cable transit systems, verify fire test certification to ASTM E814/UL 1479 or EN 1366-3, marine type approval under the IMO FTP Code where relevant, an ISO 9001 quality system, and a factory approval from a recognized classification society.
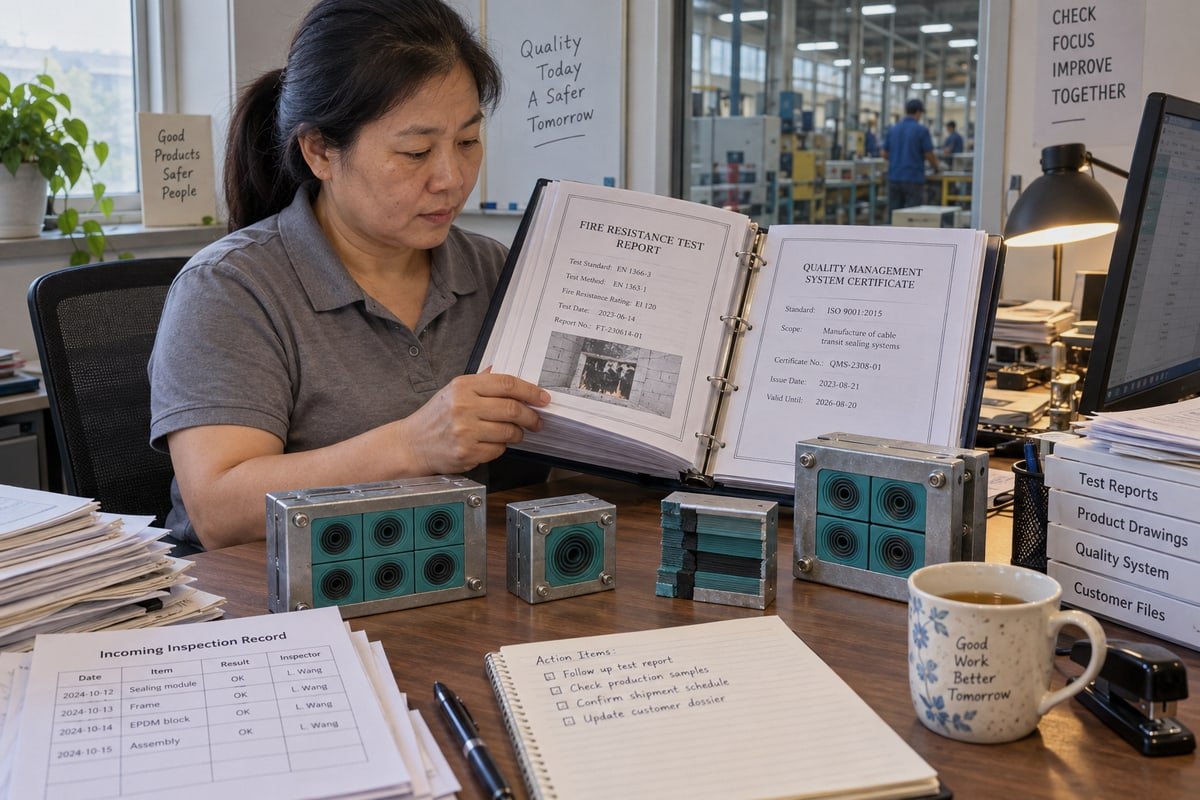
Certification is the first gate for a reason. If the paperwork is wrong, nothing you measure on site will fix it. But a certificate is only useful when it matches your application. I split the check into three layers.
Layer one: fire performance that matches your assembly
A common buyer objection goes like this: "The product passed the named standard, so the trial only needs to confirm fit and install speed." I understand the logic, but it skips a step. A fire test report describes one tested assembly. Your wall, deck, or container panel may differ. The F-rating of the transit should equal the rating of the assembly it penetrates. The L-rating, which measures air leakage, is often specified below 5 cfm across the full fill range. Ask which fill range was tested. A transit tested at 40 percent fill tells you little about a fully packed frame.
For buildings, ASTM E814 / UL 1479 3 and EN 1366-3 are the core through-penetration standards. If your trial touches construction joints rather than plain penetrations, ASTM E1966 / UL 2079 also apply. For ships and offshore platforms, the IMO FTP Code 4 and class rules decide. An A-60 fire rating means the unexposed side stays below the class temperature-rise limit for 60 minutes. H-class ratings extend to hydrocarbon fires, and ISO 22899-1 covers jet-fire exposure for hazardous offshore zones.
Layer two: type approval and factory approval
Type approval certification from DNV, ABS, Lloyd’s Register, or Bureau Veritas ties a specific product family to a specific test. Our own factory holds BV approval, and our modules are rated A-0 and A-60 with IP68 ingress protection. I still tell buyers to read the scope line on any certificate, ours included. It names the frame types, module sizes, and cable ranges covered. If your trial uses a module outside that scope, the certificate does not protect you.
Layer three: the quality system behind the parts
A test report proves one batch. A quality system proves the next batch will match. We run ISO 9001 5 and IATF 16949, the automotive-grade system, because our step-core EPDM modules need repeatable rubber hardness and dimensions. For hazardous areas, also ask whether the sealing concept has been reviewed against ATEX explosion protection requirements.
| Application | Fire standard to verify | Additional approvals | Typical threshold |
|---|---|---|---|
| Buildings, BESS containers, data centers | ASTM E814 / UL 1479 or EN 1366-3 | ISO 9001, local building code listing | F-rating equal to assembly; L-rating under 5 cfm |
| Marine (ships, FPSOs) | IMO FTP Code | Class type approval (DNV, ABS, LR, BV) | A-0 or A-60 fire rating |
| Offshore hazardous zones | IMO FTP Code plus ISO 22899-1 | Class approval, ATEX review, blast resistance rating | H-120, jet fire, gas-tight integrity |
How do I confirm dimensional compatibility with my existing 120-frame cutouts during a trial run?
Every cross-reference table we publish starts at the inspection bench, where our QC team checks module widths against the 120-frame standard before a single sample ships.
Confirm 120-frame compatibility by measuring the cutout opening, frame depth, and internal packing space with calipers, then test-fitting free validation samples of the replacement modules, stay plates, and compression unit inside the existing frame. Check that the compressed module stack reaches full tightness within the original frame's travel.
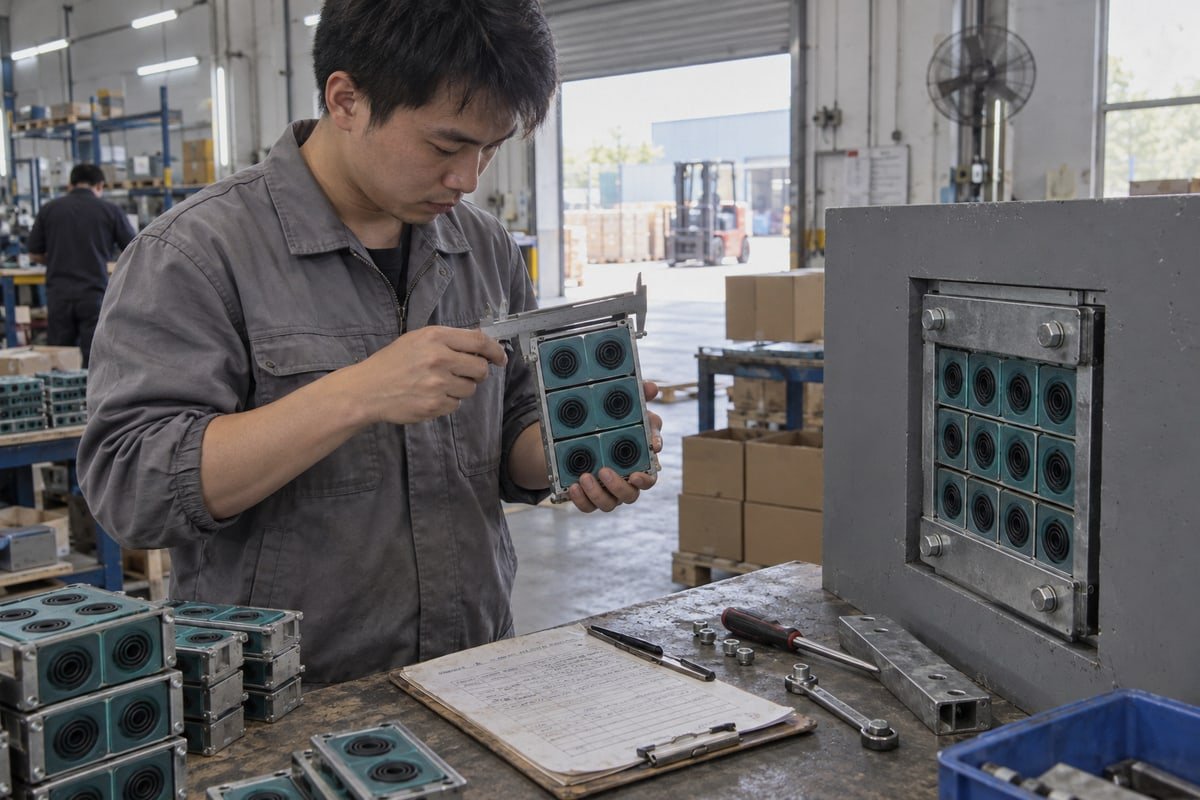
Dimensional fit sounds like the easy part. In practice it is where second-sourcing trials most often stall. A module can be two millimeters off and still look right in the box. Under compression, that error shows up as a gap or as a stack that will not close. I walk buyers through a fixed sequence.
A six-step trial-run procedure
- Measure the existing frame, not the drawing. Welded frames distort slightly. Record the internal width, height, and depth at three points each. Note any paint build-up on the inner faces.
- Log every cable diameter passing through the frame. Our step-core EPDM modules adapt to a range of diameters within one module size, so you need the real outside diameters to pick the right module, not the nominal cable size.
- Request the model cross-reference table. This maps your current module and stay plate part numbers to the equivalent DEWIN TSC square modules or TSR round assemblies. It also flags any item that has no direct equivalent.
- Order free validation samples for the mapped parts. One row of modules plus one stay plate and one compression unit is enough to prove fit. This is the point where the 40 to 60 percent cost saving becomes a real number rather than a quote.
- Test-fit and compress. Stack the modules with the cables in place. Tighten the compression unit to the specified torque. The stack should reach full tightness before the compression unit bottoms out.
- Overlay CAD/STEP files. For new cutouts, we supply STEP files so your mechanical engineer can check clearance to adjacent equipment before the trial even arrives.
What to record during the fit test
| Parameter | How to check | Why it matters |
|---|---|---|
| Frame internal width and height | Calipers at three points | Confirms module row count and spare capacity |
| Frame depth | Depth gauge | Modules must sit fully inside for fire and IP performance |
| Module width and height | Calipers on samples | Determines whether existing stay plates can be reused |
| Compression travel remaining | Ruler after final torque | Predicts re-entry capacity after future cable additions |
| Cable packing density | Count of filled versus blank modules | Confirms the trial matches the fill level in the fire test report |
One trade-off deserves honesty. Higher cable packing density saves frame space, but it also reduces spare capacity for future cables. On a BESS container or a modular data center, cables change over the asset life. I usually advise leaving some blank modular sealing blocks in the frame rather than filling every slot on day one. The trial run is the right moment to decide that ratio.
What test documentation should I request to validate fire, IP, and pressure ratings before scaling up?
Between a thick certificate binder and a fast quote, we always send the binder first. Test reports slow the sale by a week and save months of rework later.
Request the fire test report showing the tested assembly, F-rating and L-rating, the IP68 ingress protection test certificate, hydrostatic pressure test reports at the stated watertight range (0.01–0.4 MPa), gas-tight test results, and the type approval certificate that links these reports to the module part numbers in your trial order.
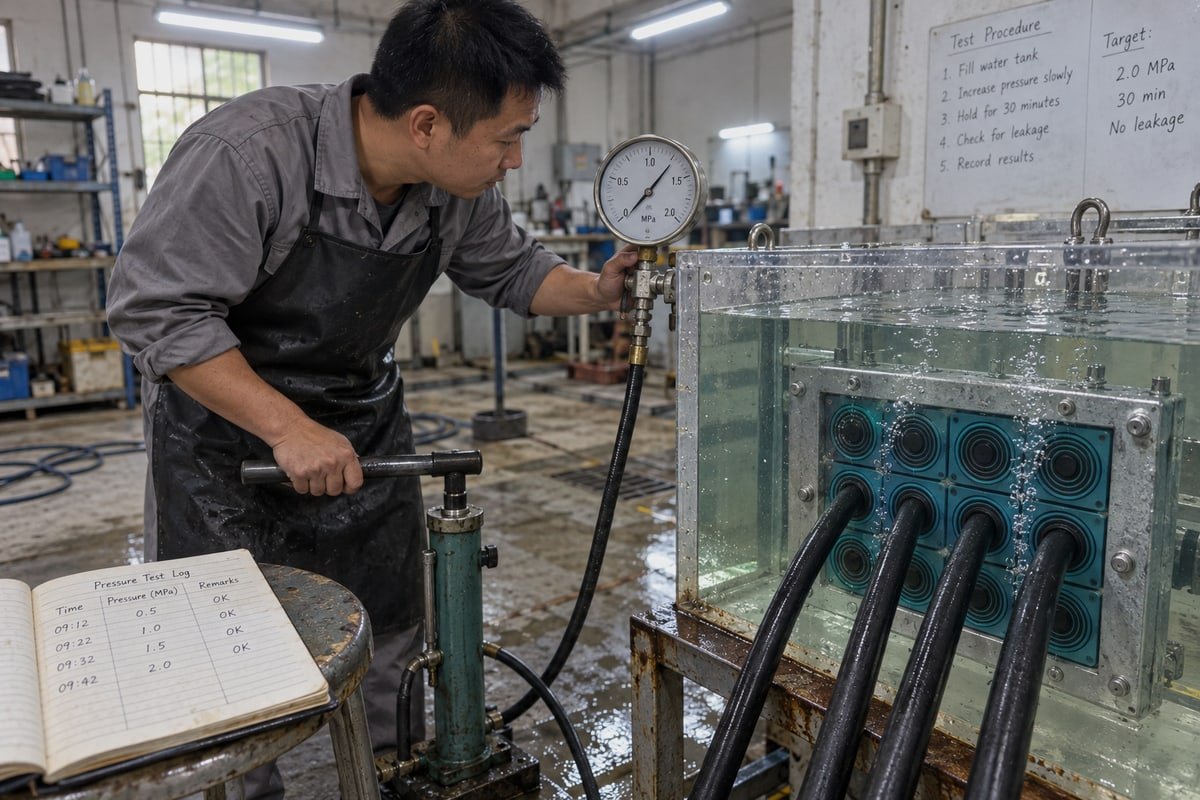
Documentation is where two buyer camps disagree. Spec-driven buyers accept the certificate and move on. Risk-averse owners want a full representative test of their own configuration. I side with the owners on principle, but I also know most projects cannot pay for a new fire test. The practical middle ground is to demand documents that describe a configuration close to yours, and then verify the gap.
The document set and its red flags
| Document | What to check | Red flag |
|---|---|---|
| Fire test report (ASTM E814 / UL 1479, EN 1366-3, or IMO FTP Code) | Tested assembly, fill range, F-rating, L-rating, thermocouple positions | Summary page only, no assembly drawing, single fill level |
| Type approval certificate | Scope of frames and modules, expiry date, issuing body | Expired date, product family names that do not match the quote |
| IP68 ingress protection certificate | Immersion depth and duration, test lab identity | Self-declared rating with no lab report |
| Hydrostatic pressure testing report | Pressure applied, hold time, direction of pressure | Pressure below your service condition |
| Gas-tight integrity report | Test gas, pressure, allowable leakage | No leakage limit stated |
| Material declaration | Halogen-free EPDM, frame steel grade and coating | Missing halogen-free statement for indoor or enclosed use |
Fire documents: read the assembly, not the headline
An A-60 fire rating on the cover means nothing without the assembly drawing. Check the deck or bulkhead thickness, the insulation, and where the thermocouples sat on the unexposed side. Marine surveyors increasingly ask for thermocouple placement guidance and dynamic testing. Onshore buyers should look for the fill range that was tested and confirm it brackets their planned fill.
IP and pressure documents: match the numbers to the site
Our modules are tested watertight and gas-tight across 0.01 to 0.4 MPa, which is 0.1 to 4 bar. Some products in the market claim water tightness up to 4.5 bar and gas and air tightness to 3 bar. Neither number matters until you compare it with your worst-case condition. A flooded cable trench, a pressurized switchgear room, or a wash-down deck each set a different requirement. Ask for the hold time as well as the pressure. A 30-second peak is not the same as a sustained head of water.
Traceability closes the loop
Every report should reference part numbers that appear on your trial order and on the module stamp itself. On our modules, the nameplate between the compression bolts carries the identifiers needed for that check. If the paperwork and the parts cannot be linked, the paperwork does not apply.
How many units should I include in my trial order to properly validate performance before full-scale procurement?
Our worst early lesson came from a two-unit trial. Both sealed perfectly, so the buyer scaled, and then his third site brought cable mixes nobody had tested.
A trial order should include enough units to cover every frame size, cable mix, and installer crew in the planned rollout—typically one complete transit per distinct penetration type plus spare modules for re-entry testing. For most integrators that means 5 to 20 frames, not a single sample.
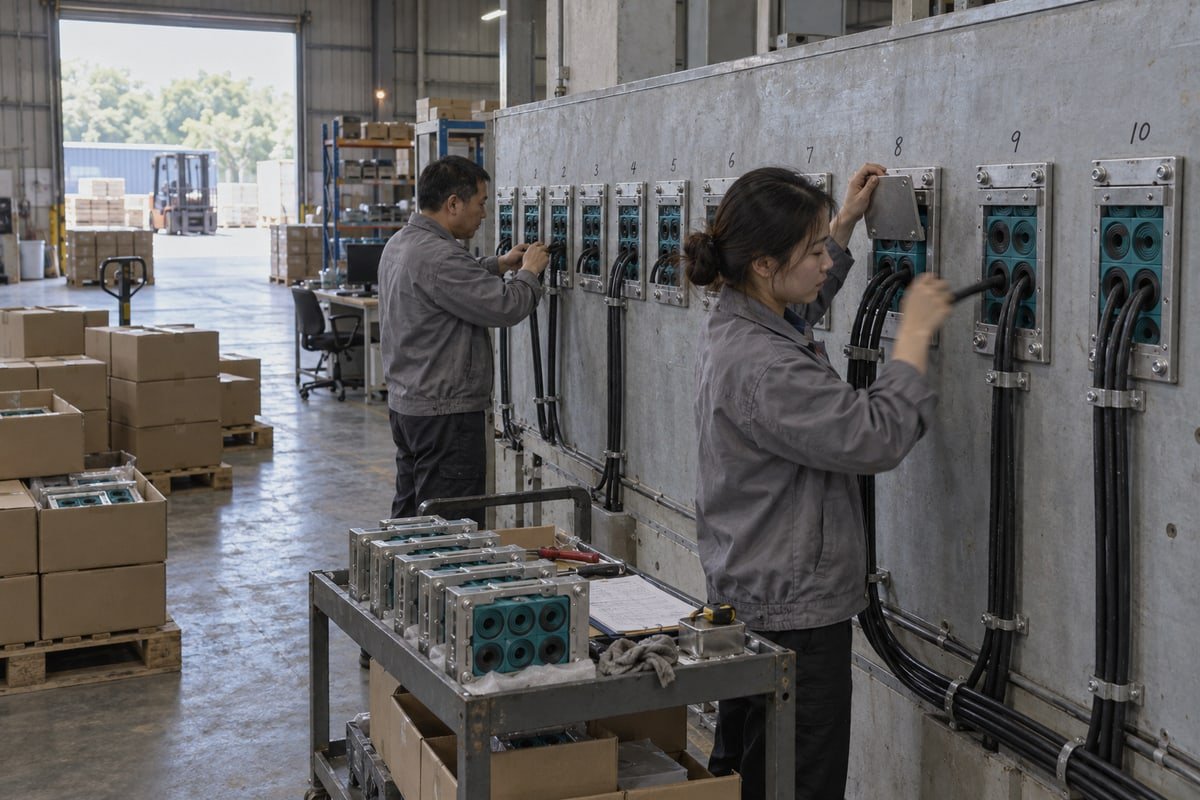
The right number is not a fixed figure. It is a function of variety. I ask buyers three questions: how many distinct frame sizes will you install, how many distinct cable mixes will pass through them, and how many crews will do the work. The trial should touch every combination at least once.
A simple sizing rule
Count your distinct penetration types. A penetration type is a unique pair of frame size and cable mix, including conduit, EMT, or pipe where relevant. Then multiply by the number of installer crews, because installation quality control is a human variable. Add one extra set of modular sealing blocks per frame for re-entry testing. That total is your minimum trial quantity.
| Buyer scenario | Distinct penetration types | Crews | Suggested trial frames | Spare module sets |
|---|---|---|---|---|
| Single BESS container prototype | 2 to 3 | 1 | 3 to 5 | 2 |
| Modular data center production line | 4 to 6 | 2 | 8 to 12 | 4 |
| EPC substation package across sites | 6 to 10 | 2 to 3 | 12 to 20 | 6 |
What each trial unit must prove
Quantity alone is not the standard. Each unit should go through the same checks.
- Installation time and torque. Record the time to first seal and the torque at which the stack closes. Consistent numbers across crews prove the design is forgiving.
- Cable handling. Cables must not be pinched, twisted, or stressed after compression. Inspect the jackets after the frame is closed.
- Pull-out resistance. Apply a controlled axial pull to a sealed cable. The module should hold the cable without shifting.
- Re-entry. Open the frame, add one cable, remove another, and re-seal. Then repeat the pressure or leak check. This is the lifecycle proof that most trials skip.
- Environment. Check frame coating and hardware for the site. Galvanized steel suits most enclosed installations; offshore and chemical sites may need stainless. Where heavy reciprocating machinery sits nearby, confirm the seal holds under vibration.
I also encourage buyers to include one frame that is deliberately overfilled and one that is underfilled. Real projects drift in both directions. If the multi cable transit trial order only tests the ideal fill, the rollout will meet the non-ideal fill without any data behind it.
Fazit
Scaling a multi cable transit trial on one good sample invites site failures. Demand certification, dimensional proof, test documents, and a representative batch; then standardize with confidence.
Fußnoten
1. Official oversight body for the IATF 16949 automotive quality management system standard. ↩︎
2. A leading classification society that provides factory approval certificates to verify manufacturing quality and compliance. ↩︎
3. Authoritative source for UL 1479, a primary fire test standard for through-penetration firestops. ↩︎
4. Official site of the International Maritime Organization, which maintains the FTP Code for marine fire safety. ↩︎
5. The International Organization for Standardization’s official page for the ISO 9001 quality management standard. ↩︎



 English
 Español de México
 Deutsch
 Français
 العربية
 Русский