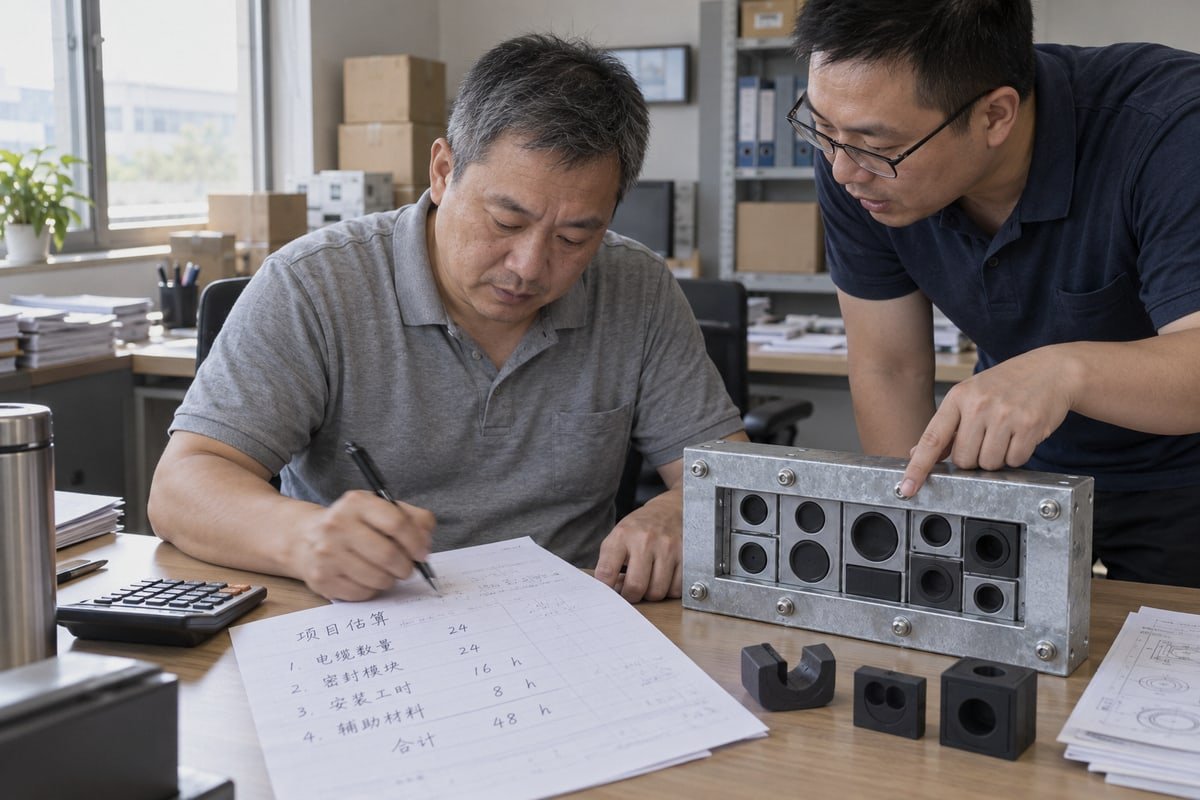
Quoting installation labor hours for multi cable transit is where our factory sees bids fail. Guess low, you lose money. Guess high, you lose the tender. Unit-rate methods fix both.
Estimate installation labor hours for multi cable transit by assigning a base man-hour unit per frame opening, typically 1.5 to 3 man-hours for basic packing of a single-window frame, then multiplying by quantity and adjustment factors for mounting method, cable density, access height, and testing, plus contingency.
That formula sounds simple. The hard part is filling in the numbers honestly. Below, I walk through how we help buyers do that, step by step, using our own module data and real site conditions.
How can I calculate installation labor hours for MCT systems accurately during the quoting stage?
A sourcing engineer in Europe once asked us for a single hour figure per frame. We sent him a formula instead, because one number would have misled his bid.
Calculate MCT labor hours with the formula: estimated hours equal quantity times a base labor unit times adjustment factors. Store the base unit in hours per opening, separate it into phases such as prep, mounting, packing, compression and testing, then price with a fully burdened labor rate and markup.
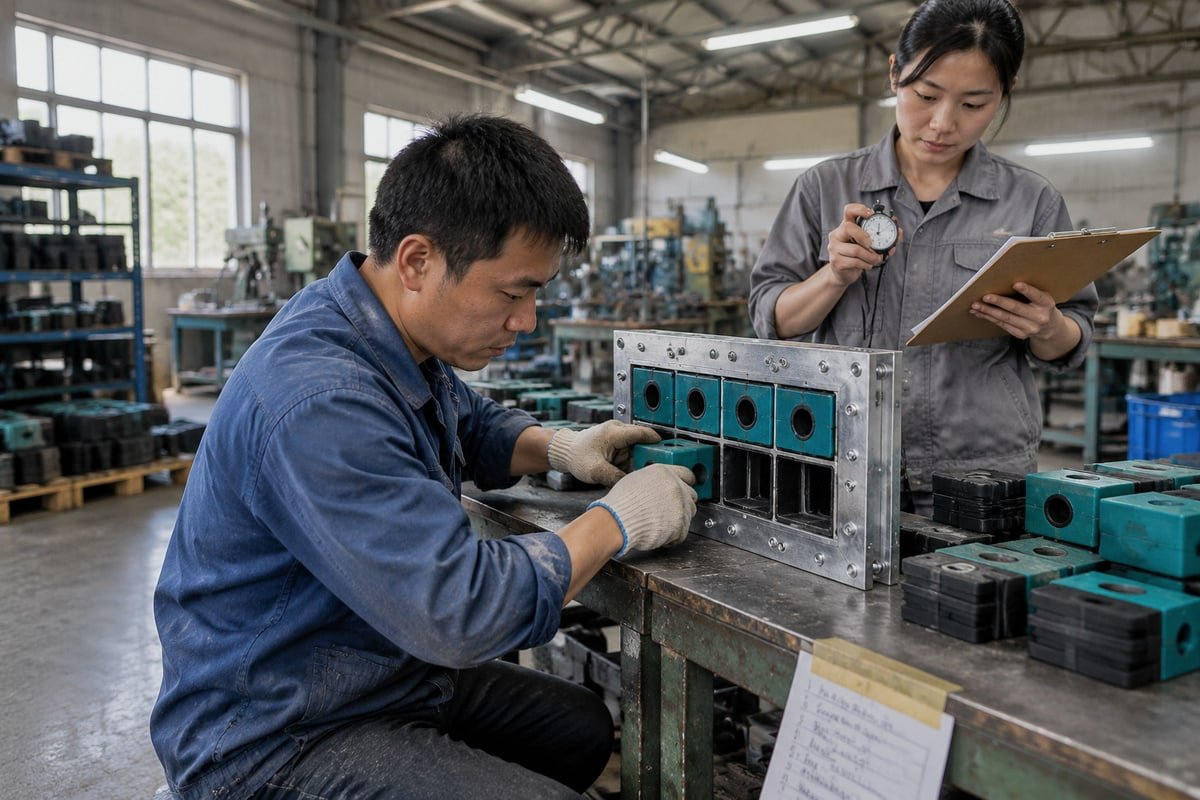
The reason I push a formula over a flat number is simple. The same TSC sealing modules can go into a frame in under an hour on a bench. The same modules can take a full shift on a congested BESS container wall. If your quote cannot explain that gap, you cannot defend it.
Start with a material takeoff, not a guess
Before any hours, we count. A proper material takeoff 1 lists every frame, every opening, and every cable with its outside diameter. From that list, you do a packing space calculation. You match each cable to a module size, add solid spare blocks, and check that the stay plates and compression wedge still fit inside the frame height. Our step-core EPDM modules cover a range of diameters within one module size, so cable diameter sizing takes fewer SKUs, but you still have to count.
Build the base labor unit in phases
I recommend storing man-hours per unit in hours, never minutes, and splitting each unit into phases. The phase split is what makes a quote auditable.
| Phase | What the installer does | Typical share of base hours |
|---|---|---|
| Layout and prep | Mark opening, clean frame internals, lubricate rubber | 10–15% |
| Frame installation | Weld, bolt, or set cast-in frame | 25–40% |
| Module packing | Select modules, peel step-core layers, insert cables | 25–35% |
| Compression and sealing | Fit stay plates and compression wedge, tighten sequentially | 10–15% |
| Testing and inspection | Visual check, pressure testing after set time, labeling | 5–10% |
| Cleanup and closeout | Photos, nameplate, documentation | 5% |
Apply the formula
The working formula is: quantity × base labor unit 2 × adjustment factors = estimated hours. Sum the openings, then multiply by the fully burdened labor rate. That rate includes insurance, travel, tools, and supervision, not just wages. Only then add markup.
Some estimators argue that a broad hours-per-transit heuristic is faster. It is, and it works for repeat jobs with the same frame and cable mix. The problem is retrofit work with unknown wall conditions. There, a phase-by-phase takeoff protects your margin. My advice is to use average historical base hours, then add explicit contingency for difficult openings, rather than quoting worst-case on everything.
What factors affect the time needed to install cable transit frames and sealing modules on-site?
On our test rig in Shaanxi, packing the same TSC modules into a bench frame takes minutes. On a site ladder at four meters, the same task takes far longer.
Installation time for cable transit frames and sealing modules depends on mounting method (welded, bolted or cast-in), cable count and diameter spread, wall thickness and substrate, new build versus retrofit, working height and confinement, hazardous-area rules, cleaning and lubrication, sequential tightening, set time before pressure testing, and crew experience.
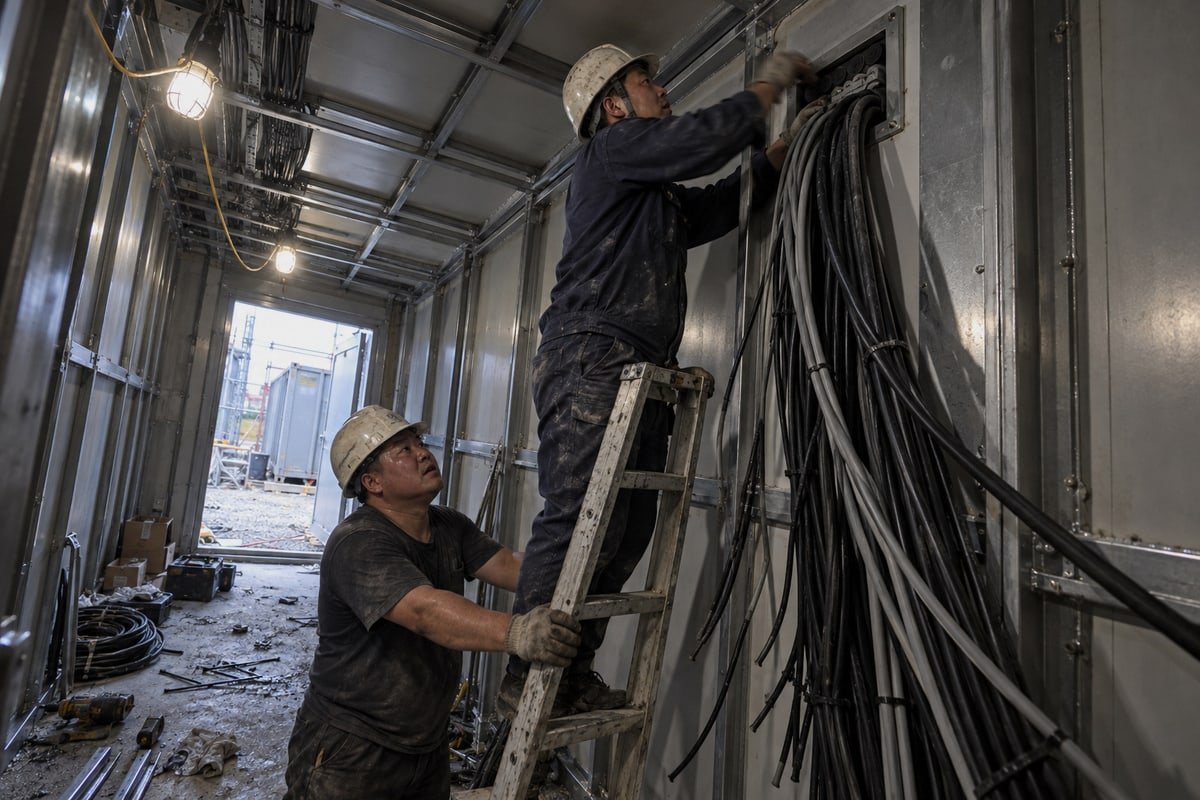
I group these factors into three buckets: the frame, the cables, and the environment. Each bucket gets its own multiplier in our quoting worksheets, and I suggest you do the same.
Welded vs bolted frames
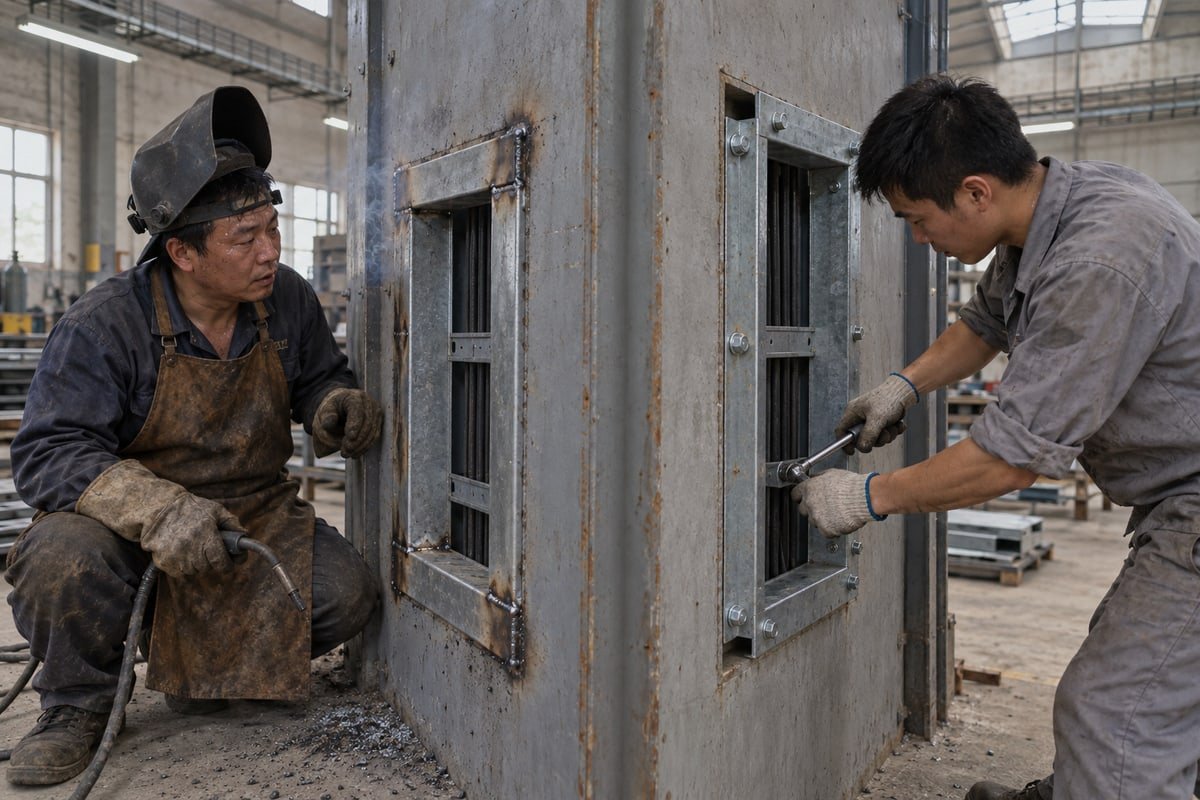
Mounting is a distinct labor category. In many jobs, it eats more time than the packing itself. A welded frame needs fit-up, welding, grinding, and coating repair. A bolted frame needs drilling, gasket placement, and torque. A cast-in frame moves most of the labor to the civil contractor, but you still pay for cleaning concrete residue out of the frame interior. When we ship frames to switchgear builders, we ask which method they use first, because that answer changes the base hours more than anything else.
Cable density and diameter spread
High cable density in a small footprint is the whole point of an MCT. It also raises packing time. Every unique cable diameter needs its own block selection and manual peeling of step-core layers to reach a certified fit. Twenty cables of one size pack fast. Twenty cables of eight sizes, some with pre-terminated connectors, pack slowly. Installation instructions also require minimum free space around the frame to insert stay plates and modules, so tight fit-up in a control panel adds hours that a cable count alone will never show.
Environmental and closeout multipliers
| Condition | Suggested adjustment to base hours |
|---|---|
| Work at height over 10 feet (about 3 meters) | +20% to +50% |
| Confined space with permit control | +30% to +100% |
| Hazardous (Ex) zone with hot-work restrictions | +30% to +100% |
| Retrofit with existing cables in place | +25% to +75% |
| Firestop penetration requiring third-party inspection sign-off | +10% to +20% |
| Inexperienced crew, first MCT job | +20% to +40% |
Two closeout items are easy to forget. First, compression units must be tightened sequentially, not all at once. Second, many specifications require a 24-to-48-hour set time before pressure testing. That set time does not consume man-hours, but it consumes schedule, and a crew standing by is a cost.
One buyer objection I hear is that the product is engineered for fast installation, so field factors should barely matter. The product side is true. Our modules are designed to drop in. But sealing verification, torque sequence, and inspection requirements still demand careful field work. Assuming a bench-speed install on a live site is the fastest way to underquote.
Can drop-in compatible MCT modules help me reduce labor hours compared to other sealing systems?
We learned early that a module which fits the frame on paper but not in the field costs more labor than any price saving returns. That lesson shaped our tolerances.
Yes. Drop-in compatible MCT modules cut labor because installers reuse existing 120-standard frame cutouts, follow the same packing plan, and avoid re-cutting or re-welding. One vendor comparison shows 20 cables sealed in 2 hours with a modular transit versus 4 hours with cable glands.
Product choice changes labor economics. Here is how the main sealing approaches compare on the factors that drive installation labor hours for multi cable transit work.
| Sealing approach | Labor profile | Where it costs time | Where it saves time |
|---|---|---|---|
| Individual cable glands | One gland, one hole, one seal per cable | Drilling and threading many holes, high hours at 20+ cables | Simple single-cable entries |
| Tool-free grommet systems | Quick for small counts, few tools | Limited density, weaker fire and pressure ratings | Light-duty enclosures |
| Modular MCT with drop-in modules | One frame, stacked modules, one compression | Frame mounting and diameter sizing | Dense bundles, retrofit into existing 120-frame cutouts |
| Non-compatible proprietary MCT | Similar to modular MCT | Requires new frame cutouts if switching supplier | Only when the frame is also new |
Why compatibility is a labor question, not just a cost question
Our TSC square sealing modules and TSR round assemblies are dimensionally compatible with common 120-frame standards. That means a second-source switch does not create a new work package. The installer uses the same frame, the same stay plates, the same compression wedge sequence, and the same packing plan. We back this with model cross-reference tables from the existing model to the DEWIN model, plus free validation samples. Buyers test fit on a sample frame before the purchase order, so the crew never discovers a mismatch at height.
The 40 to 60 percent lower component cost is the headline. The quiet benefit is that the installation productivity rate stays the same. A sourcing manager can keep his historical man-hours per unit without recalibrating.
Labor-saving practices that pair well with drop-in modules
- Pre-kit modules by opening in a warehouse. Off-site assembly can shift up to 50 percent of installation labor away from high-cost field conditions.
- Place solid spare-capacity blocks during the first install. Future moves, adds, and changes then need only a module swap, not a full transit disassembly.
- Use hydraulic pre-compression tools on multi-frame arrays instead of manual wrenches. Fatigue drops and the final sealing step speeds up.
- Match modules to the certified performance you need. Our modules carry A-0/A-60 fire ratings 3, IP68 ingress protection 4, and watertight and gas-tight sealing from 0.01 to 0.4 MPa, with test documents available on request. That avoids a second penetration system for firestop penetration duties.
A skeptical buyer may say the cheaper module could cost more in field time. That is a fair concern with untested imports. It is why we run ISO 9001 and IATF 16949 systems 5 and operate a BV-approved factory. Fit tolerances are checked at the mold, not discovered on site.
How do I use manufacturer documentation and CAD/STEP files to speed up my labor estimation process?
Every week our engineers weigh a trade-off: send a buyer a full STEP assembly, or a simple 2D cutout drawing. For labor estimation, the 3D file wins.
Use manufacturer CAD/STEP files to build a packing plan before the crew arrives, count modules and blocks directly from the model for material takeoff, and pull assembly steps, torque sequence and set time from installation instructions. BIM-based packing plans can cut field labor by up to 30 percent.
Documentation is not paperwork. It is the raw data for your labor unit. When I estimate installation labor hours for multi cable transit openings, I want four documents open at once. Here is the order I use them.
A five-step workflow
- Load the frame and module STEP files into your model. Place the frame in the wall or container panel. Check the minimum free space for inserting stay plates and modules. If clearance is short, add a congestion multiplier now.
- Assign every cable to a module in the model. This is the packing space calculation done digitally. The model tells you how many step-core layers to peel and which openings need solid spare blocks.
- Export the block list as your material takeoff. Module counts, stay plates, and compression units come straight from the model. No counting on site.
- Read the installation instructions for sequence and timing. Cleaning, lubrication, sequential tightening order, and the 24-to-48-hour set time before pressure testing all belong in the schedule.
- Turn the packing plan into a field sheet. A printed or tablet-based packing plan removes on-site trial and error. This is where the up-to-30-percent field labor reduction from digital twin and BIM integration comes from.
Documents to request from any MCT supplier
| Document | What it feeds in your estimate |
|---|---|
| STEP and 2D DXF files for frames and modules | Clearance check, packing plan, material takeoff |
| Model cross-reference table | Confirms drop-in fit for existing 120-frame cutouts |
| Installation instructions with torque sequence | Compression and sealing phase hours |
| Fire, IP68, and pressure test reports | Inspection requirements and sign-off scope |
| Spare parts list and lead times | Contingency for damaged or missing modules |
We supply all of these for our TSC and TSR ranges, and our in-house mold shop can issue STEP files for custom sizes and private-label runs. English technical support answers dimensional questions before the tender closes, not after.
One estimator objection is that this digital preparation adds office hours. It does, a little. But those hours are cheaper than site hours, and they show up once, not on every opening. Over time, the stored packing plans become your internal labor-unit library, and each job makes the next quote sharper.
Fazit
Underquoted MCT labor quietly eats margin. Build a unit-rate model, apply honest multipliers, and use our drop-in modules and STEP files to keep hours predictable.
Fußnoten
1. Essential construction estimating process for listing all materials required for a project. ↩︎
2. Official data on employer costs for employee compensation, including wages and benefits used in labor unit calculations. ↩︎
3. International maritime standards for fire-resistant divisions in ships and offshore structures. ↩︎
4. Standard definition for protection against dust and long-term immersion in water under pressure. ↩︎
5. Global automotive quality standard ensuring high-level safety and reliability in manufacturing processes. ↩︎



 English
 Español de México
 Deutsch
 Français
 العربية
 Русский