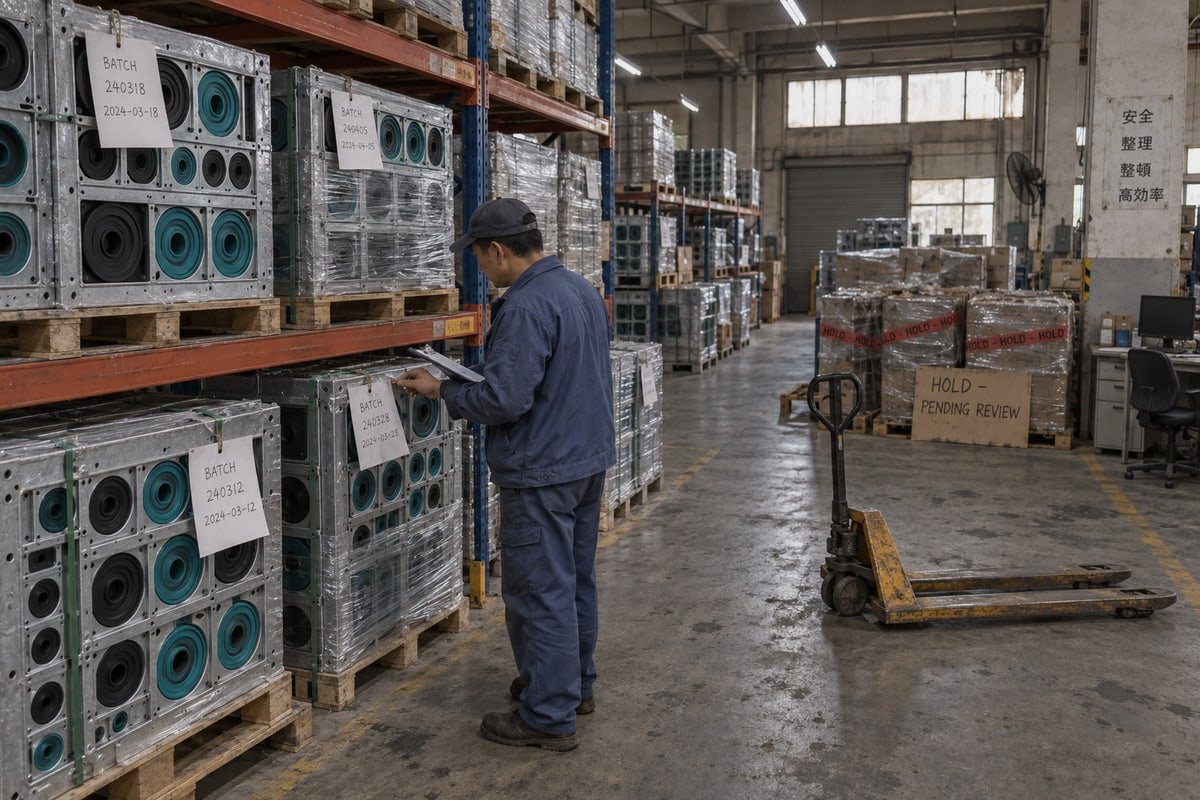
Flag state approval policy changes can turn multi cable transit modules leaving our factory into stranded stock overnight SOLAS II-2 1. I have watched buyers absorb that loss. Prevention starts before purchase.
Flag state approval policy changes impact multi cable transit inventory by invalidating older Type Approval Certificates, forcing stock segmentation by flag, raising safety stock during grace periods, and extending lead times for re-certification. Buyers limit stranded inventory by verifying approval status before purchase and stocking dimensionally compatible modules.
A cable transit is not just a part number. It is a certificate-dependent compliance asset. Below, I walk through how a policy change travels from a flag administration to your warehouse shelf, and what you can do at each step.
How do I keep my MCT stock compliant when a flag state updates its approval requirements?
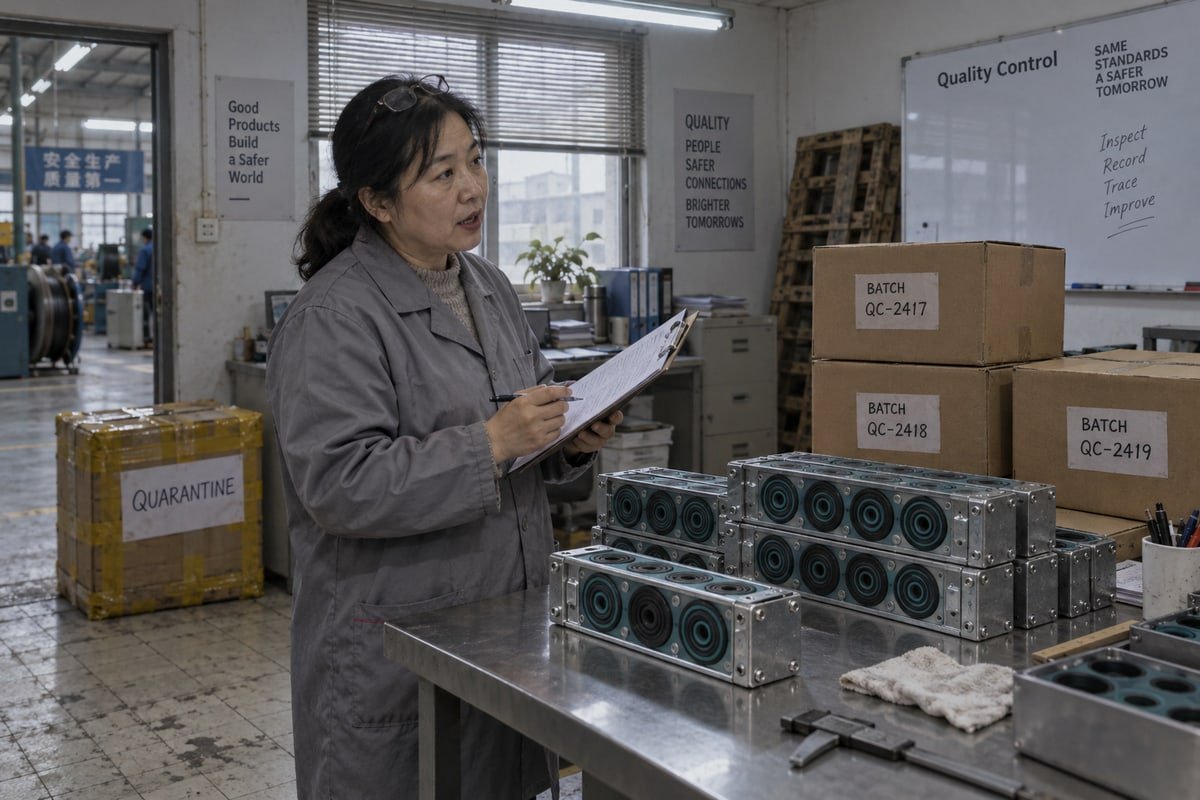
A QC audit of our outbound pallets once showed the same TSC module shipping under two different certificate revisions. Normal for a factory. Confusing for a buyer.
Keep MCT stock compliant by mapping every batch to its Type Approval Certificate revision, building an approval matrix by flag and class society, quarantining uncertain stock, and confirming acceptance with the flag or its recognized organization before installation rather than after delivery.
The chain runs in one direction. A flag administration updates its policy. That policy defines which approving bodies and test standards it accepts. Those standards decide which product variants are installable. Your warehouse planning, installation timing, and survey acceptance all sit downstream of that decision.
Where the variation comes from
Flag states do not all accept the same paper. A flag may accept approvals issued by its own administration, by a recognized organization 2 acting on its behalf, or by another body it deems acceptable. Classification Society standards from DNV, ABS, or Lloyd's Register usually form a compliance floor. IMO SOLAS regulations, especially Chapter II-2 for fire protection 3, sit above that floor. When SOLAS II-2 or the FTP Code is updated, the class societies align, and the flag follows. That alignment is what triggers an inventory audit.
Two recent shifts show how this plays out:
- Halogen-free material mandates from major registries have made older halogenated MCT stock unusable on some fleets. Our TSR and TSC modules use halogen-free EPDM, so this one has not hit our customers, but I have seen it hit others.
- New Type Approval grace periods, usually six to twelve months, create a hard enforcement date. Stock that is compliant today becomes dead stock on that date.
Building an approval matrix
I ask buyers to keep one table per fleet. It should look something like this:
| Flag | Accepted approving body | Fire class required | Material rule | Certificate revision on shelf | Status |
|---|---|---|---|---|---|
| Flag A | Own administration or RO | A-60 | Halogen-free | Rev. current | Installable |
| Flag B | RO only (DNV, ABS, LR) | A-0 / A-60 | No stated rule | Rev. prior | Quarantine |
| Flag C | EU MED wheel mark | A-60 | Halogen-free | Rev. current | Installable |
The matrix forces a decision on each bin. If the certificate revision on the shelf does not match the flag's current acceptance, that bin moves to quarantine.
Standardize or comply first?
Some operators push back here. They want one standardized transit system across the fleet to cut training and holding cost. That is a fair goal. But standardization only works if the standard product carries approvals across every flag you operate under. If it does not, you have standardized on a survey finding. My advice is to standardize on frame geometry and keep the module-level approvals flag-specific. That is exactly why we build our modules to the common 120-frame footprint.
Can dimensionally compatible drop-in modules help me avoid stranded inventory during a re-certification cycle?
The trade-off I weigh most often is simple: mold a new frame footprint or match the 120-frame standard. We chose compatibility, and it changed how buyers handle re-certification.
Yes. Dimensionally compatible drop-in modules let you replace only the sealing blocks affected by a new approval while keeping installed frames, compression units, and stay plates. This isolates the re-certification cost to the module level and stops whole-frame assemblies from becoming stranded inventory.
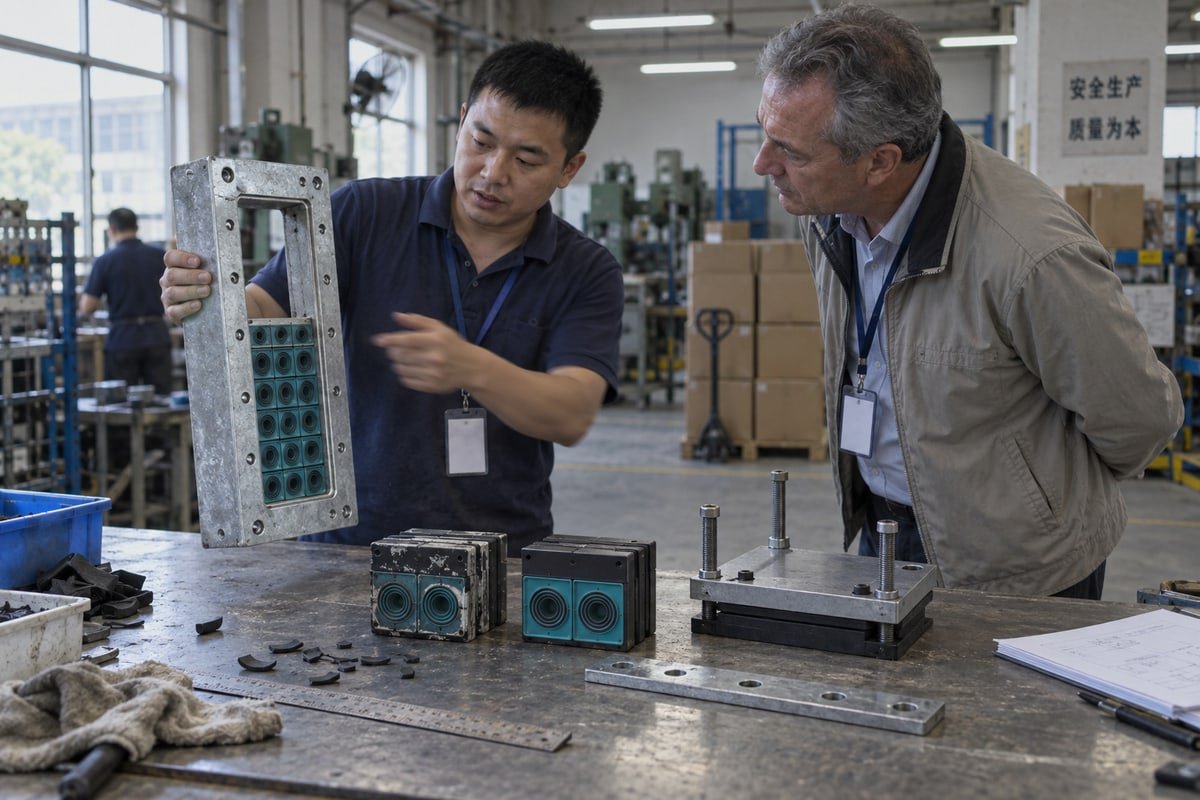
Modular cable seals are now a procurement priority for a reason. When a seal standard changes, a modular design lets you update compliance at the component level. You do not touch the welded frame in the bulkhead. You do not re-drill the penetration. You swap the blocks, torque the compression unit, and update the register.
What changes and what stays
| Component | Affected by a seal standard change? | Affected by a fire class change? | Typical action |
|---|---|---|---|
| Welded frame | No | Rarely | Keep installed |
| Stay plates | No | No | Keep installed |
| Compression unit | No | No | Re-torque after swap |
| Sealing modules (TSC / TSR) | Yes | Yes | Replace with approved revision |
| Spare module kit in warehouse | Yes | Yes | Quarantine, requalify, or rotate |
The table makes the economics clear. The frame is the expensive part to install. The modules are the part that carries the certificate. Separating those two lifecycles is what keeps stock obsolescence risk contained.
Why the step-core design matters here
Our step-core EPDM modules adapt to a range of cable diameters within one module size. That reduces the number of SKUs a buyer has to hold. Fewer SKUs means fewer bins to quarantine when a policy changes. It also means a spare module kit covers more penetrations, so safety stock stays smaller during a transition.
Second sourcing during a transition
Here is a scenario I see often. An integrator holds frames from an incumbent brand. A flag tightens acceptance. The incumbent's updated modules have a long supply chain lead time. The buyer needs installable stock now. Because our modules drop straight into the existing 120-frame cutouts, we can supply a qualified second source at 40–60% lower cost without a frame change. We back that with model cross-reference tables from the existing model to the DEWIN equivalent, free validation samples, and CAD/STEP files so the buyer's engineer can check fit before committing.
Two more points on hedging. Cross-flag reciprocity, where inventory is selected for pre-approval across multiple major registries, protects resale value and operational flexibility. And the Hong Kong Convention on ship recycling 5 pushes buyers toward inventory whose material composition is logged for end-of-life disposal. Halogen-free EPDM is a simpler story to document than a halogenated compound.
What documentation should I request from my supplier to requalify existing stock under a new flag state approval?
A sourcing manager in the Netherlands once emailed me one question: which certificate revision is the batch on my shelf? Answering took our QC team an afternoon. Too long.
Request the current Type Approval Certificate with revision and expiry, the fire test report referencing SOLAS II-2 and the FTP Code, the IP68 and pressure test reports, the installation manual matching that revision, a batch-to-certificate traceability statement, and a material declaration for halogen-free content.
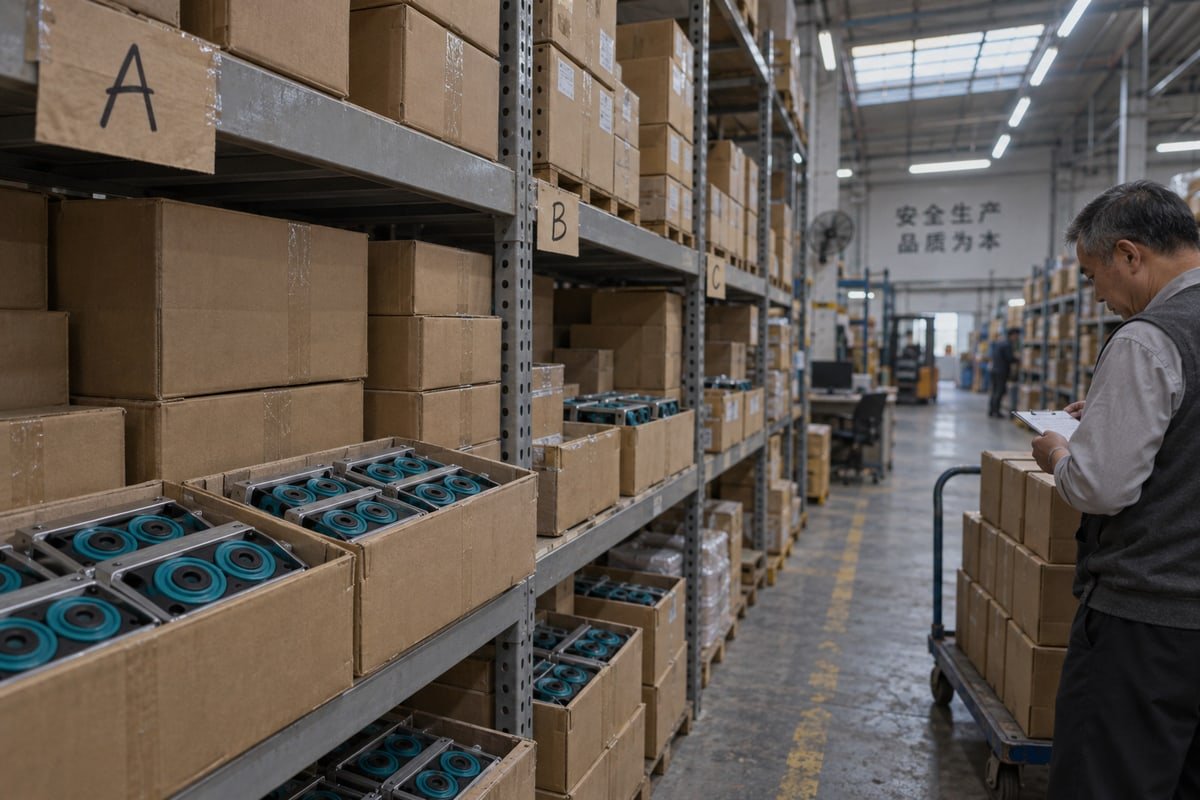
Technical compliance documentation is what turns a physical block of rubber into installable inventory. A surveyor does not test the module on board. The surveyor checks it against the approval certificate and the installation manual, then records the result in the cable transit seal register. If the paper trail breaks, the stock is worthless on that vessel regardless of how well it seals.
The requalification package
| Document | Why it matters | What to check |
|---|---|---|
| Type Approval Certificate | Establishes acceptance by class or flag | Issuing body, revision number, expiry date, scope of module sizes |
| Fire test report | Proves A-0 / A-60 fire-rated penetrations | Test standard cited, tested configuration, bulkhead versus deck |
| IP68 and pressure test reports | Proves watertight integrity and gas tightness | Test pressure range, for our modules 0.01–0.4 MPa, duration |
| Installation manual | Surveyors inspect against it | Revision matches the certificate revision |
| Batch traceability statement | Links shelf stock to a certificate | Batch or serial numbers, production date, plant of origin |
| Material declaration | Supports halogen-free and recycling rules | Compound identity, halogen content statement |
| Factory quality certificates | Shows a controlled process | ISO 9001, IATF 16949, BV factory approval |
A five-step requalification process
- Pull the batch numbers from your warehouse system for every quarantined bin.
- Send the batch list to the supplier and ask which certificate revision covers each batch.
- Compare that revision to the flag's current acceptance in your approval matrix.
- For batches that fall short, ask whether a technical equivalency notice exists. Some flag states have issued these when flame-retardant raw material shortages forced alternative compounds that meet performance but not the original material spec.
- Update the onboard register with the new certificate reference before the next survey.
Format matters now
Flag states are moving toward e-certificates, and some port inspections are already less tolerant of physical-only documentation. I keep our test documents in a form we can send the same day on request. Ask your supplier for the same. If a supplier needs weeks to produce a certificate revision number for a batch, that delay becomes your lead time.
How do I manage lead times and safety stock while waiting for updated fire and IP68 test certificates?
One lesson from more than a decade of running production in Shaanxi, Shandong, and Hunan: a certificate delay costs more than a press delay. Plan stock around paperwork.
Manage lead times by splitting inventory into three pools: certified stock for immediate installation, in-transition stock held in quarantine, and a qualified second source with compatible modules. Size safety stock to cover the grace period plus supplier certificate turnaround, and release quarantined stock only when documents arrive.
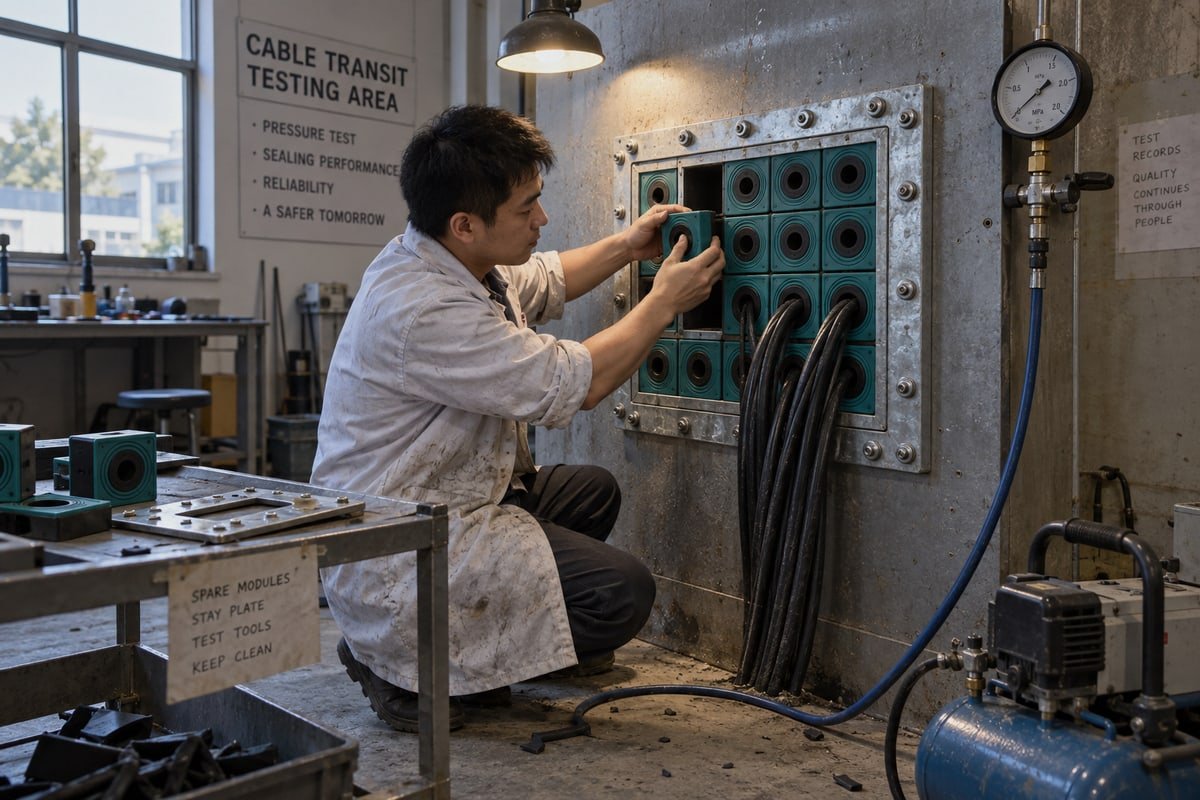
Supply chain lead times for MCT rarely come from molding. Our spare sealing modules ship fast because the molds are in-house. The lead time comes from certificate verification, manufacturer authorization, and service-supplier approval. During a flag policy transition, each of those steps gets longer because the flag itself may add verification.
A transition timeline, old stock versus new requirement
| Phase | Trigger | Inventory action | Risk if ignored |
|---|---|---|---|
| Announcement | Flag publishes updated acceptance | Freeze new purchases of the affected revision | Buying stock that dies at enforcement |
| Grace period, months 1–6 | Enforcement date set | Consume old stock on vessels where it is still accepted; open second source | Old stock idle while new stock is on order |
| Certificate wait | Supplier submits updated fire and IP68 tests | Hold quarantined stock; raise safety stock on certified pools | Project delay at survey |
| Enforcement | Grace period ends, often at 6 to 12 months | Liquidate or write down non-compliant stock | Dead stock on the books |
| Post-enforcement | Register updated | Return to normal safety stock | Over-holding and cost of carry |
This is the dump-and-replace cycle in practice. The point is to control the timing so you liquidate on your schedule, not the flag's.
Sizing the buffer
I keep the rule qualitative because every fleet differs. The buffer should cover two intervals added together: the time until enforcement, and the supplier's realistic turnaround for updated fire and IP68 documents. If the second interval is unknown, that is a supplier problem, and a second source is the fix. Watertight integrity and fire rating do not change between our A-60 module and a competitor's A-60 module of the same footprint, so a compatible second source is a real hedge, not a compromise.
Centralized or flag-segmented stock?
Large fleets often want one regional warehouse. The objection to that is real: compliance variation means the wrong approved item can reach the wrong vessel. My resolution is a hybrid. Centralize frames, stay plates, and compression units, since those rarely carry the certificate risk. Segment only the sealing modules by flag, with bin labels that carry the certificate revision. Some teams are even modeling policy shifts against current batches to rotate stock early. I treat those tools with caution, but the underlying discipline, knowing which batch dies on which date, is sound.
Conclusion
Flag state approval policy changes turn certificate revisions into inventory risk. Treat approval status as stock value, verify before purchase, and keep drop-in modules qualified.
Footnotes
1. Primary international treaty governing maritime safety and specific fire protection requirements for vessel construction. ↩︎
2. IMO guidance on organizations authorized to perform statutory surveys and certifications on behalf of flag administrations. ↩︎
3. Official IMO overview of international fire protection regulations and safety standards for merchant ships. ↩︎
4. Authoritative resource for maritime type approval certificates and technical compliance verification processes. ↩︎
5. International convention establishing standards for safe ship recycling and material composition logging. ↩︎



 English
 Español de México
 Deutsch
 Français
 العربية
 Русский