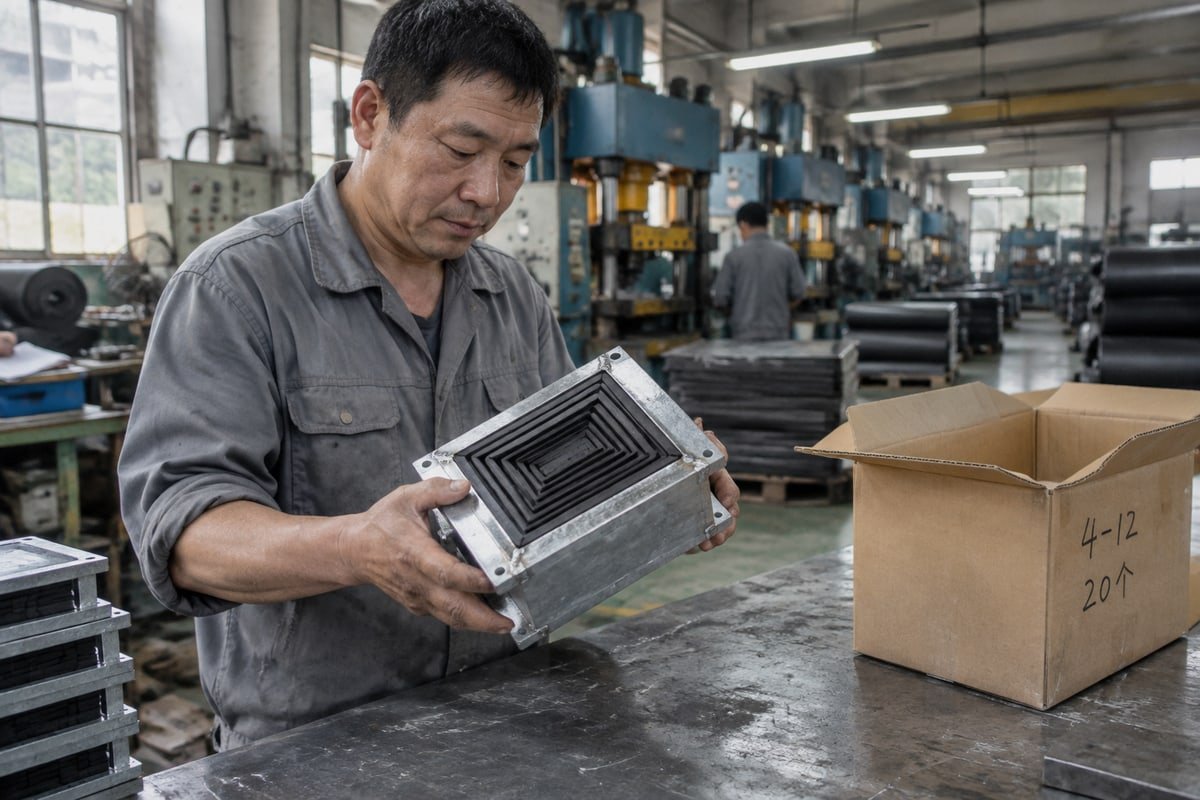
I ship free MCT samples weekly, yet in debating mailed samples vs factory visits for Chinese multi cable transit suppliers, one polished module proves little; layered checks prove more.
Mailed samples vs factory visits for Chinese multi cable transit suppliers answer different questions. A sample reliably verifies product fit, dimensions, and sealing on one unit. A factory visit or audit reliably verifies the supplier’s identity, equipment, QMS, and production consistency. Use both before qualifying a second source.
Below, I break the problem into four practical questions. Each one covers what a sample can prove, what only a visit or audit can prove, and how to tie the paperwork to the part on your bench.
Can I trust free validation samples to predict full-batch sealing performance before I commit to an order?
Last quarter our QC team pulled a TSC module off the regular molding line for a European integrator's validation sample, not from a display shelf. That choice matters.
Free validation samples can predict full-batch sealing performance only when they come off regular production tooling, ship from the registered factory address, and are tested against a written spec. A hand-finished golden sample from a sample room proves the product exists, not that every batch will seal identically.
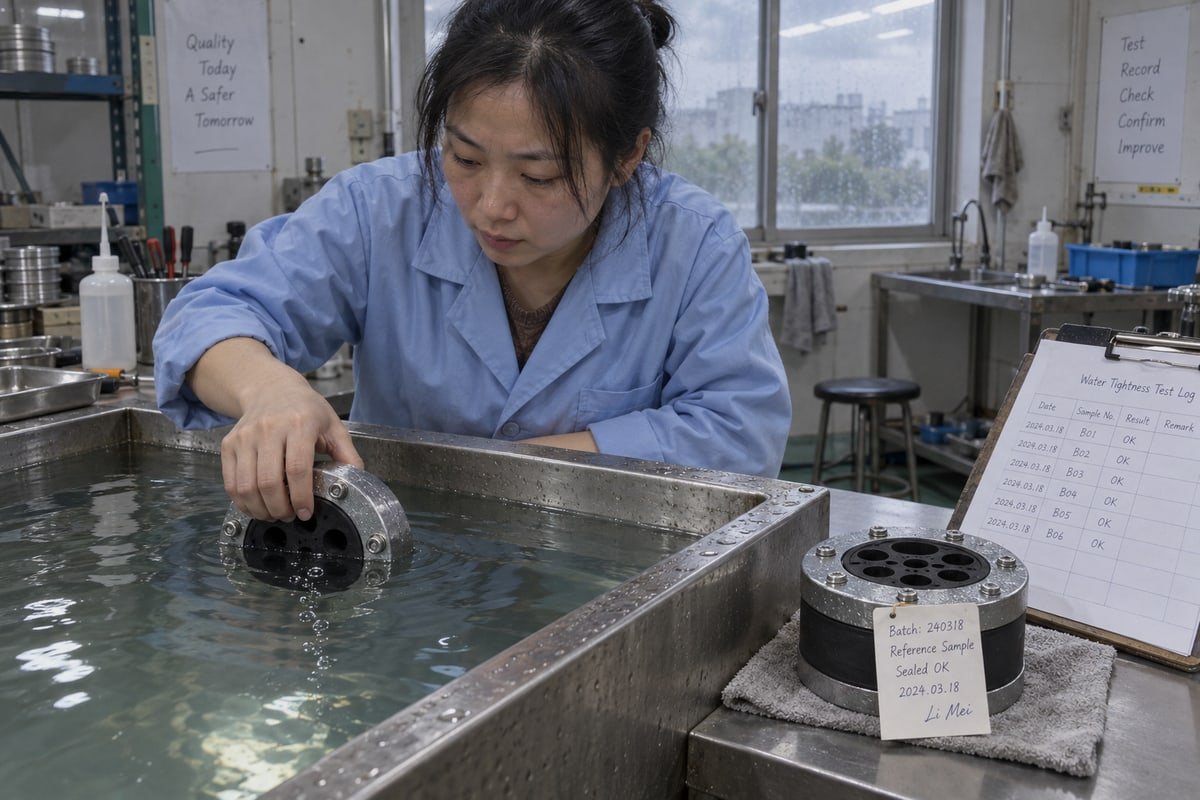
A mailed sample is a product-level check. It is fast, cheap, and honest about a narrow set of facts. The trouble starts when a buyer treats it as a supplier-level check. Here is how I separate the two.
What a mailed MCT sample can and cannot prove
| Aspect checked | A mailed sample proves | A mailed sample cannot prove |
|---|---|---|
| Frame fit and dimensions | The module drops into your existing 120-frame cutout | Every module in a 2,000-piece lot holds the same tolerance |
| Step-core cable adaptation | It grips your specific cable diameters without gaps | Core peeling behaves the same across all production shifts |
| Rubber compound | Surface finish, hardness by feel, no smell of plasticizer | The EPDM lot is halogen-free and fire-retardant in every batch |
| Sealing on the bench | One unit passes your watertight integrity testing | Repeatable IP68 results across lots and months |
| Labeling and packaging | The supplier can read and follow your spec sheet | The supplier has the staffing and discipline to repeat it |
Why a golden sample can mislead you
Some suppliers hand-finish a sample. A senior technician trims flash by hand, picks the best rubber lot, and packs it carefully. That unit looks perfect. The container-load units come from a high-speed line with different people and different pressure settings. The gap can be wide.
A common buyer objection is that samples are enough. For a low-risk spare-part order, where the only question is fit, I agree. For a BESS container or a modular data center, where the seal protects a fire boundary, fit is not the only question. Production consistency is the question. A single sample cannot answer it.
Use a sealed sample protocol
The fix is procedural, not emotional. Approve one reference sample against a written specification. Sign and date two identical units. Keep one at the factory and one on your side. Every later batch is judged against the sealed unit. This gives both sides a physical benchmark for any dispute.
Demand line samples with traceability
I also recommend three simple requests. First, ask that the sample come from regular tooling, not a prototype mold. Second, check that the courier return address matches the registered business address. Third, ask for material test reports for the exact EPDM lot used. We attach the batch mark to every sample we send from Shaanxi for this reason. It lets the buyer trace the rubber later.
What can a factory visit or video audit reveal about a Chinese MCT supplier that a mailed sample cannot?
A sourcing manager in the Netherlands once asked me to point a phone camera at our compression presses before he would read our quote. I understood why.
A factory visit or video audit reveals whether a Chinese MCT supplier is a real manufacturer or a trading company, whether it owns the molding presses and tooling for modular cable seals, how its quality control standards work in practice, and whether the site matches its registered address.
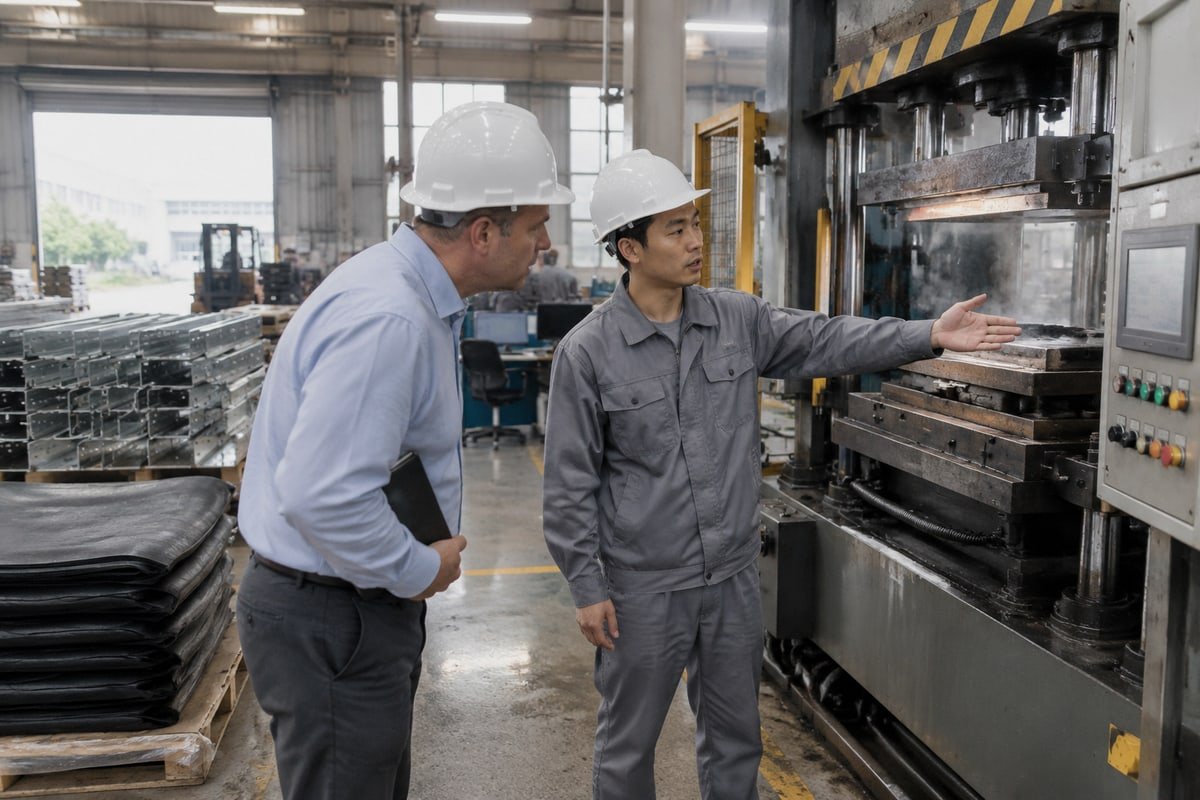
A sample proves the product can exist. A visit proves the supplier can make it again. That is the whole distinction. The table below shows what each method actually surfaces.
| What you need to learn | Mailed sample | Live video audit | In-person factory visit |
|---|---|---|---|
| Legal identity and address match | No | Partial | Yes |
| Ownership of presses and molds | No | Yes, if unscripted | Yes |
| Hidden subcontracting to other workshops | No | Partial | Yes |
| Working QMS with real records | No | Partial | Yes |
| Witness testing on a live batch | No | Yes, if streamed live | Yes |
| Personal accountability and priority | No | Some | Strong |
Manufacturer or trading company?
This is the first thing a visit settles. A trading company can mail an excellent sample sourced from a factory it does not control. The next order may come from a cheaper workshop it never disclosed. Walking the floor, or watching an unscripted walk-through, shows whether the people who quoted you are the people who mold the rubber. Our headquarters is in Shaanxi, with production also in Shandong and Hunan. Any of those sites can be shown live, because they are ours.
The machinery question
MCT block production needs specific equipment. Compression molding presses 1 with enough tonnage, curing control, and a mold shop for custom sizes. If a supplier claims in-house mold making but cannot show a single mold cabinet, that claim is marketing. During a video audit, I ask buyers to name a random module size from our cross-reference table and ask to see its mold. It is a fair test.
A QMS you can see, not just a PDF
A certificate on a wall proves an audit happened once. A working system shows calibrated gauges, filled inspection sheets, and a rejection bin with real rejects in it. Ask to see the last week's incoming rubber inspection records. Ask how a nonconformance is closed. A supplier who runs ISO 9001 2 and IATF 16949 daily can answer in plain terms. One who borrowed a certificate cannot.
Witness testing and live data
For safety-critical orders, ask to witness a pressure test or a fire test on your actual batch. A third-party inspection agency can stand in for you. Some Chinese plants now share real-time line data through monitoring dashboards, which sits between a static sample and a flight. Face-to-face contact also builds accountability. A supplier who has shaken your hand answers emails faster.
How do I verify ISO 9001, IATF 16949, and BV test documents match the physical samples I received?
Early in our export years we learned that a PDF certificate persuades nobody unless the buyer can tie it to the exact module on their bench.
Verify certificates by checking the certificate number in the issuing body's online registry, matching the legal entity name and site address to the factory that shipped your sample, and then matching model numbers, material compound, and batch marks on the physical module to the test report and the certificate's scope.
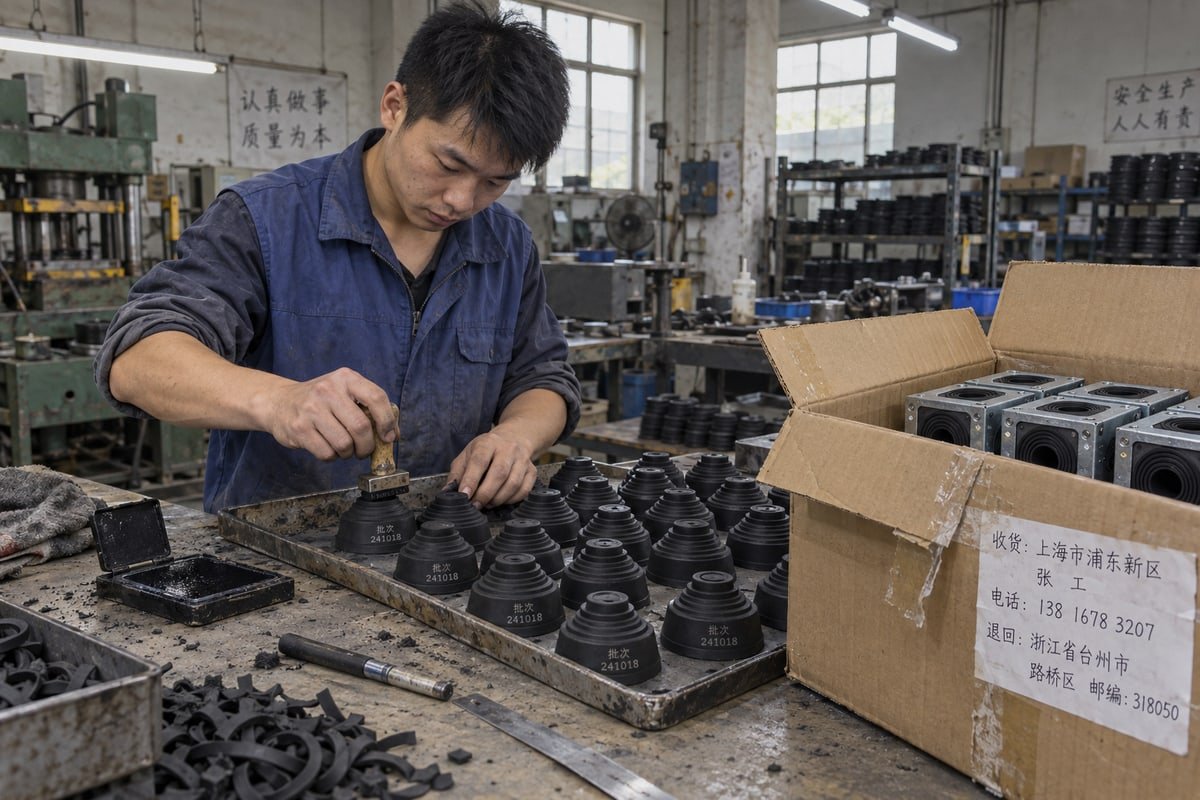
Document verification is a chain. Every link must connect to the next. If one link is missing, the certificate tells you about some company, somewhere, at some time. It does not tell you about your part. I walk buyers through this process in six steps.
- Confirm the certificate exists. Enter the certificate number in the certification body's public registry. Check the expiry date and the current status.
- Match the legal entity. The company name on the certificate must match the name on the business registration 3 and on your commercial invoice. Spelling variations are a warning sign.
- Match the site. ISO 9001 and IATF 16949 4 certificates list the audited site address. That address should be where your sample was molded and shipped from.
- Read the scope line. The scope should name cable transit or sealing module manufacturing. A certificate for general rubber parts or trading is not the same thing.
- Match the type approval to the model. A BV factory approval or type approval lists specific product families and ratings. Your sample's model number should appear in that scope.
- Match the batch. Material test reports and pressure test records carry lot numbers. The batch mark on the module should trace to them.
What each document should tell you about your sample
| Document | What it covers | How to match it to the module in hand |
|---|---|---|
| ISO 9001 certificate | The quality management system at a named site | Site address equals the shipping origin; scope names cable transit products |
| IATF 16949 certificate | Automotive-grade process control, PPAP-style discipline | Same entity and site; ask for the control plan for your module family |
| BV factory approval | Approved production of listed MCT types | Your model number sits inside the approved family |
| Fire rating certification | A-0 and A-60 division performance | Module type, frame type, and insulation arrangement on the report equal your sample configuration |
| Ingress and pressure reports | IP68 and watertight, gas-tight sealing across 0.01–0.4 MPa | Test specimen description equals your model; pressure range covers your project need |
| Material test reports | EPDM compound properties, halogen-free status | Lot number on the report equals the batch mark on the rubber |
Certification chain verification during a visit
Classification societies such as BV, DNV, and ABS approve specific production sites and processes 5. A supplier with three plants may hold approval for one. During an audit, ask which line produced your sample and whether that line is the approved one. We keep our BV approval, fire rating certification, and pressure test documents available on request. We also mark modules so the buyer can trace them. That is the only way a document and a physical part can be said to match.
Should I combine sample testing with a virtual factory audit before qualifying a new MCT second source?
Every week I weigh the same trade-off: a buyer wants a fast second-source decision, but a fast decision built only on a sample can cost a project later.
Yes. Combine measured sample testing with a virtual factory audit before qualifying a new MCT second source. The sample confirms dimensional compatibility and sealing on your cables; the audit confirms the supplier, equipment, and quality system behind it. Reserve an in-person visit or third-party inspection for large or safety-critical orders.
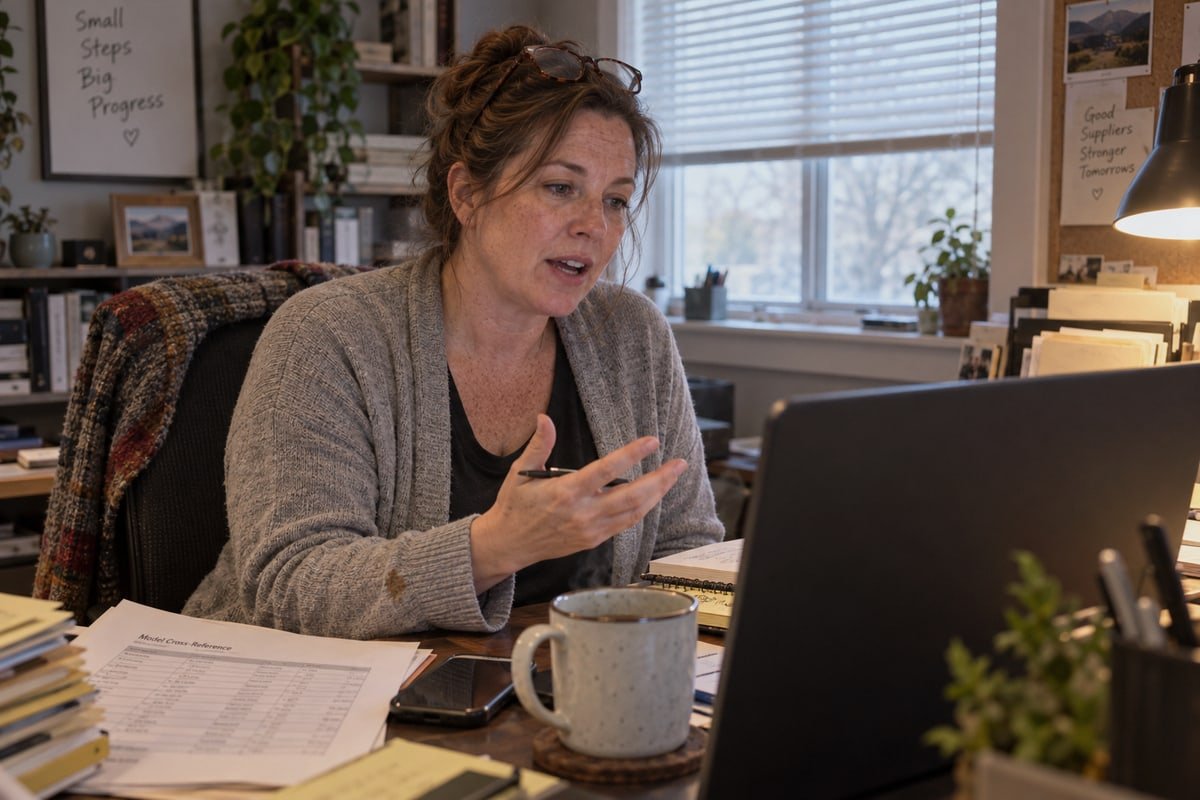
The best sourcing teams I work with no longer argue about samples versus visits. They stack verification in layers. Each layer costs a little more and proves a little more. Here is the layered supplier verification process I recommend for modular cable seals.
The four trust layers
- Documents. Business registration, ISO 9001, IATF 16949, BV approval, fire rating certification, and material test reports. Cost: a few hours of desk work.
- Sample. A free validation sample from regular tooling, measured against your spec sheet and your existing frame. Cost: one week and a bench test.
- Virtual audit. An unscripted live video tour of presses, mold shop, incoming inspection, and finished-goods area. Cost: one hour.
- Visit or third-party inspection. A physical audit, witness testing, and a pre-shipment inspection on the first production lot. Cost: travel or an agency fee.
A decision framework by order size and risk
| Order profile | Minimum verification | Recommended add-on |
|---|---|---|
| Spare sealing modules, low value, non-critical | Documents plus sample | Photo evidence of batch marks |
| First order for a repeat OEM part | Documents, sample, virtual audit | Sealed sample protocol |
| Container-scale order for BESS or data center | Documents, sample, virtual audit, pre-shipment inspection | Third-party inspection of the first lot |
| Fire-boundary or offshore application | All four layers | Witness testing of pressure or fire test on your batch |
Resolving the two common objections
Some buyers tell me a sample is enough. They are right when the question is product fit. Our cross-reference table maps existing models to DEWIN models, and a free sample settles fit in a day. They are wrong when the question is who will make lot number twenty. Other buyers tell me only a flight to China counts. They are right for high-stakes orders. They are wrong that nothing short of a flight helps. A virtual factory audit catches most trading companies and most missing machinery. It is a strong pre-screen that makes the eventual visit shorter and better targeted.
Why we push both, even though we are the second source
A second source only saves money if it never fails. Our pitch is 40–60% lower cost with the same drop-in compatibility. That pitch collapses the moment a batch leaks. So we would rather a buyer test our sample hard, audit our line on camera, and then send an inspector before the first container leaves. It protects the buyer, and it protects our long-term position on their approved vendor list.
Conclusion
A leaking seal ruins a project. A polished sample cannot rule that out. Test samples for the product, audit factories for the supplier, and qualify your second source on both.
Footnotes
1. Technical overview of the compression molding process used to manufacture modular cable seals. ↩︎
2. Authoritative source for the ISO 9001 quality management standard mentioned for supplier evaluation. ↩︎
3. U.S. government resource for performing due diligence and verifying foreign business registrations. ↩︎
4. Official site for the IATF 16949 automotive quality standard used to verify production discipline. ↩︎
5. DNV is a leading classification society that certifies production sites and technical product types. ↩︎


 English
 Español de México
 Deutsch
 Français
 العربية
 Русский