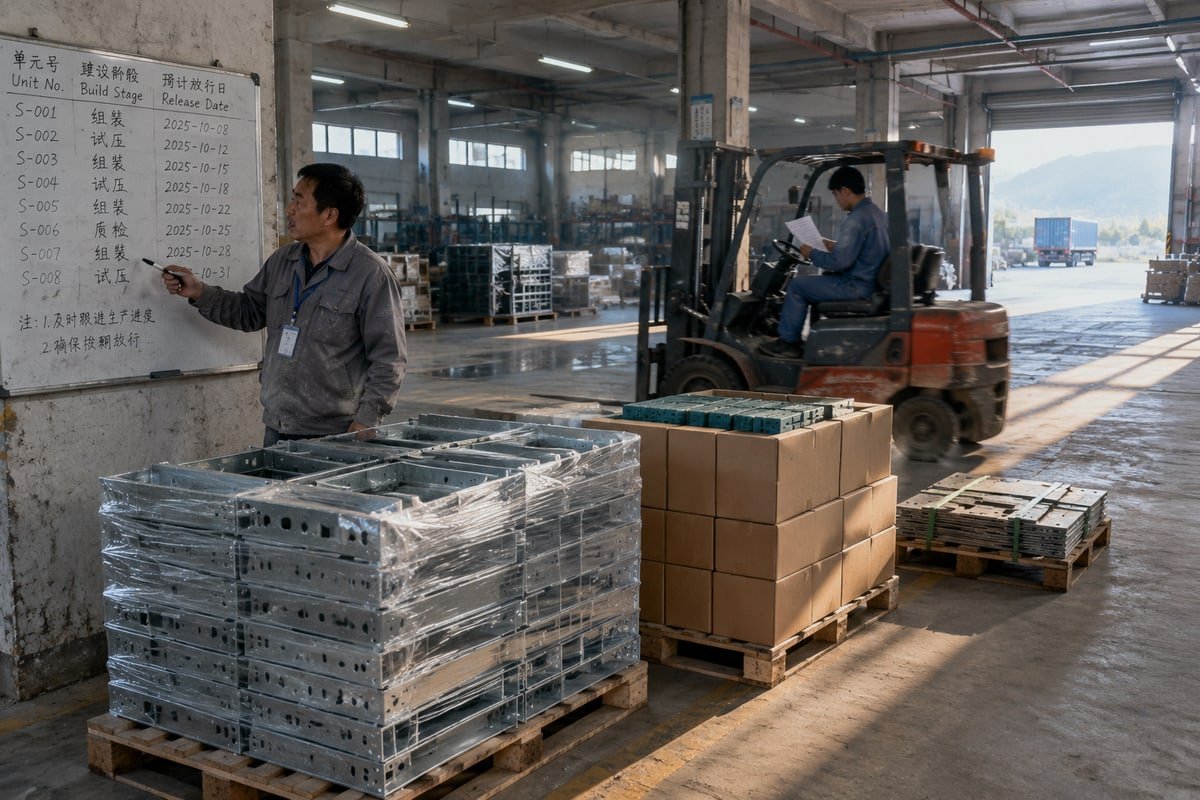
Staggered deliveries for multiple multi cable transit E-House orders fail when logistics comes last. I have seen site crews idle while our sealing modules waited at customs.
Schedule staggered deliveries for multiple multi cable transit E-House orders by building a workback plan from each unit’s commissioning date, releasing MCT batches against confirmed build stages, holding a small validated buffer, and locking certification documents to every shipment lot.
That is the short version. The rest of this article shows how we plan it with buyers. I will cover build-stage coordination, lead times and buffers, sample validation, and documentation control for cable sealing systems delivered over many months.
How can I coordinate staggered delivery schedules across multiple E-House build stages without delaying final assembly?
A sourcing manager in Europe once sent me four E-House purchase orders with one delivery date. Our planners pushed back, because his fabricator needed frames weeks before modules.
Coordinate staggered delivery schedules by splitting each E-House into build stages, matching MCT frames to structural fabrication, sealing modules to cable pull, and spares to commissioning, then releasing every batch against the fabricator's master delivery schedule with a confirmed readiness gate.
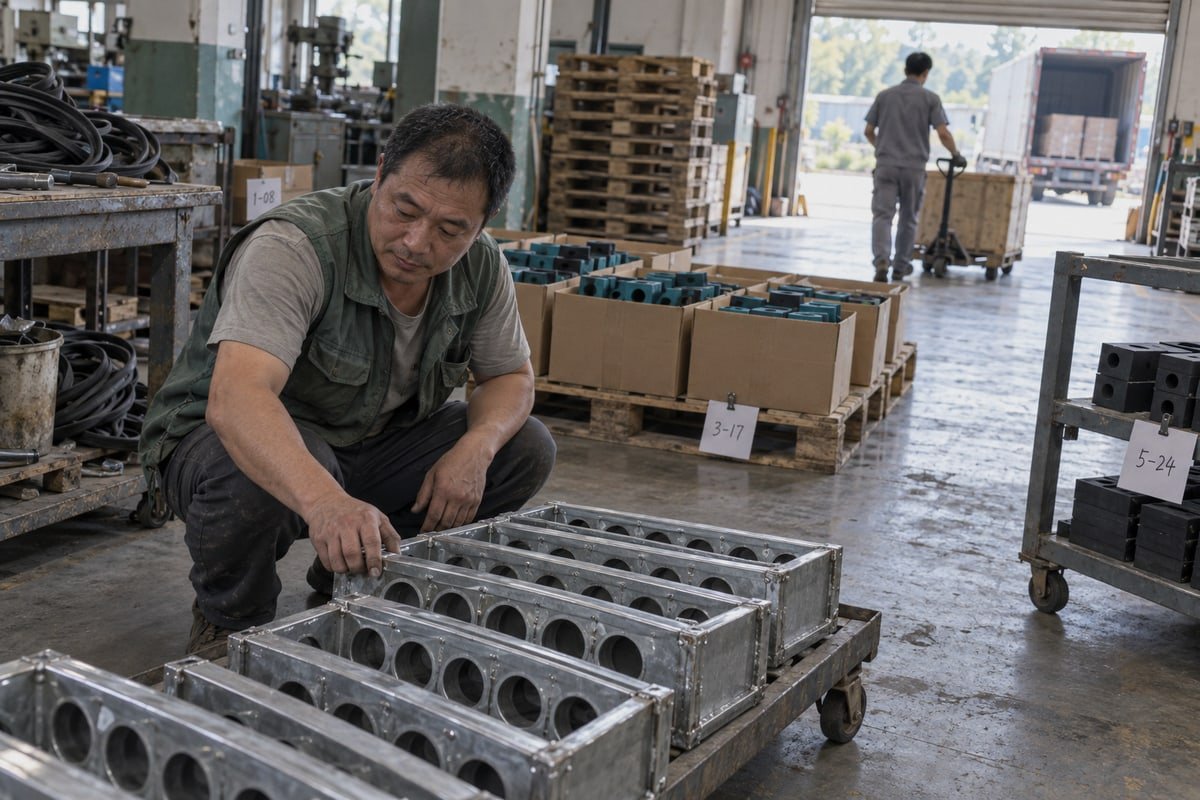
The mistake in that four-order request was simple. The buyer planned MCT as one line item. In reality, a multi cable transit package touches three different build stages. Each stage needs a different part of the kit. If you ship everything at once, the frames arrive too late and the modules arrive too early.
Build the workback schedule from commissioning, not from the PO date
We always start at the end. Take the commissioning date for each E-House. Work backward through site set, cable pull, FAT, packaging, and factory release. Modular substation logistics only saves time when this chain is defined before fabrication starts. Some E-House suppliers quote global lead times of around 12 weeks, and one walk-in unit in 2025 was delivered in roughly 6 to 10 weeks depending on customization. That leaves very little room for a late penetration drawing.
| E-House build stage | MCT scope needed on hand | Release trigger | Risk if the batch is late |
|---|---|---|---|
| Structural fabrication | Frames, stay plates, gland-plate cutouts | Approved penetration drawing | Wall panel rework or field-cut openings |
| Cable pull | TSC/TSR sealing modules, spare blanks | Frozen cable schedule | Crew idle, temporary seals used |
| FAT / pre-commissioning | Compression units, nameplates, torque record | FAT date confirmed | Failed IP68 or fire-seal inspection |
| Site commissioning | Spare modules, service kit | E-House shipment release | Punch-list stays open |
Sequence by critical path, not by purchase order number
The second rule is to ship the unit that unlocks downstream work first. That is usually the E-House needed for the utility tie-in or the controls room. We kit each batch per unit number so parts from order two never mix with order three. Some project reports claim installation-ready kitting cuts manual sorting labor by up to 30 percent. I treat that figure as project-specific, but the direction is right.
Now the objection I hear most: staggered shipments add coordination complexity. That is true. Our answer is a single logistics coordinator on each side, one shared master delivery schedule 1, and a weekly review with engineering, procurement, and commissioning. Where the fabricator uses 4D BIM 2, we can tie our release dates to module completion status in their model. This kind of supply chain coordination is what makes prefabricated building procurement work. Without it, the site installation sequence drives the schedule instead of the other way round.
What lead time and buffer stock should I plan for when ordering MCT modules in phased batches?
Every phased order forces the same trade-off on our production floor: cut extra EPDM modules early and tie up capital, or run lean and risk a stalled cable pull.
Plan lead time by component class: standard sealing modules are the shortest, welded frames and compression units are mid-length, and custom or fire-rated transits are longest. Hold a buffer of roughly one build stage of modules plus spare blanks, sized by cable-schedule uncertainty rather than a fixed percentage.
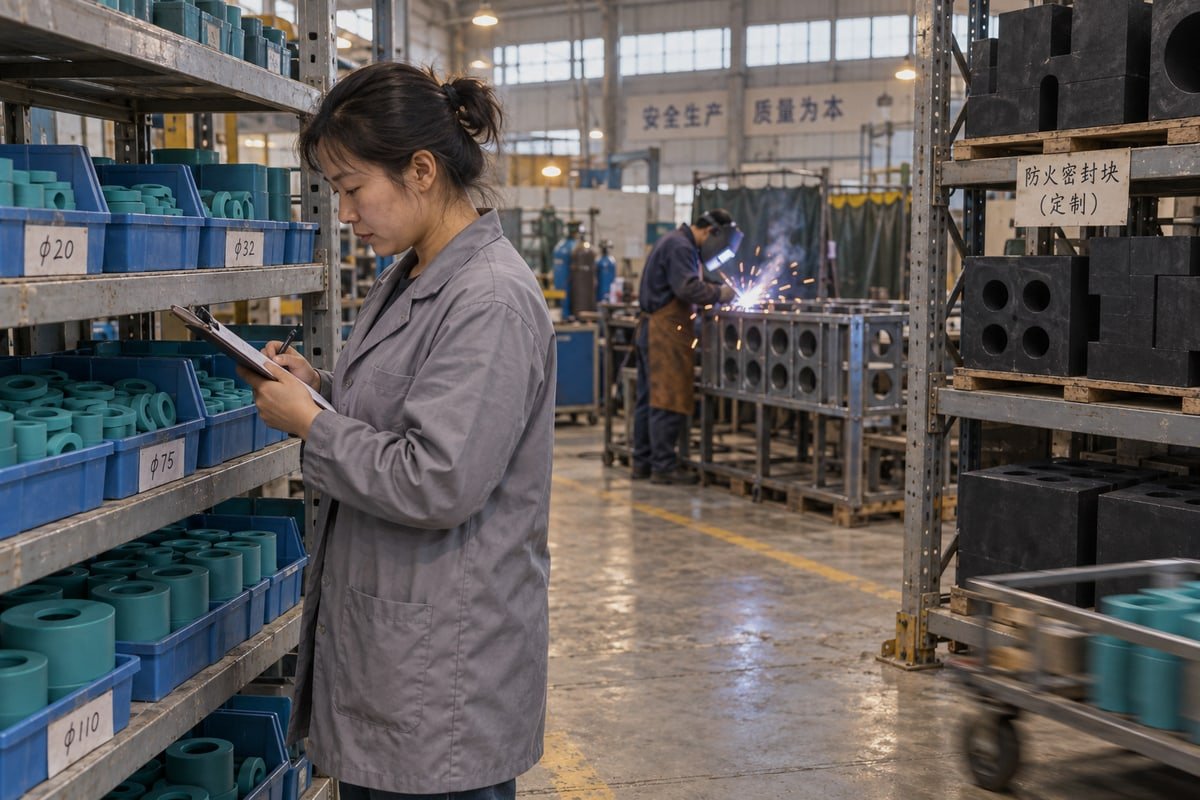
Lead time is not one number for an MCT package. It depends on what is inside the box. I break every phased order into three classes and plan each one separately.
| Component class | Main lead-time driver | Buffer approach we recommend |
|---|---|---|
| Standard TSC square and TSR round modules | Catalog molds, stocked halogen-free EPDM compound | Small rolling buffer, released just-in-time per unit |
| Frames, compression units, stay plates | Welding, galvanizing, frame size | Order per unit, no buffer beyond spare hardware |
| Fire-rated A-60 or custom-size transits | Mold making, fire-test documentation | Order full project quantity early, stagger release dates |
Why step-core modules shrink your buffer
Our modules use a step-core design. One module size covers a range of cable diameters. So when the cable schedule changes late, the same module often still fits. That means your buffer does not need to cover every possible diameter. In our experience, a sensible buffer is one set of blanks per frame plus a few modules in the widest diameter band. That is inventory buffer management driven by uncertainty, not by habit.
Treat fire-rated transits as long-lead items
Fire-rated cable transits sit on the critical path. One public tender for multi cable transit supply 3 set a five-month delivery period and attached penalties for delay. That tells you how buyers view this scope. For A-0 and A-60 rated frames 4, we advise securing the bulk material and molds early. Then we hold finished stock in our warehouse and release it in dated batches. This gives you just-in-time delivery on site without the risk of running out.
The counter-argument is real. Early delivery creates storage and damage risk. Late delivery stalls the crew. The solution is to hold the buffer at the factory under a call-off agreement, not on site. When batches do stage on site, keep EPDM modules in sealed cartons, out of direct UV and away from extreme temperatures. Elastomer that sat in the sun for six months will not compress the same way as fresh stock.
Can DewinMCT confirm dimensional compatibility and provide validation samples before I commit to a staggered order plan?
Before any phased plan is signed, our QC bench mounts the sample module into a 120-frame cutout and torques the compression unit, because compatibility on paper proves nothing.
Yes. DewinMCT confirms dimensional compatibility through model cross-reference tables mapping existing 120-frame standard modules to TSC and TSR equivalents, supplies CAD/STEP files, and ships free validation samples so your fabricator can test fit, compression and sealing before the first staggered batch is released.
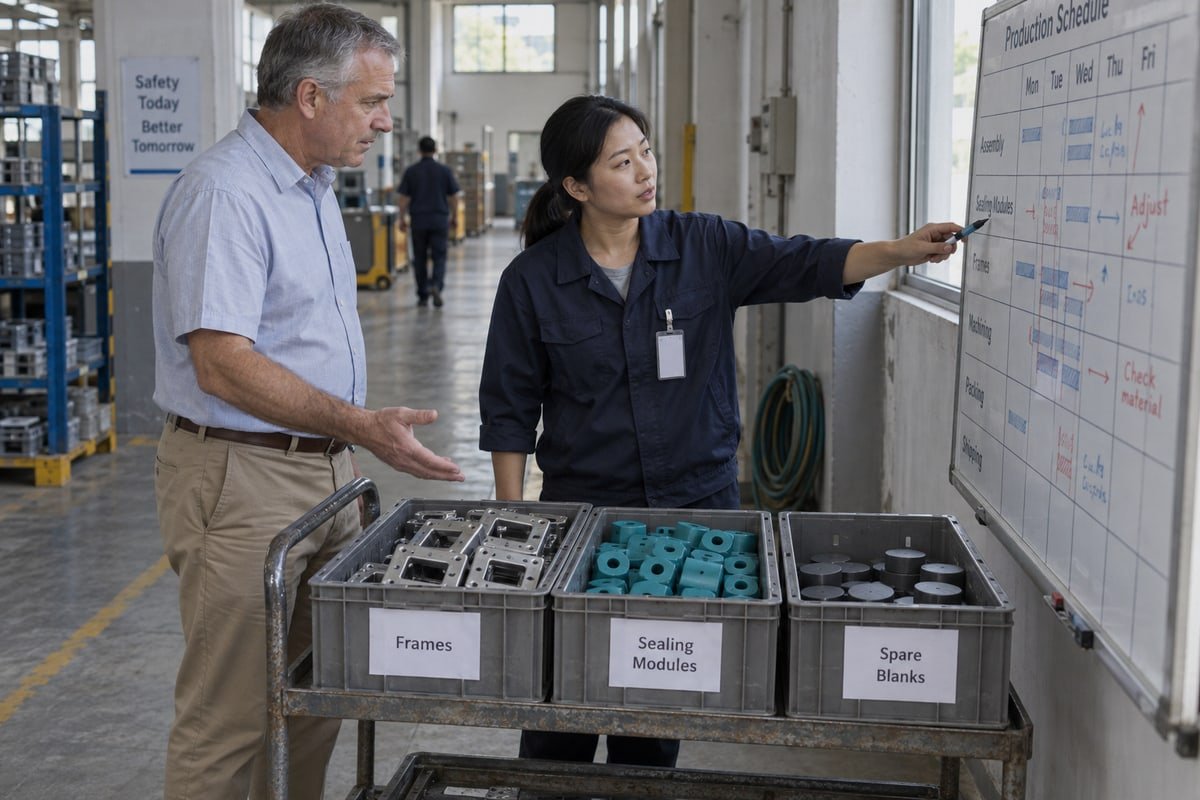
A staggered plan spanning many months only works if the first batch fits. If the frame cutout is wrong on unit one, every later release is wrong too. So we front-load validation. Here is the sequence we run with new OEM and EPC buyers.
The five-step validation sequence
- You send the existing bill of materials with current supplier model numbers and the penetration drawings.
- We return a cross-reference table listing each existing model against the matching DEWIN TSC or TSR module, plus STEP files for the frames and modules.
- We ship free validation samples of each model family in the plan. This includes at least one frame, stay plates, a compression unit, and modules across the diameter bands you use.
- Your fabricator installs the sample in an existing 120-frame cutout, checks stack height, and torques the compression unit to the specified value.
- Both sides sign the compatibility record. Only then do we schedule the phased releases.
| Check on the sample | Method | What passing looks like |
|---|---|---|
| Frame fit | Drop into existing cutout | No shimming or grinding needed |
| Stack height | Build full column with stay plates | Compression unit closes within its travel |
| Диапазон кабелей | Fit smallest and largest cable from schedule | Step-core module seals both without changing size |
| Sealing | Pressure or water test to project spec | Meets the IP68 or watertight requirement on the drawing |
This is how we act as a qualified second source rather than a cheap alternative. The 40 to 60 percent cost saving is only useful if the module drops into the same frame with no redesign. For sizes outside the standard range, our in-house mold shop makes custom cable entry seals 5, and we validate those the same way. The sample stage also catches problems in the cable schedule itself. More than once a fabricator has found that a cable diameter on paper did not match the drum on the floor. Finding that on a sample is cheap. Finding it on the sixth E-House is not.
How do I ensure consistent certification and quality documentation across multiple shipments delivered over an extended project timeline?
The hardest lesson from our early export years was simple: a certificate issued for shipment one does not automatically satisfy an auditor inspecting shipment six a year later.
Ensure consistent certification across staggered shipments by fixing the approved specification, test reports and drawing revisions in the frame contract, then requiring every lot to ship with batch-traceable certificates of conformity, packing lists tied to unit numbers, and the same ISO 9001 and IATF 16949 controlled documentation.
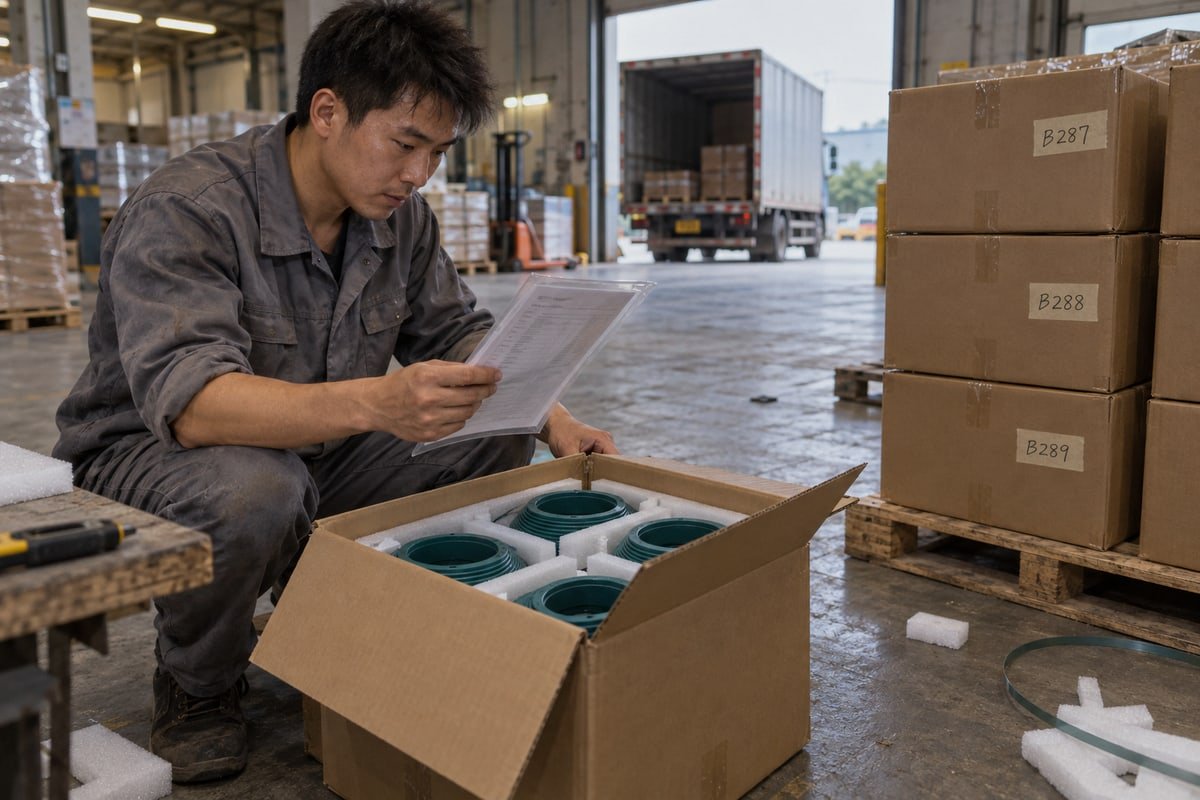
Long projects create a documentation problem that short projects never see. People change. Drawing revisions change. Sometimes the auditor changes. The only defense is a documentation package that repeats itself, lot after lot, without depending on anyone's memory.
Split the documents into once-only and every-lot
We divide project documentation into two groups. The first group is issued once at qualification. The second group ships with every batch.
| Document | Frequency | Purpose in a staggered project |
|---|---|---|
| Type test reports: A-0/A-60 fire rating, IP68, watertight and gas-tight 0.01–0.4 MPa | Once at qualification, reissued only if the spec changes | Proves the design performs, referenced by every later lot |
| Factory approvals: ISO 9001, IATF 16949, BV factory approval | Once, renewed on expiry | Confirms the system behind every lot is the same |
| Certificate of conformity with batch numbers | Every lot | Ties the delivered parts to the qualified design |
| Material declaration for halogen-free EPDM | Per compound batch | Supports fire and environmental compliance checks |
| Packing list keyed to E-House unit number | Every lot | Prevents mixing parts between orders |
| Drawing revision record | Whenever a penetration drawing changes | Shows which lots were made to which revision |
Freeze the specification and control every change
The frame contract should name the exact module models, frame drawings, and test reports that apply. After that, any change goes through written change control with a new revision number. We do this internally as well. Our production runs across sites in Shaanxi, Shandong, and Hunan, and all of them work under the same controlled documents. A module from any site carries the same batch traceability.
For project milestone tracking, we log each release date, batch number, and unit number in one shared file with the buyer. Some buyers add IoT tracking on frames in transit to get live arrival estimates. That is useful for rescheduling crews. It does not replace the paper trail. When the final auditor arrives, the file that answers every question is the one that links each installed frame to its lot, its revision, and its original type test.
Conclusion
Staggered deliveries protect your critical path only when planned as one integrated schedule. Match batches to build stages, buffer wisely, validate samples early, and lock documentation to every lot.
Footnotes
1. U.S. government resource for international trade, supply chain management, and logistics best practices. ↩︎
2. Explanation of 4D Building Information Modeling which integrates time-related data into project schedules. ↩︎
3. Technical overview of multi-cable transit systems used for sealing cable penetrations in industrial environments. ↩︎
4. International Maritime Organization standards defining fire-rated divisions such as A-60 for structural safety. ↩︎
5. Official site for ISO standards governing technical specifications and quality management in manufacturing. ↩︎



 English
 Español de México
 Deutsch
 Français
 العربية
 Русский