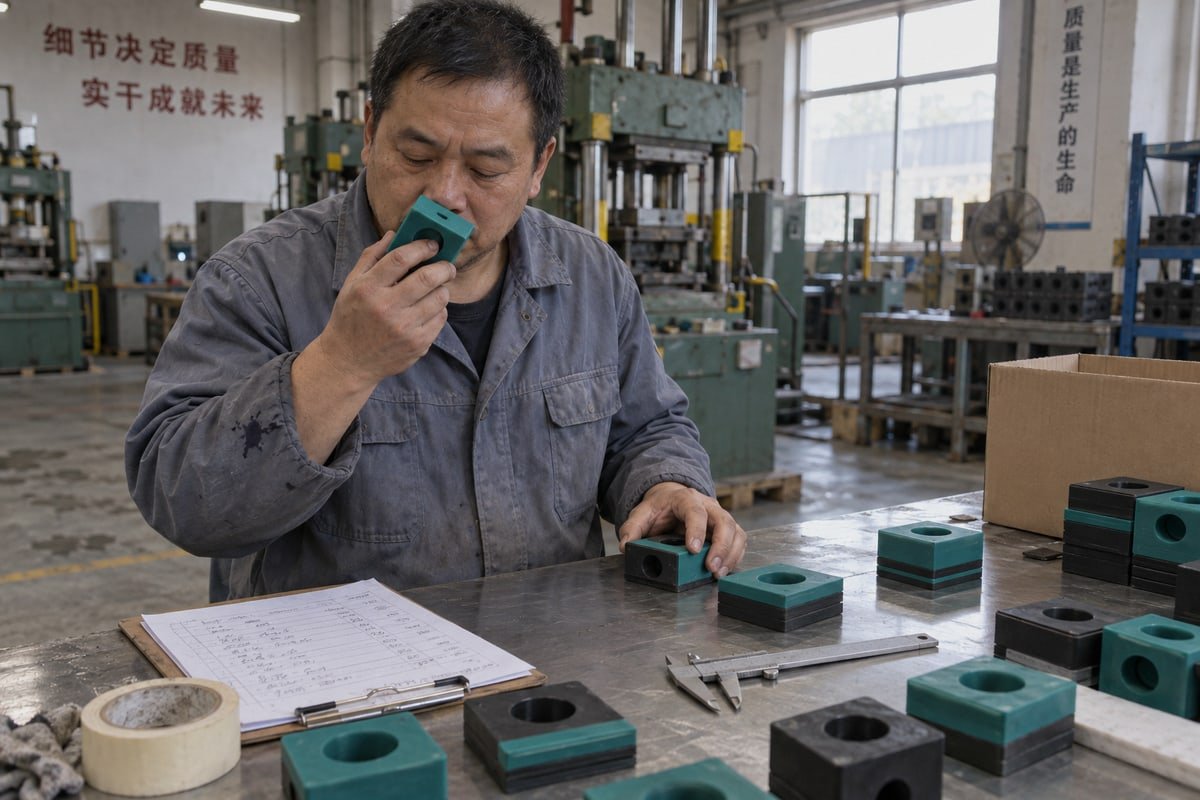
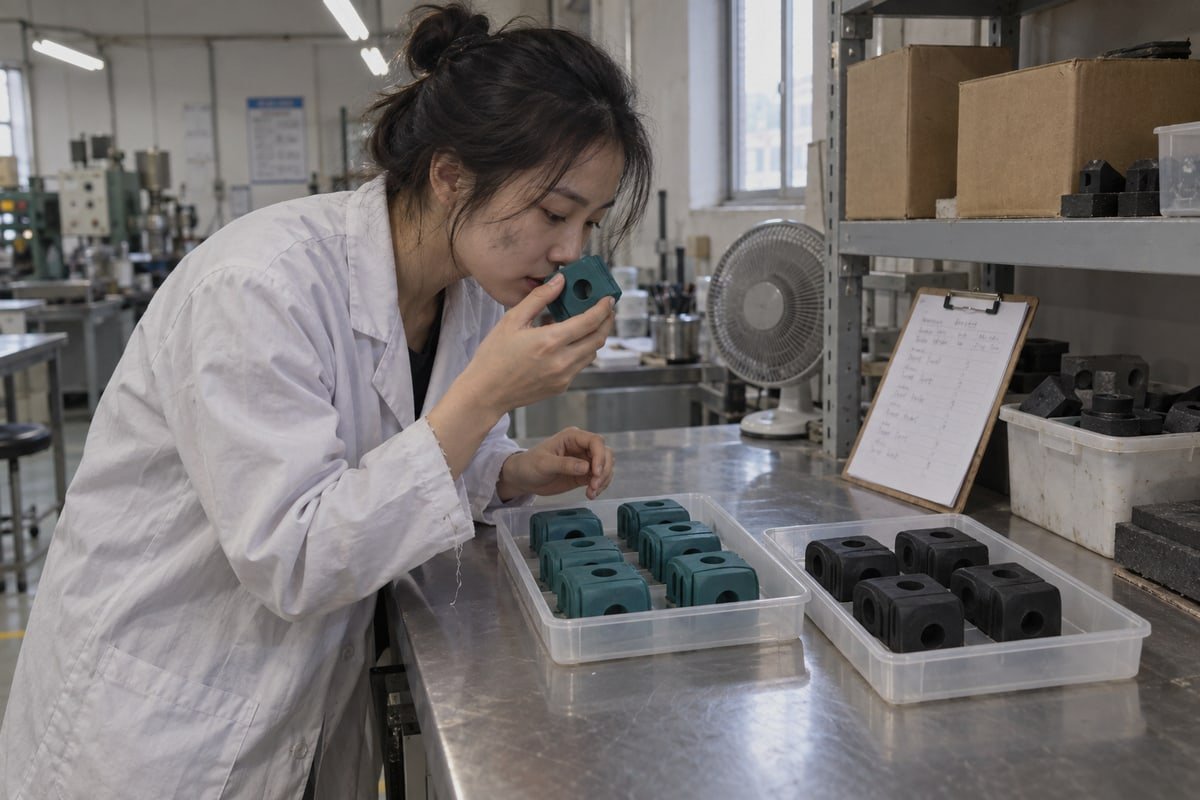
A module that looks fine can still leak, and site rework is costly IATF 16949 1. Our QC bench screens multi cable transit rubber module quality by eye, nose, and hand first.
Качество резиновых модулей для многокабельных проходок можно проверить, обратив внимание на гладкую, однородную поверхность с минимальным облоем, нейтральный резиновый запах без химических или горелых нот, а также упругое, эластичное ощущение с быстрым восстановлением после сжатия. Эти сенсорные проверки выявляют очевидные дефекты; сертификаты испытаний подтверждают соответствие.
This guide walks through each of the three senses in order. I will show you what to look for, what to smell for, and what to feel for. Then I will explain where these checks stop and where test documents must take over.
Какие Визуальные Признаки Говорят Мне, Если Резиновый Модуль Был Отлит и Отвержден Правильно?
Last year a batch of teal TSC modules came off a Shandong press with faint pigment streaks. We scrapped it, and that decision shaped our incoming inspection sheet.
Правильно отформованный и отвержденный резиновый модуль демонстрирует гладкую, однородную поверхность, тонкие и чистые линии разъема формы, равномерный цвет без полос или пятен, острые края и точные размеры. Пустоты, пузыри, меление, деформация или отсутствующий ступенчатый стержень — все это сигнализирует о проблемах формования или отверждения.
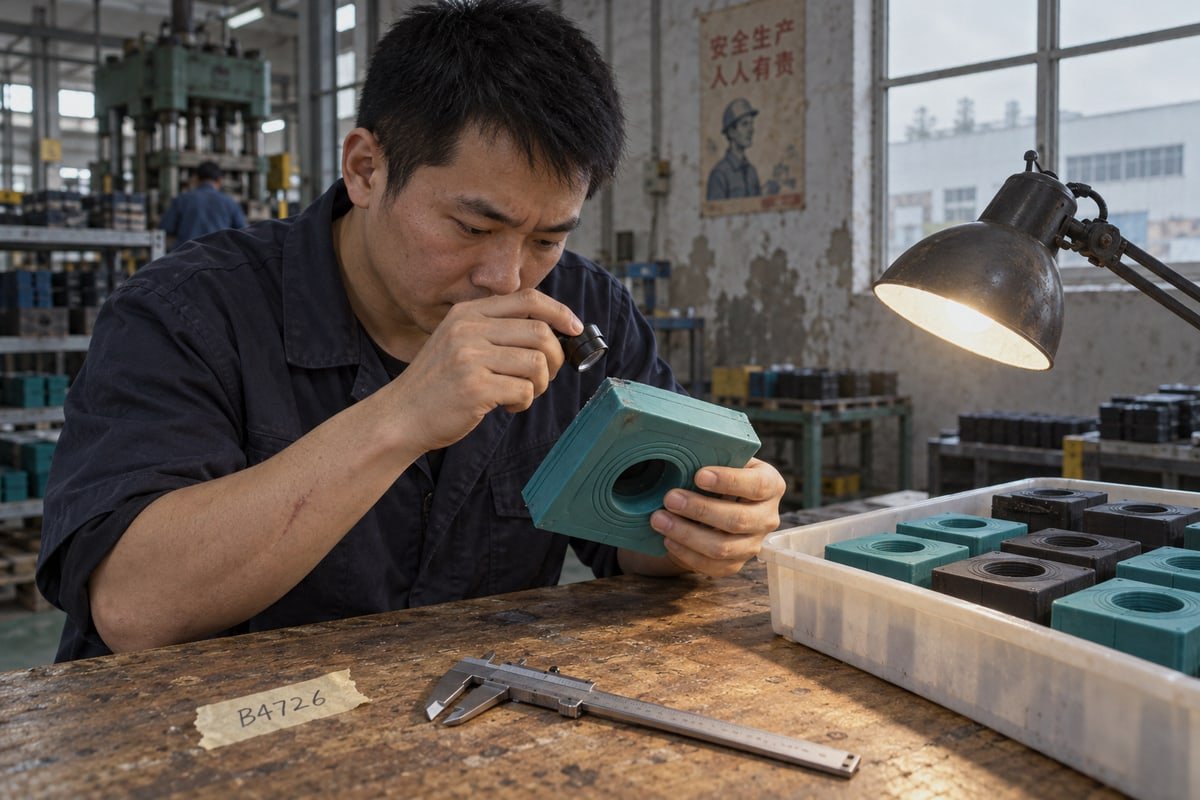
Your eyes are the fastest tool you have. A cable penetration seal works by compressing rubber against a cable jacket 2 and against its neighbors. Any surface flaw becomes a possible leak path under that compression. So I train our inspectors to slow down and look at four things.
Surface finish quality
Hold the module under good light. The surface should be matte and even. Look for small pits, voids, or "clinker" particles sitting on the skin. These often come from contaminated compound or trapped air during molding. A sunken area on a flat face usually points to under-filling or a short cure. Both create micro-gaps when the module is squeezed in the frame.
Flash and seam precision
Now check the mold parting lines. On a well-maintained mold, flash is almost invisible. Thick or jagged seams tell you the mold halves no longer meet cleanly. Worn molds also drift in size. Because our TSC modules must drop into standard 120-frame cutouts, dimensional accuracy is not optional for us. We keep mold making in-house partly so we can retire worn tools before flash grows.
Color uniformity
Color matters more than it looks. Streaks or blotched pigment can mean poor mixing. If the pigment did not disperse, the flame retardant additives 3 may not have either. That can affect the fire resistance rating in ways you cannot see. Color also carries information. Many systems use color to mark module size or type, so a module that is the wrong shade may simply be the wrong part.
Signs of aging
Finally, look for chalking, fading, or fine surface cracks. Good EPDM rubber properties include strong resistance to ozone and UV, so visible aging on a new module is a red flag for the compound itself.
| Visual sign | Likely cause | Risk to the seal |
|---|---|---|
| Pits, voids, clinker on surface | Contaminated compound or trapped air | Micro-leakage paths under compression |
| Thick, jagged flash | Worn or misaligned mold | Poor fit in frame, uneven compression |
| Pigment streaks or blotches | Poor mixing of additives | Uneven flame retardant or UV stabilizer content |
| Warping or sunken faces | Short cure or under-filling | Gaps between modules and stay plates |
| Chalking, cracks, fading | Aged or low-grade compound | Early loss of material elasticity |
| Missing or loose step core | Handling or molding error | Wrong cable diameter fit |
Почему Запах модуля EPDM имеет значение, и Чего мне следует остерегаться?
A sourcing engineer from Germany once opened our sample box and sniffed a TSR module before measuring anything. His reason was practical.
Запах модуля EPDM важен, потому что запах указывает на качество отверждения и чистоту компаунда. Правильно вулканизированный, безгалогенный EPDM имеет нейтральный или слабый резиновый запах. Остерегайтесь резких химических, горелых, кислых или маслянистых запахов, которые могут указывать на регенерированную резину, неполное отверждение или нестабильные пластификаторы.
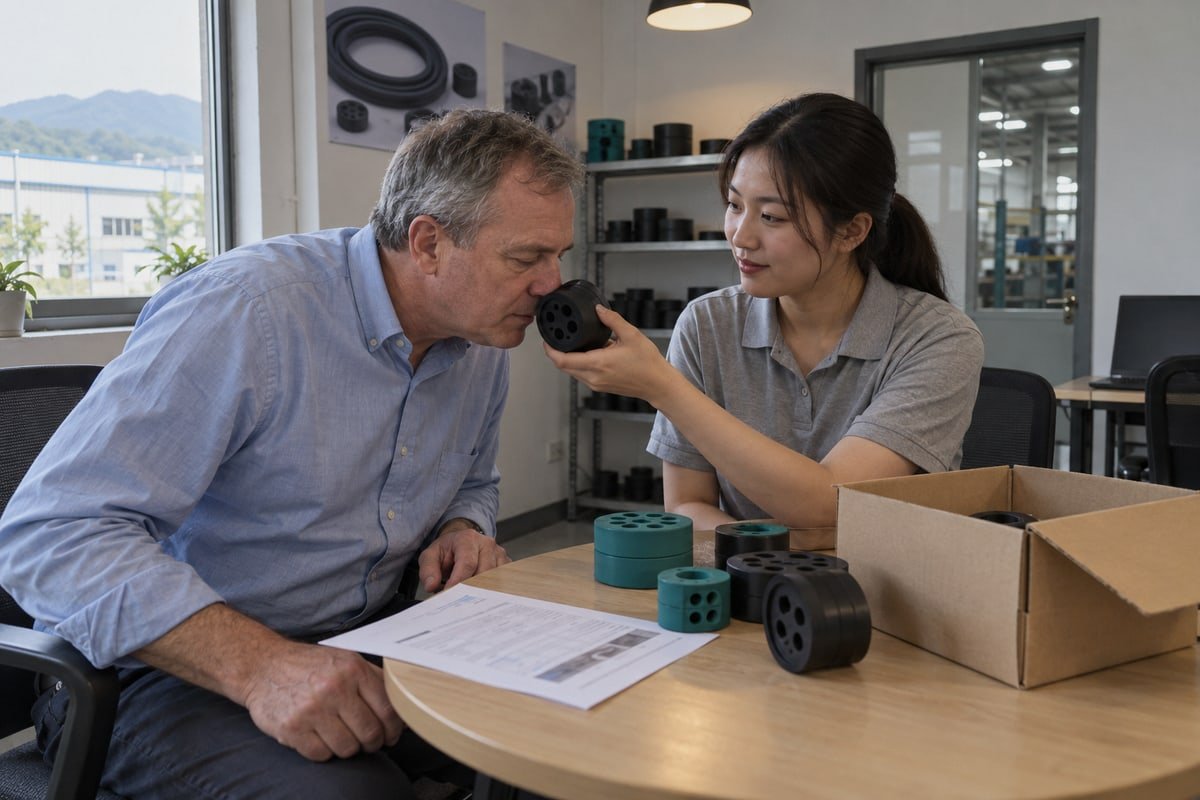
That engineer told me he had once received a shipment of sealing blocks that smelled like a tire fire. The lab later confirmed a high share of reclaimed rubber. He never skipped the sniff test again. I think his habit is sound, as long as you keep it in its place.
What different odors may suggest
Vulcanization is a chemical reaction. When it runs correctly, most volatile components are driven off or locked into the polymer network. What remains is a mild, clean rubber scent. When it runs badly, or when the compound is wrong, the nose often notices first.
| Odor type | What it may indicate | Suggested action |
|---|---|---|
| Neutral or faint rubber | Normal for cured, halogen-free EPDM | Proceed to visual and tactile checks |
| Pungent chemical | Excess volatile additives or incomplete cure | Isolate sample, request batch cure data |
| Burnt or acrid | Overheated cure or reclaimed rubber content | Isolate sample, request compound declaration |
| Sour or sharp | Contamination or unstable curing agents | Isolate sample, consider laboratory analysis |
| Oily or greasy | Plasticizer migration, low-cost fillers | Check surface for residue, request hardness data |
Why odor is a weak indicator on its own
Here is the objection I hear from careful buyers: odor is subjective, and it is not standardized. They are right. Dimensions, Shore A hardness, and compression set have test methods. Smell does not. Temperature, storage time, and even packaging change what you notice. A module fresh from a sealed carton smells stronger than one aired for a week.
So I treat smell as an early warning, not a decision tool. If a module smells off, we do not reject it on the spot. We tag it, pull it aside, and run the measurable checks. Then we compare it with the batch record. Halogen-free material matters for our customers in rail, marine, and BESS enclosures because of smoke toxicity in a fire. A strong chemical smell is worth a question, but the answer must come from a compound declaration and test report, not from anyone's nose.
Как Могу ли я Судить Эластичность Резины и Плотность Просто путем Прикосновения к модулю?
Every compound recipe forces a trade-off. Softer rubber seals more easily around cables, but it takes a set faster. We tune our step-core EPDM between those two limits.
Оцените эластичность и плотность резины, крепко ущипнув модуль и наблюдая за восстановлением. Качественный EPDM ощущается упругим, но гибким, мгновенно пружинит обратно, имеет постоянную твердость по всему блоку и не оставляет жирной пленки. Губчатые пятна, стойкие вмятины, жесткость или ощущение пластика указывают на наполнители или плохое отверждение.
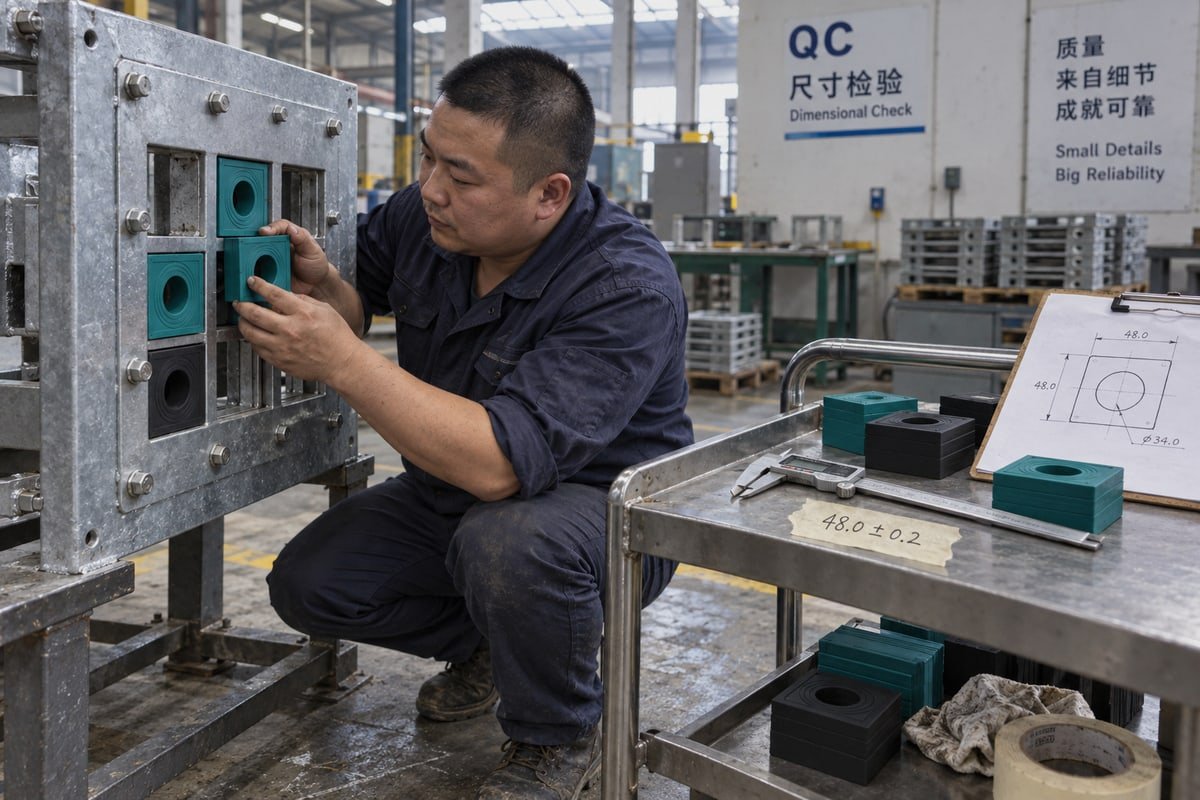
Touch tells you what the surface hides. Compression seal performance depends on the rubber pushing back evenly for years. A hand test cannot give you a number, but it can tell you when a number is worth chasing. I run five simple checks, in this order.
A five-step hand test
- Pinch and release. Squeeze a corner firmly between thumb and finger, hold for a few seconds, and let go. Good EPDM snaps back at once. A dent that lingers suggests high compression set, which means poor sealing memory over time.
- Press across the face. Move your thumb over the whole block. Hardness should feel the same everywhere. A soft or spongy spot often means an internal air pocket. Under a gas or water event, that pocket can collapse and open a path.
- Bend gently. Flex the module slightly. Listen and look. A cracking sound or a white stress line means the rubber is brittle or over-filled.
- Rub the surface. Your fingertips should feel a slight grip, not a slick or waxy slide. Grip helps the module lock against the cable jacket under vibration. A greasy film points to plasticizer leaching out.
- Peel a layer. On a step-core module, remove one adaptation layer. It should need a consistent, firm pull. Layers that fall off on their own, or layers that are fused, both show loose manufacturing tolerances.
Reading temperature and stiffness
Room temperature tells you more than you might expect. High-grade EPDM stays flexible in a cool workshop. If a module feels plastic-like or stiffens noticeably at ordinary indoor temperatures, the compound likely carries too much low-cost filler. On our own line we check Shore A hardness on every batch, but the hand test is how an inspector decides which module goes to the durometer first.
| Tactile cue | Good module | Suspect module |
|---|---|---|
| Recovery after pinch | Immediate, full | Slow or lasting dent |
| Hardness across block | Even | Spongy or hard spots |
| Bending | Silent, no whitening | Cracking or stress lines |
| Surface feel | Slightly grippy, dry | Slick, waxy, or oily |
| Layer peeling | Firm, consistent pull | Falls off or fused |
| Cool-room flexibility | Unchanged | Noticeably stiffer |
One more word on the trade-off I mentioned. Buyers sometimes assume the softest module seals best. It does not. A module that is too soft compresses unevenly, extrudes past the stay plates, and loses pressure faster. The target is a balance of material elasticity and firmness, and that balance is best confirmed by a hardness reading.
Can I Trust Appearance and Feel Alone, or Should I Also Ask for Test Certificates?
The lesson that stuck with me came from a BESS container builder. Their team approved our free validation samples by hand, then still requested the IP68 report. They were right.
Appearance and feel alone cannot be trusted for a final decision. They screen out obvious defects, but only measurable checks prove performance. Always ask for fire rating, IP68, water and gas tightness test documents, Shore A hardness records, and dimensional reports before qualifying a cable transit module supplier.
Here is the honest limit of everything above. A module can pass every sensory check and still fail under pressure, in a fire, or after five years offshore. Official inspection checklists know this. They lead with measurable items: correct number and size of modules, secure seating in the frame, full compression, no visible gaps, and correct lubrication. Sensory judgment sits behind those items, not in front of them.
Sensory screening versus measurable proof
| Вопрос | Sensory check can answer | Requires test document or measurement |
|---|---|---|
| Is the surface free of voids and flash? | Да | Optional dimensional report |
| Is the compound fully cured? | Hint only (smell, feel) | Cure record, Shore A hardness |
| Will it hold water and gas pressure? | Нет | Water tightness testing, gas tightness to stated MPa |
| Will it resist fire spread? | Нет | Fire resistance rating certificate |
| Is it halogen-free? | Нет | Compound declaration, test report |
| Does it fit a 120-frame cutout? | Rough visual only | Dimensional accuracy report, CAD/STEP file |
Two installation checks that back up the hand test
Two field checks bridge the gap. First, after the compression unit is tightened, no light should pass through the transit. If you can see daylight, the seal is not complete no matter how good the rubber felt. Second, in many systems a small amount of lubricant pushed out at the edges is a sign of good compression, while a visible gap between modules is a sign of a problem.
What we hand over
On our side, we keep both layers of evidence. Our factory runs ИСО 9001 4 and IATF 16949 systems and is BV-approved. Our modules are tested for A-0 and A-60 fire rating, Защита от проникновения IP68 5, and watertight and gas-tight sealing from 0.01 to 0.4 MPa. When a European integrator qualifies us as a second source, we send free validation samples for the hand test, a cross-reference table from their existing model to the DEWIN model, and the test documents on request. The sample answers "does it look and feel right?" The documents answer "does it perform?" You need both, and you should never accept one in place of the other.
Заключение
Bad modules cause leaks and rework. Screen with eyes, nose, and hands first, then demand test documents. Our validation samples and certificates give you both.
Сноски
1. Official oversight body for the automotive quality management standard IATF 16949. ↩︎
2. General technical information regarding cable construction and the function of the outer jacket. ↩︎
3. Technical overview of flame retardant additives and their role in material fire resistance. ↩︎
4. Official landing page for the ISO 9001 quality management standard mentioned in the text. ↩︎
5. Official body for international standards regarding IP ratings and ingress protection. ↩︎
 English
 Español de México
 Deutsch
 Français
 العربية
 Русский