A buyer once asked our QC team which quality inspection reports for multi cable transit orders actually matter. Thin paperwork hides boundary failures. Here is the full dossier we recommend.
Suppliers should provide a traceable inspection package for multi cable transit orders: ISO 9001 and IATF 16949 certificates, a Certificate of Compliance, Mill Test Certificates, dimensional and visual inspection reports, fire resistance and IP68 test reports, hydrostatic and gas-tight pressure test records, batch traceability logs, and a final release.
That list looks long. It is not. Each item answers one buyer question. The four sections below walk through those questions in the order a sourcing engineer usually asks them.
Which certifications should I request to confirm ISO 9001 and IATF 16949 compliance before placing an order?
During a customer audit at our Shaanxi plant, the visiting engineer spent more time checking certificate dates and scopes than watching the presses run. That visit taught me something.
Request current ISO 9001 and IATF 16949 certificates showing the certification body, certificate number, expiry date, and a scope that names cable transit or sealing module manufacturing. Add a Certificate of Compliance for your order and, for marine work, a BV, DNV GL, or Lloyd's Register factory approval.
A certificate is only useful if it is real, current, and relevant. So I always tell buyers to check three things before they read anything else.
Check the scope, not just the logo
Many factories hold an ISO 9001 certificate 1 for a different product line. The scope text matters. It should name sealing modules, cable transit frames, or penetration sealing systems. Our own certificates cover the TSR round assemblies and TSC square modules we make, and we send the scope page with every quotation. IATF 16949 is an automotive-grade system. It adds process control, measurement system analysis 2, and stronger batch control on top of ISO 9001. For BESS container builders and switchgear OEMs, that extra layer is what keeps rubber hardness and compression stable from lot to lot.
Ask for the full document set
| Document | What it proves | Who issues it |
|---|---|---|
| ISO 9001 certificate | A working quality management system | Accredited certification body |
| IATF 16949 certificate | Automotive-level process and batch control | IATF-recognized body |
| Factory approval (BV, DNV GL, Lloyd's Register) | The plant is recognized for marine-grade production | Classification society |
| Certificate of Compliance | The shipped order matches the agreed spec | Supplier QA manager |
| Mill Test Certificate | Steel grade and chemistry of the frame | Steel mill or supplier lab |
| REACH/RoHS declaration | Halogen-free EPDM is chemically compliant | Supplier or compound maker |
One buyer objection comes up often. "The product is standardized and type-tested, so a short Certificate of Compliance is enough." For a low-risk spare module order, I partly agree. But a Certificate of Compliance only says the supplier believes the product conforms. It does not show who audited the factory or when. Our plant is BV-approved, and we still attach the ISO 9001 and IATF 16949 pages to first orders. It costs us nothing and saves the buyer a qualification round.
Verify online, then file it
Every accredited certificate has a number you can check on the certification body's website. Do it. Then file the document with the expiry date in your supplier record. A lapsed certificate on a critical fire boundary is an audit finding waiting to happen.
How do I verify fire rating and IP68 test results match my project's technical specifications?
Every time we quote an A-60 configuration, I weigh the same trade-off: send the buyer the full fire resistance test 3 report, or just the one-page summary.
Compare the test report against your spec line by line: fire class (A-0 or A-60), division type, tested module and frame configuration, cable fill, IP68 immersion depth and duration, test standard, lab name, test date, and report number. Any mismatch means the result does not cover your installation.
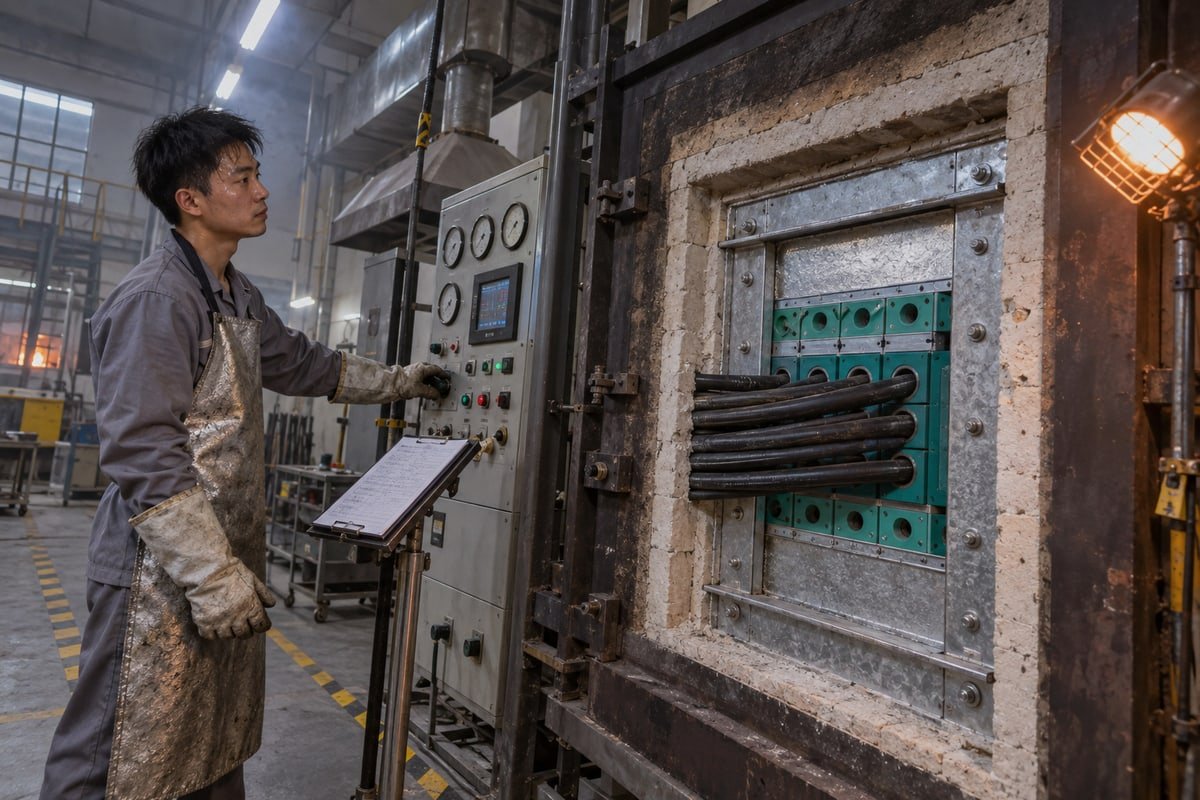
I now send the full report every time. The summary is what causes trouble. A summary says "A-60, IP68." The full report says which frame, which modules, which cable fill, and which side the fire was applied to. Those details decide whether the result covers your job.
Read the fire resistance test report like an inspector
An A-0 or A-60 class result belongs to one tested assembly. Frame size, stay plate arrangement, module count, spare capacity, and cable type are all part of it. If your as-built drawing differs, ask the supplier which test covers the change. IMO-related guidance also notes that when several transits are tested together in one division, spacing between them is controlled. So a single test may cover multiple frame sizes, but the report must say so.
Naval buyers should watch one more trend. NAVSEA is developing updated qualification requirements for multi cable transits 4 under MIL-DTL-24705. Vibration and medium-weight shock are now placed before the fire resistance test for QPL products. That means a transit must survive mechanical abuse first and then hold the fire boundary. If you sell into defense or offshore, ask whether the supplier's fire test included a mechanical pre-conditioning step.
Match the IP68 report to your exposure
| Report item | What your spec says | What the report must show |
|---|---|---|
| IP class | IP66, IP67, or IP68 | Same class, same test standard |
| Immersion depth and time | e.g. 1 m for 30 min, or deeper | Actual depth and duration used |
| Configuration | Frame type, module sizes, fill | Identical or bounded configuration |
| Test lab and date | Third-party preferred | Lab name, accreditation, report number |
| Halogen-free rubber | Required for enclosed spaces | Material declaration for the EPDM |
IP66/67 rating documentation is not the same as IP68. IP66 covers water jets. IP67 covers short immersion. IP68 covers longer immersion at a stated depth. Our TSC and TSR modules are tested to IP68, and we share the report with the exact test conditions so the buyer's engineer can compare them with the site's flood risk.
Do not forget the secondary tests
Some projects need more. Data center builders sometimes ask for EMC shielding effectiveness. Submarine and architectural projects ask for acoustic attenuation results. Hazardous-area switchgear may require ATEX certification for the enclosure the transit sits in. Ask early. These tests are configuration-specific and take time.
What documentation proves watertight and gas-tight sealing performance at my required pressure range?
A BESS container builder in the Middle East emailed me a single line: 'Prove 0.3 MPa.' No drawing, no configuration. We answered with a hydrostatic test record and a question.
Ask for a hydrostatic pressure test report and a gas-tight leak test report that state the exact frame, module, and cable configuration, the test medium, the applied pressure within your range (for example 0.01–0.4 MPa), hold time, leakage criteria, result, test date, and the inspector's signature.
The question we sent back was simple: "Which side is pressurized, and what is the cable fill?" Pressure performance depends on both. A transit that holds 0.4 MPa from the water side with a full module stack may behave differently with spare blank modules or a half-empty frame. So the report must describe the tested assembly, not just the number.
What a good pressure test record contains
Our factory tests watertight and gas-tight sealing across 0.01 to 0.4 MPa. The record we issue lists the items below, and I suggest you demand the same from any supplier.
- Frame model, stay plate count, and module sizes, with a drawing reference and revision.
- Cable diameters and fill pattern, including any spare or blank modules.
- Test medium, either water for hydrostatic pressure testing or air or nitrogen for gas-tight testing.
- Applied pressure, ramp method, and hold time.
- Acceptance criterion, such as no visible leakage or a maximum pressure drop.
- Result, date, inspector name, and signature.
Type test versus batch test versus installed test
| Test level | When it happens | What it proves | Typical document |
|---|---|---|---|
| Type test | Once per design | The design can reach the rated pressure | Third-party test report |
| Factory Acceptance Test | Per order or batch | The delivered units match the type | FAT record with serials |
| Installed-condition test | After cable installation | The seal works as built on site | Site air test report and register entry |
Here is the second buyer objection I hear. "Self-certification is fine if the manufacturer is qualified." For repeat spare orders, yes. For a first order on a critical pressure boundary, I recommend a witnessed Factory Acceptance Test, either by your engineer or a third party. We host these at our Shaanxi, Shandong, and Hunan plants and send video when travel is not practical.
Factory proof is not installation proof
A transit can leave the factory compliant and still leak on site. Naval standard items call for a local air hose test on new and disturbed multi cable transits after cable installation, with a light test allowed for non-structural assemblies. That is why we include compression wedge inspection and torque records in our installation guidance. The compression unit must be tightened to the specified value. If the installer under-torques it, no factory report will save the seal. Ask your supplier for the torque value in writing and record it on the installation checklist.
Can I request batch-specific inspection reports and free validation samples before committing to full production?
Years ago I learned that a free validation sample earns trust faster than any brochure. Since then, every qualification request from our factory starts with samples and a batch report.
Yes. A serious supplier will issue batch-specific inspection reports tied to lot numbers, production dates, and material certificates, and will ship free validation samples with a model cross-reference so you can fit-check them in your existing 120-frame cutouts before committing to full production.
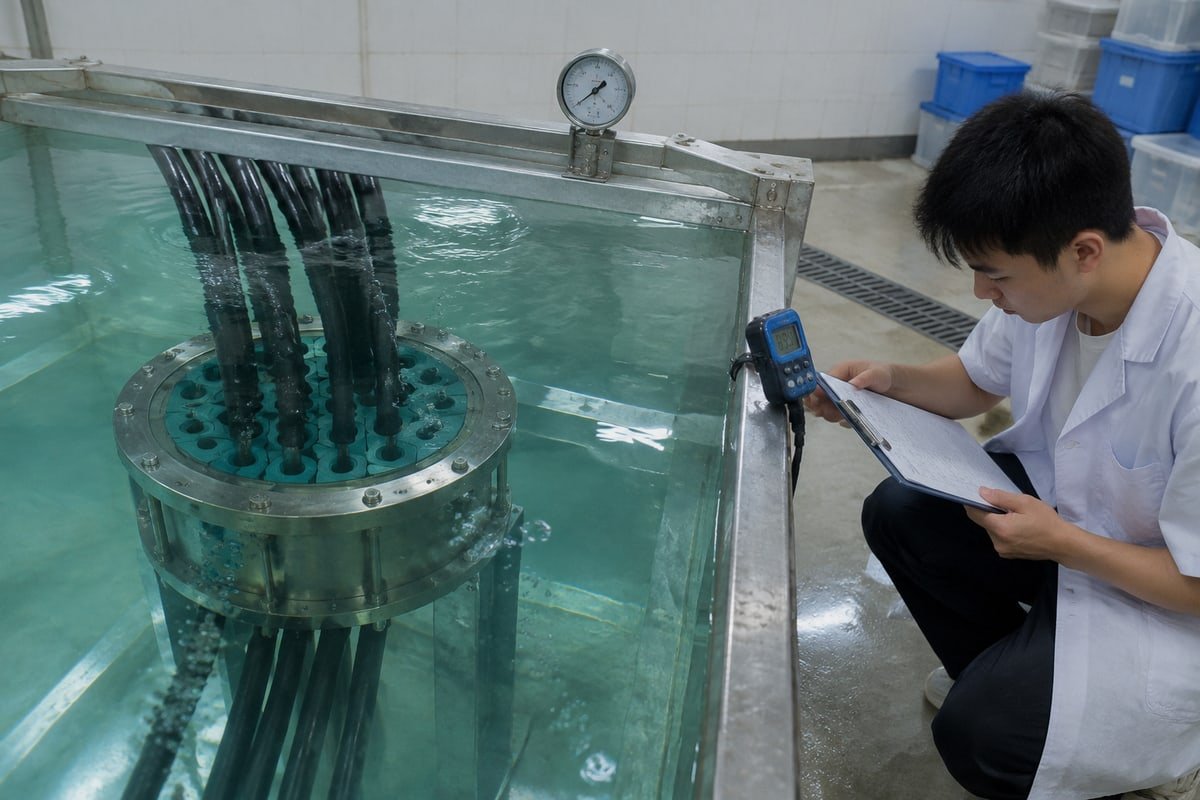
Batch reports matter because rubber is a natural material. EPDM hardness, compression set, and dimensions drift if the mix or cure changes. A type test from three years ago does not tell you what came out of the press last week. Our step-core, halogen-free EPDM modules 5 are dimensionally compatible with common 120-frame standards, so the batch report is also your proof that the drop-in replacement really drops in.
What we put in a batch-specific inspection report
The package we issue against each production lot contains these items, and I would ask any second source for the same.
- Product identification: model, size, quantity, project reference, and the buyer's original part number from the cross-reference table.
- Lot and traceability data: batch number, molding date, rubber compound lot, and steel heat number on the frame.
- Material Traceability Report linking the Mill Test Certificate for the frame and the compound certificate for the rubber.
- Dimensional inspection report: module height, width, core diameter range, and frame cutout dimensions against drawing tolerances.
- Visual inspection report: no surface cracks in the rubber, no voids, no weld irregularities on the frame, correct marking on the nameplate.
- Nonconformance log: any defects found, corrective action, retest evidence, and final disposition.
- Signed final release from QA.
Some buyers now ask for a QR code on each module that links to this record. We support this for private-label orders, and it gives the maintenance team a digital history from production to installation.
How the validation loop works
- Send us your existing frame drawing or module part number.
- We return the DEWIN equivalent from the cross-reference table, plus CAD or STEP files.
- We ship free validation samples with the batch report for that lot.
- Your engineer fit-checks the samples in an existing frame and runs a pressure or torque check.
- You approve, and the first production order ships with a matching Factory Acceptance Test record.
The last objection is about speed. "All this paperwork slows the project." It does not have to. We keep the batch report as a standard template, so it adds no lead time. For low-risk spare orders, the Certificate of Compliance plus the dimensional inspection report is usually enough. For fire or pressure boundaries, the full dossier is worth the extra pages. With 38 granted patents and in-house mold making since 2013, we can also produce custom sizes and document them the same way.
Conclusion
Thin paperwork hides boundary failures. Demand the full dossier: certificates, fire and IP68 reports, pressure test records, batch traceability, and free samples. Then qualify your second source with confidence.
Footnotes
1. Official ISO page explaining the requirements and scope of the ISO 9001 quality management standard. ↩︎
2. IATF 16949 requires specific quality tools like measurement system analysis for automotive-grade production. ↩︎
3. The IMO provides the regulatory framework for fire resistance testing in the maritime industry. ↩︎
4. Technical overview of multi-cable transit systems used for sealing cable penetrations in high-risk environments. ↩︎
5. REACH regulations ensure that materials like EPDM used in cable transits are free from hazardous chemicals. ↩︎



 English
 Español de México
 Deutsch
 Français
 العربية
 Русский