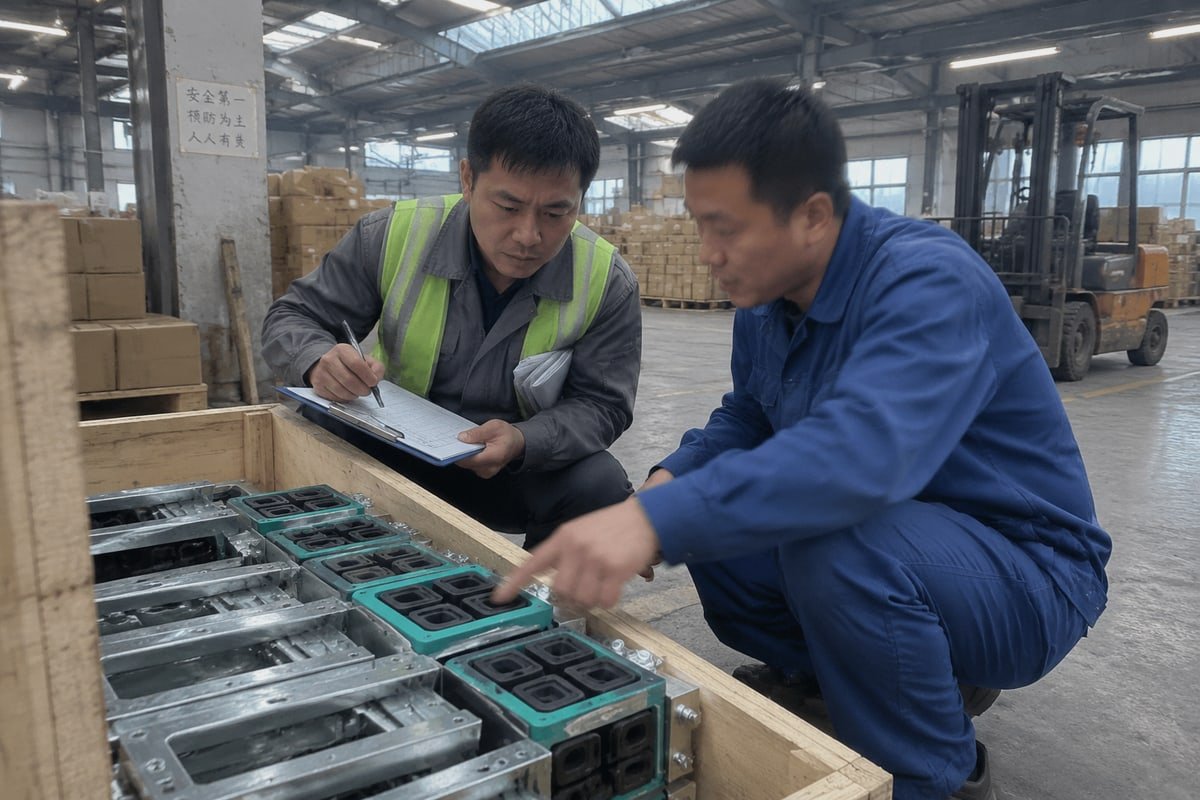
A blocked container of MCT modules at port ruins a project schedule. On our production line, third-party inspection before shipping multi cable transit products is the gate that prevents this.
Arrange third-party inspection before shipping multi cable transit products by appointing an independent verification agency, agreeing an Inspection and Test Plan with hold points, preparing certificates and traceability records, scheduling the visit after final QC but before crating, and releasing goods only on a signed Inspection Release Note.
That sounds simple. In practice, each step has details that decide whether the shipment clears on the first visit. I will walk through the four questions our buyers ask most often, in the order they come up.
How do I choose a qualified third-party inspection agency for MCT cable transit products?
A sourcing manager in Germany asked us which inspector we preferred. Our answer was none; we told him to pick the agency his classification society 1 or end client already trusts.
Choose an inspection agency that is accredited to ISO/IEC 17020, has inspectors experienced with marine or industrial cable transit systems, is recognized by your project's classification society, operates near the factory in China, and can issue an Inspection Release Note in English within agreed timelines.
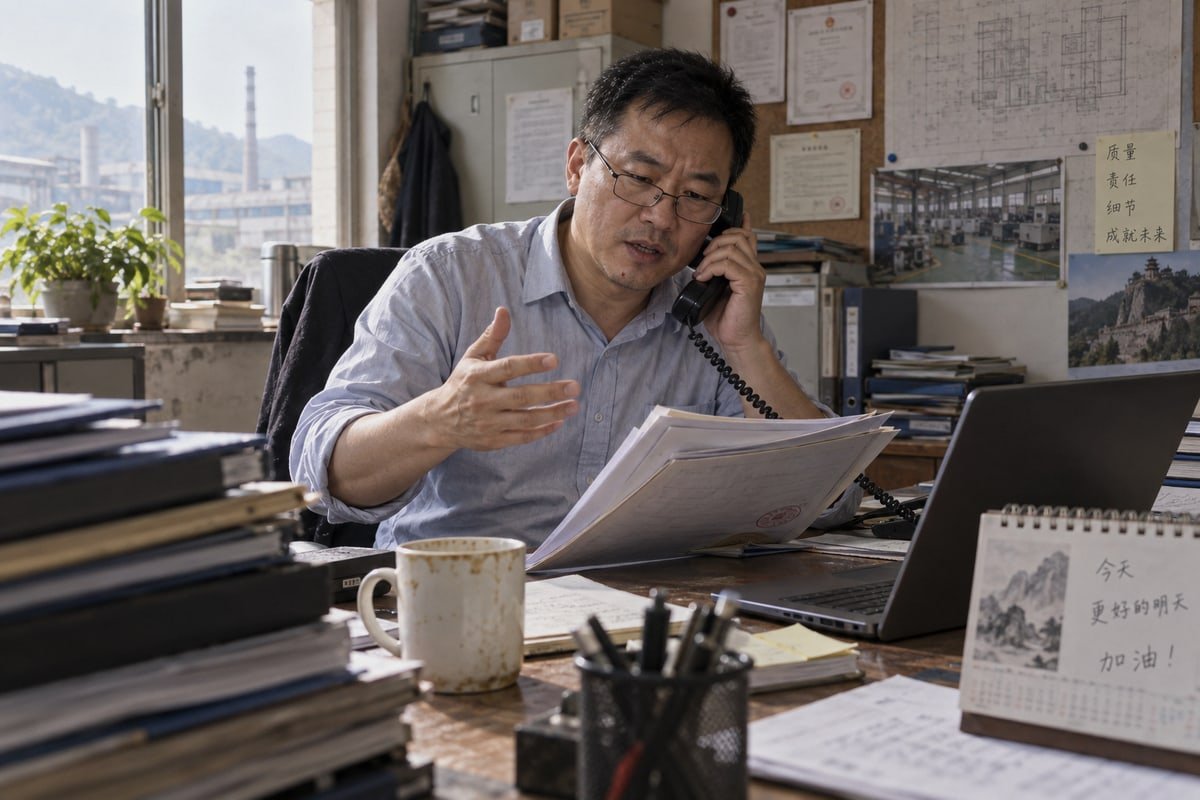
The agency you appoint shapes the whole pre-shipment inspection (PSI). A generalist inspector will count cartons and check labels. A specialist will open a TSC module, measure the step-core layers, and ask for the EPDM batch certificate. You want the second type.
Three types of independent verification agency
| Agency type | Typical names | Best fit | Watch out for |
|---|---|---|---|
| Global TIC firm | SGS, Intertek, TÜV, Bureau Veritas | Most industrial and BESS/data center orders | Confirm the assigned inspector knows cable transits, not just general goods |
| Classification society surveyor | DNV, ABS, Lloyd's Register, BV Marine | Marine, offshore, and SOLAS-governed projects | Longer booking lead time; scope tied to class rules |
| Regional independent inspector | Local agencies in Shaanxi or Shandong | Repeat orders, spare module lots, low-risk projects | Check accreditation and independence from the supplier |
What to verify before signing the service agreement
I suggest four checks. First, ask for the ISO/IEC 17020 accreditation certificate 2. This is the standard for inspection bodies. Second, ask for a sample report on a similar product. Look for photos, measured values, and a clear pass/fail table. Third, ask who pays the agency. Even if the supplier settles the invoice, the buyer must nominate and instruct the inspector. Fourth, confirm the agency can reach our plants in Shaanxi, Shandong, or Hunan without a two-day travel premium.
Buyer objection: is an agency worth the cost on a routine order?
Some suppliers argue that inspection adds cost and delay to routine orders. I understand the point. But one rejected lot of frames means air freight for replacements, site idle time, and a claim discussion. That cost is far higher than an inspector's day rate. Our position is practical: use a specialist agency for first articles and classed projects, and a regional inspector for repeat spare-part lots.
What inspection standards and certifications should I verify before scheduling a factory audit?
Every certificate we file costs engineering time, so we weigh which documents actually decide acceptance. For MCT frames and modules, the fire, ingress, and hazardous-area papers decide it.
Before a factory audit, verify ISO 9001 and IATF 16949 quality system certificates, classification society type approval such as BV, DNV, ABS, or Lloyd's Register, fire ratings A-0/A-60 under SOLAS fire safety standards, IP68 ingress protection, and ATEX/IECEx or MED marks where the application requires them.
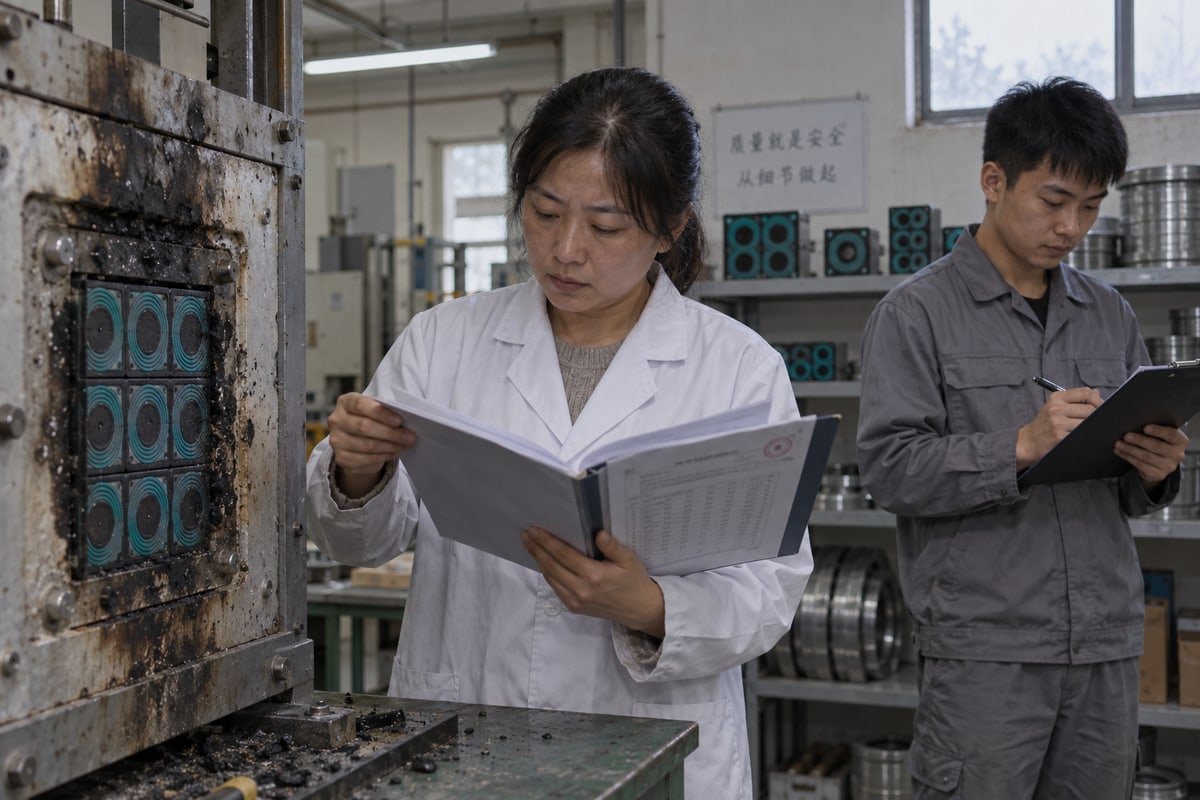
Inspectors spend as much time on paper as on steel. This is not bureaucracy. An MCT system carries performance claims that cannot be seen by eye. A teal EPDM block looks the same whether it passed a 60-minute fire test or not. The document is the proof.
Quality system certificates versus product approvals
These are two different things, and buyers often mix them. ISO 9001 and IATF 16949 3 tell you the factory runs a controlled process. Our BV-approved factory status tells you a classification society has audited that process. Neither one says a specific module is fire rated. That comes from type approval and test reports for the product itself. Ask for both layers.
Building the manufacturer's data book
| Document | What it proves | What the inspector checks |
|---|---|---|
| ISO 9001 / IATF 16949 certificates | Controlled quality management system | Validity date, scope covers cable transit products |
| Classification society certification (BV, DNV, ABS, LR) | Design accepted for marine or industrial class use | Certificate number matches product family and frame size |
| Fire test report A-0 / A-60 | Bulkhead and deck fire integrity per SOLAS fire safety standards | Tested configuration matches the shipped frame and module type |
| IP68 and gas-tight test report | Sealing performance, 0.01–0.4 MPa | Test pressure equals or exceeds project specification |
| Material traceability reports (MTRs) | Steel grade of frames and stay plates | Heat numbers match frame stampings |
| Galvanization certificate | Coating thickness and process | Values match drawing requirement |
| EPDM material certificate | Halogen-free rubber composition and hardness | Batch number matches module markings |
Hazardous-area marks are application-specific
ATEX, IECEx, and MED marks matter when the transit sits in an explosive atmosphere 4 or on a vessel under EU marine equipment rules. They do not apply to every BESS container or switchgear cabinet. Put the requirement in the purchase order only when the site needs it. Otherwise the inspector will hunt for a document that was never part of the contract, and the visit stalls.
Which technical checks and test reports should I request during pre-shipment inspection?
Last quarter our QC team rejected a batch of TSC modules because the step-core layers showed flash on the parting line. The inspector never saw them, which is the point.
Request dimensional checks of frames, stay plates, and rubber modules against approved drawings, visual checks for weld defects and elastomer damage, rubber hardness verification, witnessed fire and water tightness testing or gas pressure tests to the specified IP rating, material traceability records, marking review, and packaging verification.
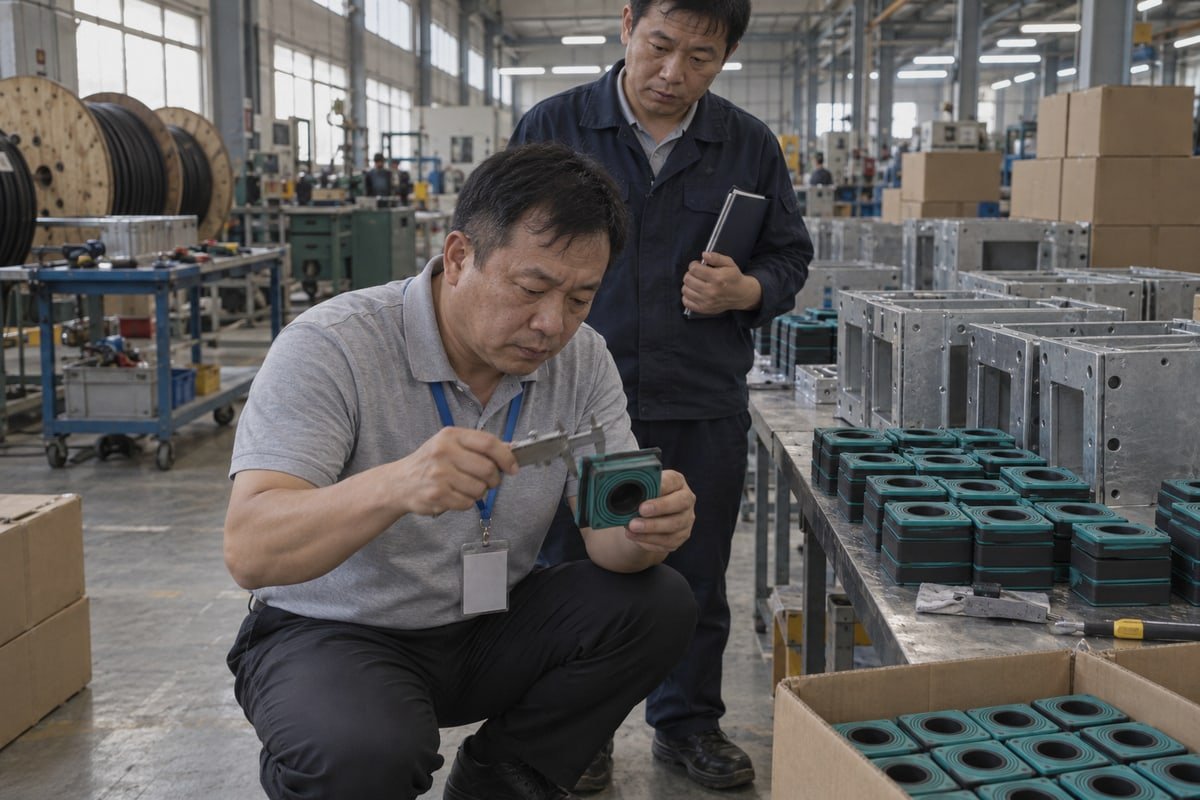
The strongest tool here is a written Quality Control (QC) checklist shared between buyer, supplier, and inspector before the visit. Without it, the inspector makes ad hoc decisions on the shop floor. With it, everyone knows what "pass" means.
A working QC checklist for MCT products
| Check item | Method | Acceptance reference |
|---|---|---|
| Frame outer and inner dimensions | Tape and caliper | Approved drawing, 120-frame cutout tolerance |
| Weld seams on frame corners | Visual and gauge | No cracks, porosity, or undercut |
| Stay plate thickness and flatness | Caliper, straight edge | Drawing tolerance |
| Rubber module size and step-core layers | Caliper, layer count | Drawing; layers intact and evenly peelable |
| EPDM hardness | Shore A durometer on sample | Material certificate value |
| Compression unit bolt torque function | Trial compression on one frame | Smooth travel, no thread damage |
| Marking and nameplate | Visual | Model, batch, fire rating readable |
| Quantity and accessory sets | Count against packing list | Zero shortage |
| Export crating | Visual, moisture check | Shipping marks, weights, destination correct |
Witnessed tests and the Factory Acceptance Test
For classed projects, buyers often combine the PSI with a Factory Acceptance Test (FAT). The inspector witnesses a sample frame being fitted with modules and cables, compressed, and pressure tested. We run gas-tight tests 5 within the 0.01–0.4 MPa range and water tightness tests to IP68 on request. Fire and water tightness testing at type-approval level is not repeated per lot; instead, the inspector confirms the lot matches the tested configuration.
Common failure points we see
Most rejections are not about rubber quality. They are about mismatches. A wrong module size for the cable range. A missing spare blank module. A nameplate with the wrong revision. Crates marked for the wrong port. These are cheap to prevent and expensive to fix after sealing.
Digital evidence is becoming standard
Buyers increasingly want photos with timestamps, not paper alone. Some projects now use QR codes on each module linking to its batch and test history. Remote inspection through live video is also used when travel is hard. We support these where the buyer requests them, but the physical hold point still comes first.
How do I schedule and coordinate inspection timing with my supplier to avoid shipping delays?
We learned early that booking the inspector for the day packing finishes is a mistake. One rescheduled visit can push a container onto the next sailing.
Schedule inspection by fixing the date in the purchase order, setting a hold point after final QC and before crating, giving the agency at least five working days' notice, confirming a staged sample area and document pack, and reserving one buffer week between release and the vessel cut-off.
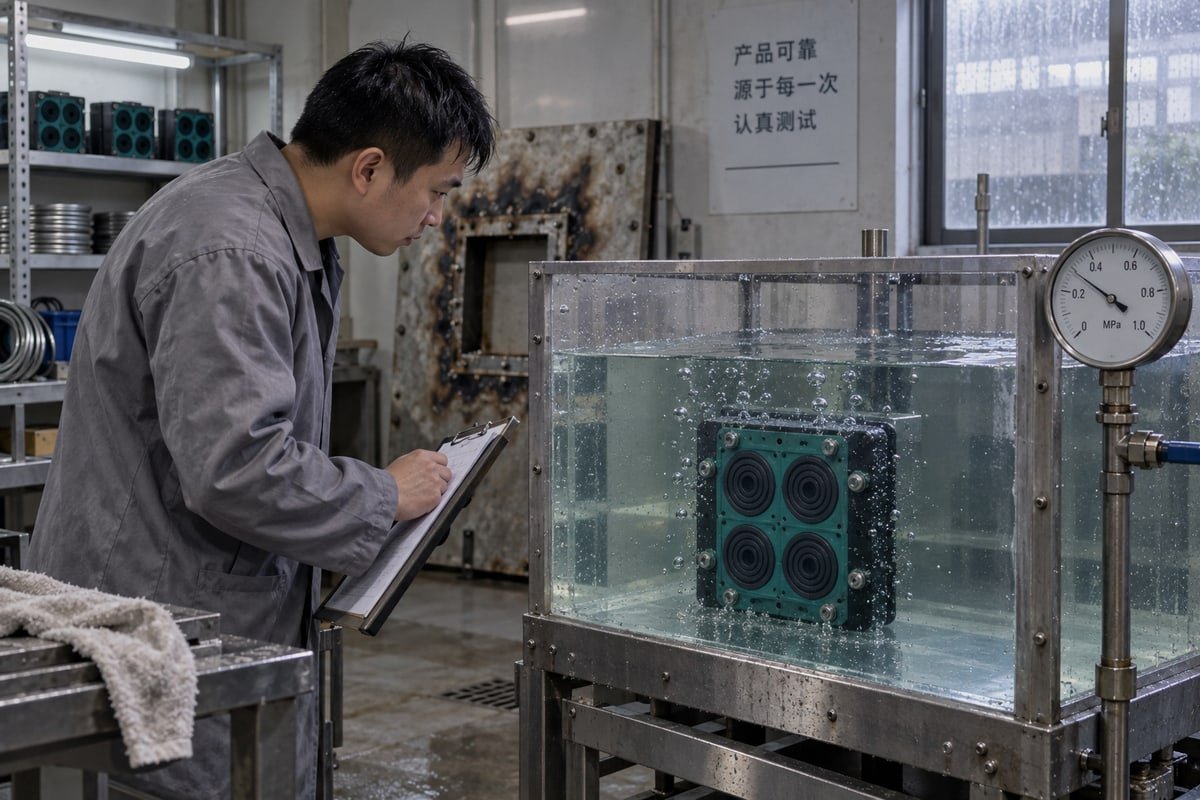
Timing is where most disputes start. Too early, and damage during packing is missed. Too late, and the crates are sealed and the truck is booked. The fix is to treat inspection as a planned hold point, not an event squeezed in at the end.
A step-by-step coordination process
- Write the Inspection and Test Plan (ITP) into the purchase order. Name the hold points and witness points.
- Agree the sampling level. Full count for quantity; sample for dimensions; one frame for witnessed pressure test.
- Our planning team sends a production readiness notice when final QC is complete.
- The buyer confirms the inspector's date. We stage samples, open cartons, and lay out the data book.
- The inspector visits, records findings, and lists any nonconformities.
- We close nonconformities and provide photo evidence. Re-inspection is agreed only for critical items.
- The agency issues the Inspection Release Note (IRN). Only then do we seal crates and book the container.
Timeline reference
| Milestone | Typical timing | Owner |
|---|---|---|
| ITP agreed | At order placement | Buyer and supplier |
| Readiness notice | After final internal QC | Supplier |
| Inspector booking | Five working days before visit | Buyer or supplier |
| Inspection visit | Before crating | Agency |
| Nonconformity closure | Within days, with photos | Supplier |
| IRN issued | After closure | Agency |
| Crating and booking | After IRN | Supplier and forwarder |
| Vessel cut-off | One week buffer after IRN | Forwarder |
Buyer objection: every shipment, or only critical ones?
Some buyers ask whether every order needs an inspector. Others insist on full inspection every time. Neither extreme fits. We recommend full PSI for first articles, new frame sizes, and any marine or classed project. For repeat spare module lots under an approved cross-reference, a document review plus photo report is often enough. Write the rule into the frame agreement so nobody debates it per order.
Export documentation compliance
The IRN is one document among several. The packing list, commercial invoice, certificate of origin, and material certificates must match each other and the goods. We handle export documentation compliance in-house and send the full pack to the buyer before the container leaves. A mismatch between invoice and IRN is a common cause of customs holds, and it is entirely avoidable.
Conclusion
Unplanned inspection causes rejected lots and missed sailings. Plan it early, define acceptance criteria, and treat documents as evidence. Then your MCT shipment arrives ready for installation.
Footnotes
1. Official site of DNV, a leading global classification society for the maritime and industrial sectors. ↩︎
2. Official ISO page for the standard governing the competence of bodies performing inspection. ↩︎
3. Official portal for the IATF 16949 automotive quality management system standard. ↩︎
4. Official site for the IECEx system regarding equipment for use in explosive atmospheres. ↩︎
5. Homepage of the International Electrotechnical Commission, the body responsible for IP and sealing standards. ↩︎


 English
 Español de México
 Deutsch
 Français
 العربية
 Русский