Multi cable transit installation usually forces a line stop. That stop costs more than the hardware. Our factory has shipped drop-in modules since 2013 precisely to shrink that window.
Multi cable transit installation avoids takt-time disruption when you move work upstream: verify 120-frame cutout dimensions, pre-select step-core EPDM sealing modules, pre-kit and label blocks, then complete frame drop-in, compression, and leak testing inside one short, scripted shutdown or shift change.
The rest of this article walks through that sequence in order. I start with dimensional verification, move to offline validation, then quantify where step-core modules save time, and finish with how to get samples and CAD files before you commit. Every section is written for a purchasing engineer who reads the spec sheet first and the sales pitch never.
How can I verify MCT module dimensions match my existing 120-frame cutouts before installation?
A QC engineer 1 on our Shaanxi line once rejected a whole frame batch because the inner opening drifted out of tolerance. That habit is exactly what your cutout check needs.
Verify fit by comparing three dimensions: the frame inner opening width and height, the module width in the 120-frame system, and the packing depth including compression unit. Request the supplier's cross-reference table, CAD/STEP files, and a free validation sample to check against your cutout.
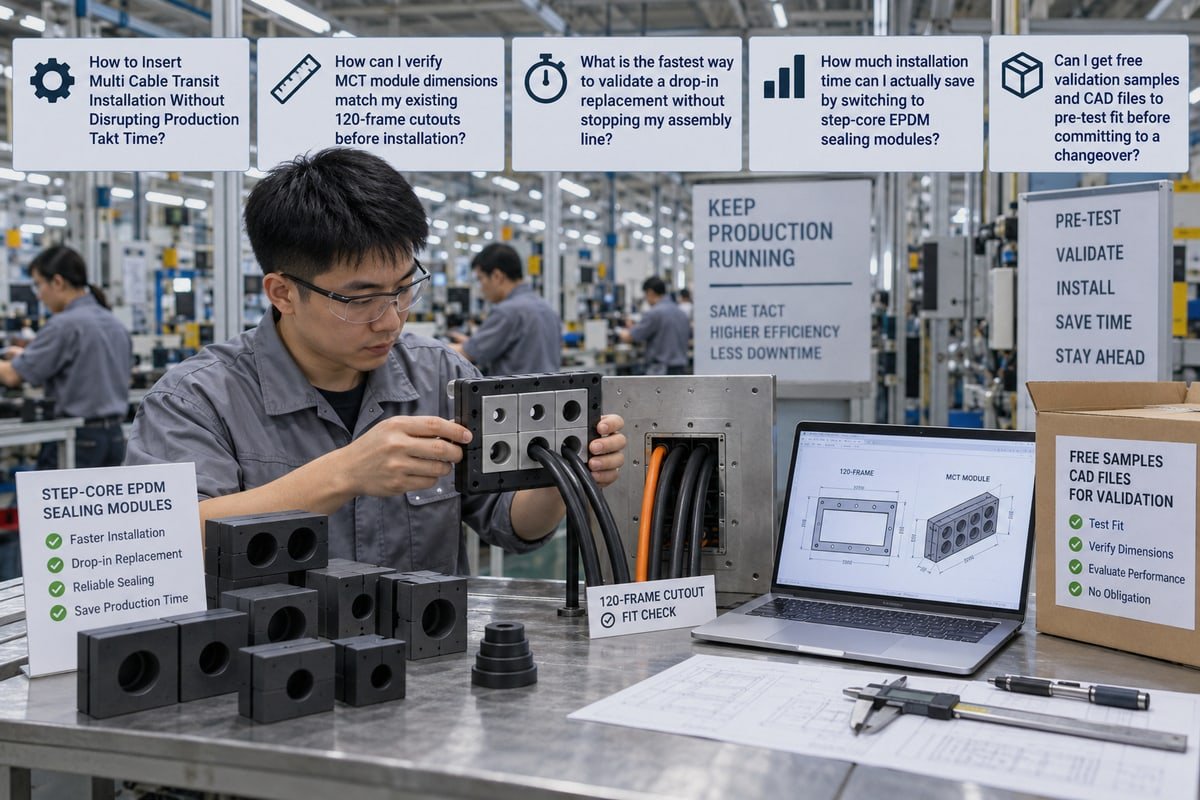
A cable sealing system has only three physical parts: the frame, the rubber sealing blocks, and the compression unit. That simplicity is good news for a retrofit installation. If those three parts share a common dimensional standard, a second-source module drops into a first-source frame. The 120-frame family is that common standard in most switchgear, BESS container 2, and modular data center penetrations we see from European buyers.
What the 120-frame standard actually fixes
The number refers to the nominal inner packing width 3 of the frame, so every module in the system is sized to stack across that width. Our TSC square modules and TSR round assemblies are built to those same nominal widths and heights. So when your existing frame was cut and welded for a 120-series product, our sealing blocks fill the same opening in the same stacking pattern.
But nominal is not the same as verified. I ask every buyer to check the items in the table below before a single block ships to the line.
| Check point | What to measure | Why it matters for takt time |
|---|---|---|
| Frame inner opening | Width and height at three points along each side | Weld distortion can narrow the opening; a tight stack means field trimming during shutdown |
| Module width and height | Compare against the cross-reference table (existing model → DEWIN model) | Confirms one-to-one substitution with no re-layout of the block plan |
| Packing depth | Frame depth versus module depth plus stay plates | Shallow frames leave the compression unit proud of the wall |
| Compression unit travel | Wedge or bolt stroke available versus stroke required | Too little travel means no seal; too much means over-compression |
| Spare capacity | Blank blocks as a percentage of total opening | Industry guidance recommends a minimum of 30% spare capacity, and many projects specify 100% |
How the cross-reference table shortens the check
Our model cross-reference table maps each common 120-frame module code to its DEWIN equivalent, with width, height, depth, and accepted cable diameter range side by side. Your engineer can compare it against the as-built drawing at a desk. Then the CAD/STEP file goes into your plant model or digital twin to confirm clearance behind the panel. Only after that does a physical sample touch the cutout. This ordering keeps all measurement work outside the production window, which is the whole point of a takt-safe multi cable transit installation.
What is the fastest way to validate a drop-in replacement without stopping my assembly line?
Three shifts, no gap for a trial. That was the constraint a sourcing manager at a European BESS container builder gave me. We built the validation plan around it.
The fastest validation is an offline bench test: mount a spare frame identical to your production cutout, insert sample sealing modules with representative cable diameters, compress, then run the flashlight leak test and pull test. Approve the second source before any live penetration is touched.
Two views compete here. One camp says validate on the real penetration during a planned outage, because that is the only true test. The other camp says never touch the line for a trial, because every minute of operational downtime hits assembly line throughput directly. My position is that both are right about different things. The real penetration must be tested once, at final cutover. But qualification of the module itself does not belong on the line at all. It belongs on a bench.
The five-step offline validation
- Build a twin of the cutout. Order or fabricate one spare frame to the same drawing as your production panel. Our modular frames ship in the same sizes as the cutout you already have, so this step is usually a purchase order, not a fabrication job.
- Load representative cables. Pull short cable offcuts covering the smallest and largest outer diameters in your build. Label each with its production circuit tag.
- Insert the sample sealing blocks. Follow the block plan from the cross-reference table. Note any block that needs force to seat; that is a dimension issue, not an installer issue.
- Compress and verify. Tighten the compression unit fully. A mechanical or torque-controlled tool gives repeatable pressure and removes operator variation.
- Run the two QA/QC checks. Shine a flashlight from the back and look for daylight around every block. Then pull each cable to check for slippage. Both are standard checkpoints in the industry and both take minutes.
Moving the result to the line
Once the bench passes, the live cutover becomes a repeat of a rehearsed sequence. Schedule it at a shift change or a natural production gap. Where live cables cannot be disconnected, split frame technology lets the frame close around them without re-threading. Give the installer a mobile digital checklist with the same five steps. Then the only new variable on the day is the wall itself, and you already measured that in the previous section.
How much installation time can I actually save by switching to step-core EPDM sealing modules?
Every module design in our mold shop weighs one trade-off: wider diameter range per block, or tighter fit per block. Step-core EPDM is how we settled it.
Step-core EPDM modules save time mainly by removing steps, not by faster tightening. One module size covers a range of cable diameters, so installers skip precise diameter measurement, module sorting, and re-ordering when a cable lands off-spec. Savings scale with cable count and mix.
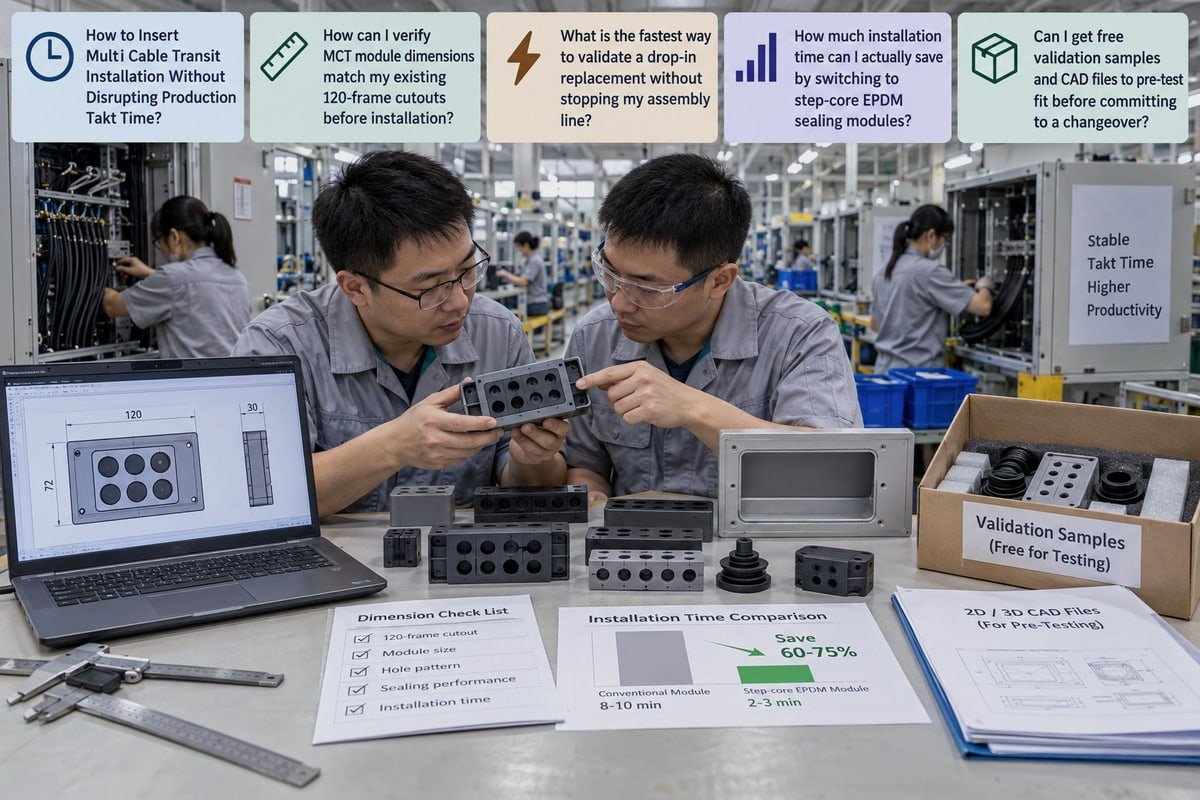
I will not quote you a fixed minutes-per-block figure. Installation time depends on cable count, access, and how well the kit was prepared. What I can do is show exactly which tasks disappear when the module adapts to the cable instead of the other way round.
Where the minutes actually go
| Installation task | Fixed-bore module | Step-core EPDM module |
|---|---|---|
| Measure every cable outer diameter | Required, to the millimetre | Confirm it sits inside the module's range |
| Sort modules by exact bore | Required, many SKUs | Fewer SKUs, sorted by range |
| Handle an off-spec cable | Stop, re-order or field modify | Same module absorbs the variation |
| Fill spare capacity | Blank blocks in each size | Fewer blank sizes to stock |
| Compression | Same | Same, wedge tightened to full position |
| Leak test and pull test | Same | Same |
The compression and inspection stages do not change. Rubber still has to be pressed by the compression wedge until the unit is fully tightened. What changes is everything before that. In a BESS container with dozens of DC, AC, and control cables of mixed gauge, the sorting and off-spec handling steps are where an installer loses the most time during a shutdown. Step-core geometry moves that risk out of the window entirely, because one block plan tolerates the real cable population.
The speed-versus-quality objection
Some buyers worry that a module built for a range seals less tightly than one built for a single diameter. Our engineers hear this often, so we test for it. The step-core halogen-free EPDM in our TSC and TSR modules is rated to IP68 and to watertight and gas-tight pressures of 0.01 to 0.4 MPa, with fire ratings 4 of A-0 and A-60 for firestop penetration duty. Test documents are available on request. So the range does not come at the cost of the seal. It comes at the cost of a slightly larger rubber volume per block, which we accept.
Cable management efficiency after the install
There is a second saving that shows up months later. When a cable is added to spare capacity, the same module range covers it. Spare sealing modules ship fast from our stock, and a Kanban-style reorder point for blank blocks keeps the production cell supplied without engineering involvement. That is cable management efficiency measured over the asset's life, not just on installation day.
Can I get free validation samples and CAD files to pre-test fit before committing to a changeover?
The lesson we learned early in exporting to Europe is simple. A spec sheet never closes a qualification. A sample in the buyer's hand does.
Yes. Qualified second-source suppliers such as DewinMCT provide free validation samples of round and square sealing modules, plus CAD/STEP files and model cross-reference tables, so engineers can pre-test fit in an existing 120-frame cutout, run leak and pull tests, and document supplier qualification before changeover.
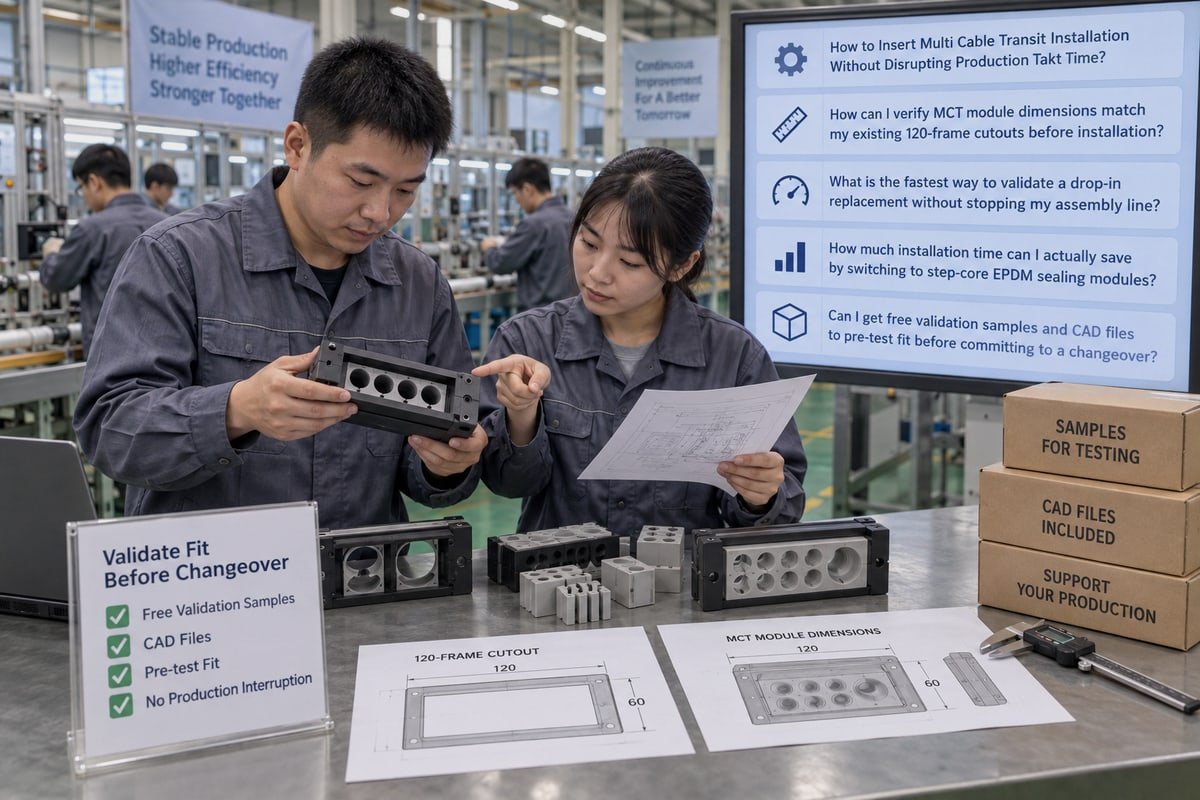
I treat the sample request as the start of a qualification file, not as a marketing gesture. Purchasing engineers at OEM integrators need evidence they can attach to a supplier approval form. So we structure the validation pack around what that form asks for.
What the validation pack contains
| Item | Format | How you use it |
|---|---|---|
| Sample sealing modules | Physical TSC square and/or TSR round modules in your requested sizes | Bench fit test, compression, leak and pull test |
| CAD/STEP files | Native 3D and 2D drawings of modules, frames, stay plates, compression units | Digital twin clearance check, block plan layout |
| Cross-reference table | Existing model → DEWIN model with dimensions and diameter ranges | One-to-one substitution mapping for your BOM |
| Test documentation | A-0/A-60 fire, IP68, 0.01–0.4 MPa watertight and gas-tight reports | Attach to supplier qualification and compliance records |
| Quality system evidence | ISO 9001, IATF 16949 certificates, BV factory approval | Audit trail for your quality department |
Why the factory behind the sample matters
A second source is only useful if it stays available. We are a factory, not a trading company, with headquarters in Shaanxi, additional production in Shandong and Hunan, RMB 50M registered capital, and more than 38 granted patents. In-house mold making means a custom size for a non-standard cutout does not wait on a third party. Private-label production is available for integrators who want their own part number on the module. Export documentation is handled on our side.
How to run the request
Send the frame drawing or a photo of the nameplate on your existing transit. We reply with the matching cross-reference entries and STEP files first, usually before samples ship, so your engineer can start the digital check immediately. Then the physical modules follow for the bench test described earlier. The typical outcome is a qualified drop-in second source at 40–60% lower component cost, with no change to your frame, your cutout, or your takt time.
Conclusion
Takt time survives multi cable transit installation when you verify fit, validate offline, kit step-core modules, and script the shutdown. Our free samples and CAD files make that step risk-free.
Footnotes
1. The American Society for Quality provides resources and standards for quality control engineers in manufacturing environments. ↩︎
2. IEA report on the growth and technical requirements of battery energy storage systems (BESS) in global infrastructure. ↩︎
3. Technical overview of multi-cable transit systems, explaining frame sizing and packing space for industrial cable management. ↩︎
4. UL Solutions provides testing and certification for fire ratings of penetration seals in industrial and marine applications. ↩︎
5. Official ISO page for the 9001 standard, the global benchmark for quality management in series production. ↩︎



 English
 Español de México
 Deutsch
 Français
 العربية
 Русский