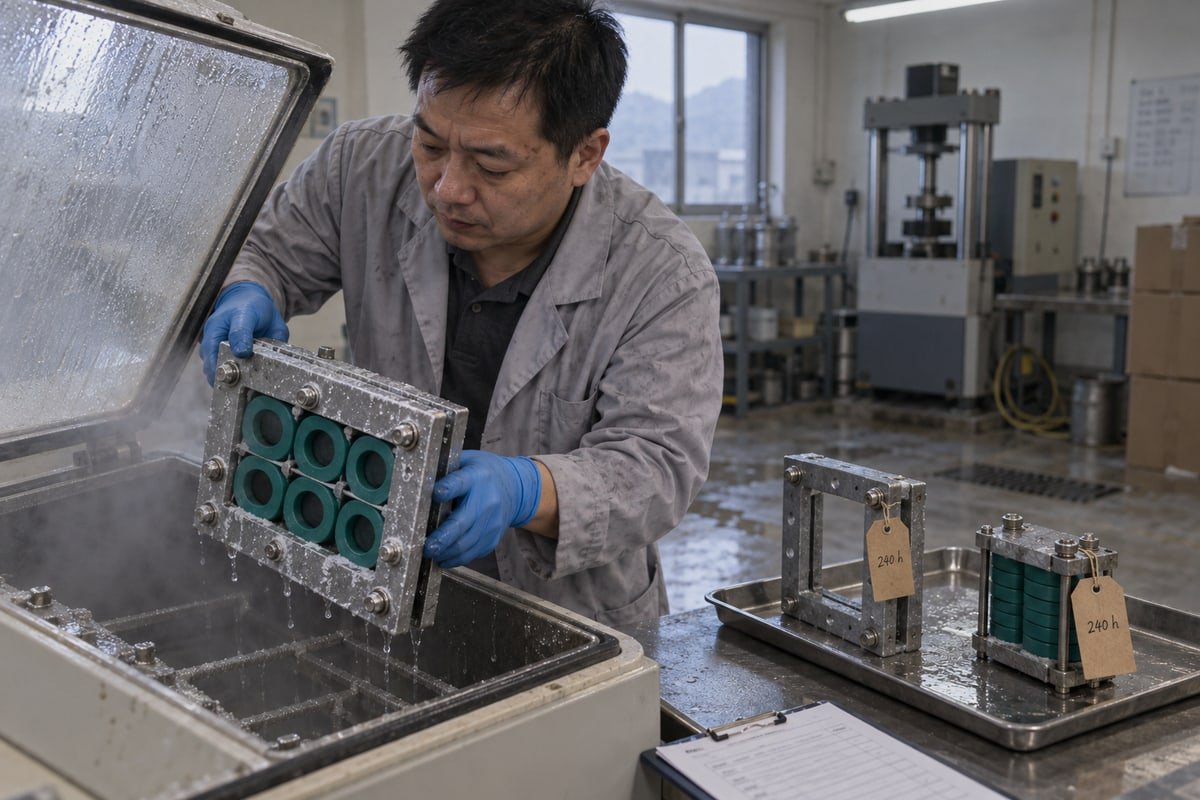
A salt spray chamber exposes weak cable penetration seals fast. When our engineers reviewed corrosion resistance of sealing materials in multi cable transits, hardware often failed before rubber.
Verify corrosion resistance of sealing materials in multi cable transits by requesting neutral salt spray testing to ISO 9227, ASTM B117, or IEC 60068-2-52 on the full assembly, at 5% NaCl and 35°C, for a stated duration, followed by documented inspection of seals, frame, bolts, and repeat ingress testing.
That is the short version. The rest of this article explains each part of it. I will cover the standards, the hours, the compounds, and the paperwork. I will also point out where salt spray claims tend to mislead.
What test standards should I ask my MCT supplier to reference for salt spray certification?
A sourcing engineer in the Netherlands once sent us a competitor's brochure with "1000 hours salt spray" and asked one question: to which standard? That question is the right one.
Ask your MCT supplier to reference ISO 9227 or ASTM B117 for neutral salt spray, and IEC 60068-2-52 for cyclic salt mist. The report should state the 5% NaCl solution, 35°C chamber temperature, exposure hours, specimen type, and pass/fail criteria for both elastomer and metal parts.
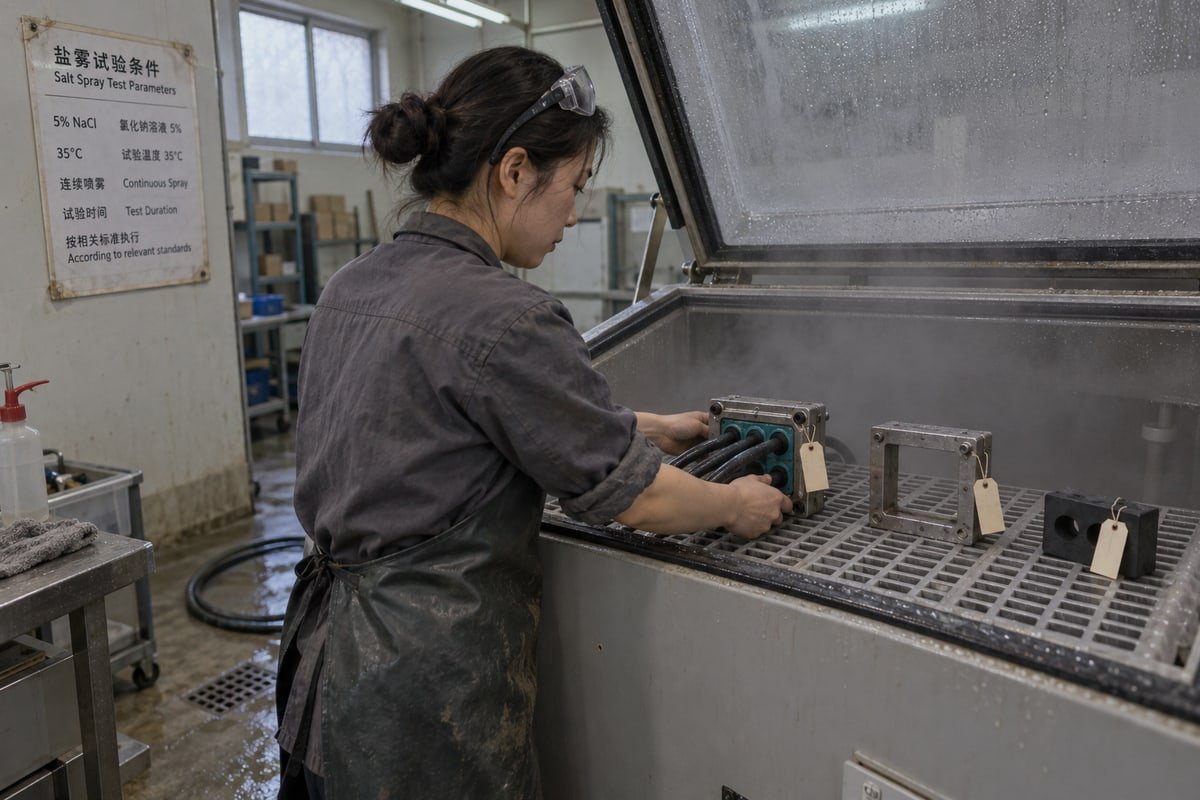
The standard tells you how the chamber was run. Without it, an hour count is just a number. Three standards come up most often for cable penetration seals. They are related, but they are not the same.
Three standards, three purposes
| Standard | Type | Typical conditions | What it is good for |
|---|---|---|---|
| ASTM B117 standard | Continuous neutral salt spray | 5% NaCl, 35°C, continuous fog | Screening coatings, fasteners, and frame finishes |
| ISO 9227 1 testing (NSS method) | Continuous neutral salt spray | 5% NaCl, 35°C, continuous fog | International equivalent; common in European specs |
| IEC 60068-2-52 | Cyclic salt mist | Spray phases followed by humid storage phases | Electrical enclosures and assemblies; closer to wet-dry service |
ASTM B117 and ISO 9227 are close cousins. Both use neutral salt spray with a 5% sodium chloride solution at about 35°C. Both are continuous fog. If a supplier quotes one, they can usually explain the other. IEC 60068-2-52 is different. It alternates salt mist with humid storage. That cycling is harder on some coatings and on crevices between module and frame. One published transit product claims 720 hours, or 30 days, under this method. Another claims 1,000 hours corrosion-free on a marine frame under ISO 9227. Both claims can be true. They just do not mean the same thing.
Why the standard alone is not enough
Here is the objection I hear most from skeptical buyers. "The test method itself says it does not simulate a seacoast or shipboard environment. So why bother?" That caution is real, and it is written into the standard language. But it does not make the test useless. It makes it a screen. A frame that shows red rust after 168 hours in neutral salt spray will not survive a coastal BESS container yard. A frame that passes 1,000 hours has cleared a meaningful bar. The screen sorts out bad candidates. It does not promise a service life.
The second point is scope. Ask whether the specimen was a loose rubber block, a bare frame, or a compressed assembly with cables installed. Corrosion resistance of sealing materials in multi cable transits is a system property. Galvanic or electrochemical corrosion 2 between a carbon steel frame and stainless bolts can seize the compression unit long before the EPDM changes. When we prepare test documents on request, we always state which configuration was in the chamber.
How long should salt spray testing run before I can trust the corrosion resistance results?
Every extra hour in the chamber costs test budget and delays a qualification. Every hour cut raises the risk of shipping a frame that rusts. We weigh that trade-off often.
Treat 168 hours of neutral salt spray as the minimum for marine validation, 336 hours for harsher exposure, and 720 to 1,000 hours for offshore or coastal frames. Trust results only when the report names the method, acceptance criteria, and a post-exposure ingress protection recheck.
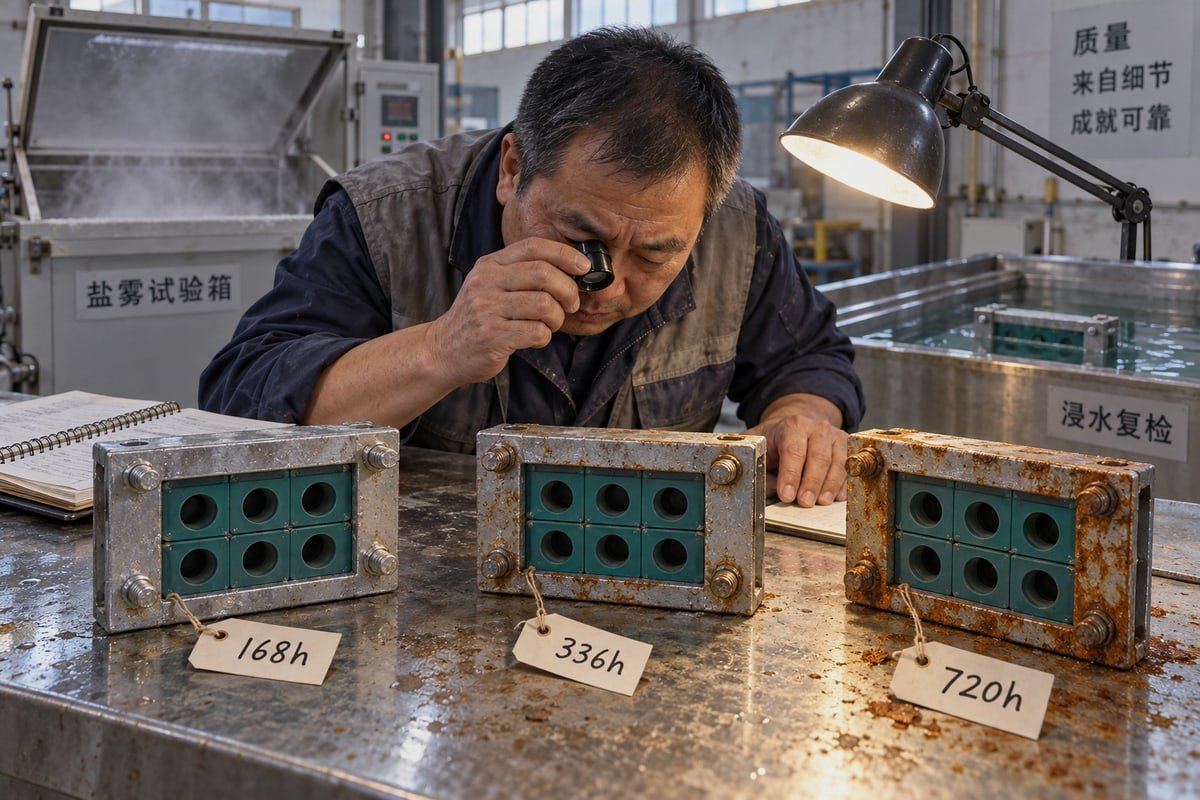
Duration is the number everyone quotes. It is also the number that misleads most. Let me put the common tiers side by side first, then explain why the tier is only half the story.
Common duration tiers and what they usually cover
| Exposure time | Typical use | What it can tell you |
|---|---|---|
| 96 hours | Quick screening of coatings and plating | Gross defects, bare spots, poor passivation |
| 168 hours | Common minimum benchmark for marine cable assemblies | Basic fitness for humid, salt-laden air |
| 336 hours or more | Harsher exposure categories | Crevice and edge behaviour, fastener condition |
| 720 hours (30 days) | Long-duration claims tied to IEC 60068-2-52 | Cyclic wet-dry resilience of the assembly |
| 1,000 hours | Marine frame claims under ISO 9227 | Pitting resistance of 316L-class stainless and coatings |
Why hour counts mislead
Some buyers push back here. "If a vendor says 1,000 hours, that beats 336 hours. Done." Not always. A 1,000-hour result on a polished 316L frame coupon says nothing about the compression wedge, the bolts, or the seam where the module meets the frame. A 336-hour result on a fully assembled, compressed transit with cables installed may tell you more. Read the specimen description before you compare hours.
The second trap is acceptance criteria. Some reports count "no red rust" only on visible faces. Others include a mass-loss measurement and a compression-force check on the elastomer. Those are very different levels of material durability analysis. Ask which one you are looking at.
What passes and fails look like after exposure
A real pass, in my view, has five parts. No red rust on frame, bolts, or stay plates. No cracking, swelling, or chalking on the sealing blocks. No measurable loss of compression when the wedge is re-torqued. No leakage when the assembly is retested for water or gas tightness. No seized fasteners. On our side, the tightness retest matters most. A sealing system rated for 0.01 to 0.4 MPa watertight and gas-tight service should hold that range after the chamber, not just before it.
One more objection deserves an answer. Engineers rightly say that continuous fog misses UV, temperature cycling, and vibration. I agree. That is why I recommend asking whether cyclic corrosion testing was considered for real service conditions. Cyclic exposure with humid rest phases stresses the module-to-frame interface in a way a static fog does not. It is not a replacement for a long neutral salt spray run. It is a second lens.
Which sealing materials perform best against corrosion when I compare EPDM to alternative compounds?
On our production line in Shaanxi, every batch of step-core EPDM modules gets hardness and compression-set checks before packing. Salt rarely scares that compound. Its frame neighbors do.
Halogen-free EPDM performs best against salt spray corrosion among common sealing compounds, with strong resistance to chloride, ozone, and water swelling. Silicone tolerates higher temperature but tears more easily, nitrile resists oil but degrades in salt and ozone, and neoprene sits between them.
Here is the direct comparison first. The ratings are qualitative and reflect how these compounds behave under saline environment exposure in cable transit service.
| Property | EPDM (halogen-free) | Silicone | Nitrile (NBR) | Neoprene (CR) |
|---|---|---|---|---|
| Salt water and chloride resistance | Excellent | Good | Poor to fair | Good |
| Ozone and weathering | Excellent | Excellent | Poor | Good |
| Water swelling | Very low | Low | Moderate | Low to moderate |
| Tear and abrasion resistance | Good | Poor | Good | Good |
| Oil and fuel resistance | Poor | Poor | Excellent | Fair |
| Compression set at ambient | Good | Fair | Good | Fair |
| Typical role in cable penetration seals | Standard marine module | Special high-temperature cases | Oil-exposed panels | Legacy or mixed duty |
Why the elastomer is rarely the weak link
Buyers often assume the rubber is the part that corrodes. Rubber does not corrode. It degrades. Elastomer degradation in salt spray shows up as surface cracking, swelling, hardening, or loss of compression. EPDM is a saturated polymer with no double bonds in its backbone, so ozone and chloride have little to attack. In an accelerated aging test, it holds its elasticity better than nitrile or neoprene. That is why nearly every marine module on the market uses it, ours included.
The weak link is usually metal. A frame in plain galvanized steel will show white then red corrosion products long before the module changes. A frame in 316L stainless resists pitting and crevice corrosion far better. Mixed metals add another risk. Stainless bolts in a carbon steel frame set up electrochemical corrosion at the contact points. Marine grade materials across the whole assembly, not just the module, decide the outcome. When we quote a frame for a coastal data center or BESS project, we ask about the frame material first and the compound second.
Interface effects that a material sheet will not show
Two failure modes live at the interface. The first is wicking. Salt water can migrate along a cable jacket into the transit interior by capillary action. A module that grips the cable over its full contact length, as a step-core design does across its diameter range, limits that path. The second is salt crystal abrasion. Salt that dries in the seal-to-cable gap forms a crust. Under vibration, that crust can abrade or tear the sealing face. Cyclic testing catches this better than continuous fog.
For early detection, some labs apply electrochemical impedance spectroscopy 3 to coated frames. It picks up sub-surface electrolyte penetration before visible damage appears. It is not common in MCT reports yet. It is worth asking about for critical projects.
What documentation should I request to verify test results before qualifying a new supplier?
We learned early, after a European integrator rejected a report because photos lacked a scale bar, that documentation quality is judged as hard as the test itself.
Request the full third-party or in-house salt spray report with standard reference, test conditions, specimen description, exposure hours, before-and-after photos, pass/fail criteria, and post-test ingress protection results, plus material certificates for the stainless grade, coating, and elastomer compound, and the lab's accreditation.
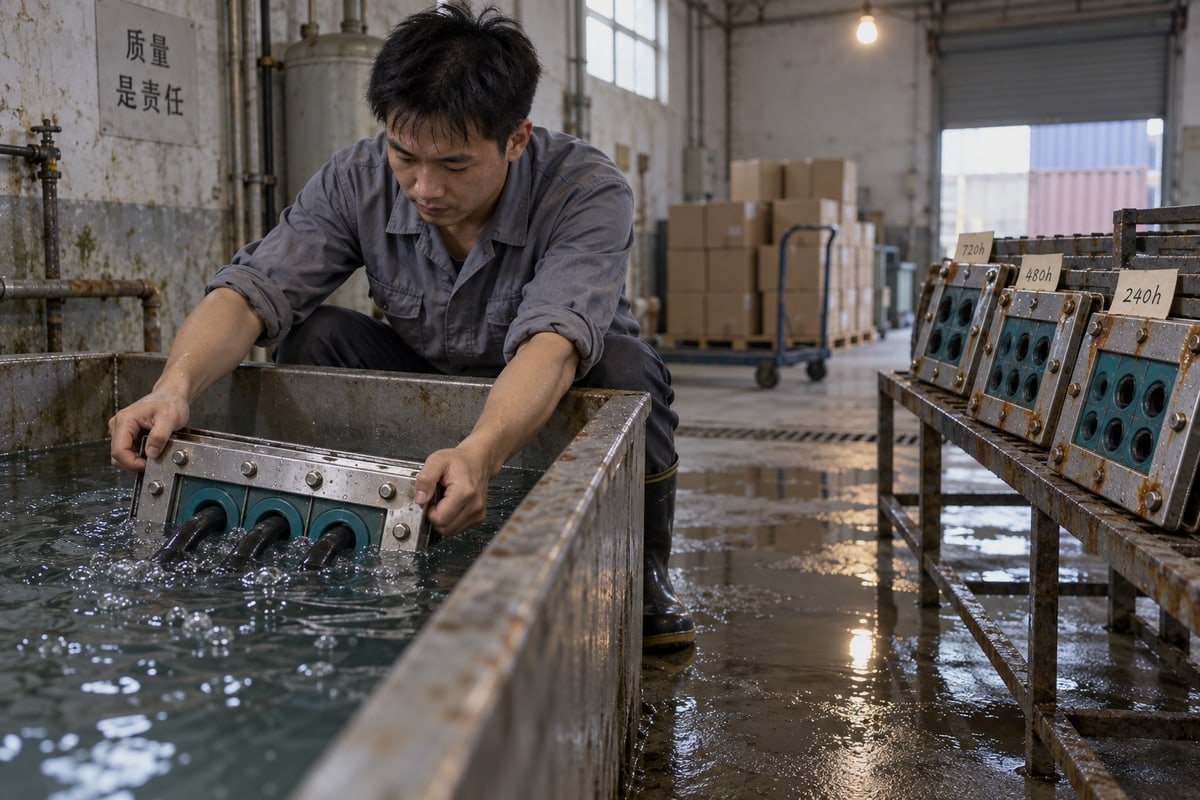
A brochure statement is not evidence. A report is. The table below lists what I would ask for, and what each document actually proves.
| Document | What to check | What it proves |
|---|---|---|
| Salt spray test report | Standard, NaCl concentration, temperature, hours, specimen description | The exposure was real and repeatable |
| Photo set with scale | Before, during, and after; close-ups of bolts, seams, module faces | Where corrosion started, if anywhere |
| Post-exposure tightness report | Water or gas pressure held, duration, leak criteria | Sealing function survived the exposure |
| Ingress protection certificate | Rating claimed (IP66, IP67, IP68, IP69K) and test body | The enclosure class the assembly meets |
| Material certificates | Stainless grade (for example 316L), coating type and thickness, elastomer compound datasheet | The tested materials match what you will receive |
| Quality system certificates | ISO 9001, IATF 16949 4, class society approval | The supplier can repeat the tested build |
| Cross-reference and drawings | Existing model to new model, CAD or STEP files, 120-frame cutout dimensions | The part drops into your frame without rework |
A five-step qualification sequence that works
- Send the supplier your existing module or frame model numbers. Ask for a cross-reference table to their equivalents.
- Request the salt spray report, tightness report, and material certificates for those exact models. Confirm the report covers the compressed assembly, not loose blocks.
- Ask for free validation samples. Fit them into your current 120-frame cutout and check the compression travel and bolt torque.
- Run your own short check. Even 168 hours of neutral salt spray at your local lab, followed by a tightness test, tells you a lot.
- Confirm lead time for spare sealing modules and export documentation before you place the first order.
On our side, buyers ask for the same set. Our ISO 9001 and IATF 16949 systems and our BV-approved factory status cover step 2. Our A-0 and A-60 fire rating, IP68 ingress protection rating 5, and 0.01 to 0.4 MPa watertight and gas-tight documents are available on request. The cross-reference table and free samples cover steps 1 and 3. That is how a second source at 40 to 60 percent lower cost gets qualified without guesswork.
Questions that expose a weak claim
Ask which exact standard was used. Ask whether the test covered the full assembly or single materials. Ask what concentration, temperature, and duration applied. Ask for pass/fail criteria and photos. Ask whether ingress protection was rechecked afterward. Ask whether the stainless grade, coating, and compound are documented. Ask whether cyclic corrosion was considered. A supplier who answers all seven quickly has probably done the work.
Conclusion
Salt attacks the whole transit, not just rubber. Verify with a named standard, full-assembly exposure, post-test ingress checks, and complete documents before you qualify any cable transit supplier.
Footnotes
1. Official ISO standard page for the referenced neutral salt spray test method. ↩︎
2. Wikipedia background on galvanic corrosion between dissimilar frame and bolt metals. ↩︎
3. Background reference explaining this early corrosion detection technique mentioned in the article. ↩︎
4. Official body for the automotive quality management standard cited as supplier certification. ↩︎
5. IEC/ISO ingress protection rating standard relevant to enclosure classification discussed. ↩︎


 English
 Español de México
 Deutsch
 Français
 العربية
 Русский