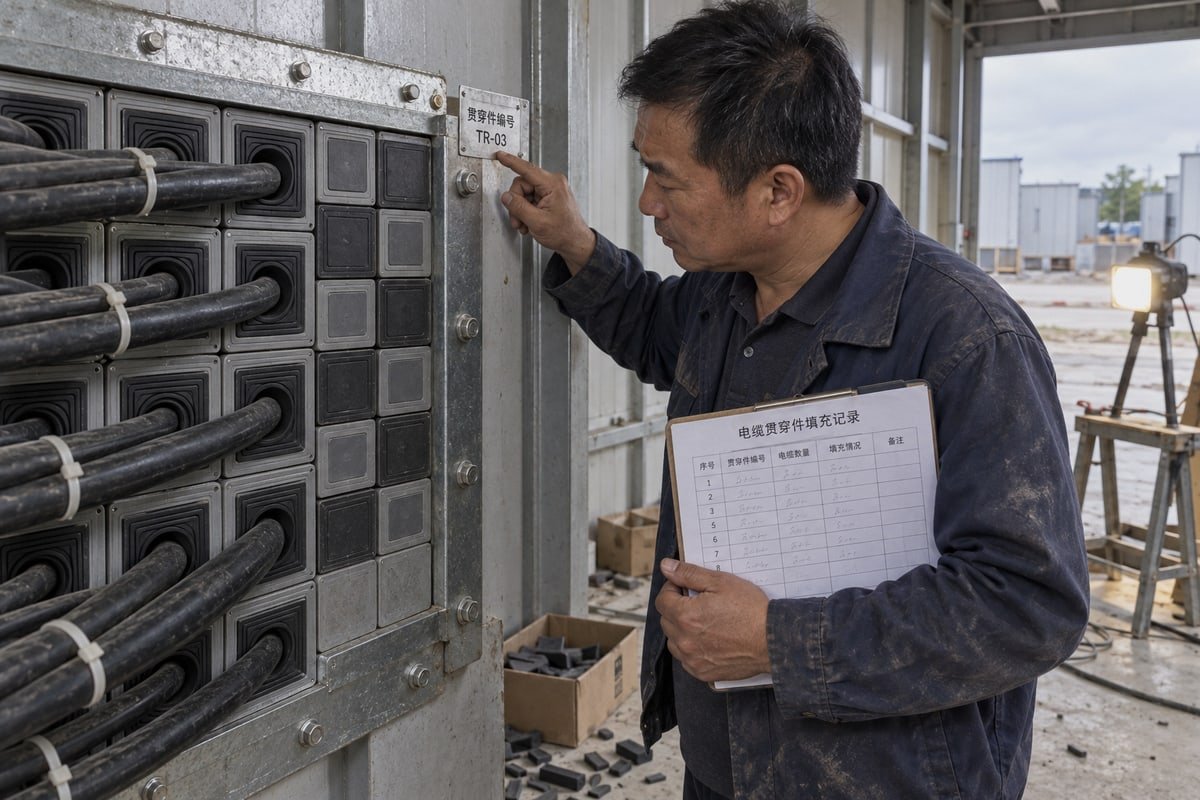
Your E-House is built, but the MCT sealing module filler record sheet has gaps as-built documentation 1. Handovers stall for weeks over this. Our export team sees it constantly; here is the fix.
Organize the MCT sealing module filler record sheet with one line per transit opening. Record the transit tag, frame type, cable IDs, module and filler sizes by row and column, compression status, reserved spare capacity, inspection date, inspector, drawing references, and sign-off.
That is the short version. The rest of this article shows you what each field is for, how to link it to the cable schedule, which certificates belong in the dossier, and how to reuse the same sheet on every project.
What Fields Should I Include in an MCT Filler Record Sheet for Traceability?
A sourcing engineer in Rotterdam once sent us a filler sheet with many columns and no transit tags A-60 ratings 2. Nobody could tie it to the as-built drawings.
Include the project and E-House name, transit tag, location, frame size and system type, opening dimensions, cable count and IDs, module sizes, filler quantities and sizes, row and column positions, compression status, spare capacity, inspection date, installer and inspector names, drawing references, NCR status, and sign-off.
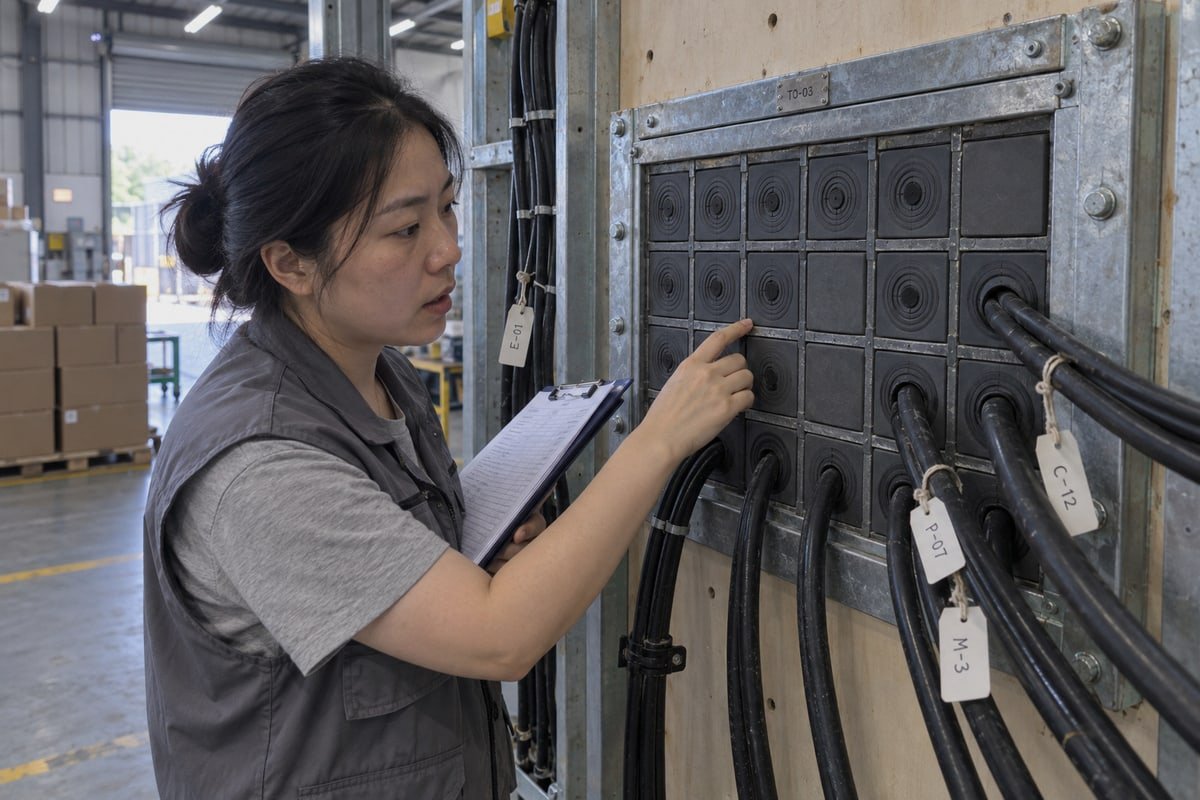
The filler record sheet is a handover control document. It is not a parts list. It has to prove four things before the client accepts the E-House. The module selection was correct. The installation was done to the approved method. The firestop seal integrity 3 and gas-tightness are intact. And the as-built documentation matches what is physically in the wall.
Why fillers deserve their own columns
An MCT transit 4 has three parts: the frame, the rubber modules, and the compression unit. Filler blocks are the modules that hold no cable. They close unused space and reserve room for future cables. They are not spacers. They carry compression load, they contribute to the fire and gas rating, and they define how much spare capacity the E-House really has. So the sheet must record them with the same care as live modules. On our TSC square modules, a filler block and a live module share the same outer dimensions, which makes row-by-row logging simple.
The core field set
| Section | Field | Why it matters at handover |
|---|---|---|
| Identification | Project, package, E-House name, transit tag | Links the sheet to the tag database and the general arrangement drawing |
| Identification | Location, wall or panel reference, opening dimensions | Confirms the frame sits where the drawing says it does |
| Configuration | Frame size, system type, module standard | Proves the frame matches the approved design and any 120-frame compatibility requirement |
| Inventory | Cable count and cable IDs | Ties each opening to the cable transit schedule |
| Inventory | Module sizes, filler sizes and quantities, row and column positions | Gives a grid map for future maintenance and spare capacity planning |
| Verification | Compression status, torque value, stay plate positioning | Validates compression wedge installation and blast or fire resistance |
| Verification | Inspection date, installer, inspector | Assigns responsibility to named people |
| References | Drawings, test packs, redlines, photos | Connects the sheet to controlled documents |
| Closeout | NCR or punch status, spare capacity reserved, client sign-off | Shows every exception was resolved before acceptance |
The lean-versus-detailed objection
Some EPC teams push back here. They say a detailed sheet duplicates the drawings and slows turnover. They prefer a lean form that records only deviations and final status. That view has a point. But a lean form cannot prove full closure of every opening. And it cannot tell a maintenance crew, three years later, which grid position is free. The middle path works best. Keep a mandatory core data set on one line per transit. Then attach photos, marked-up drawings, and test evidence as links. The core stays short enough for field use. The attachments carry the proof.
How Do I Cross-Reference Filler Configurations to Cable Diameters and Module Positions?
During final inspection on our Shandong line, we once caught a kit packed with modules one size too small for the measured cable diameters. Verification saved that shipment.
Cross-reference by giving every transit a tag, then mapping each row and column position in the frame to a cable ID from the cable transit schedule. Record the measured cable diameter, the module size selected, and whether the position holds a filler or a live cable.
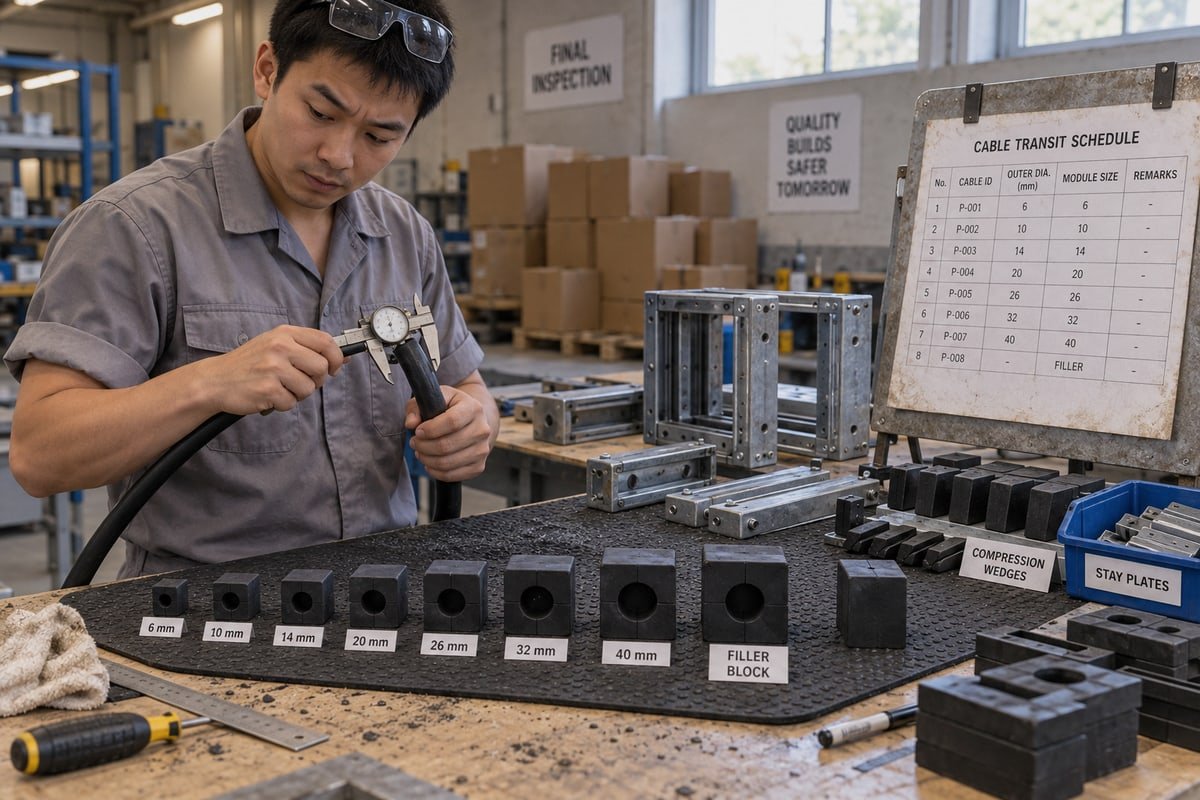
Cross-referencing is where most sheets fail. A sheet that lists "12 modules, 6 fillers" tells the auditor nothing. A sheet that says "Row 3, Column 2, cable ID PW-104, measured OD 27.5 mm, module size 30" tells the auditor everything. The difference is a coordinate-based grid.
Step one: tag the transit
Every frame gets a unique tag. We recommend the tag follow the E-House naming convention, not the supplier's. A typical form is E-House number, wall reference, and sequence. The tag goes on the nameplate between the compression bolts and on the sheet. That way the field crew, the document controller, and the maintenance team all use the same identifier.
Step two: build the grid
Number the rows from the bottom up and the columns from left to right. Each position gets one entry. This mirrors the packing plan that most designers already produce. Many of our European buyers call it a Roxtec packing plan, because that is the format their original supplier issued. Our modules are dimensionally compatible with common 120-frame standards, so the same grid drops onto our frames without redrawing. The grid notation stays the same whether the modules come from the original vendor or from us as the qualified second source.
Step three: verify diameters before selecting modules
Cable diameter verification happens on site, not on paper. Cable datasheets give nominal outer diameters. Real cables vary. The installer measures each cable at the transit, records the value, and picks the module size whose range covers it. Our step-core EPDM modules adapt to a range of diameters within one module size. The installer peels layers until the core fits the cable with no gap. The sheet should record the measured diameter and the final module size, so the auditor can confirm the range was respected.
Sample cross-reference block
| Transit tag | Row | Col | Cable ID | Measured OD (mm) | Module size | Filler or live | Stay plate above row |
|---|---|---|---|---|---|---|---|
| EH01-W2-03 | 1 | 1 | PW-101 | 33.2 | 40 | Live | Yes |
| EH01-W2-03 | 1 | 2 | PW-102 | 33.0 | 40 | Live | Yes |
| EH01-W2-03 | 1 | 3 | — | — | 40 | Filler | Yes |
| EH01-W2-03 | 2 | 1 | CT-210 | 14.8 | 20 | Live | Yes |
| EH01-W2-03 | 2 | 2 | — | — | 20 | Filler | Yes |
| EH01-W2-03 | 3 | 1 | — | — | 60 | Filler (reserved) | Yes |
Why stay plate positioning belongs on the same line
Installation guidance for cabinet seal configurations requires a stay plate above every row of insert or filler blocks. The stay plate stops rows from shifting under blast or fire load. If you record stay plate positioning next to the row it protects, the auditor sees the confirmation in one glance. If you record it elsewhere, the auditor has to hunt for it. Put it on the line.
The expansion inventory
The last column set is spare capacity planning. For each reserved position, state the filler size that occupies it and the module type that will replace it later. This turns the sheet into a plug-and-play guide for future upgrades. When the client adds cables in year three, they order the exact spare modules from the sheet. We keep spare sealing modules in stock for this reason, and a clean grid lets us ship the right part without a site visit.
What Certification Documents Should Accompany My E-House Handover Package?
Our documentation team weighs one trade-off on every export order: a thin certificate folder ships faster, but a thick one passes the client's audit.
Include the manufacturer's product catalogue and component drawings, fire test certificates for A-0 or A-60 ratings, gas-tightness and watertight test reports, ingress protection certificates, ageing reports, the approved method statement, QA/QC inspection reports, compression torque records, and the signed filler record sheet with as-built drawings.
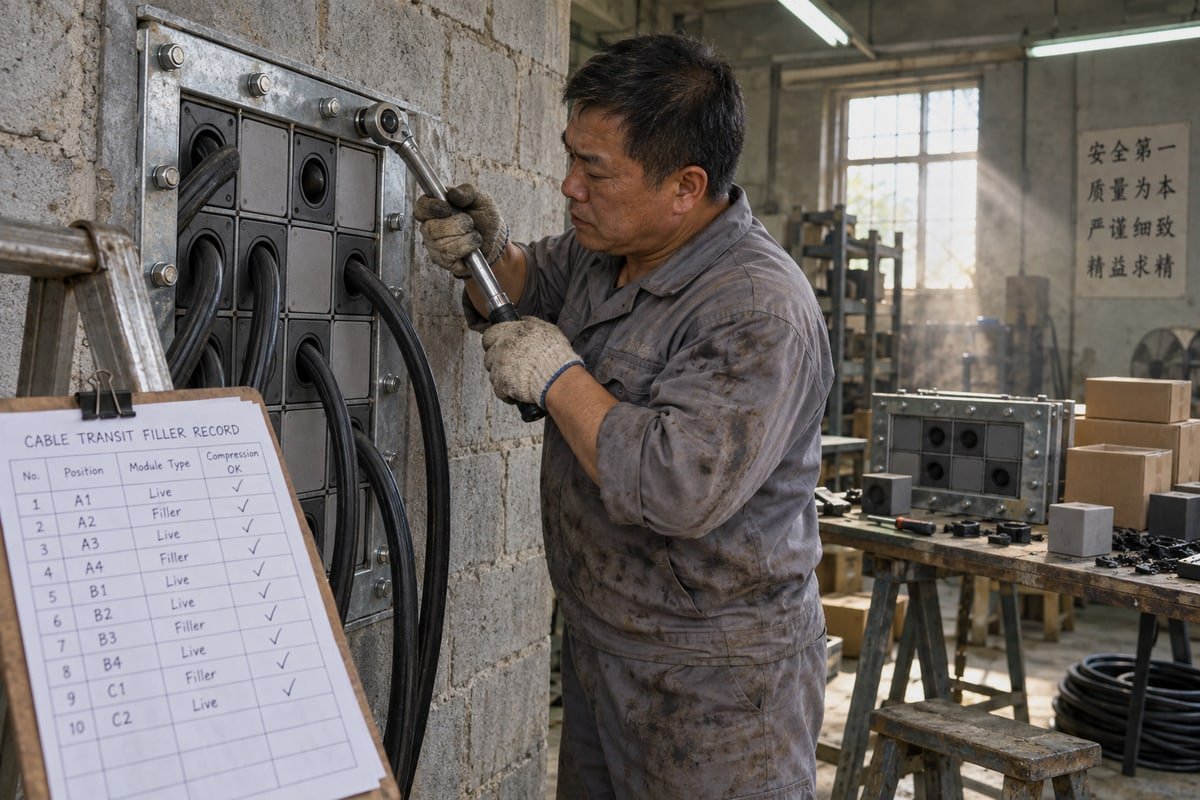
The filler record sheet does not stand alone. It sits inside a controlled handover index. The client's completions engineer opens the index, finds the transit tag, and follows links to every document behind it. If any link is broken, the transit stays on the punch list.
What formal MCT submissions normally contain
Formal submissions for MCT work usually cover three layers. The first layer is product data: catalogues and detailed component drawings. The second layer is test evidence: blast test reports, gas-tightness test reports, and ageing reports. The third layer is installation control: method statements and workmanship specifications. The handover package should carry all three, and the filler sheet should reference each one by document number and revision.
Document checklist by layer
| Layer | Document | Source | Handover use |
|---|---|---|---|
| Product data | Product catalogue, component drawings, CAD or STEP files | Manufacturer | Proves the installed frame and module models match the approved design |
| Product data | Model cross-reference table | Manufacturer | Shows equivalence when a second-source module replaces the original specification |
| Test evidence | Fire test certificate (A-0 / A-60) | Manufacturer, third-party lab | Supports the firestop seal integrity claim for the wall or bulkhead |
| Test evidence | Gas-tightness and watertight test report (0.01–0.4 MPa) | Manufacturer | Supports the pressure rating recorded on the sheet |
| Test evidence | Ingress protection 5 certificate (IP68 tested, covers IP66 ingress protection requirements) | Manufacturer | Matches the E-House enclosure rating |
| Test evidence | Ageing report | Manufacturer | Supports the design life of the EPDM material |
| Quality system | ISO 9001, IATF 16949 6 certificates, BV factory approval | Manufacturer | Satisfies vendor qualification audits |
| Installation control | Method statement, workmanship specification | Contractor with manufacturer input | Defines the accepted compression wedge installation procedure |
| Field records | QA/QC inspection report per transit | Contractor QA/QC | Records item, date, procedure, result, test equipment, and personnel |
| Field records | Compression torque log | Installer | Validates that the wedge reached the specified value |
| Field records | Photographs, internal and external faces | Installer or inspector | Visual proof of closure and orientation |
| Field records | Signed filler record sheet and as-built redlines | Contractor, client | Final acceptance record |
What a QA/QC inspection report must state
Handover guidance for industrial electrical work is specific here. Each record should identify the item tested, the date, the procedure, the result, the test equipment, and the responsible personnel. A torque value without a wrench serial number is weak evidence. A photo without a date and a tag is weak evidence. The sheet should carry the reference to the report, and the report should carry the six items above.
Where our documents fit
When we ship a TSR or TSC order, the test documents go with it on request. Our fire rating is A-0/A-60, our ingress protection is tested to IP68, and our watertight and gas-tight sealing is tested across 0.01–0.4 MPa. Our systems run under ISO 9001 and IATF 16949, and the factory holds BV approval. We also provide the model cross-reference table, so a document controller can show why a DEWIN module sits where the original specification named a different brand. That table closes the most common audit question on second-sourced transits.
Ultrasonic testing as a supplement
Some clients add non-destructive ultrasonic leak testing on installed transits. The result gives empirical proof of airtightness on the specific wall, not just on a lab sample. If the client asks for it, record the result and the instrument on the transit line. It is a supplement to the factory certificates, not a replacement.
How Can I Standardize Filler Record Sheets Across Multiple E-House Projects for Faster Audits?
We learned this lesson the hard way after supplying spare modules to an E-House whose original filler sheet used a different layout than the sister unit next to it.
Standardize by fixing one mandatory core data set, one transit tag convention, one row-and-column grid notation, and one attachment rule for photos and redlines. Issue the template as a controlled document with a revision number, and reuse it unchanged on every E-House project.
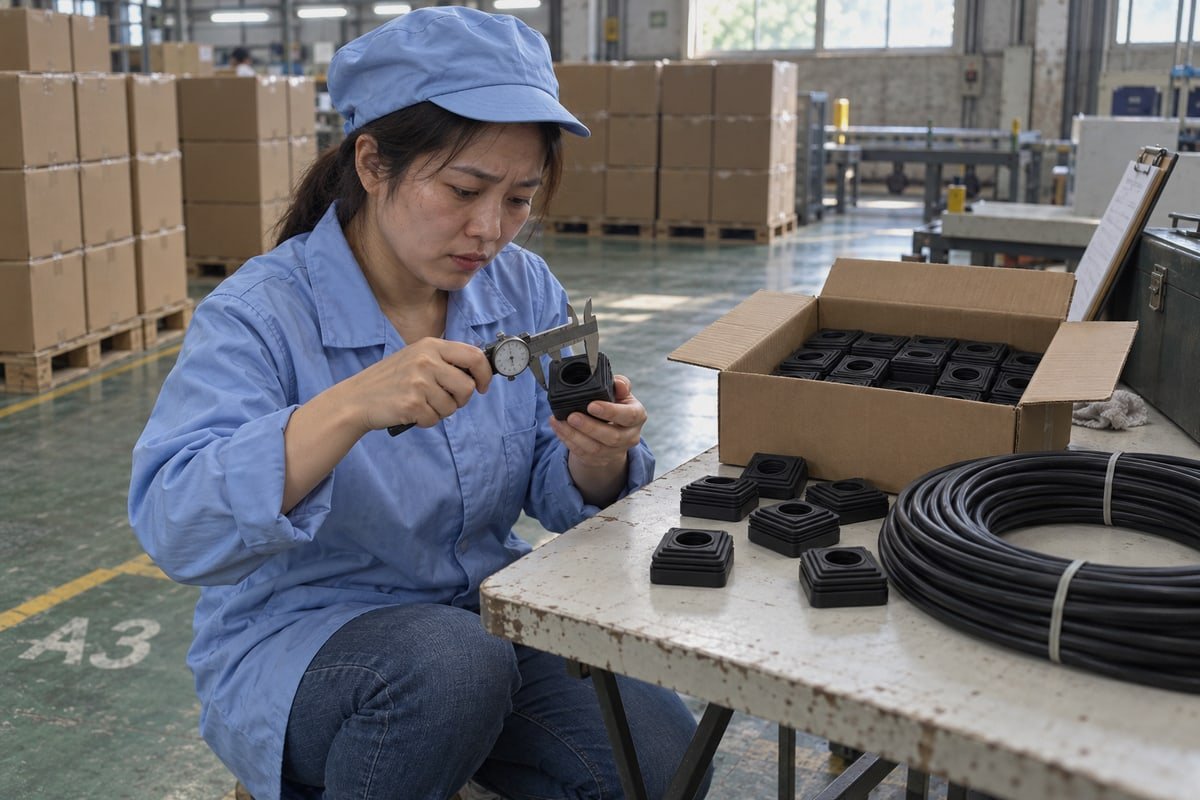
Auditors move fast when every sheet looks the same. They slow down when each project invents its own columns. Standardization is not about adding fields. It is about freezing the fields that matter and removing the rest.
A six-step workflow for every project
- Verify the approved drawings and the cable transit schedule before any module is installed.
- Assign a unique tag to every transit using the fixed convention.
- Record installed modules and fillers by row and column, with measured cable diameters.
- Photograph the completed transit, both faces, with the tag visible.
- Cross-check the sheet against the punch list and close every open item.
- Obtain QA/QC and client sign-off before the wall or cabinet is closed.
Step six matters most. Records must be complete before inaccessible areas are sealed. Once cladding goes on, nobody can re-check a stay plate.
Common mistakes a standard template prevents
Wrong module sizing is the first. A fixed diameter column with a required entry stops it. Missing transit tags are the second. A tag column that rejects blanks stops it. Undocumented spare openings are the third. A required "filler or live" entry for every grid position stops it. Mismatched drawings are the fourth. A revision column for the referenced drawing stops it. Unsigned inspection records are the fifth. A sign-off block that locks the row stops it.
Paper form versus digital record
| Aspect | Standalone paper sheet | Controlled digital record |
|---|---|---|
| Traceability | Depends on filing discipline | Linked to tag database and drawing set |
| Search | Manual | Instant by tag, cable ID, or grid position |
| Attachments | Stapled photos, easily lost | Photos and redlines linked to the transit line |
| Superseded versions | Hard to control | Revision history built in |
| Field access | Easy without devices | QR code on the frame links to the record |
| Audit speed | Slow | Fast |
The trend across our European and Middle East customers is clear. They want the sheet inside the digital handover, linked to the tag database, the drawing set, and the punch list. A weather-resistant QR code on each frame nameplate is a practical bridge. The maintenance technician scans it and sees the grid, the spare capacity, and the module part numbers.
Why standardization helps second sourcing
A frozen template makes supplier qualification easier too. When the grid notation and module sizes are fixed, our cross-reference table maps the original model to the DEWIN model position by position. The client's document controller updates one column, not the whole sheet. That is how integrators cut transit component cost by 40–60% without losing certification or traceability. The free validation sample goes into the same grid, the sheet records it, and the audit trail stays intact from the first E-House to the tenth.
Conclusion
Incomplete filler records stall E-House acceptance and future cable additions. A controlled sheet with one line per transit, grid mapping, and linked certificates fixes both. We supply matching documents.
Footnotes
1. ISO provides the international standards for technical product documentation and as-built documentation requirements. ↩︎
2. The IMO sets the international fire protection standards, including A-60 ratings for marine and offshore structures. ↩︎
3. UL is a leading global authority for testing and certifying firestop seal integrity and safety standards. ↩︎
4. Wikipedia provides a comprehensive technical overview of Multi-cable transit (MCT) systems and their components. ↩︎
5. The IEC manages the international IP Code standards used to define levels of ingress protection. ↩︎
6. The IATF is the official body for the IATF 16949 quality management standard for the automotive supply chain. ↩︎



 English
 Español de México
 Deutsch
 Français
 العربية
 Русский