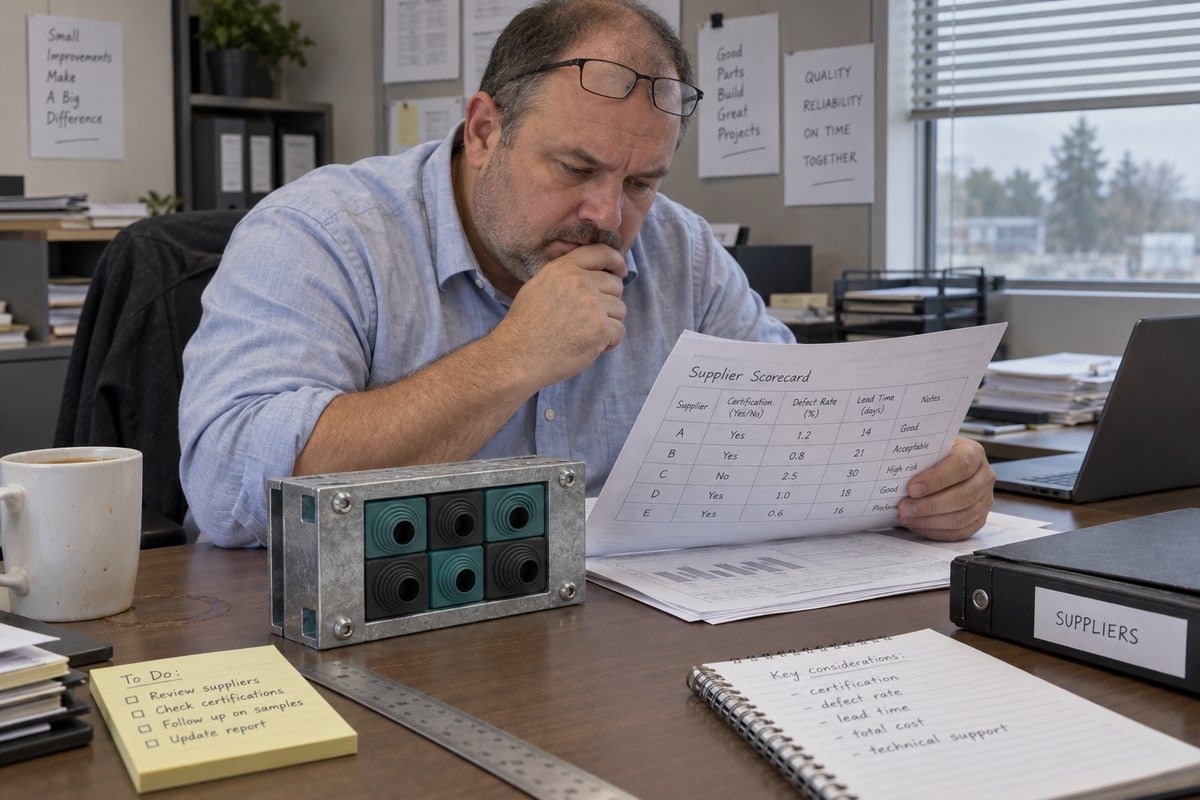
Last quarter a buyer sent our production line a frame drawing marked urgent second source. His incumbent multi cable transit supplier had slipped delivery twice, and nobody had a scorecard.
The metrics to evaluate multi cable transit suppliers are certification coverage (type approvals, fire, IP68, pressure test documents), dimensional compatibility with 120-frame cutouts, quality conformance and defect rate, on-time delivery and lead-time adherence, customization turnaround, technical support responsiveness, total cost of ownership, and supply resilience, weighted in a scorecard.
That list is the short version. Below I break each metric into documents you can request, dimensions you can measure, and numbers you can put in a spreadsheet. I write from the factory side, so I will also tell you where suppliers like us should be challenged.
What certifications and test documents should I request before qualifying an MCT supplier?
Every audit week our BV inspector 1 asks the same first question: show me the test report, not the brochure. That question is exactly what you should ask any MCT supplier.
Request ISO 9001 and IATF 16949 certificates, the type approval certificate (BV, DNV, or Lloyd's Register), A-0/A-60 fire integrity test reports, IP68 ingress protection reports, watertight and gastight pressure test data at 0.01–0.4 MPa, halogen-free material declarations, and ATEX/IECEx documentation for hazardous-area installations.
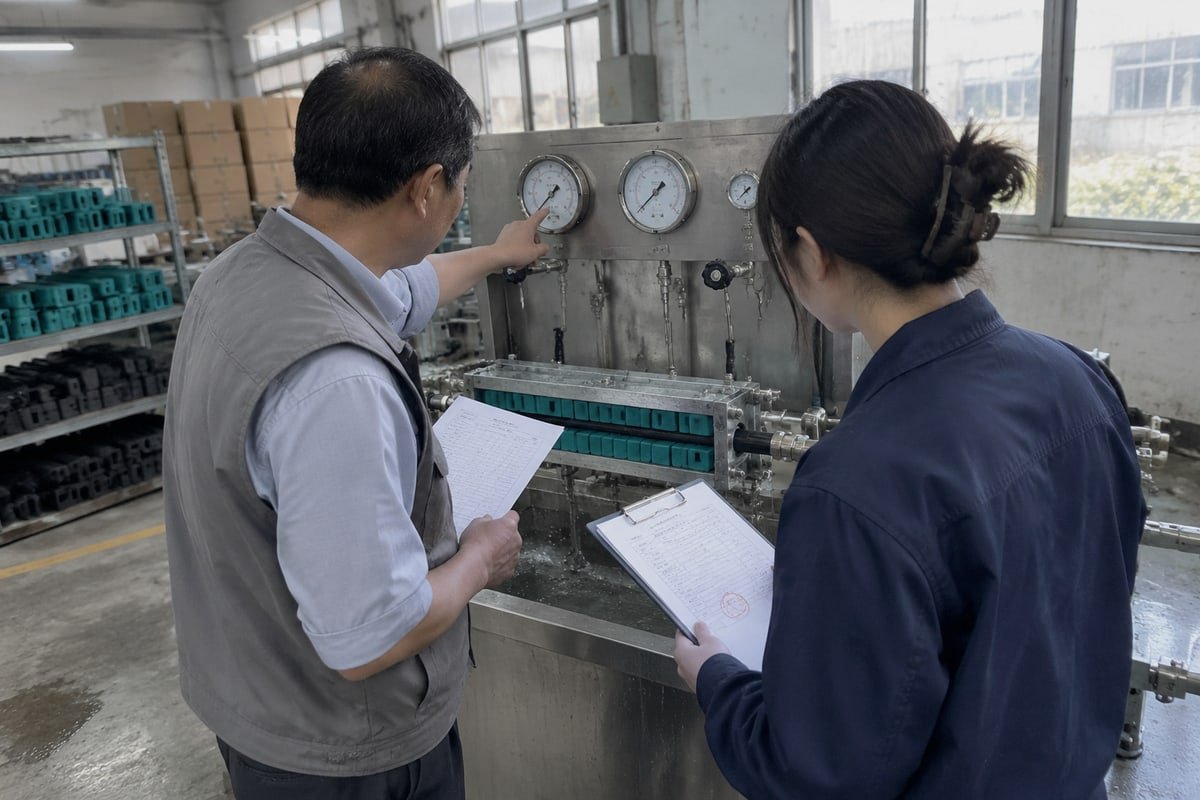
Certification is a gate, not a score. I put it in tier one of every supplier comparison. If a supplier cannot produce the document, its price does not matter yet. Once the gate is passed, the other metrics start to count.
The document pack to request
| Document | What it proves | What to check on the paper |
|---|---|---|
| ISO 9001 / IATF 16949 2 certificate | The quality system is audited by a third party | Scope covers sealing modules, valid dates, registrar name |
| Factory or product type approval (BV, DNV, Lloyd's Register) | An independent body has assessed the factory or product | Approval number, covered product range, expiry date |
| Fire test report, A-0 / A-60 | Fire integrity ratings for the tested bulkhead class | Test lab, frame size, module stack, and cable fill used in the test |
| IP68 report | Ingress protection when submerged | Depth, duration, module and frame size tested |
| Pressure test report, 0.01–0.4 MPa | Watertight and gastight seals hold under pressure | Test medium, hold time, leak acceptance criteria |
| Halogen-free material declaration | EPDM rubber meets halogen-free materials requirements | Test method used, batch traceability |
| ATEX / IECEx documentation | Suitable for hazardous zones | Zone category, and whether it covers the frame or the full assembly |
| CE / RoHS declarations | Regional compliance for Europe | Signed declaration, product list attached |
Match the test scope to your application
A fire report is tied to one tested configuration. It does not automatically cover every frame size or every module mix. So I always ask: which frame and which module stack were on the furnace? The same logic applies to pressure testing standards. A 0.4 MPa result on a round TSR assembly does not tell you how a large square TSC frame behaves. Ask for the report that matches your size.
Halogen-free materials matter most in BESS containers and modular data centers 3, where smoke toxicity is a design concern. For switchgear cabinets, ask whether the supplier offers an electromagnetic compatibility 4 version, or whether their modules are pure sealing modules. We answer that question honestly. Our step-core EPDM modules are designed for sealing, and we say so.
Calculate a certification coverage rate
Count the approvals your project requires. Count how many the supplier already holds. Divide. If you need eight documents and the supplier holds six, the coverage rate is 75%. Then decide which two are missing. ATEX and IECEx compliance 5 is mandatory for a Zone 1 platform. It is irrelevant for a data center corridor. Score accordingly.
From our side, we hold ISO 9001 and IATF 16949, a BV-approved factory, A-0/A-60 fire results, IP68, and pressure test data in the 0.01–0.4 MPa range. We send the test documents on request, before the quote if you prefer. For approvals outside that list, we tell you what we have and what we do not.
How do I verify dimensional compatibility with my existing 120-frame cutouts?
A sourcing manager in Germany once emailed us three photos of his existing frames and asked one question: will your modules fit? We answered with a cross-reference table and samples.
Verify compatibility by matching frame cutout dimensions, module width and height, stay plate thickness, and compression unit stroke against a model cross-reference table, then confirm with CAD/STEP files and free validation samples fitted into a spare 120-frame before ordering.
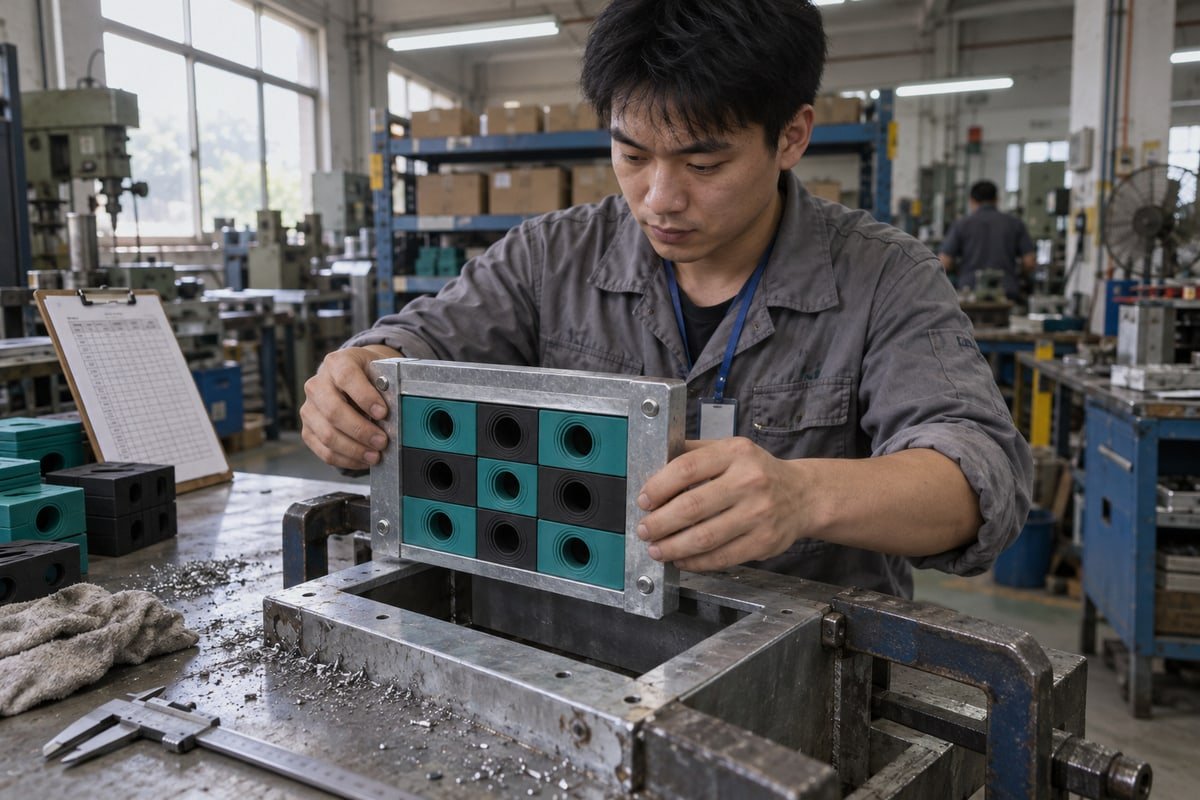
Compatibility is where drop-in second sourcing succeeds or fails. The good news is that it is fully measurable. Here is the sequence we run with buyers.
A five-step verification process
- Read the nameplates. Record the incumbent frame and module model numbers from the small metal plates between the compression bolts.
- Map the models. Use the supplier's cross-reference table (existing model → second-source model). If the supplier has no such table, that is a red flag for a claimed drop-in product.
- Compare the five critical dimensions. See the table below.
- Overlay the CAD. Request STEP files and drop them into your own frame model. Interference shows up in minutes.
- Fit physical samples. Put free validation samples, stay plates, and a compression unit into a spare frame. Measure before and after compression.
The five dimensions that decide fit
| Checkpoint | Why it matters | Question to ask the supplier |
|---|---|---|
| Frame inner opening (width × height) | The module stack must fill it exactly | Which 120-frame sizes does the table cover? |
| Module height steps | Layers must add up to the opening with room for compression | Do your height steps match the incumbent range one for one? |
| Stay plate thickness | Every plate adds to stack height | Is the plate thickness identical, or does the stack shift? |
| Compression unit stroke and bolt spacing | Compression must reach the tested sealing pressure | Do the bolts land on the existing frame holes? |
| Cable diameter range per module | Each module must accept the cables actually installed | What diameter range does one module size cover? |
Design flexibility and volumetric sealing density
Two extra metrics belong here. First, design flexibility: can a module accept a range of cable diameters without a change of module size? Our step-core modules peel down in layers, so one size adapts to several diameters. That reduces spare stock and supports later retrofits without frame replacement. Second, volumetric sealing density: how many cables pass per square inch of bulkhead. In a BESS container wall, space is scarce. A denser layout means fewer penetrations to weld, inspect, and fire-protect.
One mistake I see often: a buyer confirms the modules match and stops there. Then the stay plates arrive two millimeters thicker and the compression unit will not close. Check the whole stack, not just the rubber. Modular sealing systems are a system, and compatibility has to hold across every part in it.
What cost and lead-time benchmarks should I use to compare second-source suppliers?
When we quote a second-source package, we weigh two numbers: the unit price saving and the delivery date we can honestly commit to. Cheap and late helps nobody.
Benchmark second-source suppliers on landed unit cost savings of 40–60% versus incumbent pricing, on-time delivery rate, quoted versus actual lead time, customization turnaround, spare module availability, and total cost of ownership including freight, installation labor, rework risk, and warranty terms rather than unit price alone.
Procurement teams want numbers. Engineering teams want confidence. A weighted scorecard gives both sides the same sheet. I recommend keeping it to seven KPIs plus the certification gate from the first section.
A weighted scorecard for multi cable transit suppliers
| KPI | Peso | How to measure it | Benchmark to aim for |
|---|---|---|---|
| Landed cost saving vs incumbent | 20% | (incumbent price − landed second-source price) ÷ incumbent price | 40–60% on compatible drop-in modules |
| On-time delivery rate | 20% | Deliveries on or before confirmed date ÷ total deliveries | Take it from your ERP, not the supplier's claim |
| Lead-time adherence | 15% | Actual lead time ÷ quoted lead time on samples and first batch | No slip on the pilot order |
| Total cost of ownership | 15% | Unit + freight + duties + install labor + spares + rework + warranty exposure | Compare per installed frame, not per module |
| Customization turnaround | 10% | Days from your drawing to quote, and to a first custom sample | In-house mold making shortens this sharply |
| Technical support responsiveness | 10% | Hours to answer RFIs, CAD/STEP requests, and installation questions | Same or next business day, in English |
| Supply resilience | 10% | Number of production sites, buffered stock of spare sealing modules | More than one plant, spares on the shelf |
Resolving the two objections I hear most
The lowest-bid objection goes like this: MCT is a commodity, so buy the cheapest block that fits. My answer is that the cheapest block without a fire report is not a saving. It is a liability waiting for an inspector. The risk-focused objection goes the other way: price is secondary, so stay with the incumbent at any premium. My answer is that a certified, compatible second source removes the premium without adding risk. You do not have to pick one camp. The weights above let engineering push the certification gate and lead-time adherence, while procurement pushes cost saving and total cost of ownership.
Setting realistic lead-time benchmarks
Split lead time into two categories. Spare sealing modules in standard sizes should ship fast, because a good supplier stocks them. Custom frames need tooling time. We make molds in-house across our Shaanxi, Shandong, and Hunan sites, which is why customization turnaround is a metric we are comfortable being measured on. Ask any supplier the same question: where is the mold made, and by whom?
One more context point. Market reports project the MCT category growing at around 6.2% CAGR for 2026–2034. Growth brings more suppliers and more pressure on differentiation. That works in your favor, but only if you benchmark on hard data. Installation efficiency also belongs in TCO. Fewer module sizes to stock and faster fitting translate directly into labor hours you can count.
How can I validate performance and fit before committing to a full production order?
Our first large pilot order taught us this: a module that passes lab pressure testing can still leak if an installer overtightens the compression unit.
Validate with a staged pilot: fit free samples into a spare frame, run a witnessed pressure and IP68 water test on the assembled unit, check module dimensions against the drawing, install one production frame with your own crew, record torque and fit, then release a limited first batch.
Validation is where the scorecard meets reality. I prefer a staged approach, because each stage is cheap and each one can stop the process early. Here is the sequence we support for buyers.
The five validation stages
| Stage | What you check | Evidence you should receive |
|---|---|---|
| 1. Desk review | Certification coverage rate, cross-reference table, CAD/STEP overlay | Completed coverage sheet, drawings with your frame numbers |
| 2. Free sample fit | Modules, stay plates, and compression unit in a spare 120-frame | Fit report with measured dimensions and photos |
| 3. Bench test | Pressure test to your chosen pressure testing standards, IP68 immersion if required | Witnessed test record with medium, pressure, hold time, result |
| 4. Field pilot | One production frame installed by your own crew in a real cabinet or container | Torque values, installation time, installer notes |
| 5. Limited first batch | Incoming inspection on a small order | Defect rate, dimensional consistency data per batch |
What to measure during the pilot
Three numbers matter most. First, rejection rate at incoming inspection. Second, dimensional consistency of the sealing blocks across the batch, because rubber tolerances drift if the mold is worn. Third, installation efficiency in minutes per frame with your crew, not the supplier's crew.
Then ask about installation integrity auditing. Some buyers require formal verification of the final seal to keep the warranty valid. Ask whether the supplier reviews torque records and photos, or provides an installation checklist. Our technical support and engineering team does this remotely in English and supplies drawings for each frame.
Traceability is a growing request. At minimum, insist on a stamped nameplate and batch numbers on every module. If the supplier offers QR-coded modules for digital inspection logging, score it as a plus. For specialized environments such as semiconductor cleanrooms or aerospace, ask specifically for outgassing and ion contamination ratings. Most industrial projects do not need them, so do not pay for them by default.
Mistakes we see in validation
Skipping the field pilot is the most common one. A sample fit on a desk does not reveal an installer overtightening the bolts. The second mistake is testing a sample from one batch and then accepting production from another without inspection. The third is validating only the module and not the compression unit. Watertight and gastight seals depend on the whole stack reaching the right compression, so test the assembled unit.
Conclusion
Choose multi cable transit suppliers as risk partners: gate on certifications, verify 120-frame compatibility, benchmark cost and lead time, validate before volume. Request our cross-reference table and free samples.
Footnotes
1. Bureau Veritas is a primary authority for the factory audits and type approvals mentioned in the text. ↩︎
2. Official site for the automotive quality standard used as a benchmark for supplier qualification. ↩︎
3. Provides technical context for one of the primary applications where halogen-free MCT materials are required. ↩︎
4. Official IEC resource explaining EMC standards relevant to specialized cable transit sealing modules. ↩︎
5. The international standard for equipment in explosive atmospheres, critical for hazardous-area MCT installations. ↩︎



 English
 Español de México
 Deutsch
 Français
 العربية
 Русский