Hands-on sealing module training is often skipped in multi cable transit procurement. We see the result when installers call our factory support line after a leak. That rework is avoidable.
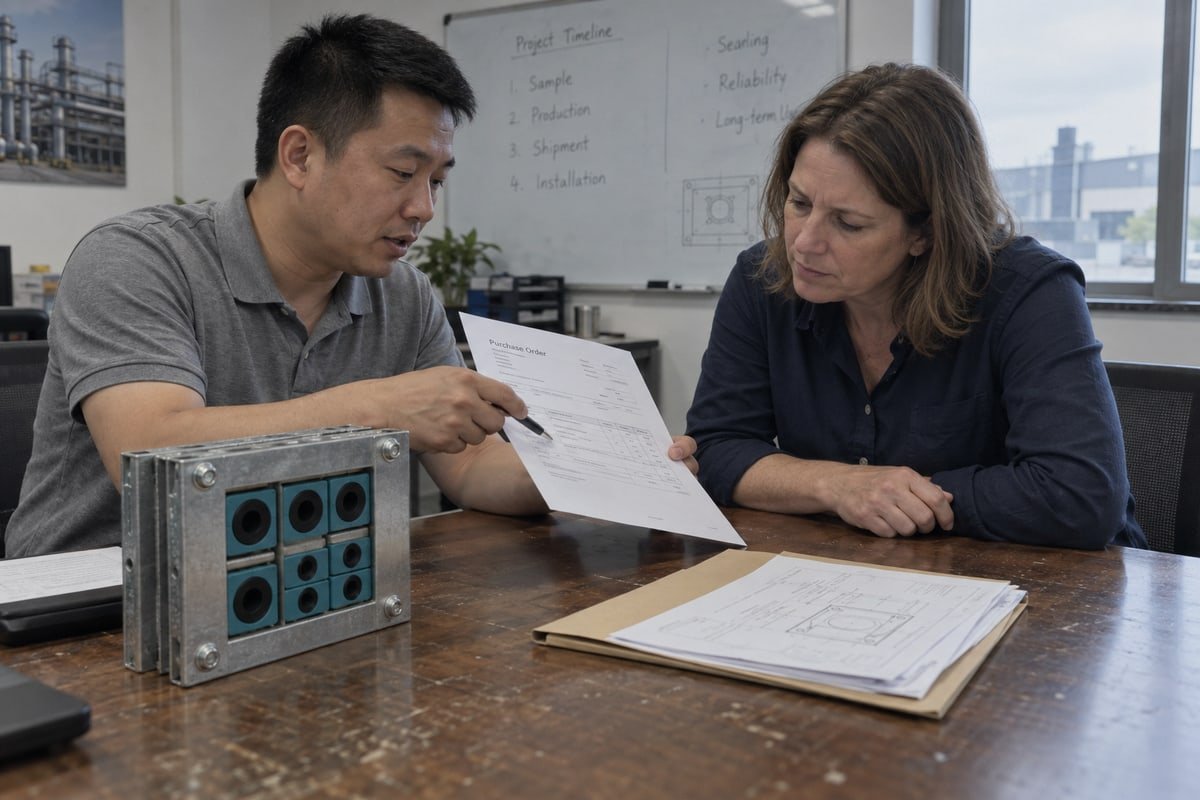
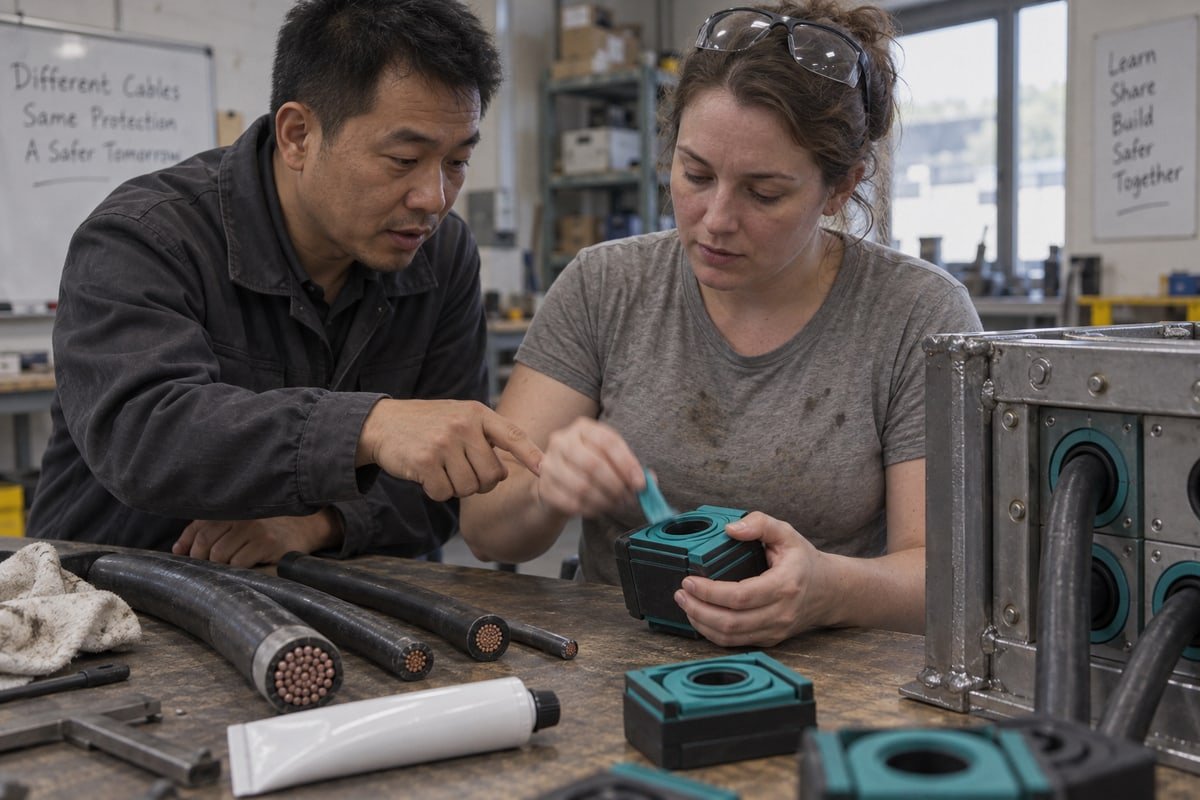
Arrange hands-on sealing module training by writing it into the purchase order before award: specify the trainer, format, attendees, agenda, and signoff documents. Schedule the session before first installation, run it on real frames and modules, and verify competence with a checklist-based mock installation.
Below, I walk through the four questions our buyers ask most. Each section gives you wording you can lift into an RFQ, a drawing note, or a purchase order.
How can I schedule a hands-on training session with the MCT manufacturer before placing my order?
A sourcing manager in Germany once asked us for training two weeks after his BESS containers 1 had shipped. For the first batch, that was too late.
Ask for training during the RFQ stage, not after the order. Request a written training offer alongside the quotation, tie the session date to your validation-sample approval or first delivery, and confirm attendees, location, and duration in the purchase order so the session is contractual.
The mistake I see most often is treating training as an after-sales service. It is not. It is part of installation quality assurance 2, and it belongs in the same document as the price and the delivery date. Here is the sequence we recommend to buyers who qualify us as a second source for cable transit frames and sealing modules.
A step-by-step procurement timeline
- RFQ stage. Add one line to your RFQ: "Quotation shall include a manufacturer-led hands-on sealing module training session, with duration, class size, and format stated." This forces every bidder to price it, so you compare like with like.
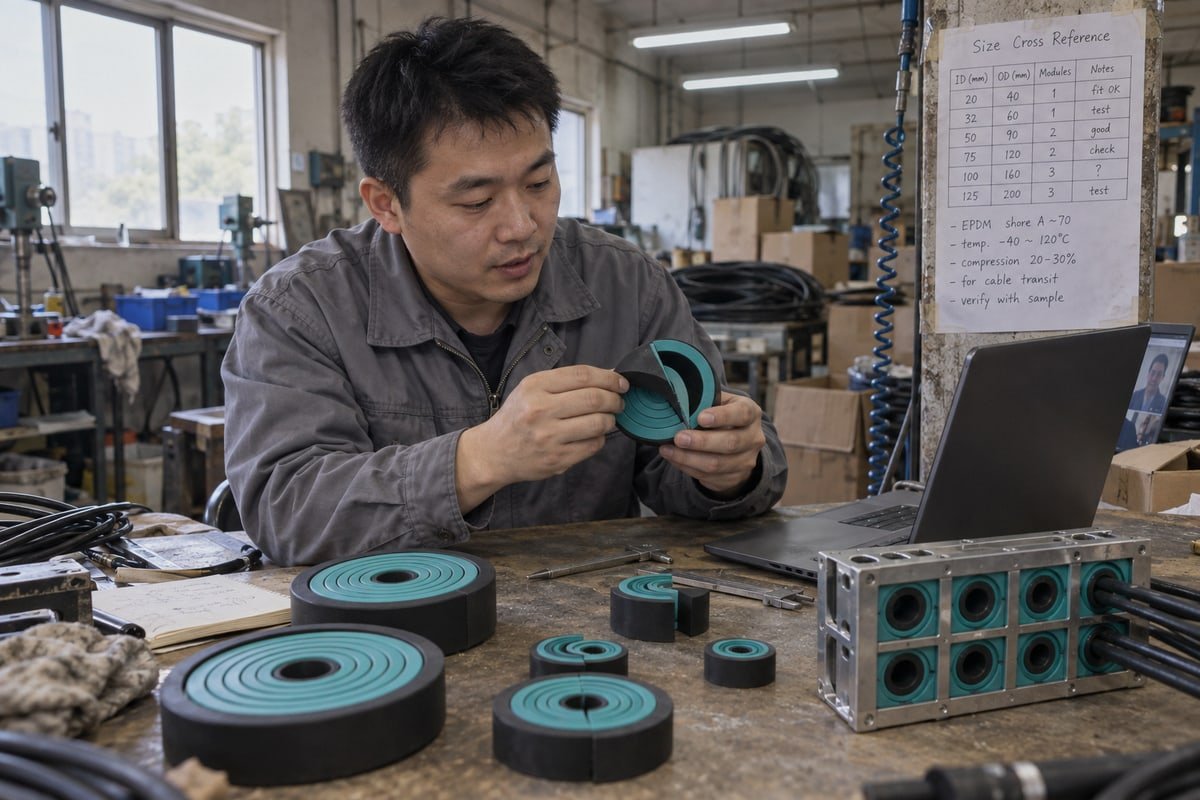
- Sample validation. When you receive free validation samples and the model cross-reference table, use the same samples for a short pre-training walkthrough. Our engineers do this by video call so your team sees how the step-core EPDM module peels to fit a cable diameter.
- Purchase order. Name the trainer role, the site, the date window, the maximum class size, and the deliverables. Make training completion a contractual KPI. Link a small payment milestone to it if your procurement rules allow.
- Before mobilization. Hold the session at least one week before the first installation crew touches a frame. The crew practices, makes mistakes, and corrects them on a training frame, not on your fire-rated bulkhead.
- Repeat for re-entry. Cable changes and retrofits are common over a system's life. Book a shorter refresher when the maintenance team takes over.
| Procurement stage | Training action | Owner |
|---|---|---|
| RFQ | Request written training offer with duration and class size | Buyer |
| Sample validation | Video walkthrough on validation samples | Manufacturer engineer |
| Purchase order | Training scope, date, attendees, and signoff written in | Buyer and supplier |
| Pre-mobilization | Hands-on session on real frames and modules | Trainer and crew |
| Commissioning | Competence checklist and inspection record filed | QA/QC |
| Maintenance handover | Re-entry refresher | Maintenance team |
Who should attend
Do not limit the room to electricians. Instrumentation teams, supervisors, QA/QC inspectors, and any local subcontractor who will pack a module should attend. A published course example for transit packing installation runs three hours with a maximum class size of eight. That size is realistic. It allows every person to handle a compression wedge kit, not just watch one.
Some procurement teams push back here. They want minimal training to save schedule days and cost. In my experience, that saving is small next to the cost of opening a leaking transit in a live switchgear room. A three-hour session costs less than one day of rework.
What should I ask the supplier to cover during sealing module installation training?
On our Shaanxi line, every TSC module batch gets a compression check before packing. The field failures we hear about rarely involve the rubber. They involve the wedge.
Ask the supplier to cover workspace preparation, straight cable routing, module adaptation by peeling layers, lubrication, stacking order from the transit plan, stayplate placement, wedge tightening, compression checks, post-installation inspection, re-entry procedures, and the tools involved. Insist on live practice with real frames and modules, not slides.
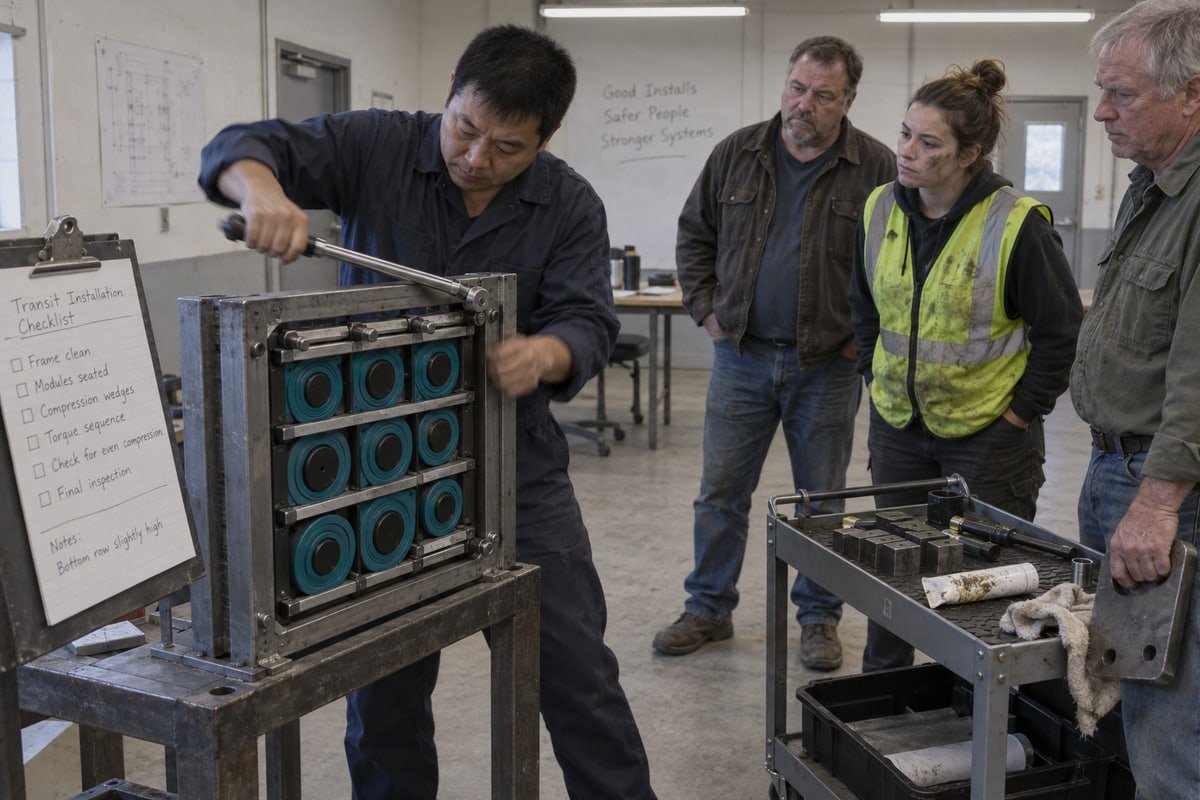
A slide deck teaches theory. A frame on a bench teaches feel. When we run certified installer training, we hand each attendee a frame, a full set of modules, stayplates and lubricants, and a wedge. Then we watch. The agenda below is what a field-ready session should contain, in the order the work actually happens.
The agenda, step by step
| Training block | What the crew practices | The error it prevents |
|---|---|---|
| Workspace preparation | Confirm the opening is accessible, all components are on hand, and the area is clear | Missing parts mid-pack, damaged modules |
| Cable routing | Pull cables straight through the frame, no angled entry | Side load on modules, loss of watertight integrity |
| Module adaptation | Peel step-core layers until a small, even gap remains around the cable | Oversized or undersized module, leak path |
| Lubrication | Apply lubricant to module faces, not the cable jacket | Modules that will not seat or slide during compression |
| Stacking order | Place modules per the transit plan, row by row | Wrong layout, blank modules missing |
| Stayplates | Insert a stayplate between every row | Rows shifting under compression |
| Wedge tightening | Tighten the compression wedge fully, using the correct tool | Under-compression, failed gas-tight sealing |
| Inspection | Check compression, gap, wedge position, and nameplate | Undetected defects at commissioning |
| Re-entry | Release, remove one module, re-adapt, re-pack | Damage during cable additions |
Tools the crew must handle
Ask the supplier to bring the module holder tool, the compression wedge kit, and any pre-compression jack or wedge puller used for larger frames. Tool handling is where slides fail. A wedge that stops one turn short looks finished and is not. The trainer should show what "fully tightened" looks like and let each attendee reach it.
Cross-brand awareness
Experienced contractors sometimes tell me sealing modules are simple. They have packed one brand and assume the next behaves the same. Our modules are dimensionally compatible with common 120-frame standards, so they drop into existing cutouts. But peel depth, lubricant type, and wedge torque feel still differ between suppliers. Ask the trainer to state these differences explicitly. Familiarity with cables is not the same as familiarity with the system.
If your project uses digital transit management software or AR overlays of packing plans, ask the trainer to use them during the session. They help with documentation. They do not replace the wedge in the hand.
Can I request training on-site at my facility or only at the factory?
We weigh one trade-off on every training request: a factory session shows our test rigs and molds, but an on-site session shows your real cutouts and cable bundles.
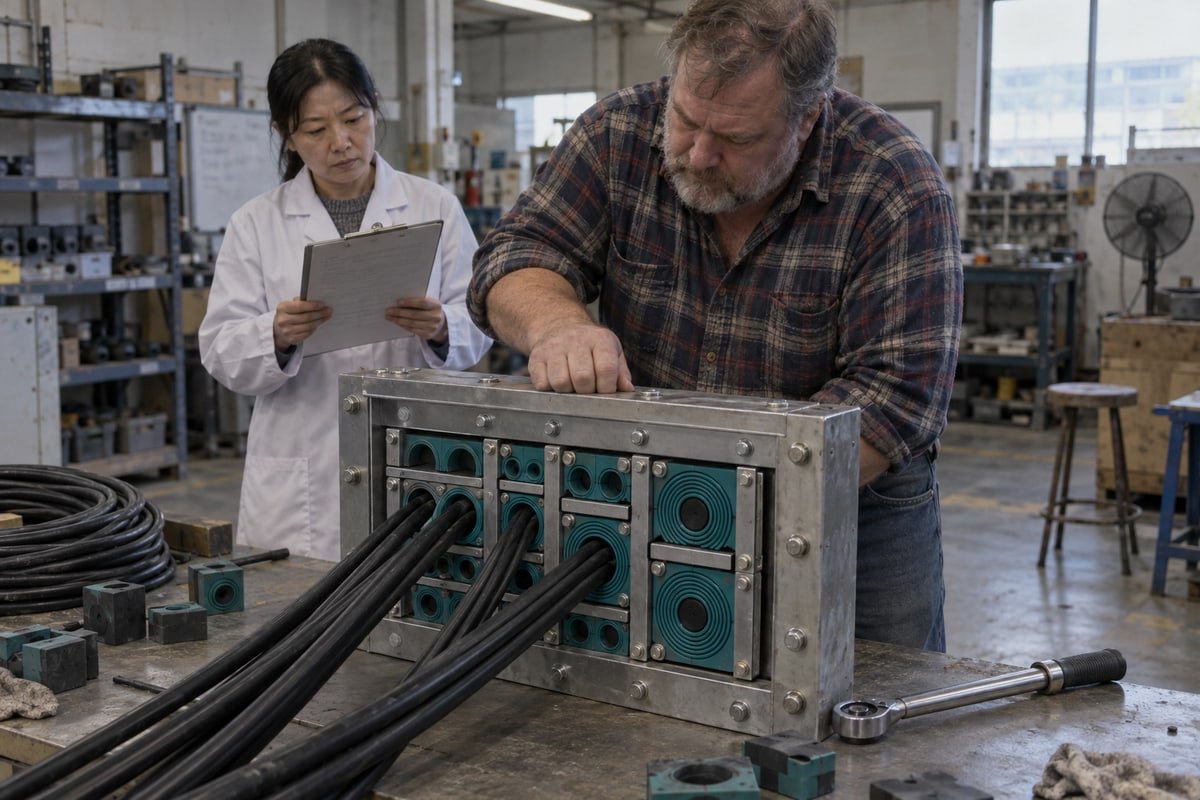
You can request either. Most MCT manufacturers deliver training on-site at your facility, at the factory, or in a blended format with web modules first and hands-on practice later. On-site is best for first installations because it uses your frames, cutouts, and cables.
Both options are legitimate. The right one depends on where the risk sits in your project. Here is how I frame it for buyers in Europe, Asia-Pacific, and the Middle East.
Comparing the three formats
| Format | Best for | Strengths | Limits |
|---|---|---|---|
| On-site at your facility | First installation, multiple subcontractors, complex bulkheads | Real cutouts, real cable bundles, real site conditions, whole crew present | Travel lead time, needs a clear workspace booked |
| At the factory | OEM integrators qualifying a second source, QA engineers | See mold making, fire and IP68 test setups, discuss custom sizes | Crew rarely travels, so field installers miss it |
| Blended (web first, then hands-on) | Distributed teams, repeat projects, maintenance refreshers | Crew arrives knowing the basics, field time spent practicing | Web portion alone is not enough for compression and tool handling |
Why we push on-site for the first job
On-site technical support is now a standard service across this market, not an extra. That trend exists for a reason. Watertight integrity depends on cables entering the frame straight, and that depends on how your tray, gland plate, or container wall is actually built. A trainer standing at your bulkhead sees the bend radius 3 problem. A trainer at a factory bench does not.
On-site sessions also standardize technique across subcontractors. In a modular data center 4 or a BESS container line, three crews may pack transits in one week. If each learned from a different video, you get three compression standards and one fire rating on paper. One shared session fixes that.
The digital objection
Buyers sometimes ask why they should pay for travel when web training is faster and cheaper. My answer is that digital training should supplement, not replace, hands-on instruction. Send the web modules two weeks ahead. Then use the on-site hours for peeling, lubricating, stacking, and tightening. The crew learns basics at their desk and skills at the frame.
For factory visits, we host sourcing and QA engineers at our plants. They see in-house mold making for custom frame sizes, review CAD and STEP files, and watch a pressure test. That builds supplier confidence. It does not build installer competence. Book both if the project justifies it, but never skip the on-site half.
What documentation or certificates should I receive after completing sealing module training?
One lesson from exporting to EPC projects in the Middle East: a training certificate without an attached inspection checklist rarely satisfies the QA department.
You should receive a named attendance certificate per installer, a signed competence checklist from the mock installation, the manufacturer's installation manual and transit plans, an MCT inspection checklist for QA, and copies of product test documents such as fire, IP68, and pressure-tightness reports.
A certificate is evidence that someone attended. It is not evidence that someone can pack a transit. Your QA/QC team needs both, plus the product documents that make the training meaningful. This is the package we assemble for buyers, and it is what I would demand from any supplier.
The full document package
| Document | Who needs it | Why it matters |
|---|---|---|
| Attendance certificate, named per installer | Site manager, subcontractor records | Proves who received certified installer training and when |
| Signed competence checklist | QA/QC, EPC quality manager | Shows each person completed a mock installation to the manufacturer's method |
| Installation manual and transit plans | Installers, supervisors | Defines stacking order, blank modules, and stayplate positions per frame |
| MCT inspection checklist | QA/QC inspectors | Gives pass/fail criteria for gap, lubrication, wedge position, and nameplate |
| Photo record template | Installers, QA | Captures each packed frame before and after compression |
| Product test documents | Procurement, engineering, insurers | Fire rating A-0/A-60, IP68, watertight and gas-tight sealing at 0.01–0.4 MPa |
| Model cross-reference table | Procurement, maintenance | Maps existing modules to drop-in equivalents for future spares |
What the competence signoff should contain
Ask the trainer to sign against specific observed actions, not a general statement. The checklist should record that the installer routed cables straight, peeled to a small even gap, lubricated correctly, placed stayplates between rows, tightened the wedge fully, and completed a re-entry. If any step was corrected during the session, note it. That record protects your project during commissioning disputes.
Linking training to product certification
Fire-rated cable seals only deliver their rating when installed to the tested method. Our factory runs ISO 9001 and IATF 16949 5 systems and is BV-approved, and we provide fire, IP68, and pressure test documents on request. Those documents describe a correctly packed transit. The competence checklist is the bridge between the test report and your bulkhead. Ask the supplier whether warranty conditions reference trained installers, and file both documents together.
Your own QA team should also learn independent verification. Non-destructive techniques such as ultrasonic leak detection let inspectors audit gas-tight sealing without opening the frame. Ask the trainer to demonstrate one method on the training frame. If the project uses digital transit management software, request that the completed checklist and photos be uploaded per frame, so every cable entry has a traceable record for the next re-entry.
Conclusion
Untrained hands turn a certified fire-rated seal into a liability. Write hands-on sealing module training, attendance, inspection, and signoff into the purchase order, and we will support that scope from day one.
Footnotes
1. Official US Department of Energy resource on battery storage infrastructure and safety. ↩︎
2. International standards for quality management and assurance in industrial installation processes. ↩︎
3. Technical definition of the minimum radius a cable can be bent without damage. ↩︎
4. Overview of modular construction techniques where cable transits are frequently utilized for sealing. ↩︎
5. Global quality standard for the automotive industry, ensuring manufacturing consistency. ↩︎



 English
 Español de México
 Deutsch
 Français
 العربية
 Русский