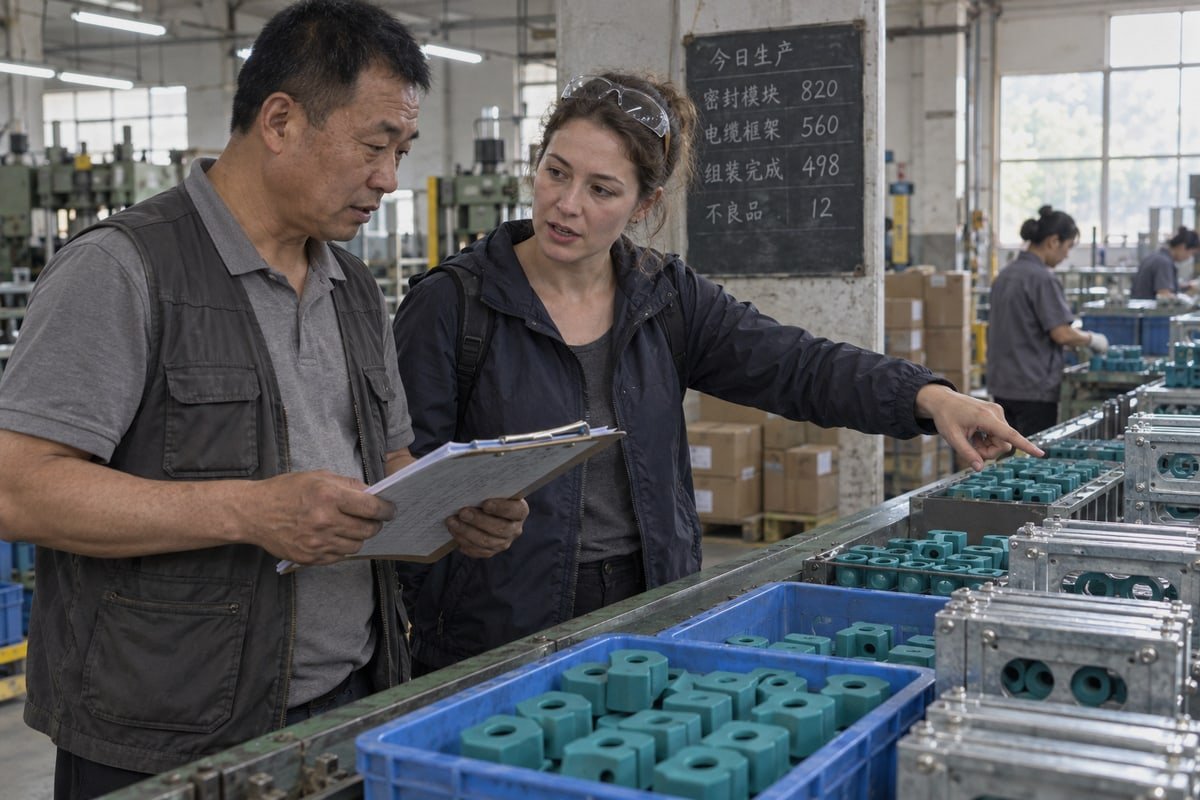
Twice last year, buyers reached our factory after a primary vendor missed a BESS deadline. Assessing a supplier’s production capacity for multi cable transits 1 early beats firefighting later.
Assess a supplier’s production capacity for multi cable transits by comparing claimed output with demonstrated output: request 8–12 weeks of production records, identify the bottleneck station, check certifications and sub-tier material supply, verify OTIF lead-time history, and confirm drop-in fit with drawings and samples before a pilot order.
That is the short version. The rest of this article walks through each step in order. I will cover the factory data to ask for, the certifications that matter, how to test lead time reliability, and which documents prove a module will actually fit your existing frame.
How can I verify a supplier's production capacity claims with real factory data?
During a customer audit at our Shaanxi plant, the visiting engineer ignored our brochure and stood at the compression-unit assembly station with a stopwatch for an hour.
Verify production capacity claims by requesting the last 8–12 weeks of work orders, quality release records, and shipment logs for the exact MCT product family, then reconcile them with staffing schedules, shift patterns, equipment lists, and machine-hour math (usable machines × working hours) adjusted for downtime and testing.
That engineer had the right idea. A brochure tells you what a plant could do in theory. A stopwatch at the slowest station tells you what it does today. Production capacity for multi cable transits lives at the process level, not at the plant level. An MCT order is not a bag of parts. It is a frame, a set of sealing modules, stay plates, a compression unit, and a test step. Each of those has its own rate.
Four kinds of capacity, and which one you should pay for
Most capacity arguments come from mixing up four different numbers. I ask buyers to separate them before they compare quotes.
| Capacity type | What it means | How to check it |
|---|---|---|
| Claimed | The number on the supplier's website or RFQ reply | Ask which product family and frame size it refers to |
| Planned | What the line could produce with full staffing and no faults | Machine-hour math: usable machines × working hours |
| Committed | Capacity already reserved for other customers | Ask for open order backlog by month |
| Demonstrated | What actually shipped over the last 8–12 weeks | Shipment logs, quality release records, work orders |
Demonstrated capacity minus committed capacity is the only figure that predicts your delivery. Everything else is a forecast.
Evidence to request instead of claims
Some suppliers push back and say annual plant output is enough to judge readiness. I disagree, and so does most procurement guidance. Plant size hides the bottleneck. A factory with large molding capacity can still be limited by seal insertion, dimensional verification, or leak testing. So I ask for evidence tied to the constraint step.
| Evidence | Why it matters for MCTs |
|---|---|
| Process flow with station rates | Shows where work queues up, usually final assembly or testing |
| Actual vs. theoretical line speed | Reveals the gap between planned and real production throughput |
| Staffing schedule and shift pattern | Confirms whether the rate assumes one shift or three |
| Equipment list and maintenance records | Backup presses and molds reduce downtime risk |
| Utilization rate or OEE data | Shows how much headroom exists for your order |
Confidentiality is a fair concern. When a buyer cannot see raw records, I offer redacted or aggregated data. The rule stays the same: the proof must connect to real throughput for the exact TSR or TSC module size you are buying, not for a "similar" product.
Ask where the queue forms
Three questions expose the true constraint quickly. Which station limits daily output? What happens during rework or mold maintenance? Does the quoted rate include inspection and pressure testing 2 time? A supplier who omits test time from the capacity claim is quoting parts, not qualified fire-rated penetration seals. Larger factories now run digital twin simulations of a project BOM to find these bottlenecks before production starts, and some offer a real-time OEE dashboard during critical runs. Those tools are useful, but they only help if the underlying station data is honest.
What certifications and quality systems should I check before qualifying an MCT supplier?
Every quarter we weigh the same trade-off: keep IATF 16949 and BV audit costs on the books, or cut them and quote a few percent lower. We keep them.
Check for an ISO 9001 quality management system (IATF 16949 for automotive-grade discipline), third-party factory approval such as Bureau Veritas, and product test evidence: A-0/A-60 fire rating, IP68 ingress protection, and watertight/gas-tight pressure results, plus marine approvals like ABS, DNV, or Lloyd's Register where the project requires them.
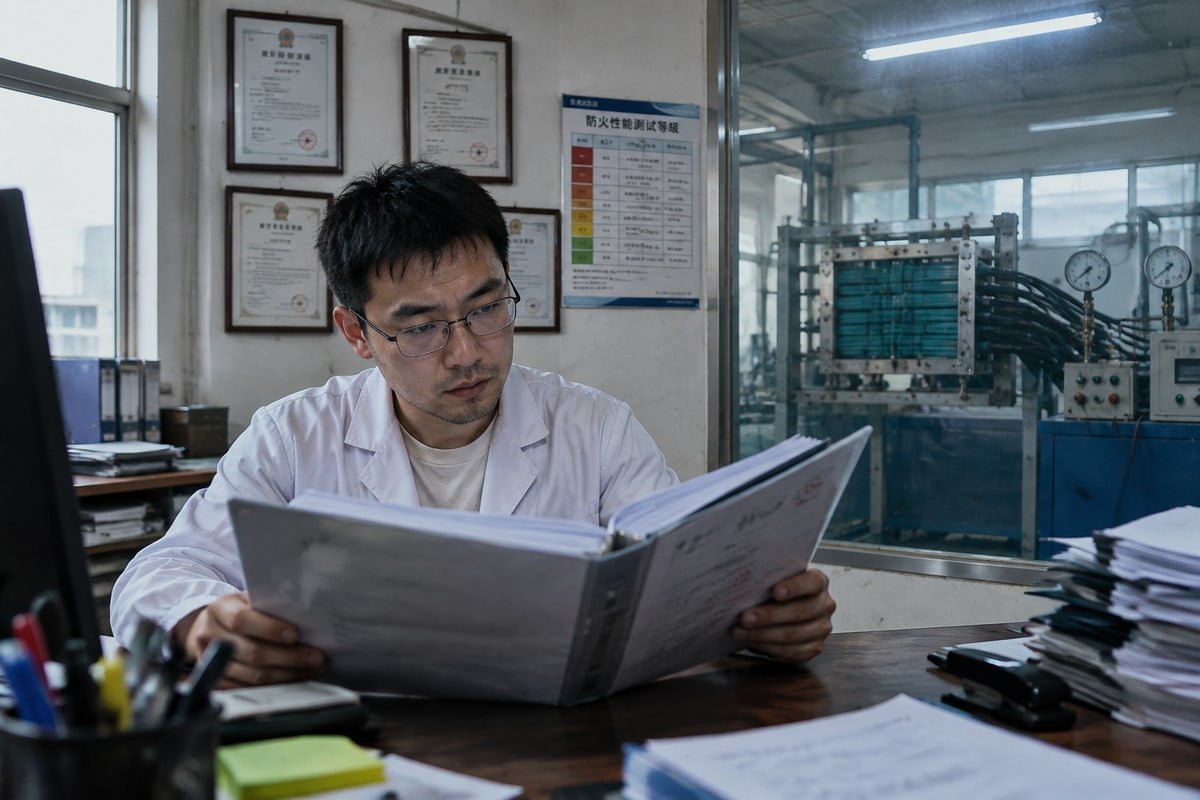
The reason we keep those systems is simple. Capacity without process control 3 is just faster scrap. A supplier who can build a thousand modules a week but cannot hold rubber hardness within tolerance will hand you a thousand leak risks. So certification and capacity have to be assessed together.
System certifications versus product test evidence
I separate the paperwork into two groups. The first group proves the factory runs a controlled process. The second group proves the product performs.
| Document | What it proves | What to ask for |
|---|---|---|
| ISO 9001 | A working quality management system with corrective action loops | Current certificate, scope statement covering MCT products |
| IATF 16949 | Automotive-level process discipline, PPAP-style documentation, Cpk tracking | Evidence the scope includes sealing modules, not only unrelated parts |
| Third-party factory approval (e.g. BV) | An external body has audited the plant, not just the office | Approval certificate with factory address matching the production site |
| Fire test report (A-0 / A-60) | The transit maintains the bulkhead or deck fire division | Full test report, not just a summary page |
| IP68 and pressure test (0.01–0.4 MPa) | Watertight and gas-tight sealing under defined pressure | Test method, test pressure, module size tested |
| Class approval 4s (ABS, DNV, Lloyd's Register) | Authorization for maritime and offshore safety-critical use | Confirm whether your project scope actually requires them |
For a BESS container or a modular data center 5, the fire and IP68 documents usually carry the most weight. For offshore or shipyard work, class approval becomes mandatory. Ask which technical compliance standards your end customer will audit, then match the certificate list to that.
Process capability and inspection depth
Certificates are a snapshot. I also look at how the supplier controls the molding and extrusion steps day to day. Process capability indices such as Cpk on module dimensions and rubber hardness tell you whether sealing performance stays consistent across a large batch. Material traceability matters too. Each batch of halogen-free EPDM compound should trace back to a compound lot and a mixing record. If a module fails on site two years later, that trail is the only way to find the root cause.
Inspection method is worth a question as well. Manual visual checks catch surface defects. Automated optical inspection, increasingly AI-assisted, can flag internal voids or surface irregularities in rubber modules 6 that a human eye misses. Not every factory needs it, but a supplier who knows their own escape rate is one who has measured it.
Questions I would put on a factory audit checklist
- Does the certificate scope name the MCT product family?
- Who signs off on quality release, and what does the release record contain?
- Can you show a Cpk study for a module dimension and a hardness value?
- How does material traceability work from compound lot to shipped carton?
- Which fire, IP, and pressure test documents are available on request?
How do I evaluate lead time reliability and scalability for large or recurring orders?
A sourcing manager for a modular data center builder once asked me a blunt question: "What happens to my lead time when your biggest customer doubles their order?"
Evaluate lead time reliability by reviewing historical on-time-in-full (OTIF) performance, equipment load rates, and planned-versus-committed capacity, then test scalability with a pilot order, questions about multi-site production, sub-tier buffer stocks for EPDM and stainless steel, and a written contingency plan for downtime, labor gaps, and material shortages.
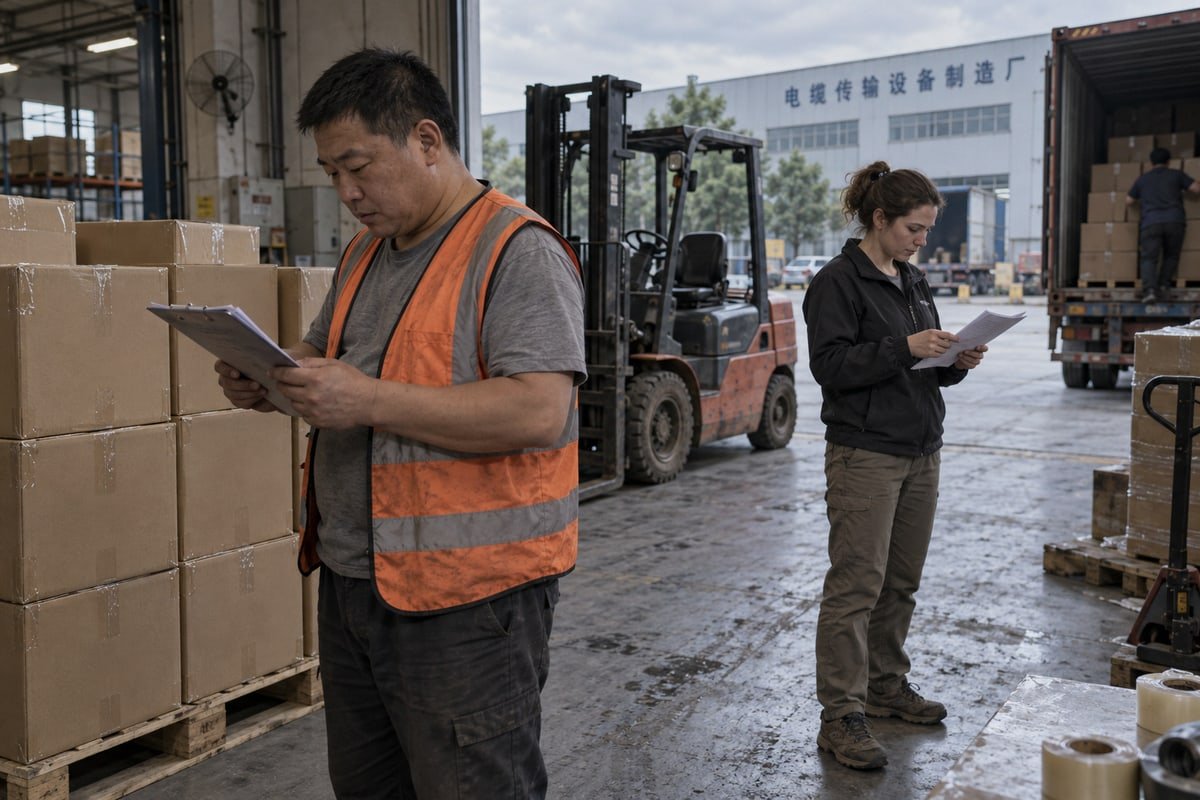
It was a fair question, and it deserved a structured answer rather than reassurance. Manufacturing lead times for modular sealing solutions depend on three things: how loaded the line already is, how quickly materials arrive, and whether the supplier has a second place to build. I answered with our Shandong and Hunan production sites and our open order backlog, not with adjectives. Any supplier you qualify should be able to do the same.
A five-step method for testing lead time reliability
- Define your demand profile. Split it into normal volume, peak volume, and growth volume. State the product mix: frame sizes, module variants, and any custom parts. Capacity for MCTs depends on mix more than on unit count.
- Request OTIF history. Ask for on-time-in-full performance over the last two or three quarters, ideally for orders of similar size. One late order is noise. A trend is data.
- Check planned versus committed capacity. Ask what portion of the next quarter's line time is already reserved. The gap is what your order competes for.
- Audit the sub-tier chain. Ask for buffer stock levels and replenishment lead times for specialized elastomers, stainless steel frames, inserts, and fasteners. If a shared sub-tier vendor serves several customers, that constraint belongs in your capacity estimate.
- Run a pilot order. Place a small but realistic order with the same mix as production. Measure delivered throughput against promised throughput, and record the defect rate at incoming inspection.
Metrics that separate a reliable supplier from a fast talker
| Metric | What a strong answer looks like | Red flag |
|---|---|---|
| OTIF rate | A number, by quarter, with root causes for misses | "We are always on time" |
| Equipment load rate | Load by station, with headroom stated | One plant-wide percentage |
| Committed capacity | Backlog by month for your product family | No breakdown by product |
| Sub-tier lead times | Named material categories with weeks and buffer stock | "Our suppliers are reliable" |
| Contingency plan | Backup molds, second site, overtime policy, alternate compound source | No clear answer on shifts or backup equipment |
The speed-versus-rigor objection
Buyers often tell me the RFQ deadline does not allow a full capacity audit. I understand the pressure. My suggestion is to scale the audit to the risk. A one-off spare module order needs a document check. A recurring order feeding a container assembly line needs the pilot. Supply chain scalability is much cheaper to verify with a small trial than to discover during a production ramp. In our experience exporting to Europe and the Middle East, the pilot order also shakes out export documentation and packaging issues before they affect a real schedule.
What documentation should I request to confirm dimensional compatibility and drop-in fit?
Our hardest lesson came early: a module can pass every seal test and still fail at site because the frame cutout is a few millimetres off. Now drawings come first.
Request 2D drawings and CAD/STEP files for frames, modules, stay plates, and compression units; a model cross-reference table mapping your existing part numbers to the alternative; a 120-frame compatibility statement with tolerances; material and hardness data sheets; and free validation samples for a trial fit in your frame.
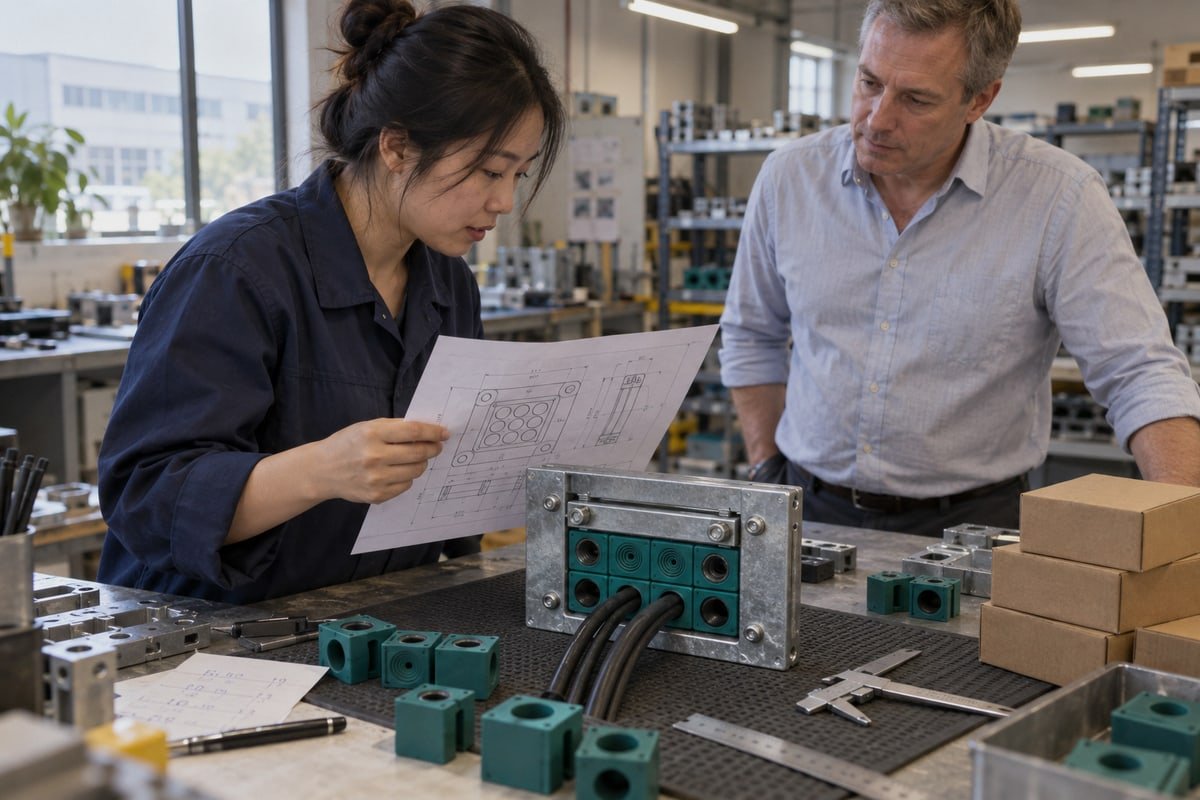
Compatibility is where capacity assessment turns into a real purchasing decision. A second source only saves money if the module drops into the existing frame without a redesign. Our TSC square modules and TSR round assemblies are built to be dimensionally compatible with common 120-frame standards, and the reason we can say that with confidence is the document set below. I would ask any supplier for the same set.
The document package that proves drop-in fit
| Document | Purpose | What to check |
|---|---|---|
| 2D dimensioned drawings | Confirms module width, height, depth, and cable diameter range | Tolerances stated, not just nominal sizes |
| CAD / STEP files | Lets your engineers test fit in the frame model | File matches the drawing revision |
| Model cross-reference table | Maps your current model numbers to the supplier's equivalents | Every part in your BOM has a match |
| 120-frame compatibility statement | Written commitment that modules fit standard frame cutouts | Names the frame standard and stack dimensions |
| Material data sheet | Confirms halogen-free EPDM, hardness, and temperature range | Aligns with your fire and IP requirements |
| Free validation samples | Physical trial fit and compression check | Same production tooling as the future order |
Why module design affects the number of parts you need to qualify
One detail often gets missed during qualification. Step-core modules let one module size adapt to a range of cable diameters by peeling layers. That reduces the number of variants you have to approve, stock, and reorder. It also reduces changeover on the supplier's side, which feeds straight back into capacity. Fewer variants means longer runs, fewer mold changes, and more predictable production throughput.
Custom sizes and non-standard penetrations
Standard frames cover most cases, but not all. For odd cutouts, ask about custom engineering capabilities. In-house mold making shortens the path from drawing to sample because no outside toolmaker sits in the loop. Some suppliers also use 3D printing to prototype custom frame geometries and check fit before committing to steel tooling. That approach cannot replace the production mold, but it can save weeks of tooling lead time on niche applications. Ask how the supplier handles a custom request end to end: who reviews the drawing, who cuts the mold, and who signs off the first article.
Turning the package into a qualification decision
My suggested sequence is short. Receive the cross-reference table and confirm every BOM line has a match. Load the STEP files into your frame model. Order validation samples and fit them in a real frame with real cables, then torque the compression unit and check the seal. Only after that, place the pilot order. Done in that order, a second source can cut component cost by 40–60% without losing certification or fit, which is the whole point of the exercise.
Conclusion
Unverified capacity claims cause missed deadlines. Missed deadlines stall containers and panels. Verify production capacity for multi cable transits with records, certificates, OTIF data, drawings, and a pilot order.
Footnotes
1. Authoritative encyclopedia entry defining the multi cable transit (MCT) product category. ↩︎
2. Official site for UL, an authority on safety testing and certification for industrial components. ↩︎
3. Official homepage of the International Organization for Standardization for quality management principles. ↩︎
4. Official site for DNV, providing standards for maritime and offshore safety certifications. ↩︎
5. Technical background on modular data centers, a primary application for cable transit systems. ↩︎
6. Authoritative Wikipedia entry that explicitly defines and describes rubber modules in the context of cable transits. ↩︎



 English
 Español de México
 Deutsch
 Français
 العربية
 Русский