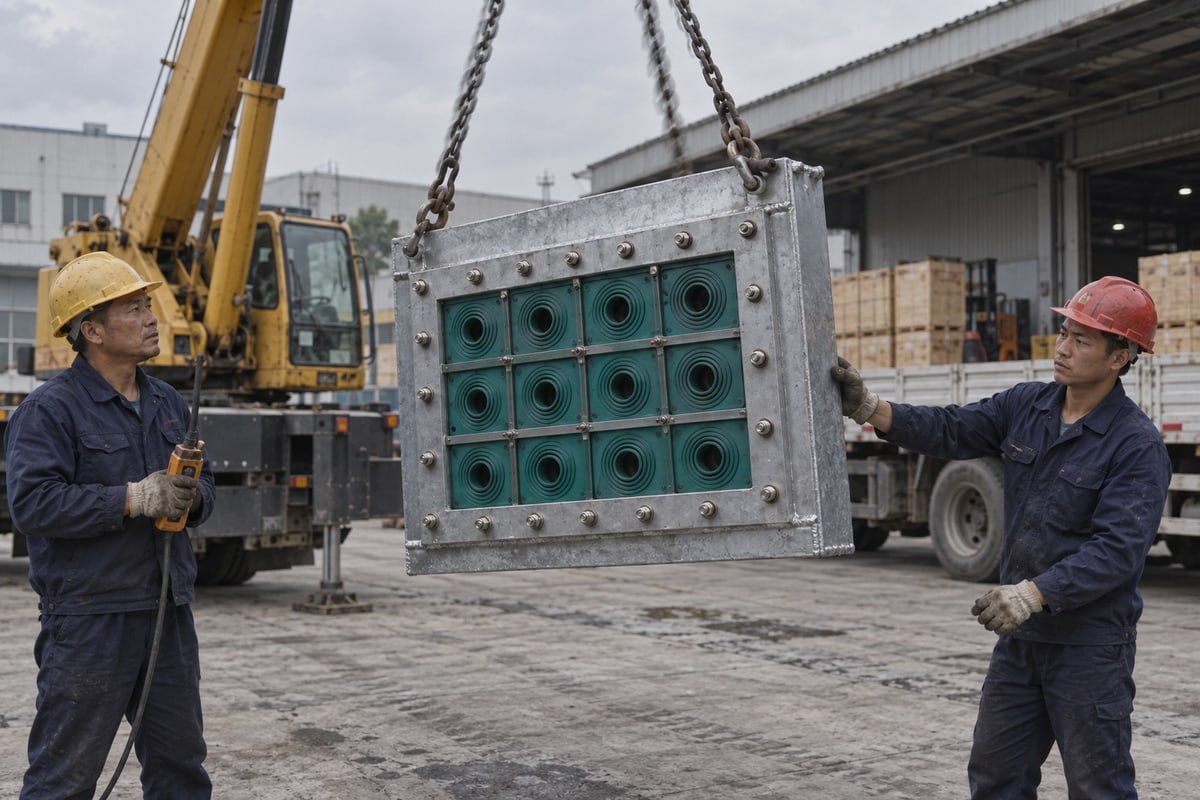
A multi cable transit frame that ships intact but leaks after a crane lift is a costly surprise. We have seen it on our loading dock, and it is preventable.
Confirm a multi cable transit frame by testing the complete assembly under realistic lifting loads and shock and vibration profiles, then inspecting for cracks, bolt preload loss, module movement, and leakage. Request the test report, material certificates, and post-test seal results before ordering.
The rest of this article walks through what to ask for, what to test yourself, and how to compare a second-source frame against the one you already use.
What Test Documents Should I Request to Verify Vibration and Shock Resistance Before I Order?
One lesson from years of exporting our sealing systems: the phrase "vibration tested" on a datasheet tells you almost nothing until you see the actual report behind it.
Request the full shock and vibration test report showing method, frequency range, acceleration, duration, and axes; confirmation the test covered the complete frame assembly; post-test leak and retention results; bolt torque retention data; and material and weld certificates. Generic datasheet claims are not evidence.
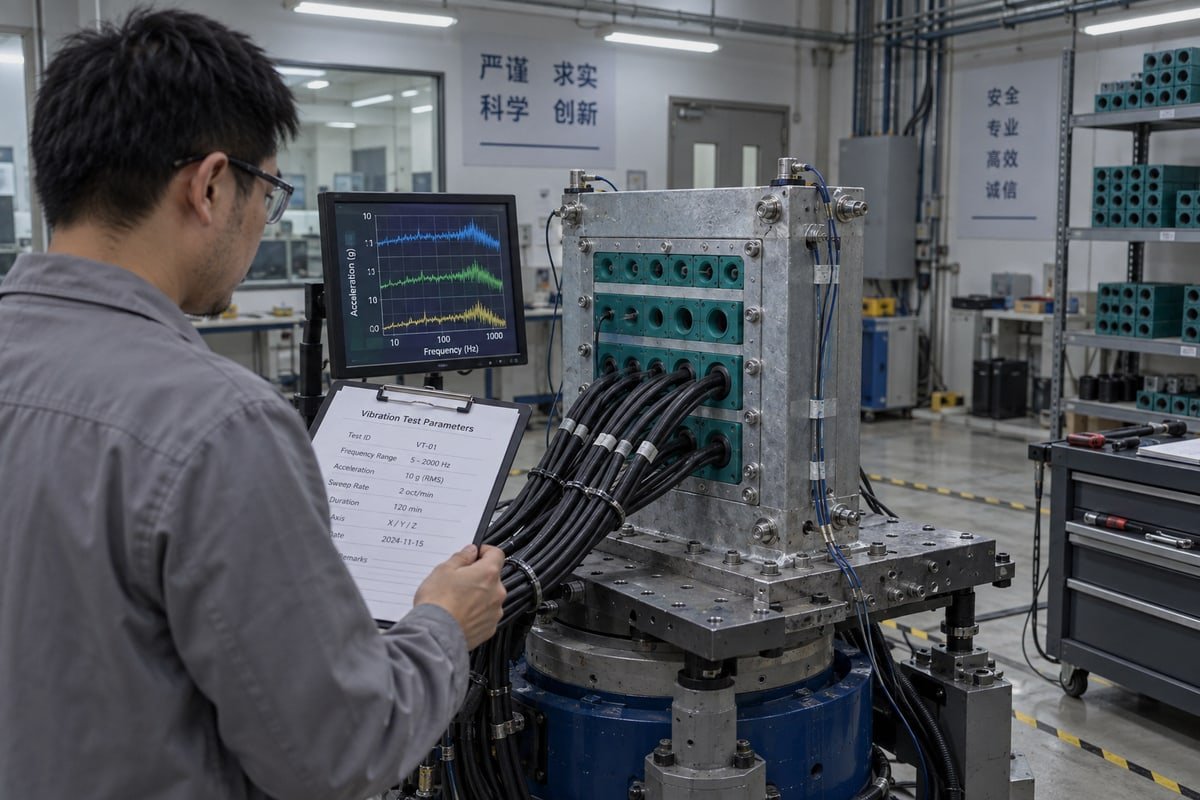
Start with the test method, not the headline
A useful report names the method. Random vibration and sine sweep testing under MIL-STD-810H 1 is one common route. Naval and marine qualification paths often run military vibration methods first, then shock, then fire-resistance testing in that order. One test package I have reviewed for a multi-cable transit seal combined shock at 100 g with vibration from 5–350 Hz, followed by a leak test. That last step is the important one. A frame can survive the shaker and still fail the seal check. "Survives transport" and "remains compliant after transport" are two different claims.
Check that the test covered the full assembly
Ask a direct question: was the shock and vibration testing run on the frame, sealing modules, stay plates, and compression unit together, or only on a rubber block? A component test can pass while the assembled multi cable transit frame loosens at the corners. Buyers in rail and marine now expect system-level qualification, and so do we when we review a competitor's claim for a cross-reference table.
| Document | What it must show | Red flag |
|---|---|---|
| Shock and vibration test report | Method, frequency range, g-level, duration, axes, sample description | No axes listed, or "component only" |
| Post-test leak or pressure test | Pressure held after dynamic loading | Leak test done only before vibration |
| Torque retention record | Bolt preload before and after test | No torque values at all |
| Material and weld certificates | Grade, yield, elongation, weld procedure | Only a trade name, no mill cert |
| Type Approval Certificate or factory approval | Issuing body and scope | Scope does not include the frame size you buy |
Match the standard to your transport route
If the frame ships offshore inside a container or skid, ask about DNV-ST-E271 or DNV 2.7-3. Those standards govern lifting and transport of portable units. They prove the packed unit and its lift points, not the frame alone. Also note that many standards define how to measure vibration but not what passes. Industrial-truck vibration standards, for example, characterize exposure; they are not acceptance criteria for a transit frame. So the report needs application-specific thresholds.
Some buyers tell me a generic test is enough. I disagree. Truck, rail, and offshore handling impose different frequencies and shock profiles. A test without the right boundary conditions can mislead you. From our side, we hand over the fire A-0/A-60, IP68 2, and watertight/gas-tight (0.01–0.4 MPa) test documents on request, plus material certificates, and we state plainly which results apply at assembly level. A structural integrity test tied to your route is worth far more than a badge on a brochure.
Can I Get Free Validation Samples to Test Lifting Durability on My Own Assembly Line?
During a batch inspection at our Shandong plant last spring, we pulled three TSC modules and ran a compression retention check before they went into sample kits.
Yes. We supply free validation samples of frames, sealing modules, compression units, and stay plates so your team can run lifting, torque retention, and vibration checks on your own line. Samples match the 120-frame dimensions, so results transfer directly to production.
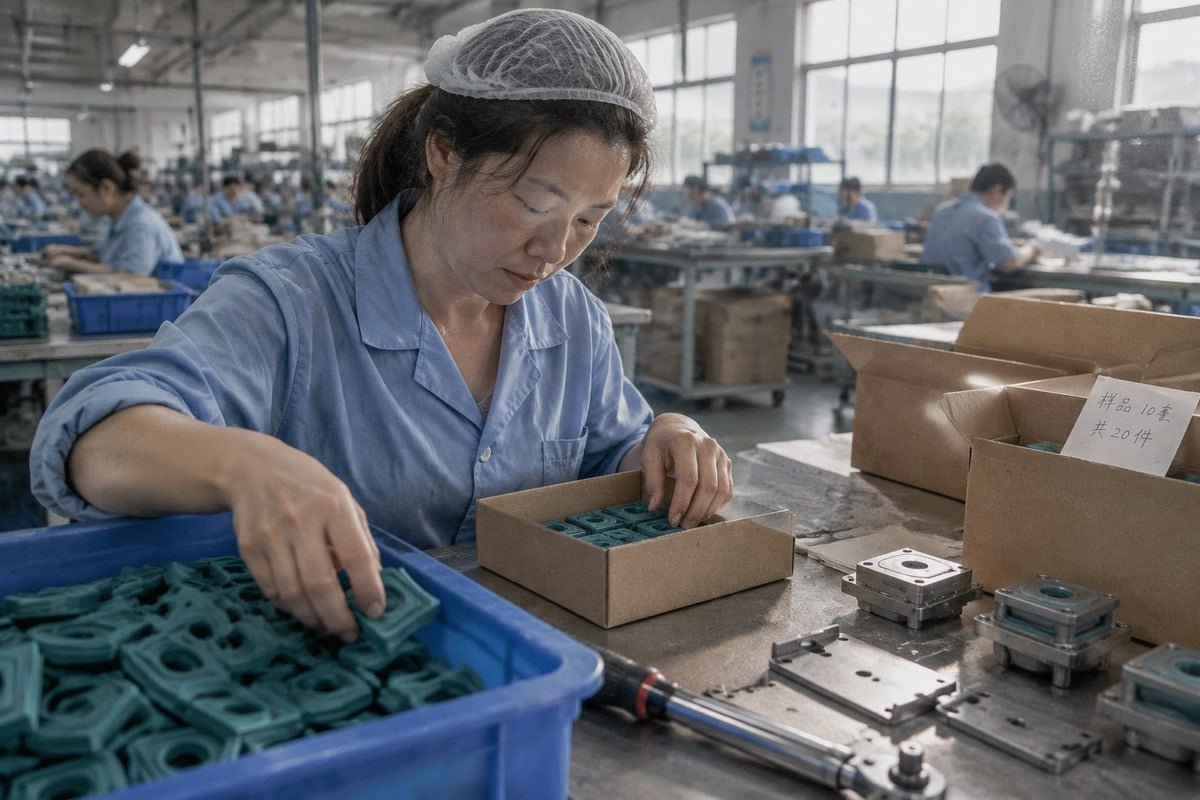
I always encourage buyers to test rather than trust. A sample costs us little, and it removes the argument about whose report to believe. Here is the process our European customers usually follow, refined from feedback we get on the returned samples.
A seven-step in-house validation routine
- Receive the kit. Check the frame against the cross-reference table and the CAD/STEP file we send with it.
- Record the baseline. Photograph the frame, measure the opening, and note the torque on each compression bolt and the wedge setting.
- Populate it realistically. Cable fill density changes the assembly's damping and natural frequency. A half-empty frame behaves differently from a full one, so fill it as production would.
- Fit stay plates between block rows. They distribute mechanical load and stop the rows from telescoping under shock.
- Lift it the way you ship it. Sling from your real lift points or cradle. Measure deflection at the corners.
- Shake it or ship it. Use a shaker table with a MIL-STD-810H profile, or strap the sample to a pallet on a real truck run with tri-axial accelerometers logging g-loads. Compare the logged data against the test profile you plan to specify.
- Inspect after the run. Re-torque and record the drop, check compression wedge retention force, pull on a cable to confirm cable retention strength, and run a pressure or leak test.
What counts as a pass
| Check | Pass criterion |
|---|---|
| Frame geometry | No permanent deformation at corners or bolt holes |
| Bolt torque | Preload loss within your allowable tolerance |
| Module position | No block movement, no visible gap opening |
| Cable retention strength | Cables hold under your specified pull load |
| Leak test | Pressure held at the rated level after vibration |
Some engineers argue that a properly bolted frame with compressive EPDM modules makes vibration a non-issue. In practice, the failures I have traced were cumulative. Small preload loss on each transport leg, one forklift bump, and a seal that looked fine but no longer held pressure. This kind of environmental stress screening on your own line catches that before a container of switchgear reaches site. Our step-core, halogen-free EPDM modules adapt to a range of cable diameters within one size, which also means your fill pattern on the sample can mirror production exactly.
How Do I Know a Drop-In Replacement Frame Will Match the Structural Strength of My Current 120-Frame Standard?
A purchasing engineer in Germany once sent us his existing frame drawing and asked a blunt question: same cutout, fine, but is the steel actually as strong?
Compare the drop-in frame against your current 120-frame standard on wall thickness, material grade, weld type, corner geometry, and compression unit load, using the supplier's cross-reference table and CAD/STEP files. Then run a structural integrity test on a validation sample under your own lifting and vibration profile.
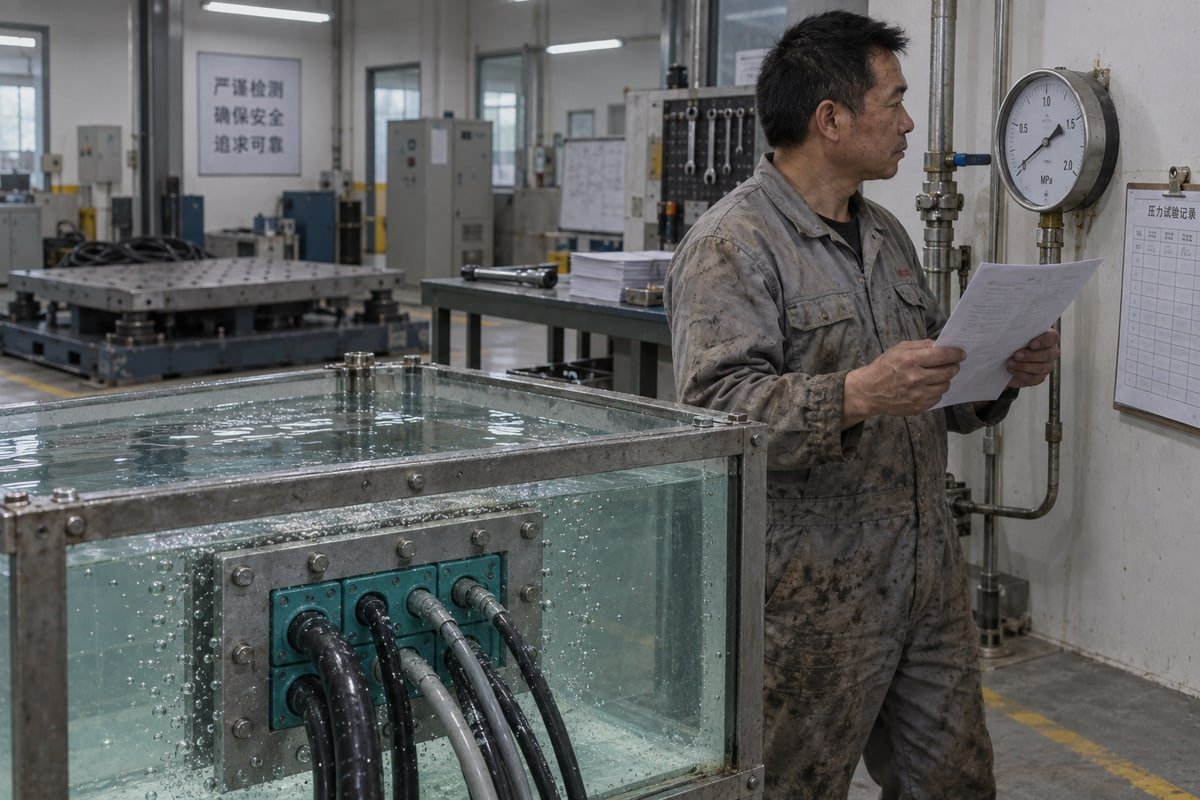
Dimensional compatibility is the easy part. Our frames are built to drop into common 120-frame cutouts, and the cross-reference table maps each existing model to a DEWIN model. Strength matching takes a closer look. That is fair. Our position is that a qualified second source has to prove equivalence, not just fit.
Parameters that actually govern strength
| Parameter | Why it matters under lifting and vibration | How to compare |
|---|---|---|
| Frame wall thickness | Sets bending stiffness during a sling lift | Measure the sample, compare drawings |
| Material grade and ductility | Fatigue resistance under repeated transport cycles | Mill certificate, elongation value |
| Weld type and corner geometry | Corners concentrate stress and crack first | Weld map, visual and NDT results |
| Bolt hole pattern and edge distance | Point loads pass through the bolts into the bulkhead | CAD/STEP overlay |
| Compression unit load | Keeps modules seated so the frame and blocks act as one system | Wedge retention force record |
Where frames fail, and why
Load travels from the crane hook or forklift tine into the cradle, then into the frame corners, then through the mounting bolts into the surrounding bulkhead, and finally into the sealing modules. Corners, bolt holes, and interfaces between dissimilar materials are the usual weak points. A galvanized steel frame bolted to an aluminum enclosure, for example, needs attention at the joint because the two materials respond to vibration differently.
Use analysis before you use the shaker
Mechanical stress analysis with Finite Element Analysis 3 lets you run a modal study on the populated frame. The goal is to keep the assembly's resonance frequency away from the dominant frequencies of the transport vehicle. If your BESS container will also face a seismic resilience requirement, the same model helps. We share STEP files so your engineers can run that comparison against your existing frame model without waiting on us. Then the physical test on the sample confirms the model. That order, analysis first and test second, is what our engineering team recommends, and it is how we approach custom sizes from our in-house mold shop.
What Certifications and Material Specifications Confirm the Frame Handles Transport Stress Without Deforming?
Every time we quote a frame for an offshore route versus a factory floor, I weigh the same trade-off: corrosion margin against ductility, weight, and handling loads.
Look for ISO 9001 or IATF 16949 quality systems, a classification society approval such as BV or DNV GL certification, material certificates with yield and elongation values, weld procedure records, and fire (A-0/A-60), IP68, and pressure test reports proving the frame keeps sealing after mechanical stress.
Certificates only help if you know what each one proves. Some cover the factory. Some cover the material. Some cover the finished performance. You need all three layers to close the loop on transport stress.
| Evidence | Layer | What it confirms about transport survival |
|---|---|---|
| ISO 9001 4 / IATF 16949 | Factory system | Repeatable production and traceable inspection records |
| BV approval, DNV GL certification, Type Approval Certificate | Third-party review | An independent body has checked the product scope and test basis |
| Material certificate (grade, yield, elongation) | Material | Enough ductility to absorb shock without cracking |
| Weld procedure and weld penetration inspection | Fabrication | Corner welds carry load rather than just holding shape |
| Fire A-0/A-60, IP68, 0.01–0.4 MPa pressure reports | Performance | The sealed system still functions after handling |
Material specifications that resist deformation
A frame that deforms is usually a frame with the wrong balance of strength and ductility. High-strength steel with low elongation can crack at a corner under a sharp shock. A more ductile grade bends slightly and recovers. Ask for elongation values on the mill certificate, not just yield. For the sealing side, our modules use halogen-free EPDM. That matters because the rubber both damps vibration and has to hold compression after it. A brittle elastomer would lose sealing force on the first cold transport leg.
Welds and post-transit inspection
Weld penetration inspection at the factory is the first gate. Full-penetration corner welds spread load; a shallow weld leaves a notch that fatigue will find. After transport, mandatory visual inspection and re-torquing of the compression units keep seal integrity. For critical installations, non-destructive testing 5 on the corner welds, such as dye penetrant, picks up vibration-induced micro-fractures that a visual check misses.
Vendor declaration or independent proof?
Here is a buyer objection I hear often: a signed vendor declaration should be enough. For a frame in a data center wall, maybe. For a marine bulkhead or a rail cabin, no. Third-party evidence is stronger because the reviewer has no stake in the sale. Our factory is BV-approved, and our fire, IP68, and pressure test documents are available on request. If your class society requires DNV GL certification for a specific project, raise it early so the approval scope is checked before the frame is specified. Naval qualification paths follow a logic worth copying: vibration under military methods, then shock, then fire-resistance testing, with the seal verified at the end. That sequence proves the frame handles transport stress and still does its real job.
Conclusion
Transport can quietly undo a good seal. Ask for full-assembly test evidence, then verify on free samples. Our team shares reports, cross-reference tables, and CAD files on request.
Footnotes
1. Widely referenced US military standard for shock and vibration testing methods mentioned repeatedly. ↩︎
2. ISO reference for ingress protection rating standard used to prove sealing performance. ↩︎
3. Background explanation of the modal/structural analysis method referenced for modal study. ↩︎
4. Official ISO reference for the quality management standard cited as certification evidence. ↩︎
5. Background concept for weld inspection methods like dye penetrant testing mentioned in article. ↩︎


 English
 Español de México
 Deutsch
 Français
 العربية
 Русский