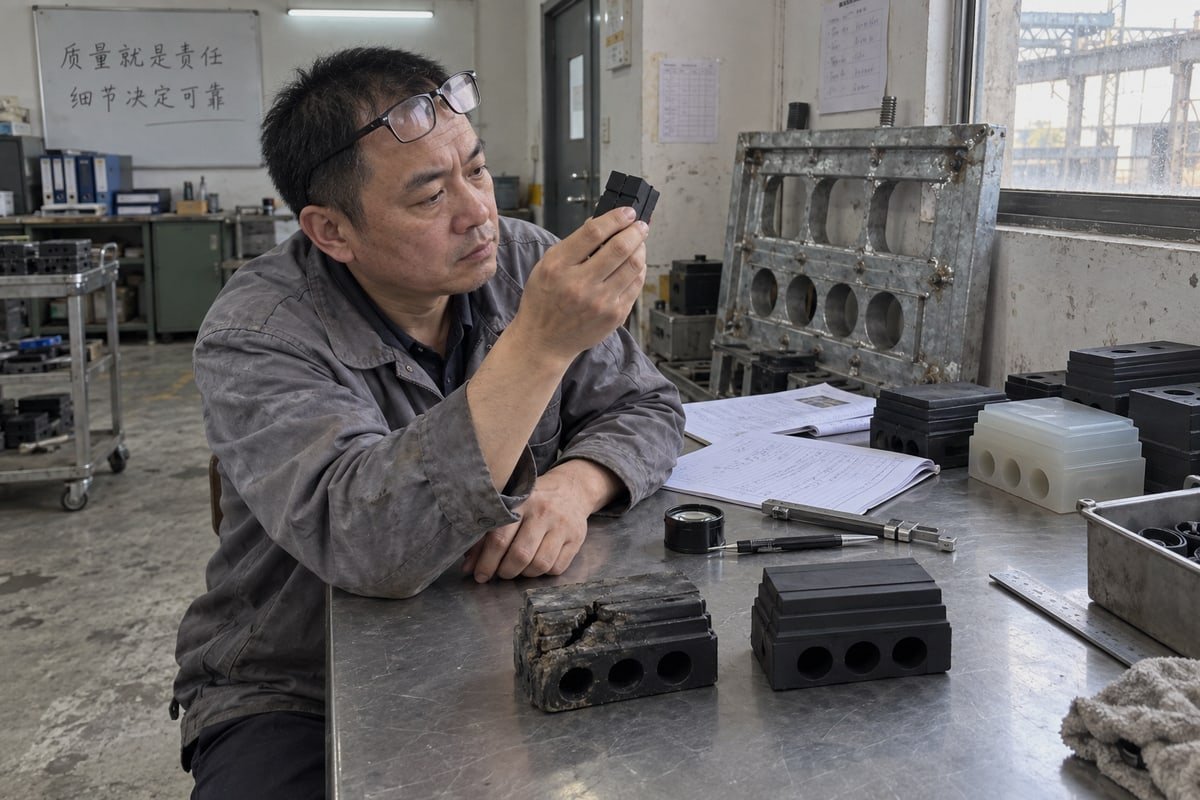
Pick the wrong rubber materials for cable transit sealing modules and the leak shows up years later. I have seen returned modules on our inspection bench that prove it.
Cable transit sealing modules use three rubber materials: EPDM, neoprene, and silicone. Halogen-free EPDM is the standard for fire-rated, marine, and outdoor transits. Neoprene suits oil-adjacent industrial sites. Silicone covers extreme temperatures from -60°C to over 200°C.
The base polymer is only half the story. Compound formulation, Shore A hardness 1, and the test certificate behind the module matter just as much. Below, I walk through each material the way our own engineers do when a buyer sends us a spec sheet.
Why Do I Need Halogen-Free EPDM Instead of Neoprene or Silicone for Fire-Rated Cable Transits?
During a burn test on our A-60 modules, the lab technician checked the smoke chamber before the flame. That order matters, and it explains why we use halogen-free EPDM.
Fire-rated cable transits need halogen-free EPDM because neoprene contains chlorine and releases corrosive acid gases when burned. Halogen-free EPDM delivers low smoke toxicity, holds A-0/A-60 fire ratings when correctly formulated, and keeps UV and ozone resistance for outdoor or marine service at lower cost than silicone.
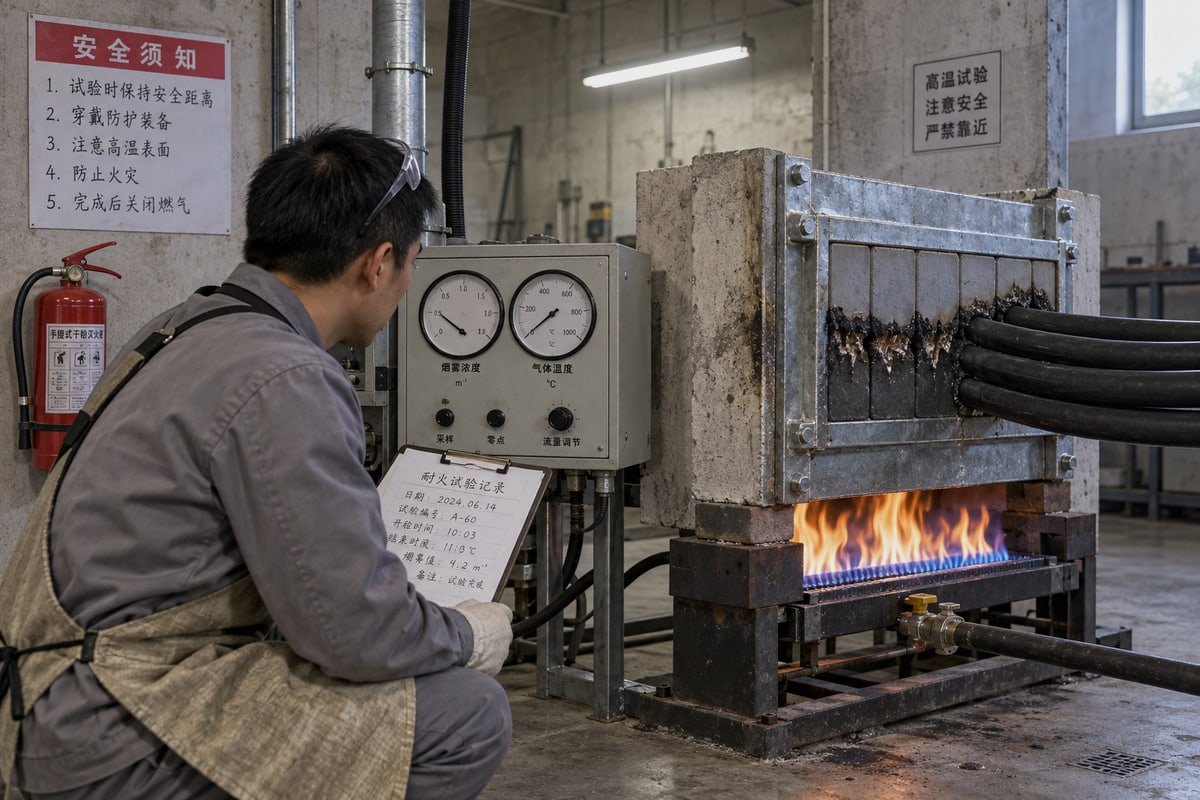
The word "fire-rated" hides two separate questions. Does the seal hold? And what comes out of the rubber while it holds? Buyers often check only the first one.
What halogen-free actually means when the module burns
Neoprene is chloroprene rubber. Chlorine sits in its polymer backbone. That chlorine makes neoprene self-extinguishing without additives. This is why neoprene shows up in general-purpose fire-stop products. But the same chlorine turns into hydrogen chloride gas 2 in a fire. Mix that gas with moisture and you get hydrochloric acid 3 on switchgear busbars, on data center racks, and on the inside of a BESS container. The fire may stay on one side of the bulkhead. The corrosion still ruins the electronics on the other side.
Halogen-free materials avoid this failure. Our step-core modules use an EPDM compound with no chlorine, bromine, or fluorine in the recipe. The flame retardancy comes from mineral fillers, not halogens. When the module is tested to an A-0 or A-60 fire resistance rating in the frame, the protected side stays sealed and the smoke stays low in toxicity. That is the behavior IMO FTP 4 testing looks for in marine and offshore applications. It is the same behavior modular data center builders now write into their tender documents.
Is silicone the safer premium choice for fire?
This is the objection I hear most often from European purchasing engineers. Silicone survives continuous heat that EPDM cannot. That is true. But a fire-rated transit is not judged by continuous heat. It is judged by whether the seal holds through the test curve and whether the smoke is survivable. A properly formulated halogen-free EPDM passes A-0 and A-60 in the frame. Silicone adds cost without adding rating at the bulkhead. I recommend silicone only when the normal operating temperature is already extreme, not as a fire upgrade.
| Property | Halogen-free EPDM | Neoprene | Silicone |
|---|---|---|---|
| Halogen content | None | Chlorine in the polymer | None |
| Smoke behavior in fire | Low smoke toxicity | Corrosive acid gas | Low smoke toxicity |
| Fire rating path | A-0/A-60 tested in frame | Depends on compound | Depends on compound; UL 94 V-0 common |
| Relative module cost | Baseline | Similar to EPDM | Premium |
How Do EPDM, Neoprene, and Silicone Compare in Temperature and Chemical Resistance for My Application?
Every compound we specify balances two enemies: heat and oil. Our engineers weigh that trade-off before we cut a mold, because no single rubber wins both.
EPDM offers the best UV and ozone resistance and handles water, steam, and mild acids, but swells in petroleum oil. Neoprene tolerates moderate oil and grease with average weathering. Silicone keeps elasticity from -60°C to over 200°C but has weaker oil resistance and costs more.
I find a table settles more arguments than a paragraph. Here is the comparison our team uses when a spec sheet lands on my desk.
| Factor | EPDM | Neoprene | Silicone |
|---|---|---|---|
| Service temperature | Broad, but ceiling sits below silicone | Narrowest of the three | Widest: -60°C to over 200°C |
| UV and ozone resistance | Excellent | Moderate | Excellent |
| Petroleum oil and grease | Poor; swells and softens | Moderate; best of the three | Poor to moderate |
| Water, steam, mild acids and alkalis | Excellent | Good | Good |
| Outdoor aging and service life | Very long | Medium | Very long |
| Relative cost | Low | Low to medium | High |
Reading the temperature column honestly
Silicone's -60°C to over 200°C range is real. The question is whether your transit ever sees it. A switchgear room, a BESS container, or a data center wall sits well inside the EPDM window. A furnace penetration or an engine room bulkhead next to an exhaust manifold may not. In my experience, most buyers who ask for silicone are paying for a temperature margin they will never use. The lifecycle-risk argument for silicone only holds when the environment is genuinely extreme.
Chemical resistance properties: the oil question
Here is where I raise the neoprene objection myself. Some engineers say neoprene is underrated. I agree in one narrow case. If cables run through a transit where hydraulic oil 5, diesel, or grease can pool against the rubber, EPDM will swell. Swelling loses compression, and lost compression means a lost seal. Neoprene resists that oil better. So for an oil-adjacent industrial penetration with no strict smoke-toxicity requirement, neoprene is a valid choice. For everything else I still start with EPDM.
A simple decision tree
- Outdoor, marine, utility, or fire-rated with low smoke toxicity required: halogen-free EPDM.
- Regular contact with petroleum oil or grease, indoor, no strict toxicity limit: neoprene.
- Continuous service above the EPDM ceiling or below -40°C: silicone.
- Tropical or subsea exposure with biological growth risk: ask for a biocide-infused compound in any of the three.
Which Rubber Material Will Meet My IP68 and Gas-Tight Sealing Certification Requirements?
A sourcing engineer in Germany once emailed me a single question: which rubber passed your IP68 test? The honest answer needed a full page, not one word.
All three rubbers can pass IP68 ingress protection and gas-tight tests if the compound has low compression set and correct Shore A hardness. Halogen-free EPDM is the proven choice; certified modules are tested to IP68 and 0.01–0.4 MPa watertight and gas-tight sealing, with test documents available on request.
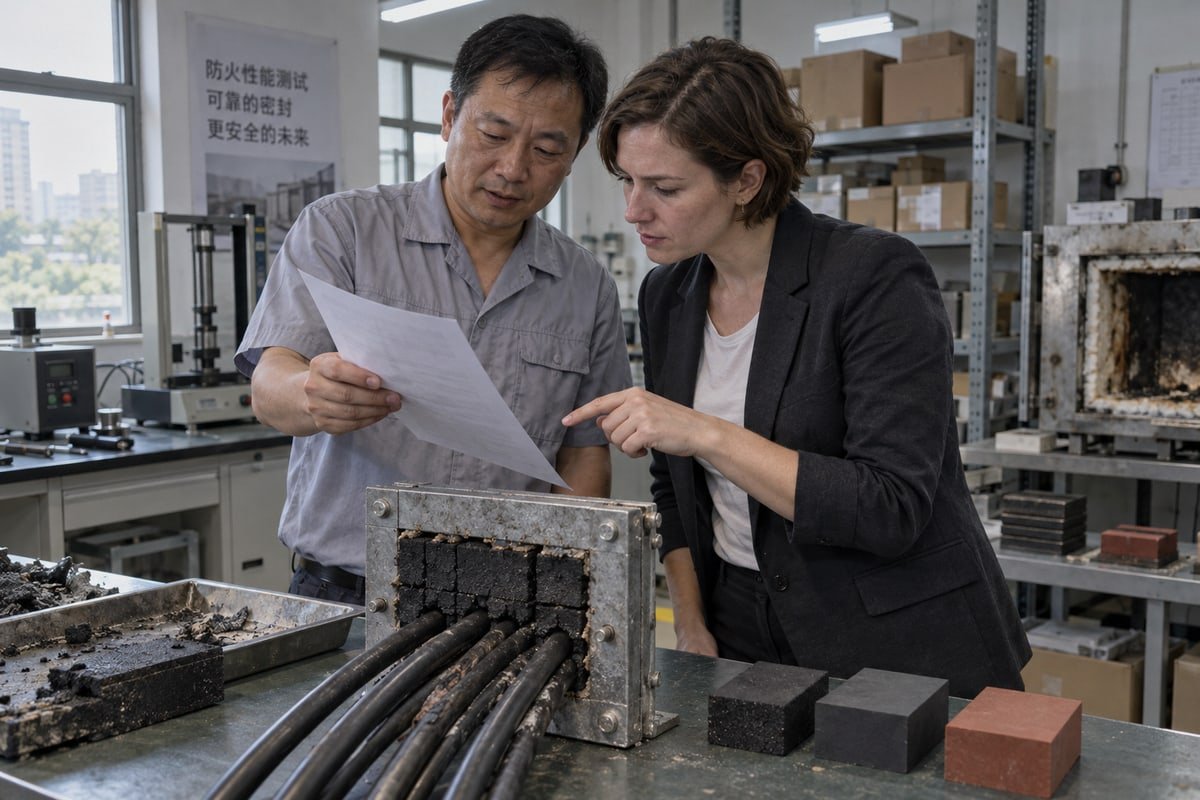
The certificate belongs to the module in the frame, not to the polymer. That distinction saves buyers from a common mistake: assuming an "EPDM module" from any source carries the same rating.
How the seal is actually created
- The installer strips the step-core layers until the bore matches the cable diameter.
- Modules and stay plates fill the frame in rows.
- The compression wedge is tightened at the top of the frame.
- Wedge pressure travels down through the stack and forces each module against the cable jacket and its neighbors.
- The rubber must hold that pressure for decades without relaxing.
Step five is where the material matters. Low compression set means the rubber springs back instead of taking a permanent set. A module with poor compression set passes the test on day one and leaks on year five.
Shore A hardness and compression set
Hardness controls how the rubber flows around the cable. Too soft and the wedge crushes the module. Too hard and the rubber never conforms to the jacket. Transit-grade EPDM typically sits around 50 to 60 Shore A, while silicone modules span roughly 40 to 60 Shore A. We check hardness on every production batch under our ISO 9001 and IATF 16949 systems because a 10-point drift changes sealing pressure noticeably.
Standards that decide the material
| Requirement | What it tests | Material implication |
|---|---|---|
| IP68 ingress protection | Continuous immersion | Low compression set; any polymer with the right hardness |
| Gas tightness standards (0.01–0.4 MPa) | Pressure differential across the frame | Same as above, verified in the frame |
| A-0/A-60 fire resistance rating | Bulkhead integrity under fire curve | Halogen-free compound with mineral flame retardants |
| IMO FTP | Marine fire, smoke, toxicity | Halogen-free EPDM or silicone |
| ATEX | Explosive atmospheres | Gas-tight seal plus non-sparking, antistatic compound |
| BV factory approval | Production consistency | Batch traceability, not a polymer choice |
One trend worth noting: hybrid EPDM compounds with nickel-graphite or silver-plated glass fillers now offer EMC shielding inside the same environmental seal. That helps switchgear and data center integrators, but ask for the IP68 report on the filled compound, not the base one.
Can I Switch From Neoprene or Silicone Modules to EPDM Without Changing My Existing Frame Dimensions?
We learned early that a module can be chemically perfect and still fail qualification because it sits proud of the frame. Dimensions decide the drop-in.
Yes. Switching from neoprene or silicone modules to EPDM does not require new frames when the EPDM modules follow common 120-frame standards. Module height, width, and depth stay identical, the compression wedge and stay plates are reused, and only the elastomer and its cable-diameter range change.
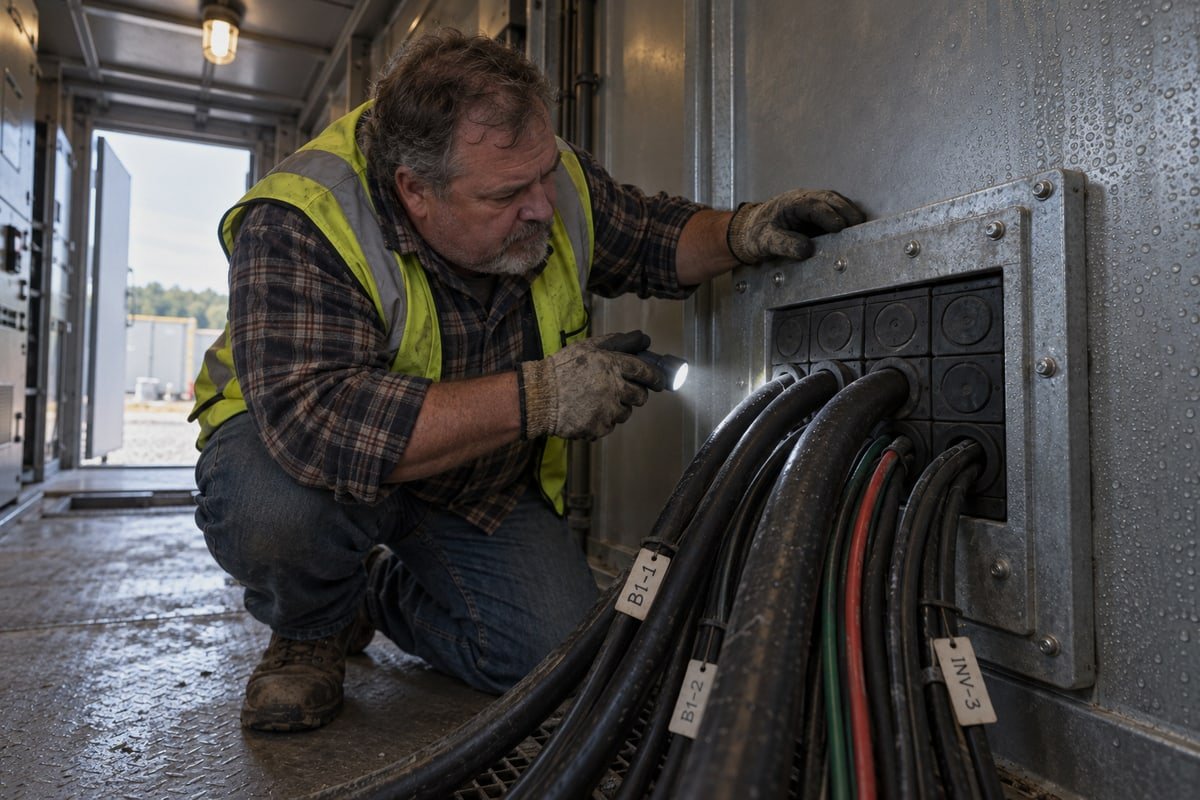
Frames are welded into bulkheads and container walls. Replacing them means hot work, re-certification, and downtime. So the only realistic path is a module that fits the frame you already own.
What changes and what stays the same
| Item | Stays the same | Changes |
|---|---|---|
| Frame cutout and weld | Yes | No |
| Stay plates | Yes | No |
| Compression wedge | Yes | No |
| Module outer dimensions | Yes, on 120-frame standard | No |
| Elastomer | — | Neoprene or silicone to halogen-free EPDM |
| Cable diameter range per module | — | Step-core widens the range in one size |
| Test documents | — | New IP68, gas-tight, and A-0/A-60 reports for the EPDM module |
A five-step qualification path for a second source
- Send us your current module part numbers. We return a cross-reference table mapping each existing model to a DEWIN TSC square module or TSR round assembly.
- Request free validation samples. We ship them for a fit check in your actual multi-cable transit frames.
- Download CAD/STEP files for the drawing review your engineering team will insist on.
- Review the test documents: IP68, 0.01–0.4 MPa gas-tight, A-0/A-60, plus BV factory approval.
- Run a pilot lot, then move volume. Buyers typically see 40–60% lower module cost against the incumbent brand.
Why the elastomer swap is easier than it looks
The rubber materials for cable transit sealing modules are held inside a rigid frame. The frame sets the geometry. As long as the module matches the standard cutout and the compound sits in the normal Shore A window, the compression unit does its job the same way. Our in-house mold shop handles custom sizes and private-label marking when the frame is non-standard.
One more trend helps here. Low-friction EPDM formulations with internal lubricants reduce the push force on dense bundles. Installers report less stiction and fewer scuffed jackets, which matters when BESS integrators pack dozens of DC cables through one frame.
Conclusion
Wrong rubber, hidden leak, costly retrofit. Halogen-free EPDM covers most fire-rated, marine, and outdoor transits; reserve silicone for extreme heat, neoprene for oil. Request cross-reference tables and samples first.
Footnotes
1. Authoritative definition of the hardness scale used to specify rubber module compression properties. ↩︎
2. Technical chemical data from NIH regarding the toxic gas released by burning halogenated polymers. ↩︎
3. Authoritative safety resource for chemical hazards like hydrochloric acid mentioned in the text. ↩︎
4. Official International Maritime Organization page regarding fire test procedures for marine safety. ↩︎
5. Reference for the chemical properties of hydraulic fluids that can cause EPDM swelling. ↩︎



 English
 Español de México
 Deutsch
 Français
 العربية
 Русский